Rugged Elastomer
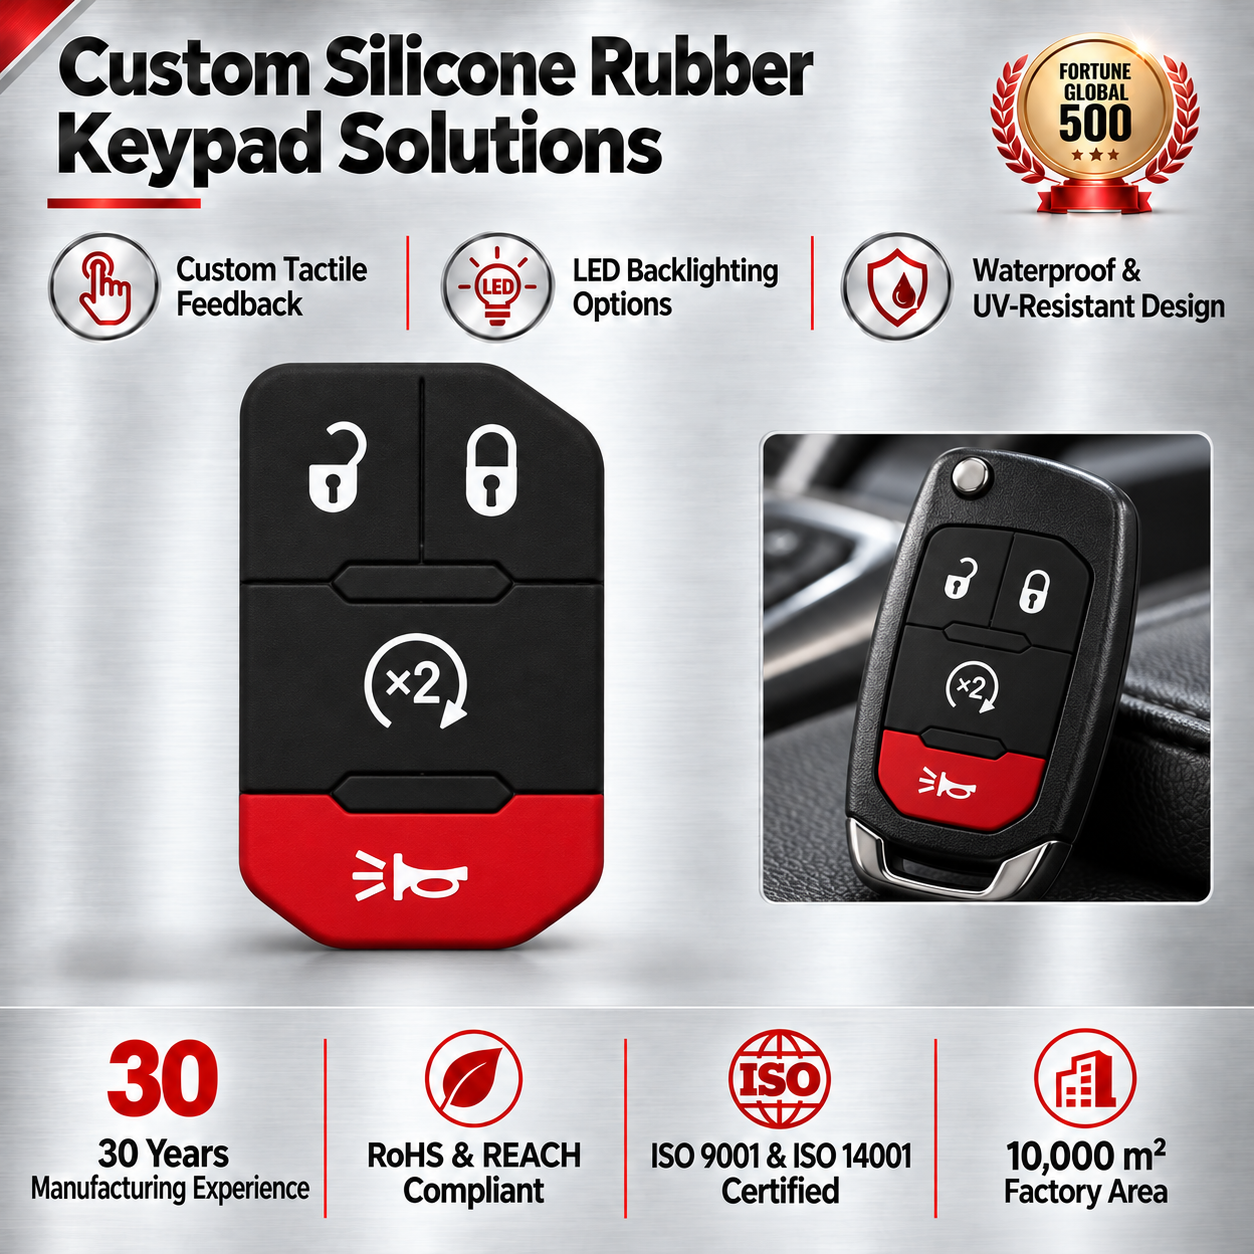
Waterproof 4-Button Silicone Car Key Cover & Keypad
- Material:Medical/Automotive Grade Silicone
- Sealing:IP67 Submersible
- Key Feel:Elastomeric Snap Response
Custom tactile stack-ups engineered with ISO9001/IATF16949 standards, high chemical resistance, and 5-million-cycle actuation longevity.
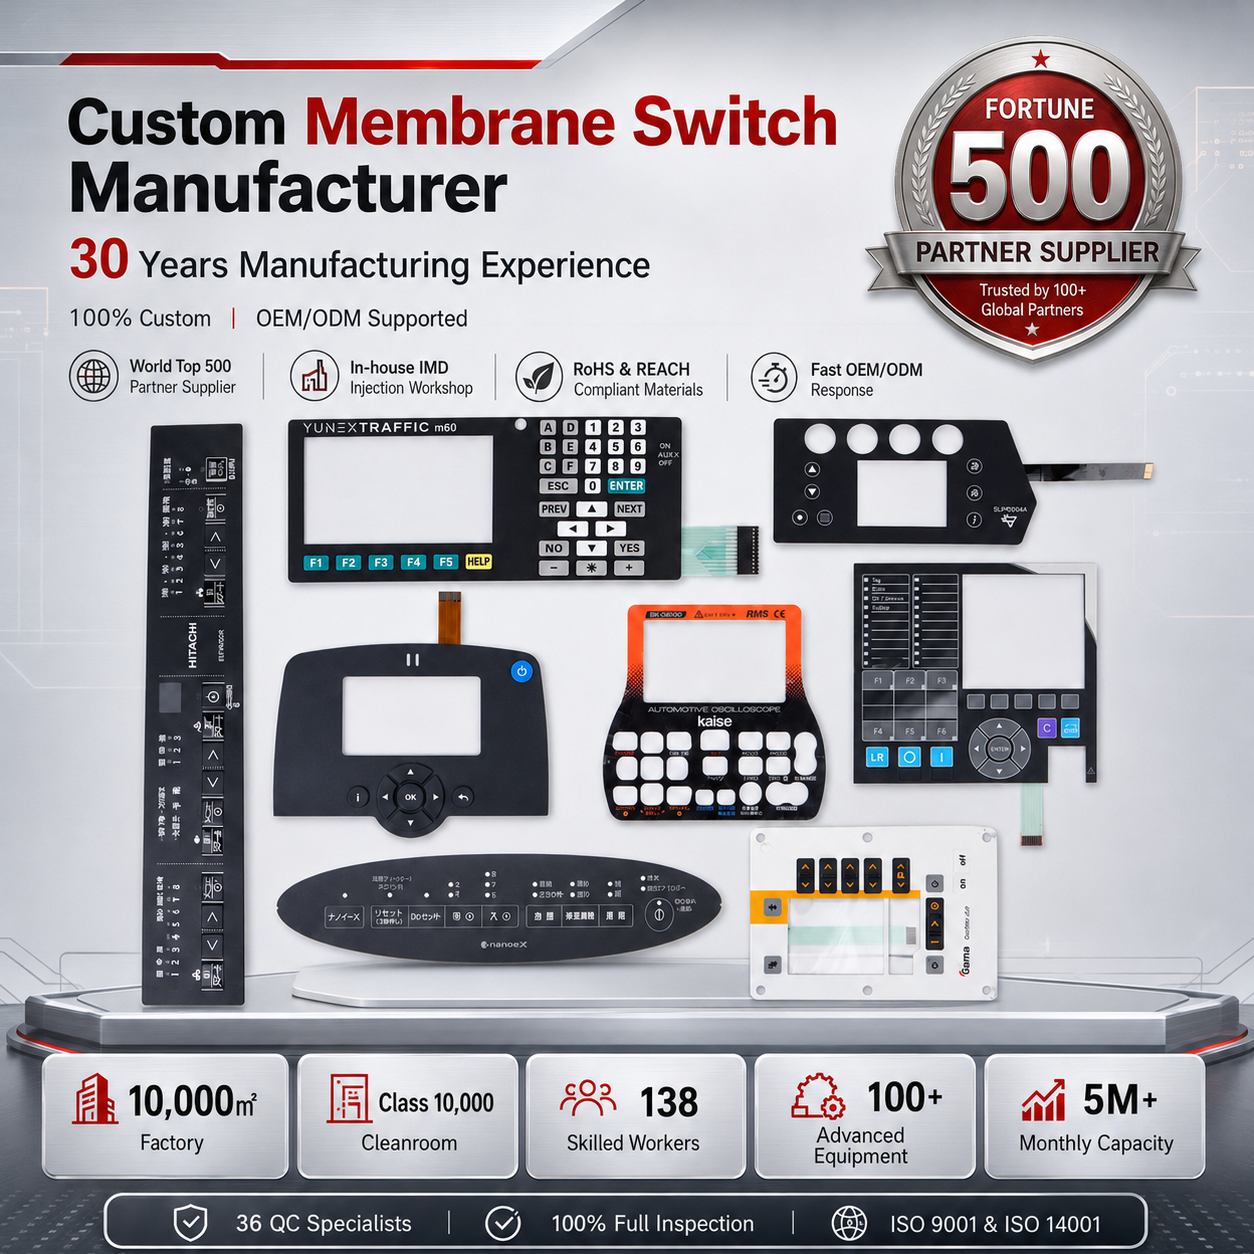
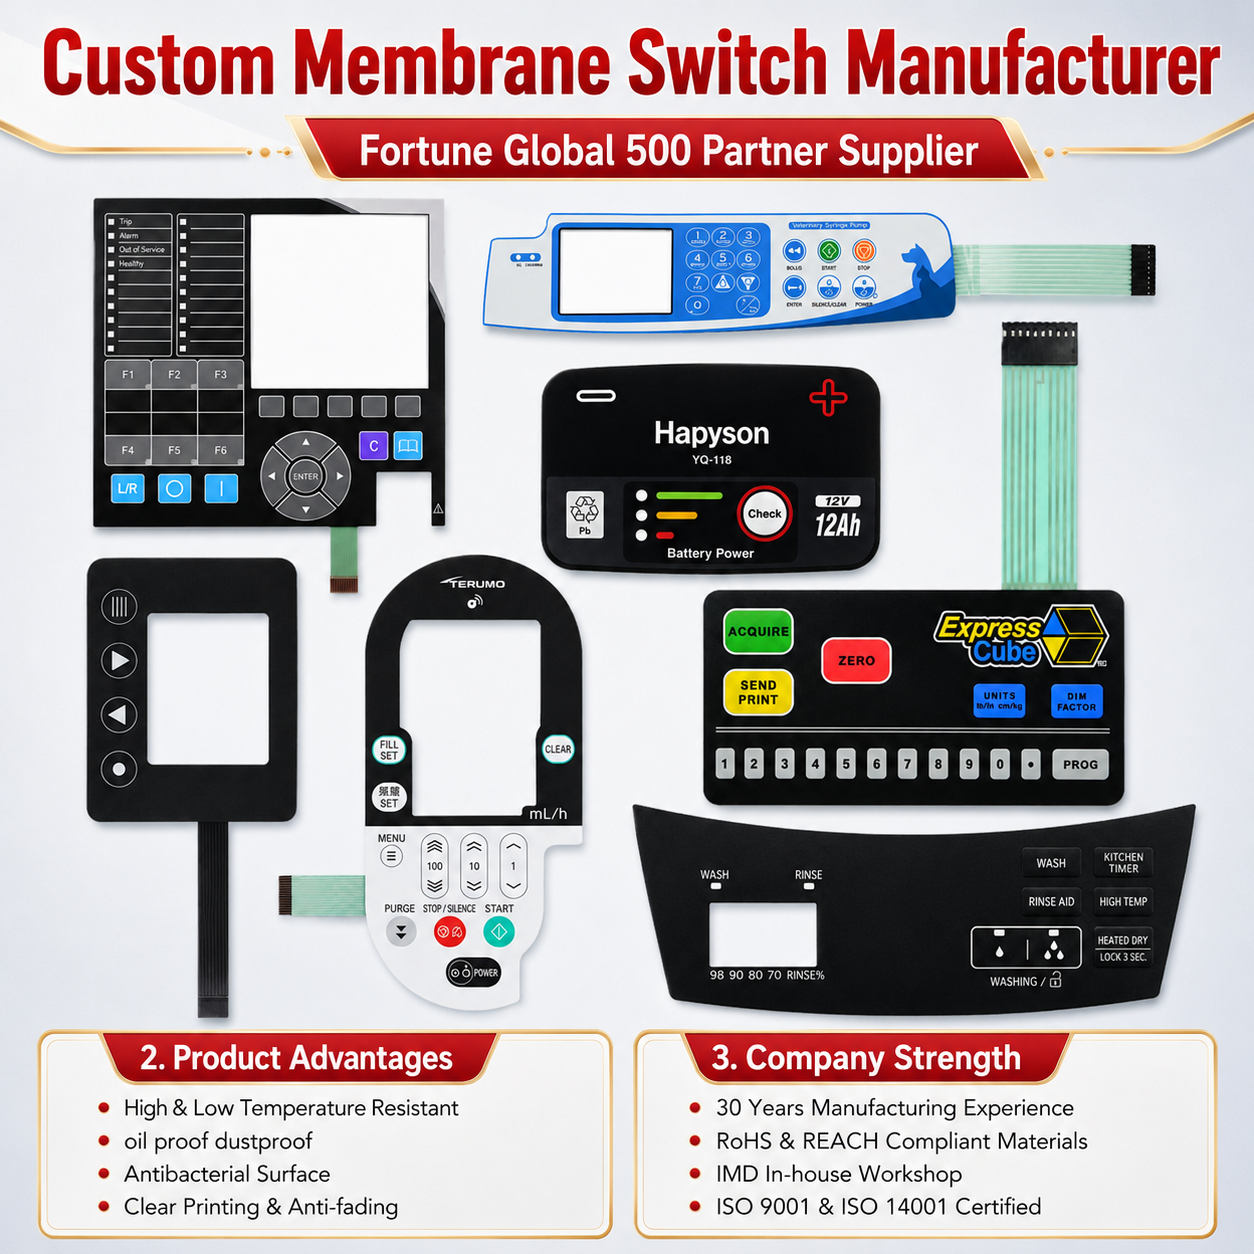
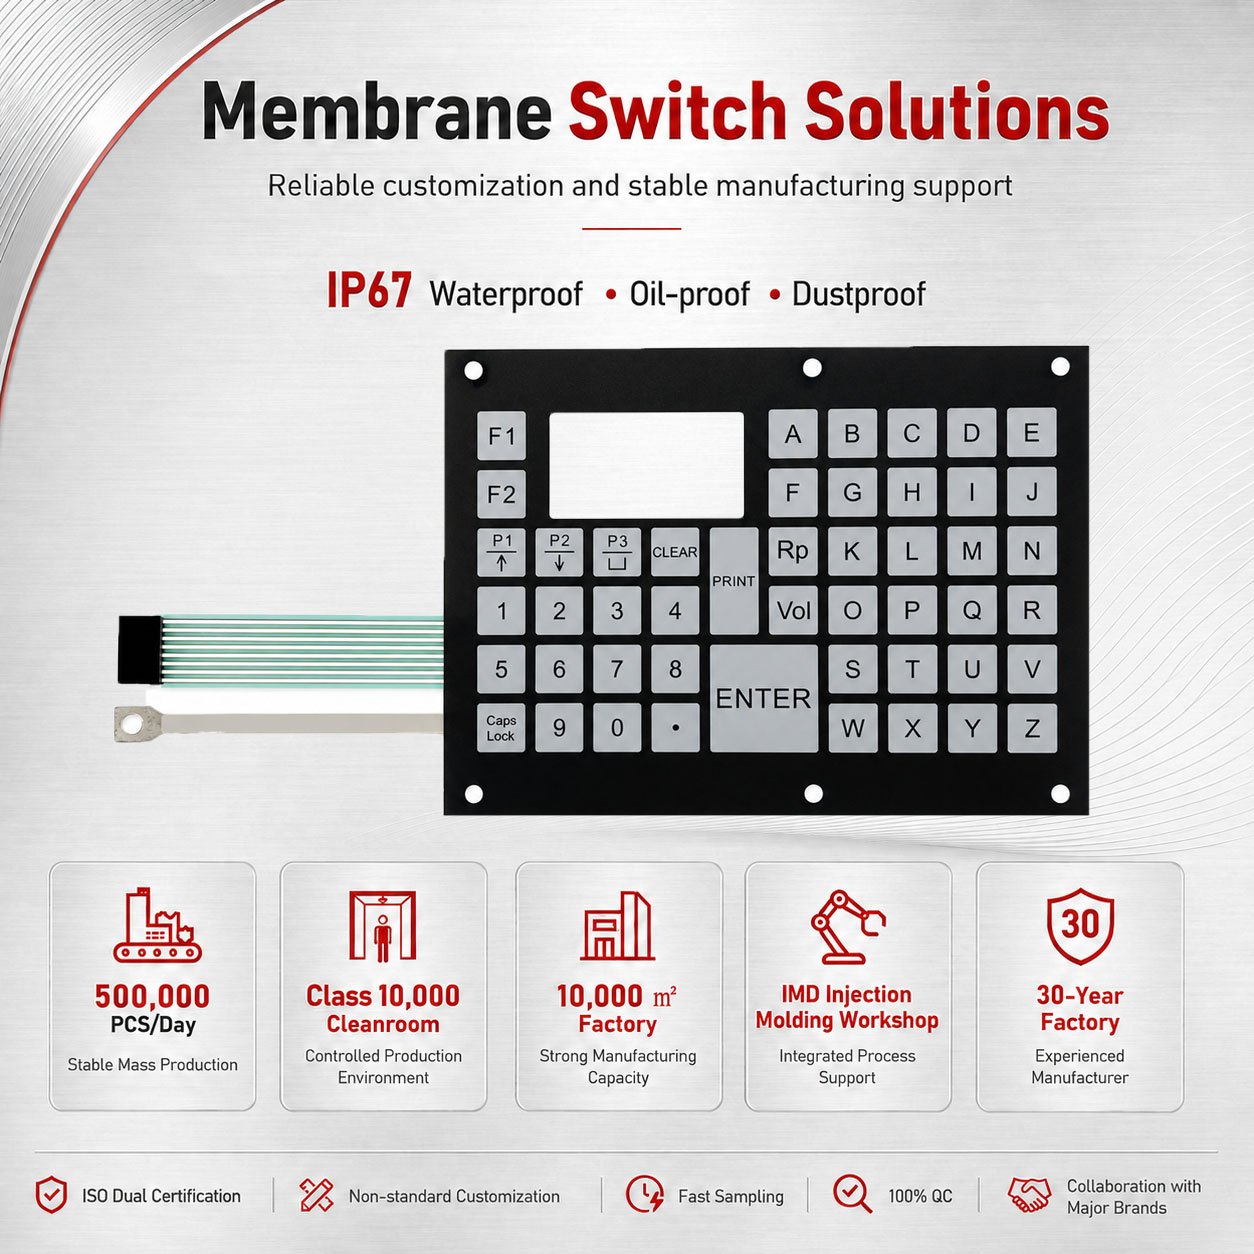
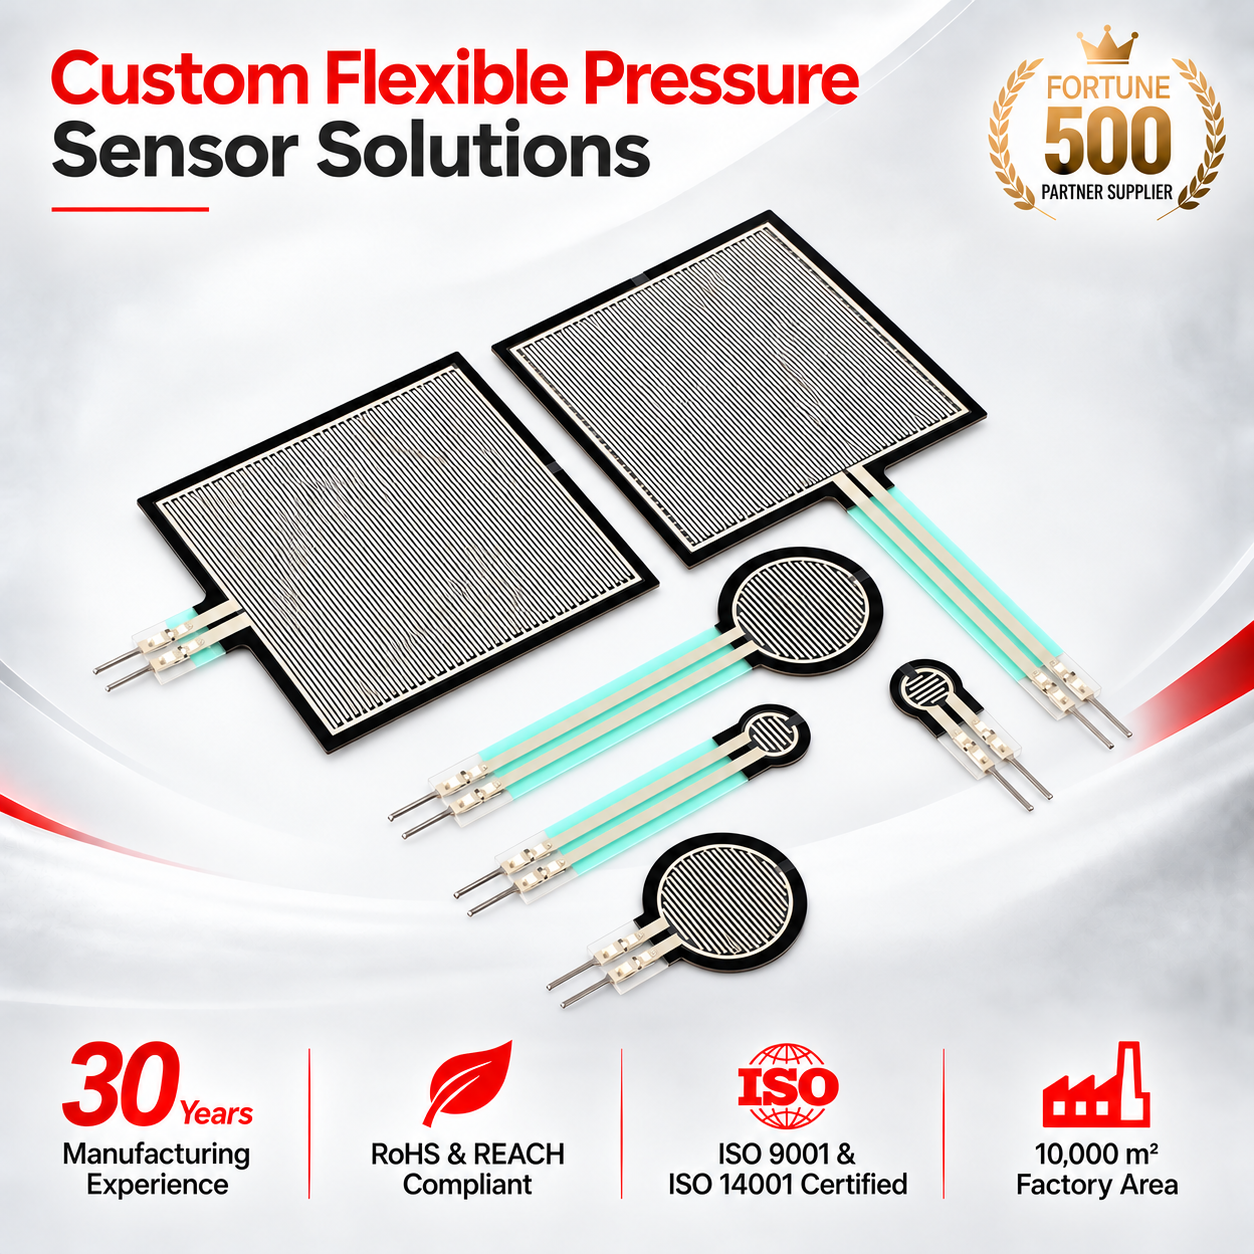
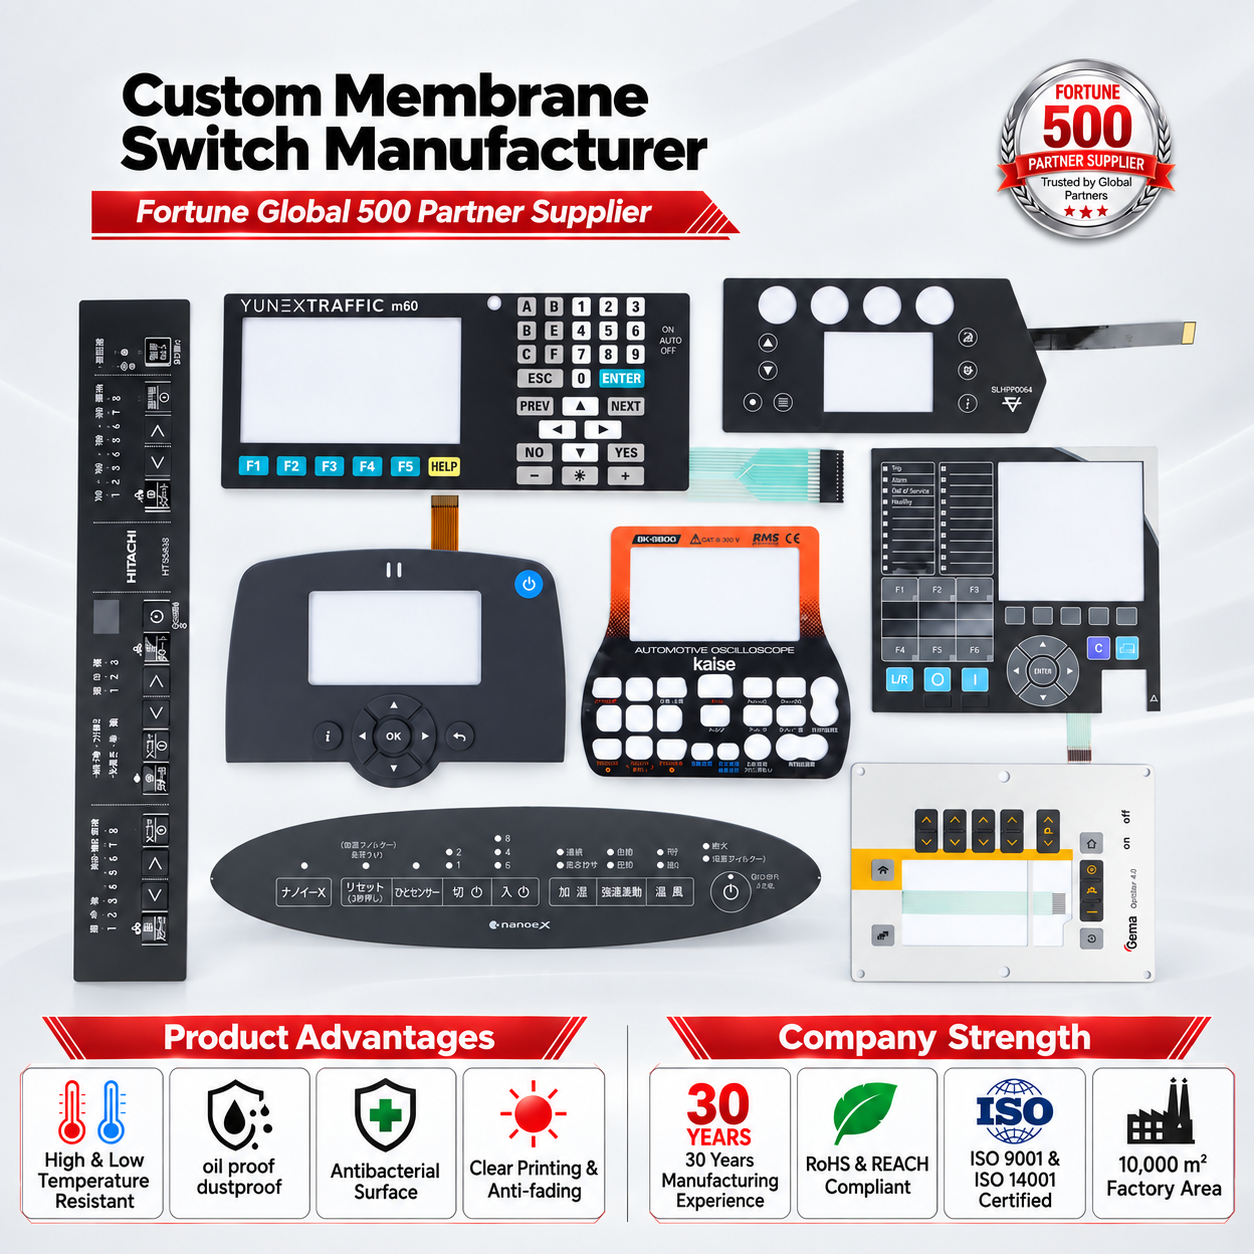
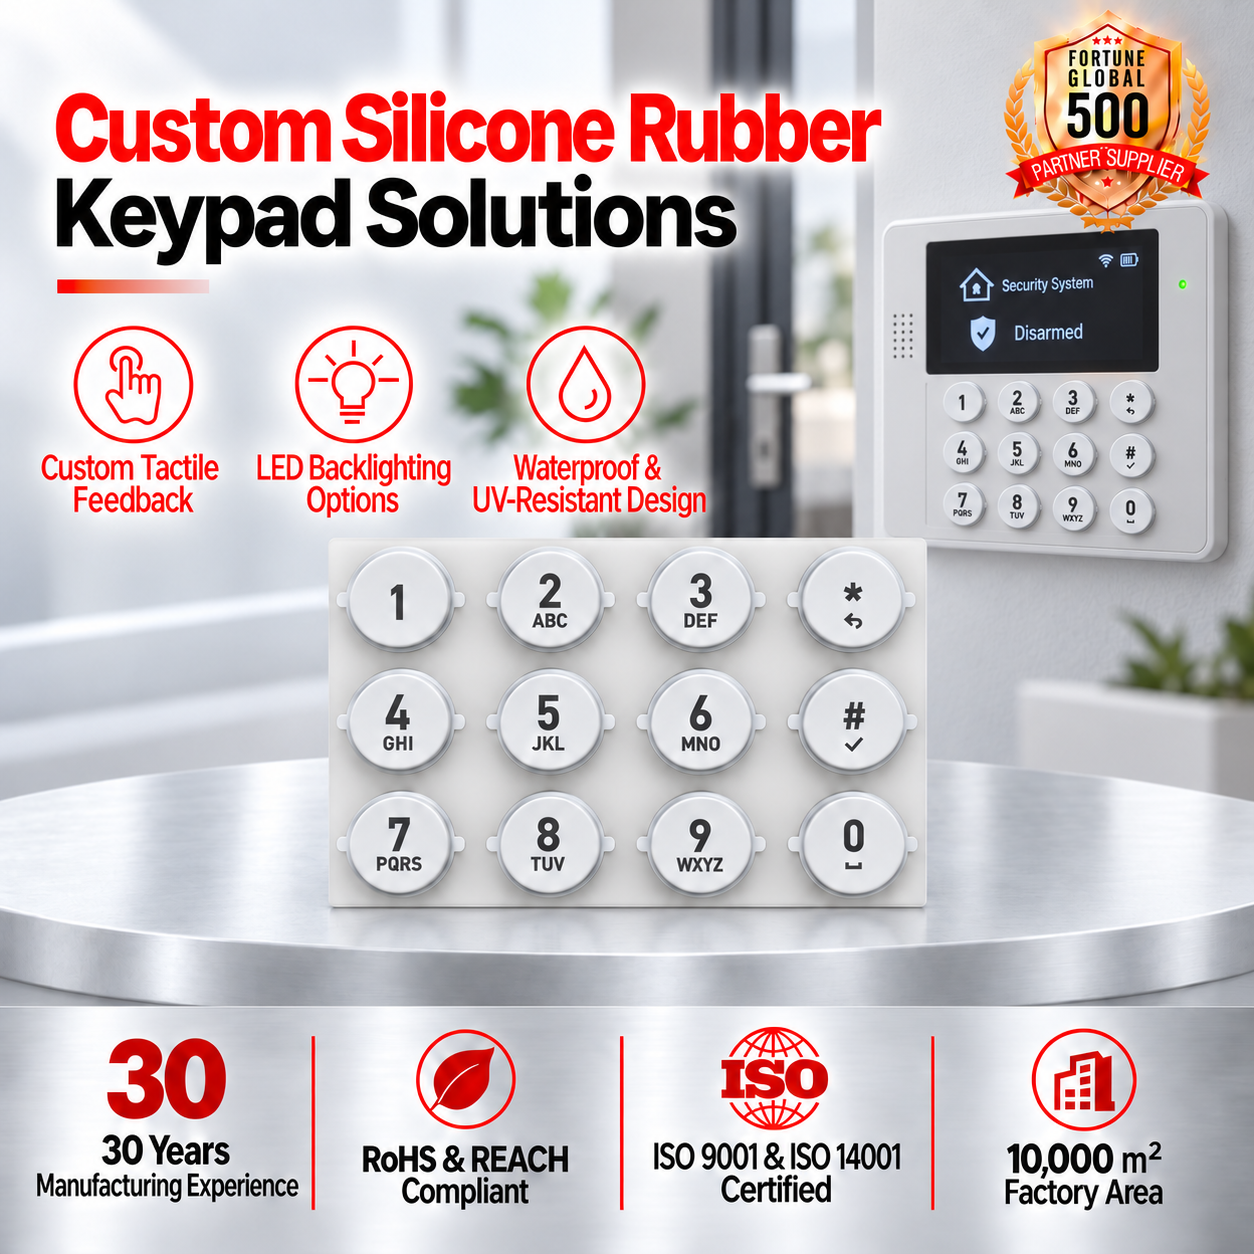
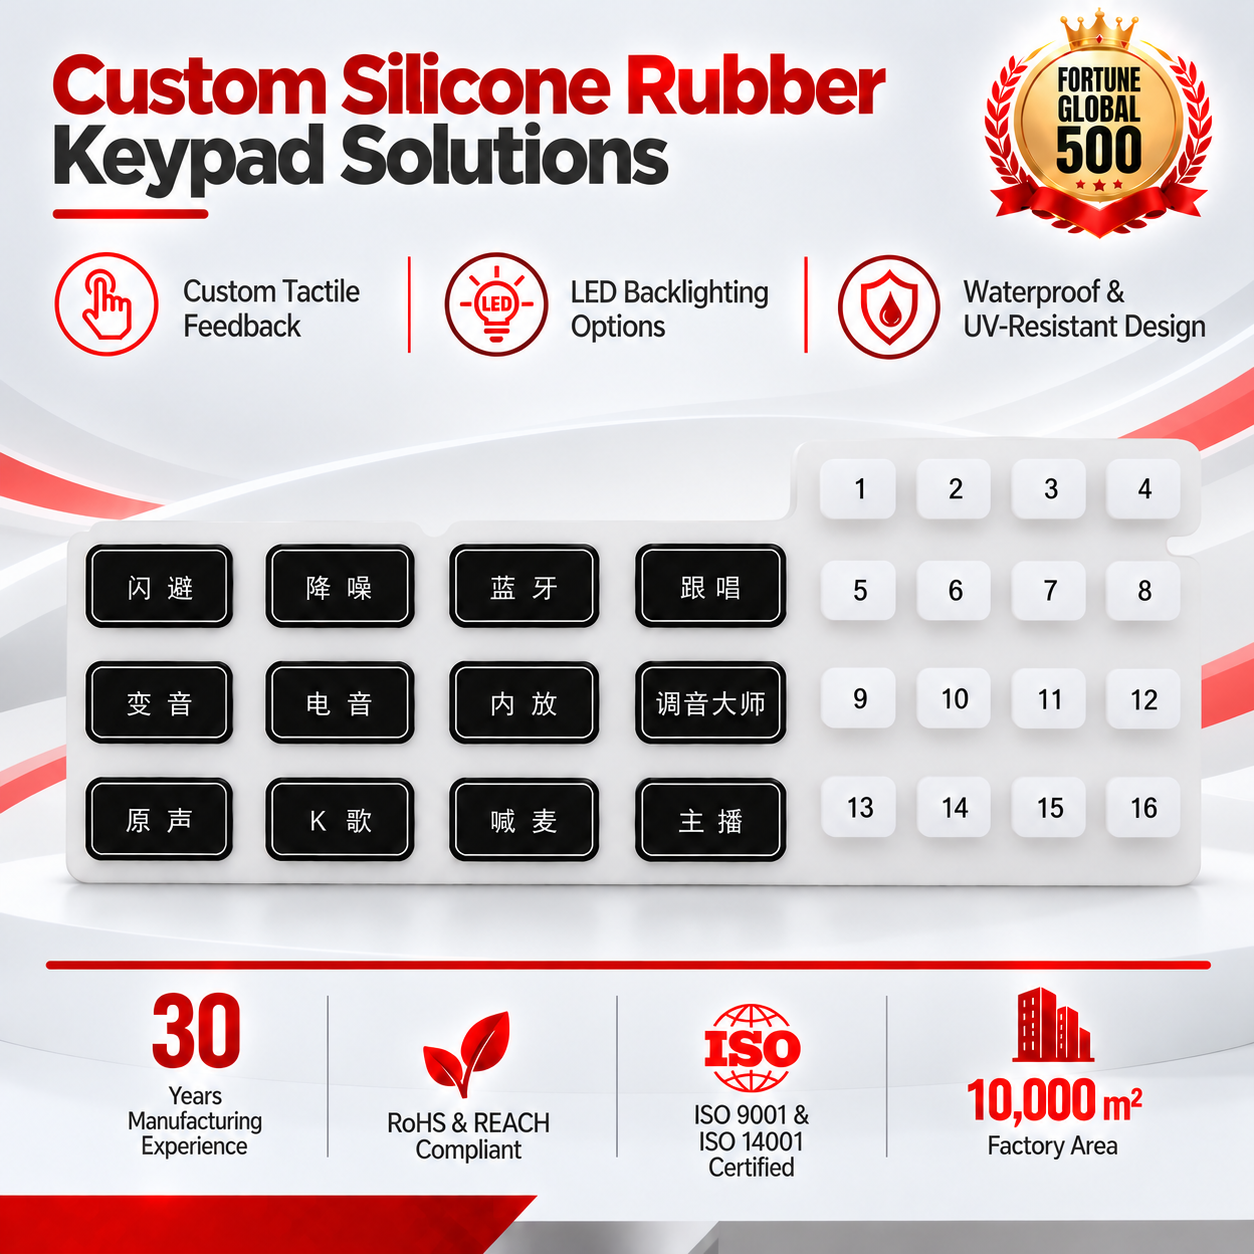
A comprehensive design blueprint detailing how modern tactile HMI systems bridge the gap between harsh North American field operating parameters and micro-tolerance electronics.
As the National Capital Region of Canada and home to one of North America's premier technology incubators—anchored by the Kanata North Technology Park—Ottawa occupies a distinctive position in high-reliability design engineering. Companies operating within Ottawa's ecosystem engineer hardware spanning telecommunications nodes, defense field communications, advanced medical diagnostics, autonomous sub-zero sensory arrays, and government-grade access control infrastructure. In these mission-critical spheres, standard consumer capacitive touch glass is fundamentally inadequate. OEM designers consistently specify precision-embossed membrane switches and sealed elastomer keypads capable of flawless tactile feedback, zero false-triggering in wet conditions, and absolute mechanical longevity.
Deploying human-machine interfaces across Eastern Ontario requires navigating severe climatic divergence—from winter lows plunging below -30°C to elevated summer humidity and high UV exposure. The structural layer stack-up must be designed proactively to resist material embrittlement, trace expansion-rate mismatch, and atmospheric moisture penetration.
Serving Ottawa's robust defense cluster, our membrane keypads are engineered to comply with rigorous MIL-STD environmental resilience. Featuring internal aluminum foil or printed carbon-grid EMI/RFI shielding, tactile snap domes engineered for gloved hand operation, and chemically inert graphic overlays, our panels ensure interference-free mission control even in tactical outposts.
Medical OEMs in the Ottawa health science sector demand HMIs that endure harsh hospital disinfectants including Isopropyl Alcohol, Bleach, and Quaternary Ammonium compounds. By deploying Autotex XE micro-textured polyester with antimicrobial silver-ion treatments and flush rim-embossed keys, we provide hermetically sealed, IP66 wash-down front panels.
From municipal transit charging pillars to outdoor hydro-metering terminals across the Ottawa Valley, HMIs must survive intense freeze-thaw cycles. We utilize specialized low-temperature viscoelastic adhesives (such as 3M 467MP/9472LE) and polyimide FPC circuits that retain mechanical flexibility down to -40°C without risk of conductive trace crazing.
The industrial control paradigm across Canada is shifting away from fragmented mechanical pushbuttons toward unified, space-saving smart surfaces. Through our extensive work with Canadian engineers, three primary technological trends have emerged as standard project requirements:
Shortlisting the optimal substrate and layer configuration early in the DFM cycle is vital for maximizing product life cycle and avoiding costly field recalls:
| Architecture Feature | Standard Silver PET Layer | Copper Polyimide (FPC) Layer | Silicone Keypad + Membrane | Dynamic FSR Pressure Layer |
|---|---|---|---|---|
| Trace Resistance | 10 – 100 Ω (Length Dependent) | < 0.5 Ω (Ultra Low Drop) | Carbon Pill (< 100 Ω) or FPC | Variable Dynamic Resistor |
| Bending & Tail Flex Life | Moderate (Avoid Sharp Creases) | Exceptional (> 50,000 tight flexes) | High (Elastomer flex fatigue free) | Flexible Thin Film Stack |
| Sub-Zero Thermal Tolerance | -20°C to +70°C | -40°C to +105°C | -40°C to +120°C | -20°C to +80°C |
| Actuation Profile | Pillow / Rim Emboss Tactile | Polydome or Metal Dome Snap | Full Travel 1.0mm - 2.5mm | Variable Pressure Sensitive |
| Ottawa OEM Target Use | Indoor Controllers & Appliances | Critical Defense, Medical & Telecom | Handheld Scanners & Field Radios | Medical Bed & Ergonomic Robotics |
Dongguan AXRU Electronics Co., Ltd. operates a specialized 10,000㎡ production facility housing 121 skilled technical specialists, providing complete end-to-end design, tooling, screen printing, lamination, and reliability validation. Rather than subcontracting critical process nodes, our integrated setup delivers complete accountability from gerber design to Ottawa customs clearance.
Audited manufacturing systems conforming to stringent ISO9001 quality management protocols with full material traceability.
Climate-controlled cleanroom screen printing guaranteeing zero dust inclusions on transparent display windows and sensor electrodes.
Every single unit undergoes computerized matrix continuity, circuit resistance, insulation resistance, and LED verification before export packing.
In-house computerized load cells measure snap ratio, peak actuation grams, and release feedback to match your mechanical specifications.
High/low temperature (-40°C to +150°C), thermal shock, UV yellowing, and constant humidity testing rigs simulating 10 years of Canadian weather.
Comprehensive engineering Design For Manufacturability (DFM) reviews completed within 24 hours; working prototypes delivered in 7-10 days.
Direct answers addressing the logistical, compliance, and design criteria relevant to Eastern Ontario procurement teams and hardware engineering groups:
We specify premium non-hygroscopic polyester films (e.g., MacDermid Autotype) and specialized 3M acrylic adhesive transfer tapes (e.g., 3M 467MP/468MP or 300LSE). Furthermore, breathing vents are routed internally between switch layers or vented through micro-porous membrane filters to allow atmospheric equalization without letting moisture or condensation degrade the contacts.
We provide full commercial export clearance packages tailored for Canada Border Services Agency (CBSA) processing under designated HS codes (such as 8537.10 / 8538.90). Every production batch ships with complete Certificates of Conformance (CoC), RoHS 3.0 declarations, REACH compliance statements, and 100% electrical inspection test reports.
DFM engineering reviews and CAD mechanical stack-up approvals are completed within 24 hours. Precision laser-cut sample prototypes are typically finalized within 7 to 10 working days. Following First Article Approval (FAI), production tooling and volume manufacturing require 15 to 20 days. Shipments via express air couriers (FedEx/DHL) reach Ottawa facilities in 3 to 4 business days.
Yes. We apply specialized hard-coat films containing built-in microban or silver-ion antimicrobial agents (such as Autotex AM). These coatings actively inhibit bacterial colonization on the touch surface and resist degradation from intense clinical wipe-downs involving harsh quaternary disinfectants, alcohols, and hydrogen peroxide vapor.
Recognizing the specialized, high-mix requirements of Ottawa's enterprise hardware innovators, our low-volume prototyping run begins at just 100 units. This allows engineering departments to conduct physical mechanical fit checks, field trials, and electromagnetic compliance testing before authorizing mass tooling.
To initiate a comprehensive DFM audit and quotation, please supply your graphic artwork in Vector PDF, Adobe Illustrator (.AI), or CorelDraw, alongside 2D/3D mechanical dimensions in DXF, DWG, or STEP format. Including electrical circuit pinout schematics, connector pitch, and designated environmental sealing ratings (e.g., IP65, IP67) expedites engineering review.
Collaborate directly with senior HMI mechanical and electrical engineers. Submit your technical drawings or reverse-engineering samples today for a complimentary DFM analysis and quotation within 24 hours.