Polycarbonate
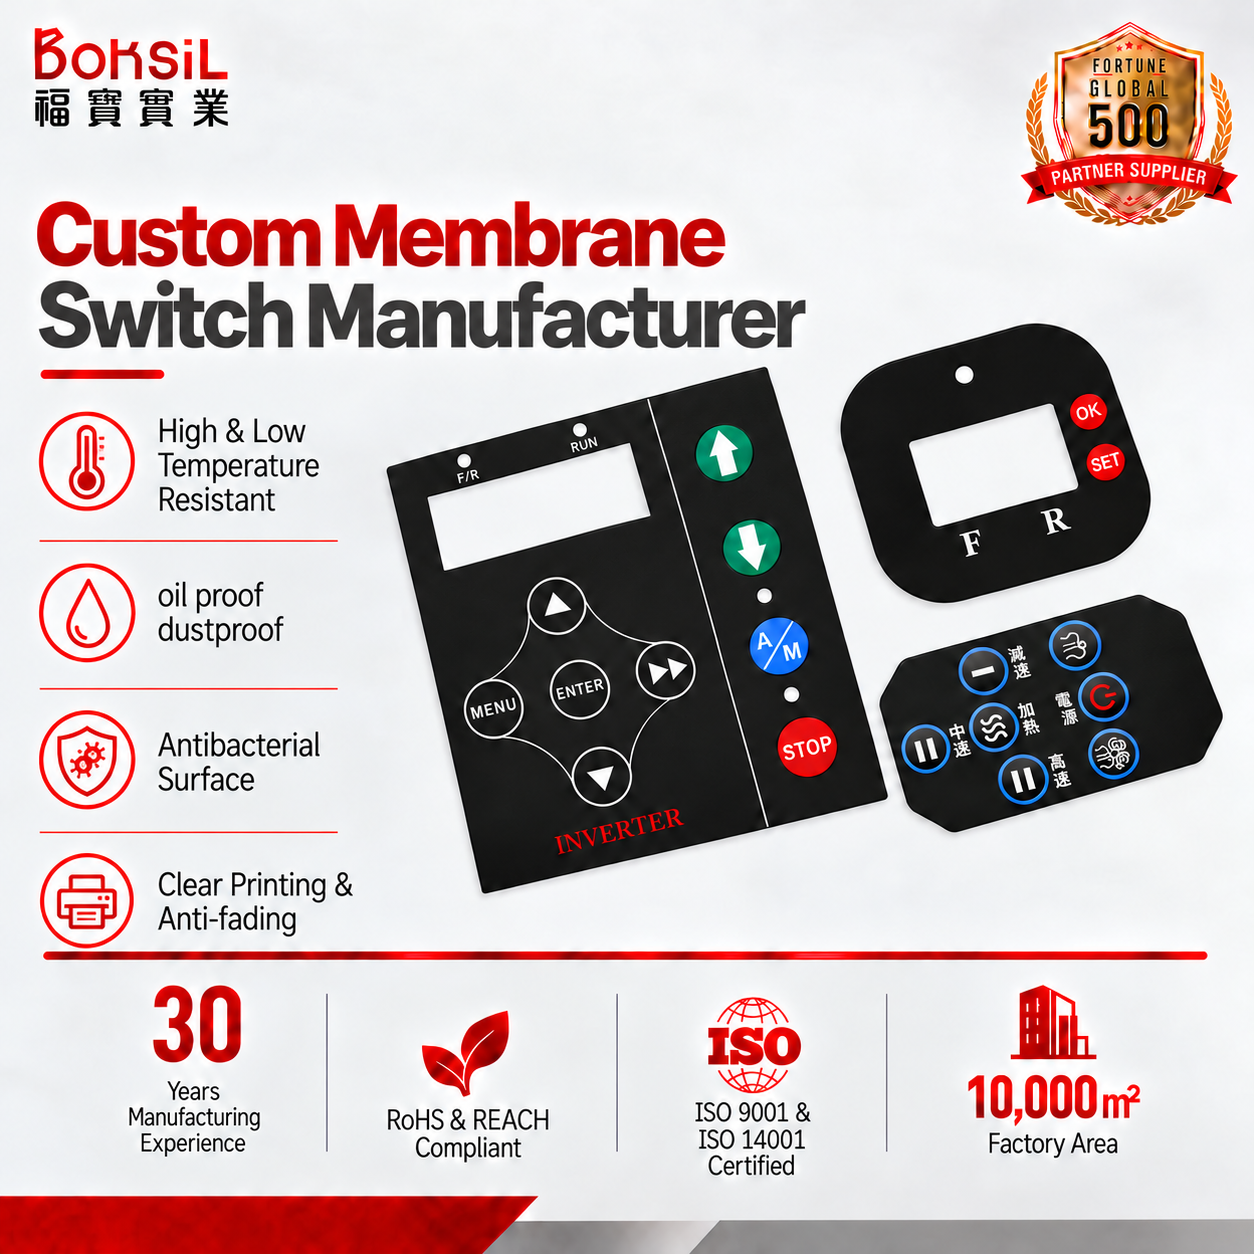
Custom-fabricated interfaces engineered for Portmore's light industrial, commercial, and automated operations. All stack-ups support tailored graphic legends, backlighting, and IP-rated environmental sealing.
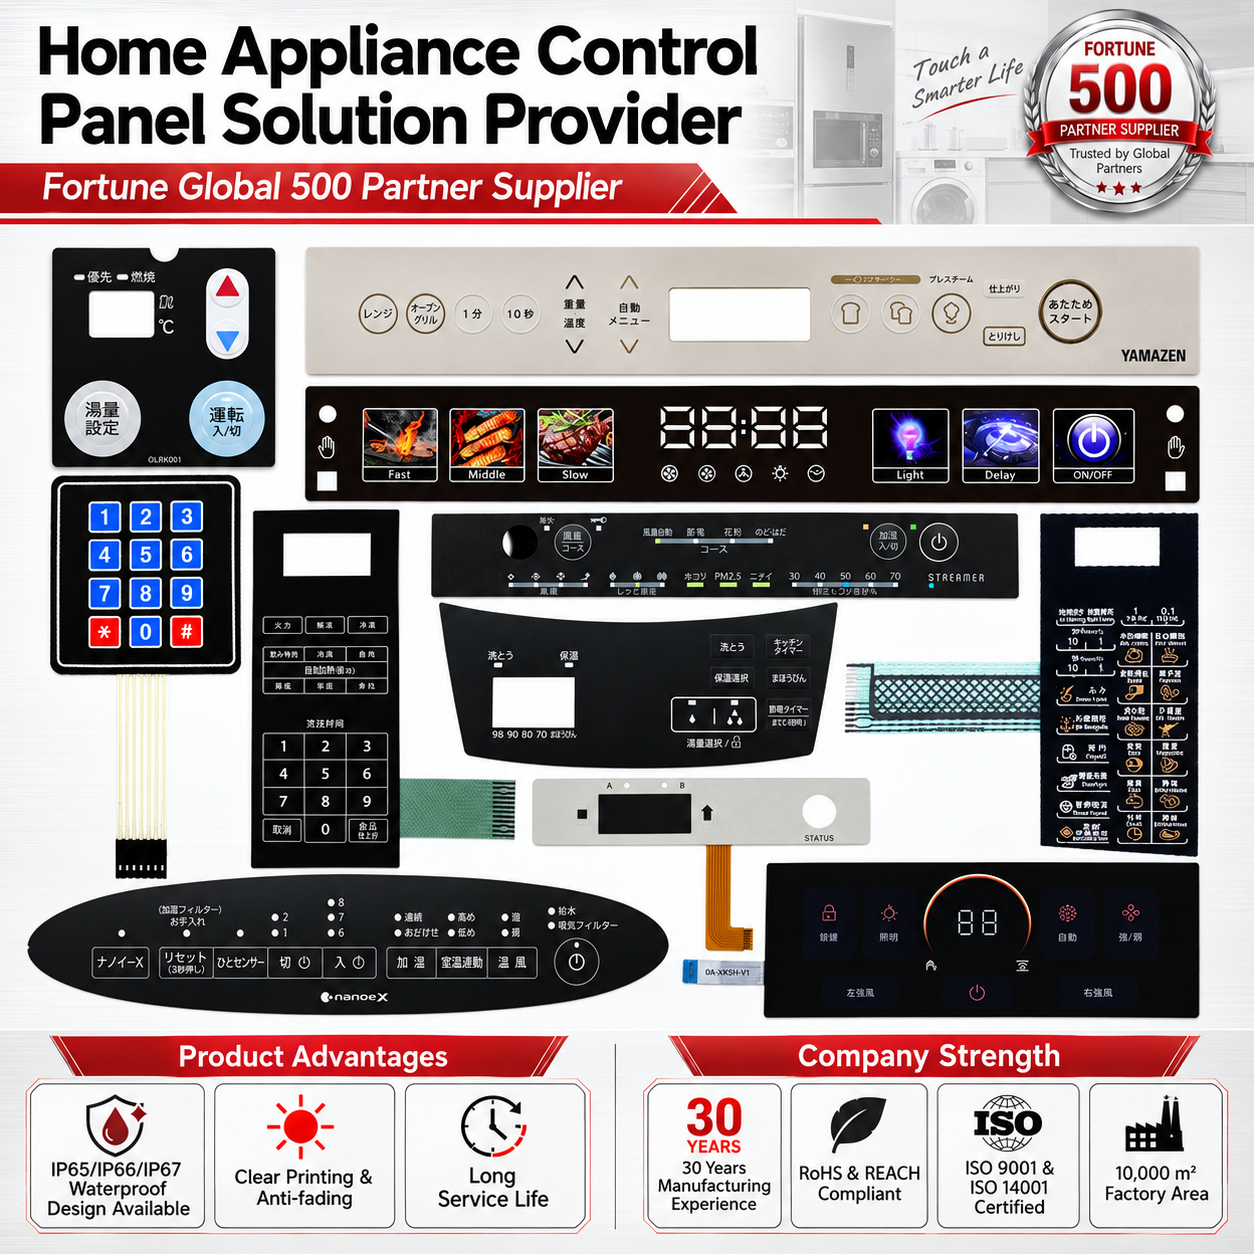
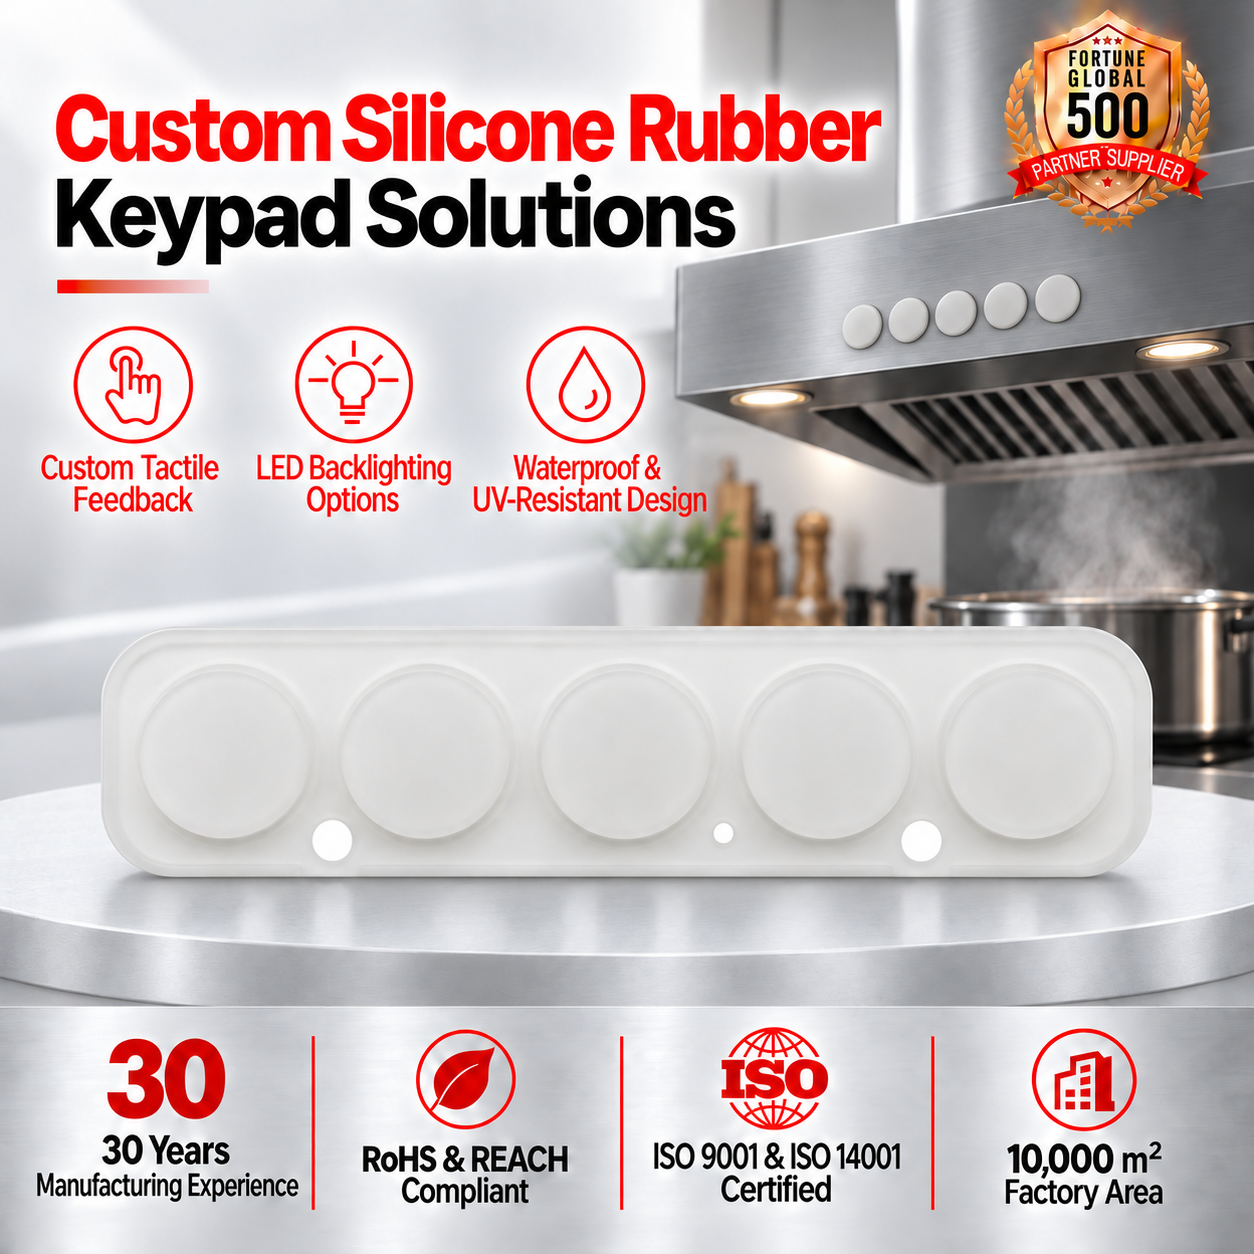
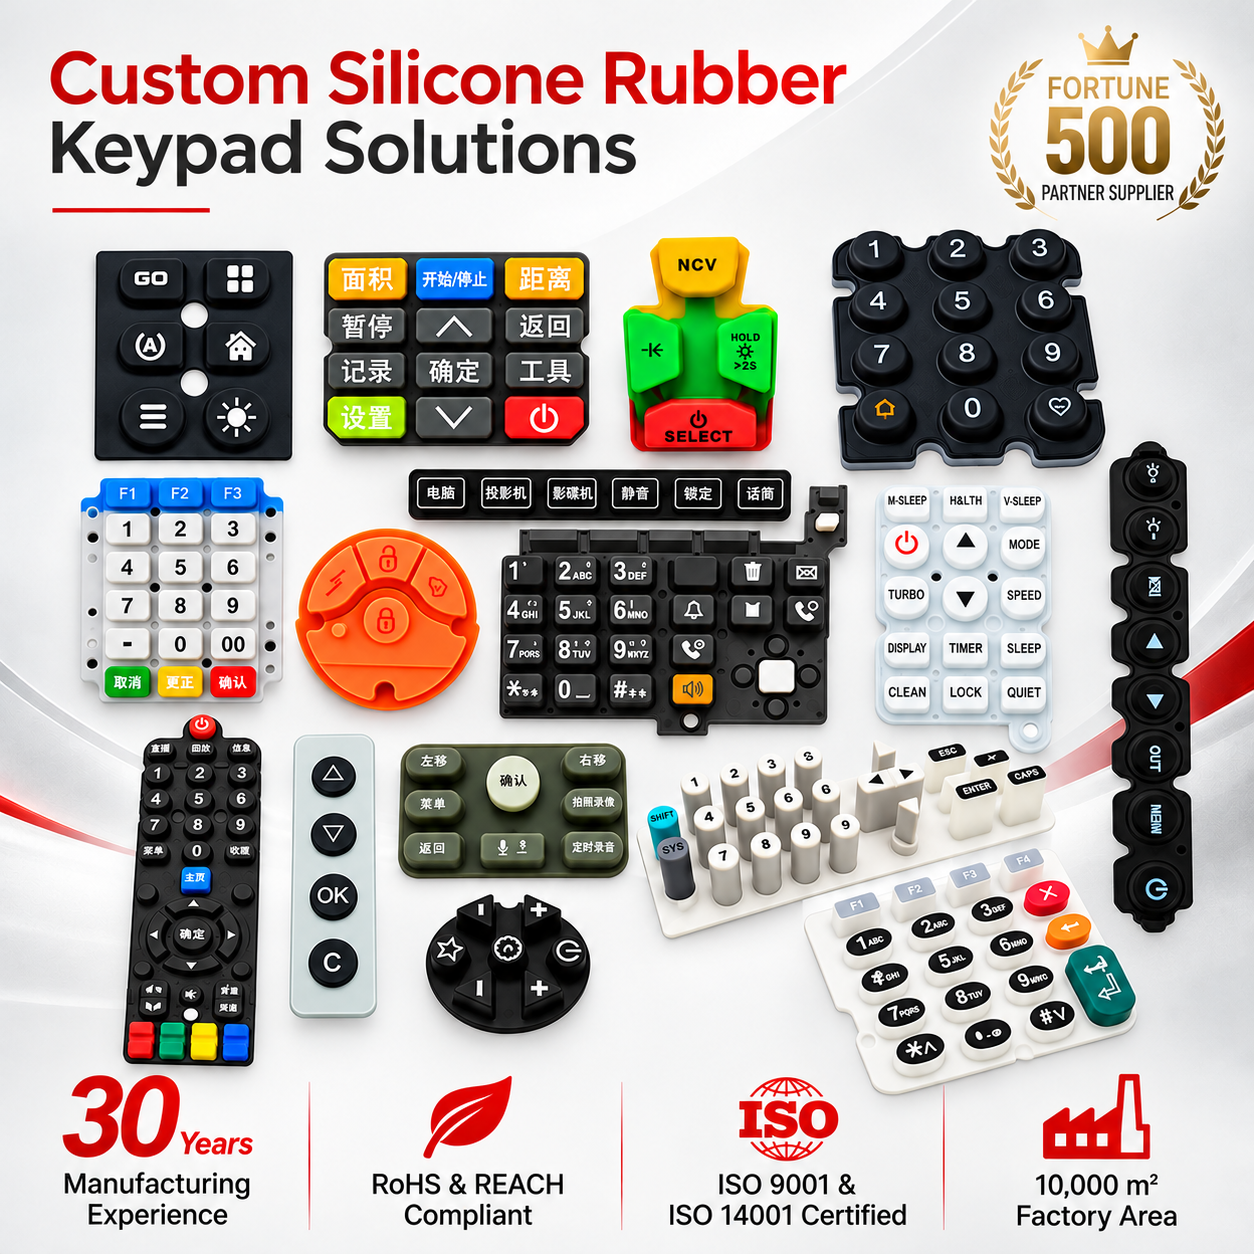
Portmore, Jamaica—recognized across the Caribbean as one of the fastest-evolving metropolitan and commercial centers—is experiencing sustained infrastructure expansion, logistical automation, and light assembly modernisation. Operating in coastal, high-temperature, and saline environments presents rigorous challenges to Human-Machine Interface (HMI) controls. Standard consumer-grade front panels suffer from silver migration, ink yellowing, and adhesive degradation when subjected to tropical solar exposure and elevated relative humidity. As an international manufacturing specialist, AXRU Electronics supplies high-reliability, custom-engineered membrane keypad overlays that bridge strict global durability specifications with the specific operational demands of the Portmore market.
Material integrity determines whether a membrane control panel retains its electrical and aesthetic characteristics across years of service or deteriorates prematurely. Engineers designing electronic assemblies for Portmore-based facilities must balance optical clarity, tactile life, and thermal resistance:
| Evaluation Parameter | Polycarbonate (Lexan) | Polyester (Autotype PET) | Hard-Coated Acrylic (PMMA) |
|---|---|---|---|
| UV & Sunlight Stability | Moderate (Prone to yellowing unless stabilized) | Exceptional (UV-resistant formulations) | Excellent Optical Clarity |
| Switch Actuation Life | ~100,000 to 300,000 cycles | > 5,000,000 cycles (Embossed) | Rigid (Non-tactile touch windows) |
| Chemical & Solvent Barrier | Vulnerable to MEK, aromatic solvents | Impervious to alcohols, acids, cleaners | Resistant to common detergents |
| Humidity Delamination Risk | Moderate moisture vapor transmission | Extremely Low moisture absorption | Rigid adhesive bonding required |
| Recommended Local Applications | Indoor POS terminals, retail scales | Industrial automation, maritime, logistics | Instrumentation cover lenses |
The geographic position of Portmore adjacent to Kingston Harbour exposes field equipment to airborne marine electrolytes, requiring hermetically sealed perimeter barriers, tailored snap-feel actuation, and resilient graphics.
Distribution yards and handling hubs near the port require crane radio controls, telemetry consoles, and vehicle tracking interfaces rated to IP65/IP67 with carbon-pill or nickel-plated tactile domes that prevent saltwater corrosion.
Financial transaction hubs, telecom self-service kiosks, and unattended utility access units demand tamper-resistant, blind-embossed keypad overlays that resist abrasive sand dust, intense sun, and round-the-clock public usage.
Municipal healthcare centers and diagnostic labs use wipe-clean, antimicrobial-treated front membranes. Chemical-resistant polyester overlays withstand hypochlorite and alcohol disinfectants without legend wash-off.
Hardware architecture in Jamaica is moving away from purely mechanical push-buttons toward multi-function hybrid control surfaces. Key engineering shifts shaping procurement in Portmore include:
1. Capacitive Sensing Integration: Combining graphic overlays directly with thin-film copper FPC or conductive printed silver capacitive switches. This eliminates mechanical contact bounce, providing a continuous flat wipe-down surface ideal for sanitized medical facilities and food preparation plants.
2. Light Guide Film (LGF) Backlighting: Traditional discrete LEDs often produce uneven light hotspots. By deploying ultra-thin LGF layers, control panels achieve uniform, low-power illumination across legends, numeric keypads, and logo areas—critical for low-visibility industrial plant enclosures.
3. ESD and EMI Shielding Layers: High relative humidity alternating with dry industrial currents can generate electrostatic discharge. Integrating solid or grid-patterned printed silver or aluminum ground planes ensures electrostatic dissipation up to 15kV, protecting sensitive microcontrollers on underlying PCBs.
Full-chain production in our 10,000㎡ plant ensures rapid engineering turns, validated stack-ups, and international testing compliance for Caribbean and worldwide OEMs.
10,000㎡ plant fully certified by Intertek, ensuring stringent ISO9001-aligned quality management.
Zero-defect shipment policy: every circuit is tested for continuity, contact resistance, and short-circuits.
Equipped with force-displacement testers, thermal cycling chambers, and UV weathering rigs.
Direct communication with experienced HMI stack-up engineers to optimize drawings and cut tooling costs.
Established express and sea routes directly servicing Jamaican procurement channels with rapid turnarounds.
Practical answers covering international logistics, material selection, circuit design, and prototype turnarounds.
Send your CAD drawing or functional parameters to our factory engineering desk. Receive an in-depth Design for Manufacturability (DFM) review and competitive factory pricing within 24 hours.