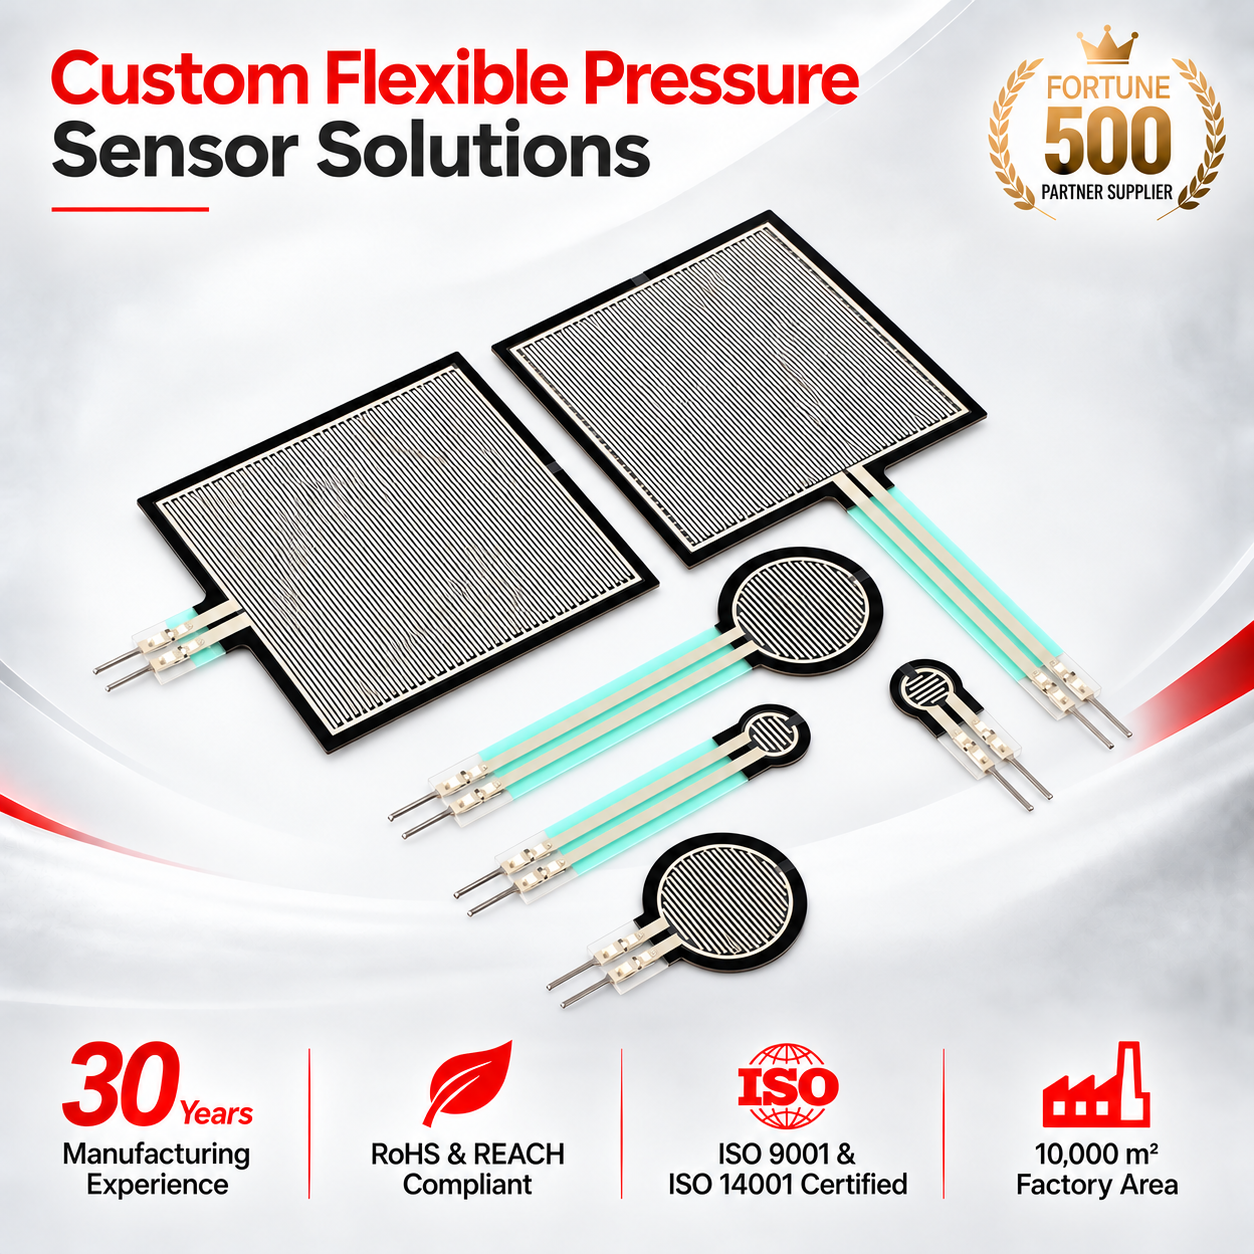
High Sensitive Capacitive Multi Touch Sensor Membrane Ultra-Soft Thin Film Pressure Sensor Fsr Type Pressure
- Technology: Capacitive / FSR Matrix
- Sensing Range: 0.1N – 20N Linear
- Durability: > 5,000,000 Actuations
Direct factory supply of capacitive touch systems, high-durability elastomeric keypads, and thin-film force resistors compliant with ISO 13485 production standards.
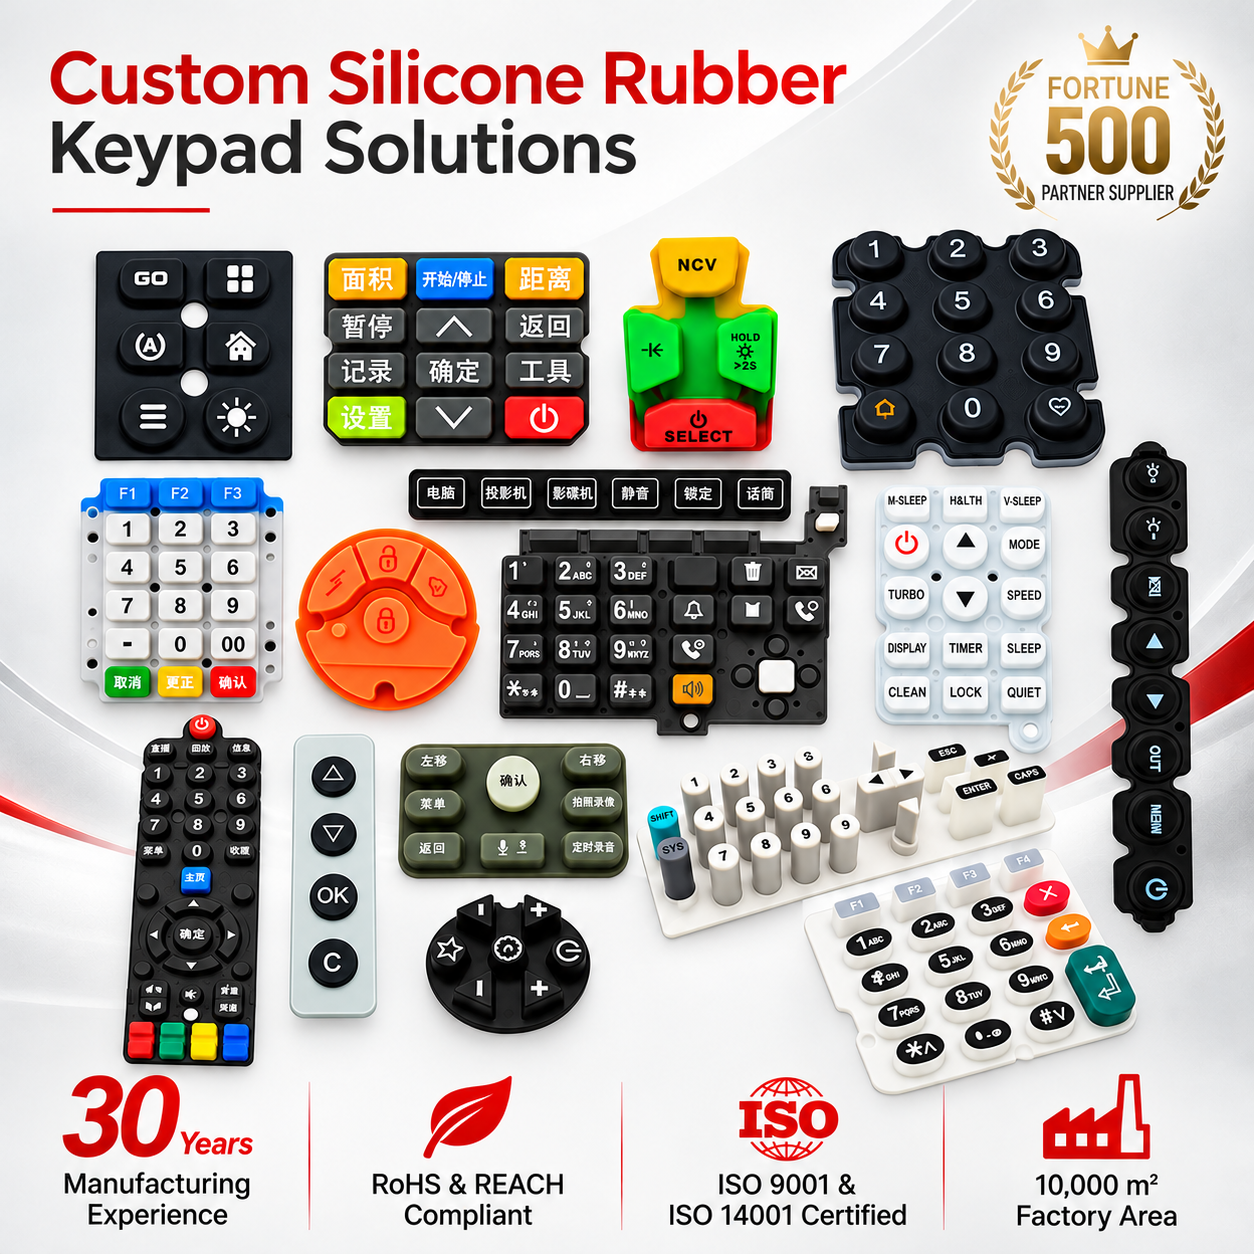
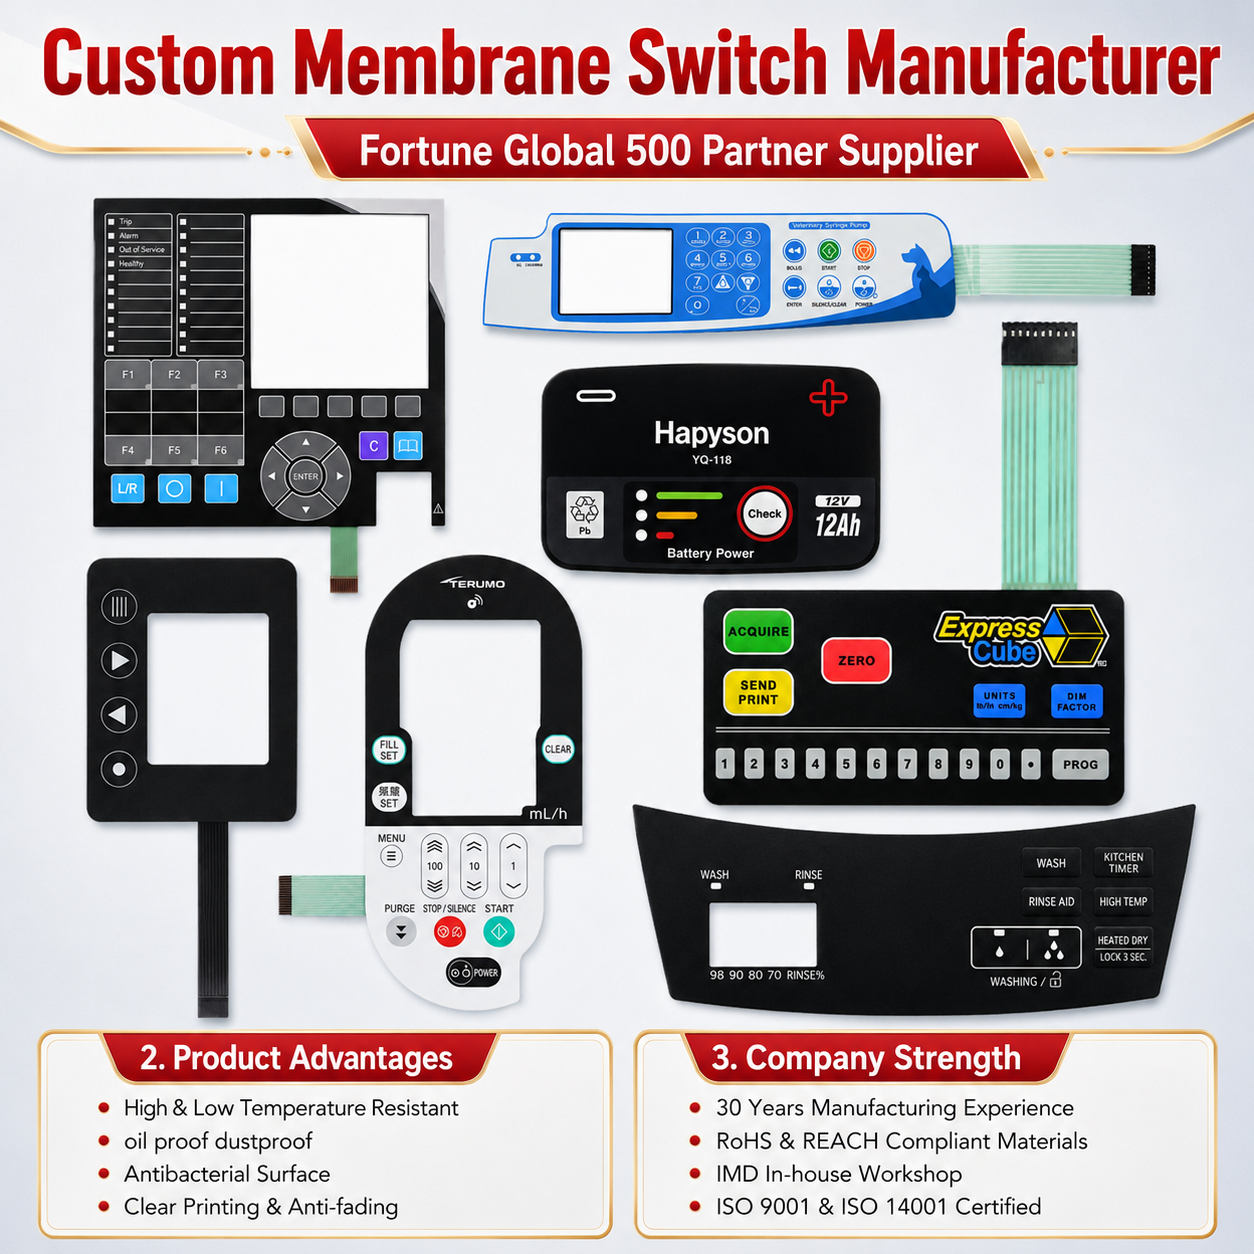
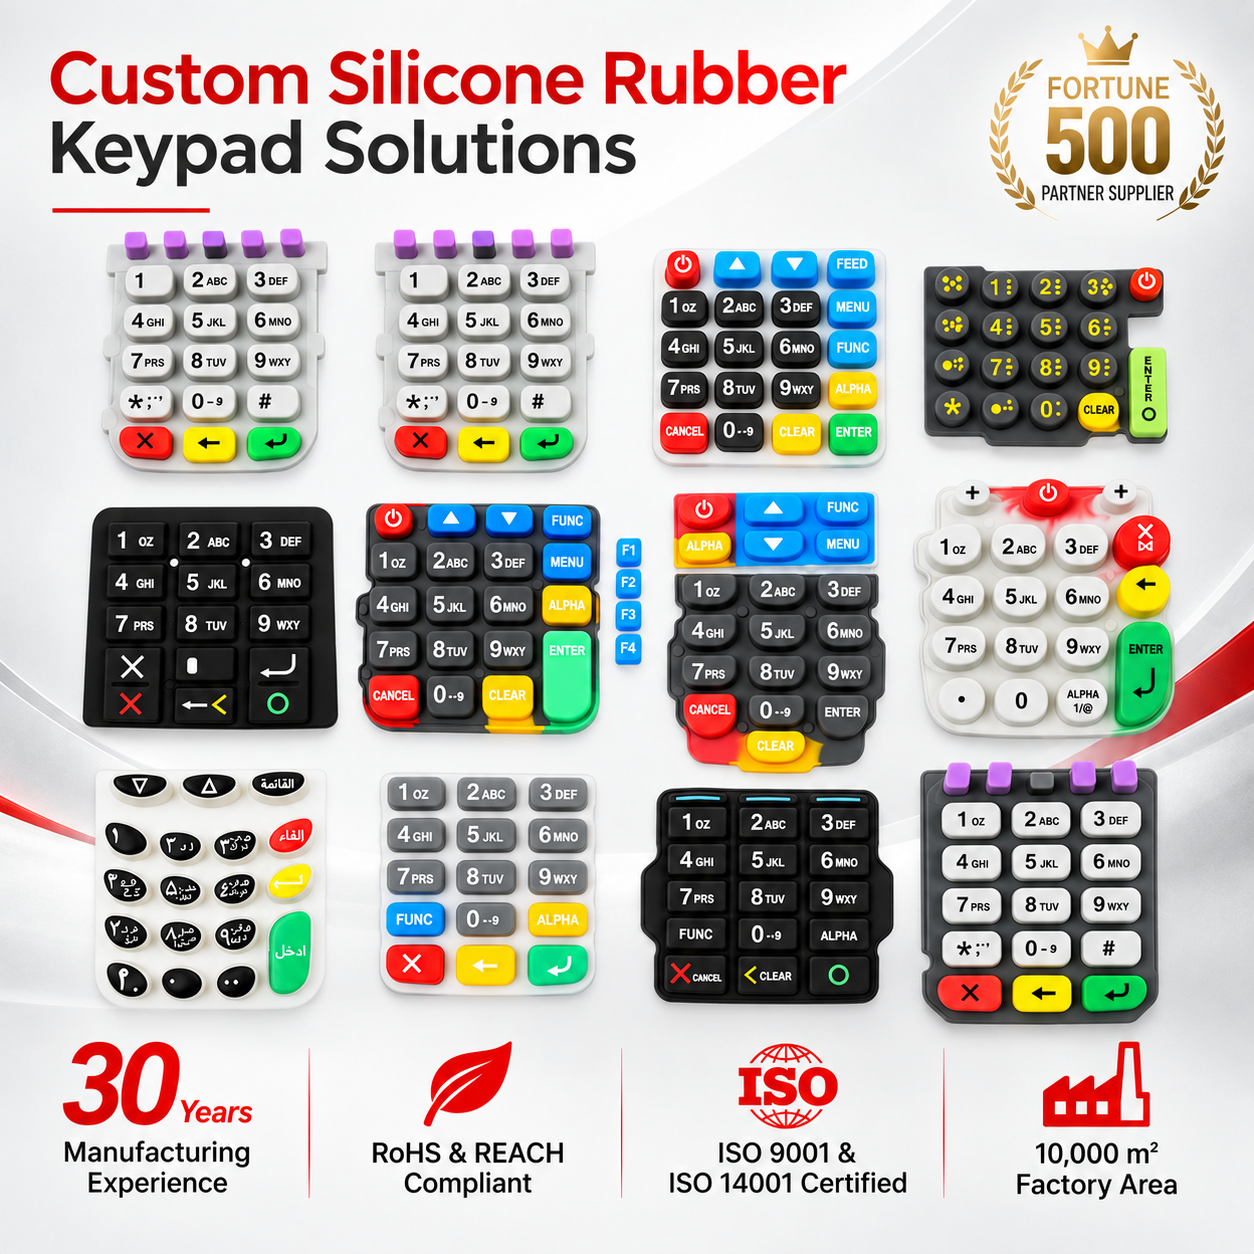
The Liverpool City Region, bolstered by Knowledge Quarter Liverpool (KQ Liverpool), Liverpool Science Park, and neighboring Cheshire manufacturing corridors, represents an expanding hub for medical robotics, diagnostics, and clinical equipment development.
Instrumentation deployed within the Royal Liverpool University Hospital and clinical labs demand impermeable front-panel sealing. Our membrane switches utilize continuous polyester layers treated with antibacterial micro-textures, resisting repeated sterilization with hospital disinfectants like sodium hypochlorite, isopropyl alcohol (IPA), and quaternary ammonium compounds without graphic degradation or micro-fissuring.
Chemical Immersion ProofOperating suites and bedside monitors engineered in North West tech parks integrate our custom FPC circuits and tactile nickel-plated domes. With precise snap ratios exceeding 55%, clinicians receive unmistakable tactile feedback even when manipulating controls through double nitrile or surgical latex gloves, preventing critical dosing entry errors under intense emergency settings.
High-Tactile Snap RatioNext-generation robotic surgical stations require zero false activations and absolute electromagnetic immunity. We implement comprehensive ITO (Indium Tin Oxide) or selective carbon/aluminum ESD shielding planes capable of withstanding >15kV air discharge, guaranteeing stable signal integrity during high-frequency electrosurgical cutting and ablation procedures.
EMC / ESD Certified DesignA technical assessment for procurement managers and biomedical hardware designers transitioning from legacy electromechanical switches to integrated smart surfaces.
Following post-Brexit updates to the UK Medical Device Regulations (UK MDR 2002) and convergence with BS EN 60601-1 standards, medical instrumentation faceplates must meet rigorous mechanical hygiene standards. Mechanical push buttons with physical crevices are increasingly deprecated due to bio-burden accumulation and cleaning failure risks. The Liverpool health innovation corridor is transitioning rapidly to IP67- and IP68-rated planar membrane keypads featuring continuous perimeter perimeter gaskets (using structural acrylics like 3M 200MP or 300LSE adhesive matrices). This architecture isolates internal electronics completely from aerosolized pathogens, bodily fluids, and washdown processes.
Smart beds, pressure mapping mats, and infusion pump calibration units manufactured across Merseyside are abandoning rigid load cells in favor of ultra-thin flexible piezoresistive printed sensors. By depositing high-conductivity carbon nanoparticle pastes onto flexible PET films, our Dongguan cleanrooms produce ultra-sensitive FSR arrays capable of detecting pressures from 10g to 10kg with sub-millisecond dynamic responses. These matrices integrate seamlessly behind decorative silicone elastomer skins or direct underneath patient-support textiles.
Surgical suites in institutions like Alder Hey Children's Hospital often operate in dim ambient lighting during laparoscopic and endoscopic interventions. Traditional bulky LEDs create uneven light pools and localized thermal spikes. Modern medical switches export-tailored for Liverpool specify micro-etched Light Guide Films (LGF) less than 0.25mm thick, distributing uniform cold backlighting through side-firing SMD diodes. Coupled with 'dead-front' graphic printing, function icons remain invisible until activated, dramatically lowering operator cognitive load and preventing accidental touch activation in low-light environments.
Combining 12 years of specialized HMI fabrication, an Intertek-audited 10,000㎡ industrial facility, and rigorous end-to-end quality assurance.
Our manufacturing complex in Dongguan, China operates Class 1,000 and 10,000 cleanrooms for graphic printing, laser etching, and precision component placement. Complete in-house fabrication—from circuit screen printing to computerized flatbed die cutting—ensures uncompromising traceability and cost structures without intermediary margins.
Intertek Factory VerifiedEvery medical-grade membrane lot undergoes stringent validation: automated force-displacement plotting for tactile uniformity, programmable -40°C to +85°C thermal/humidity stress testing, ink rub resistance under surgical solvents, and multi-million-cycle switch actuation verification on customized servo-mechanical endurance testers.
100% In-Line TestingWe streamline procurement for UK engineers and supply chain officers. Our English-speaking engineering team delivers Design for Manufacturability (DFM) reviews within 24 hours, optimizing layer stack-ups, connector tail geometry, and circuit routing. We manage end-to-end logistics with reliable DDP air and sea freight into Liverpool and Manchester ports.
Low MOQ 100 pcs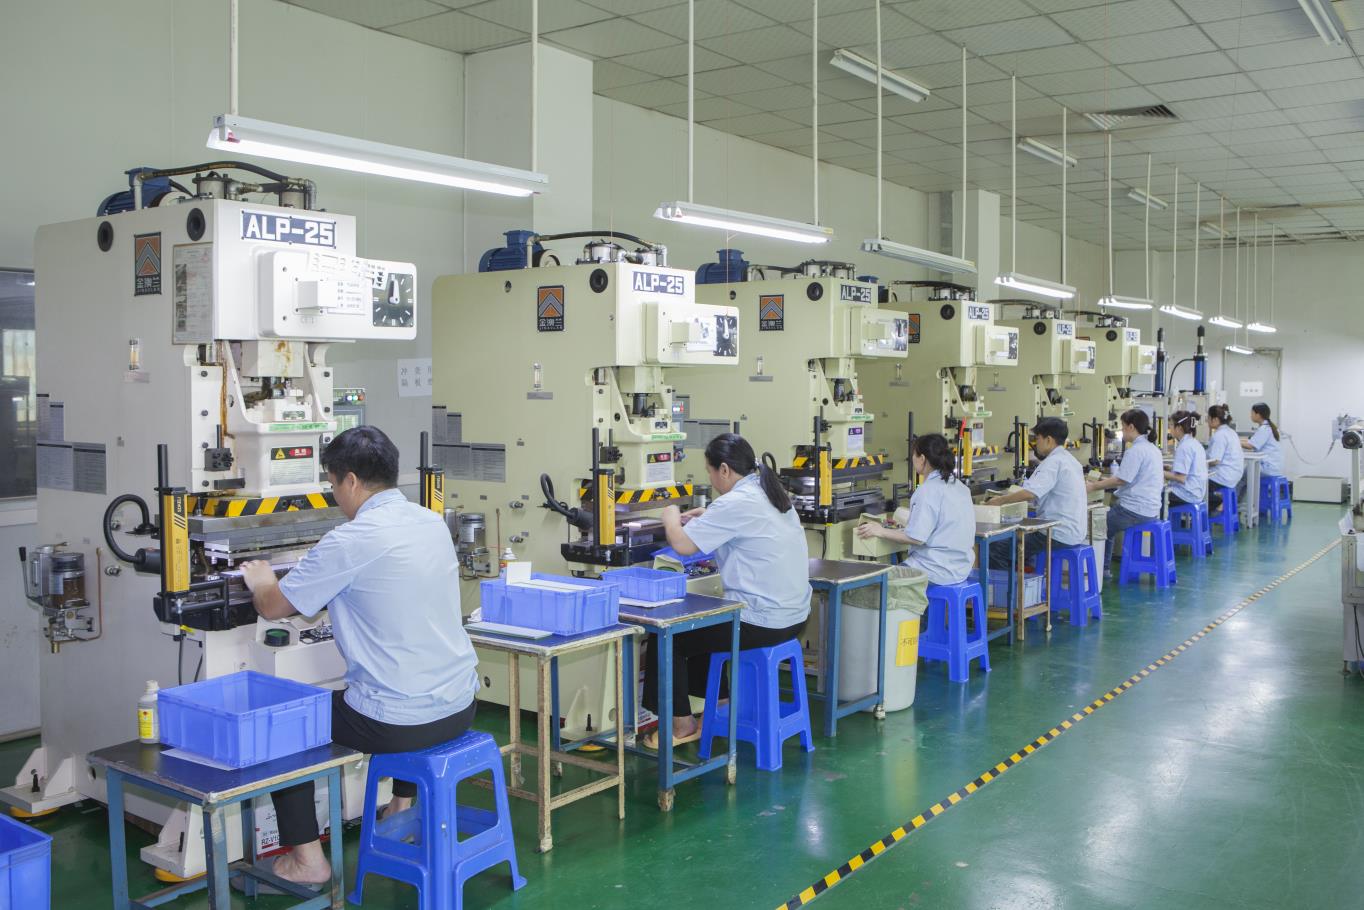
10,000㎡ scalable manufacturing footprint in Dongguan with dedicated cleanroom printing and lamination suites.
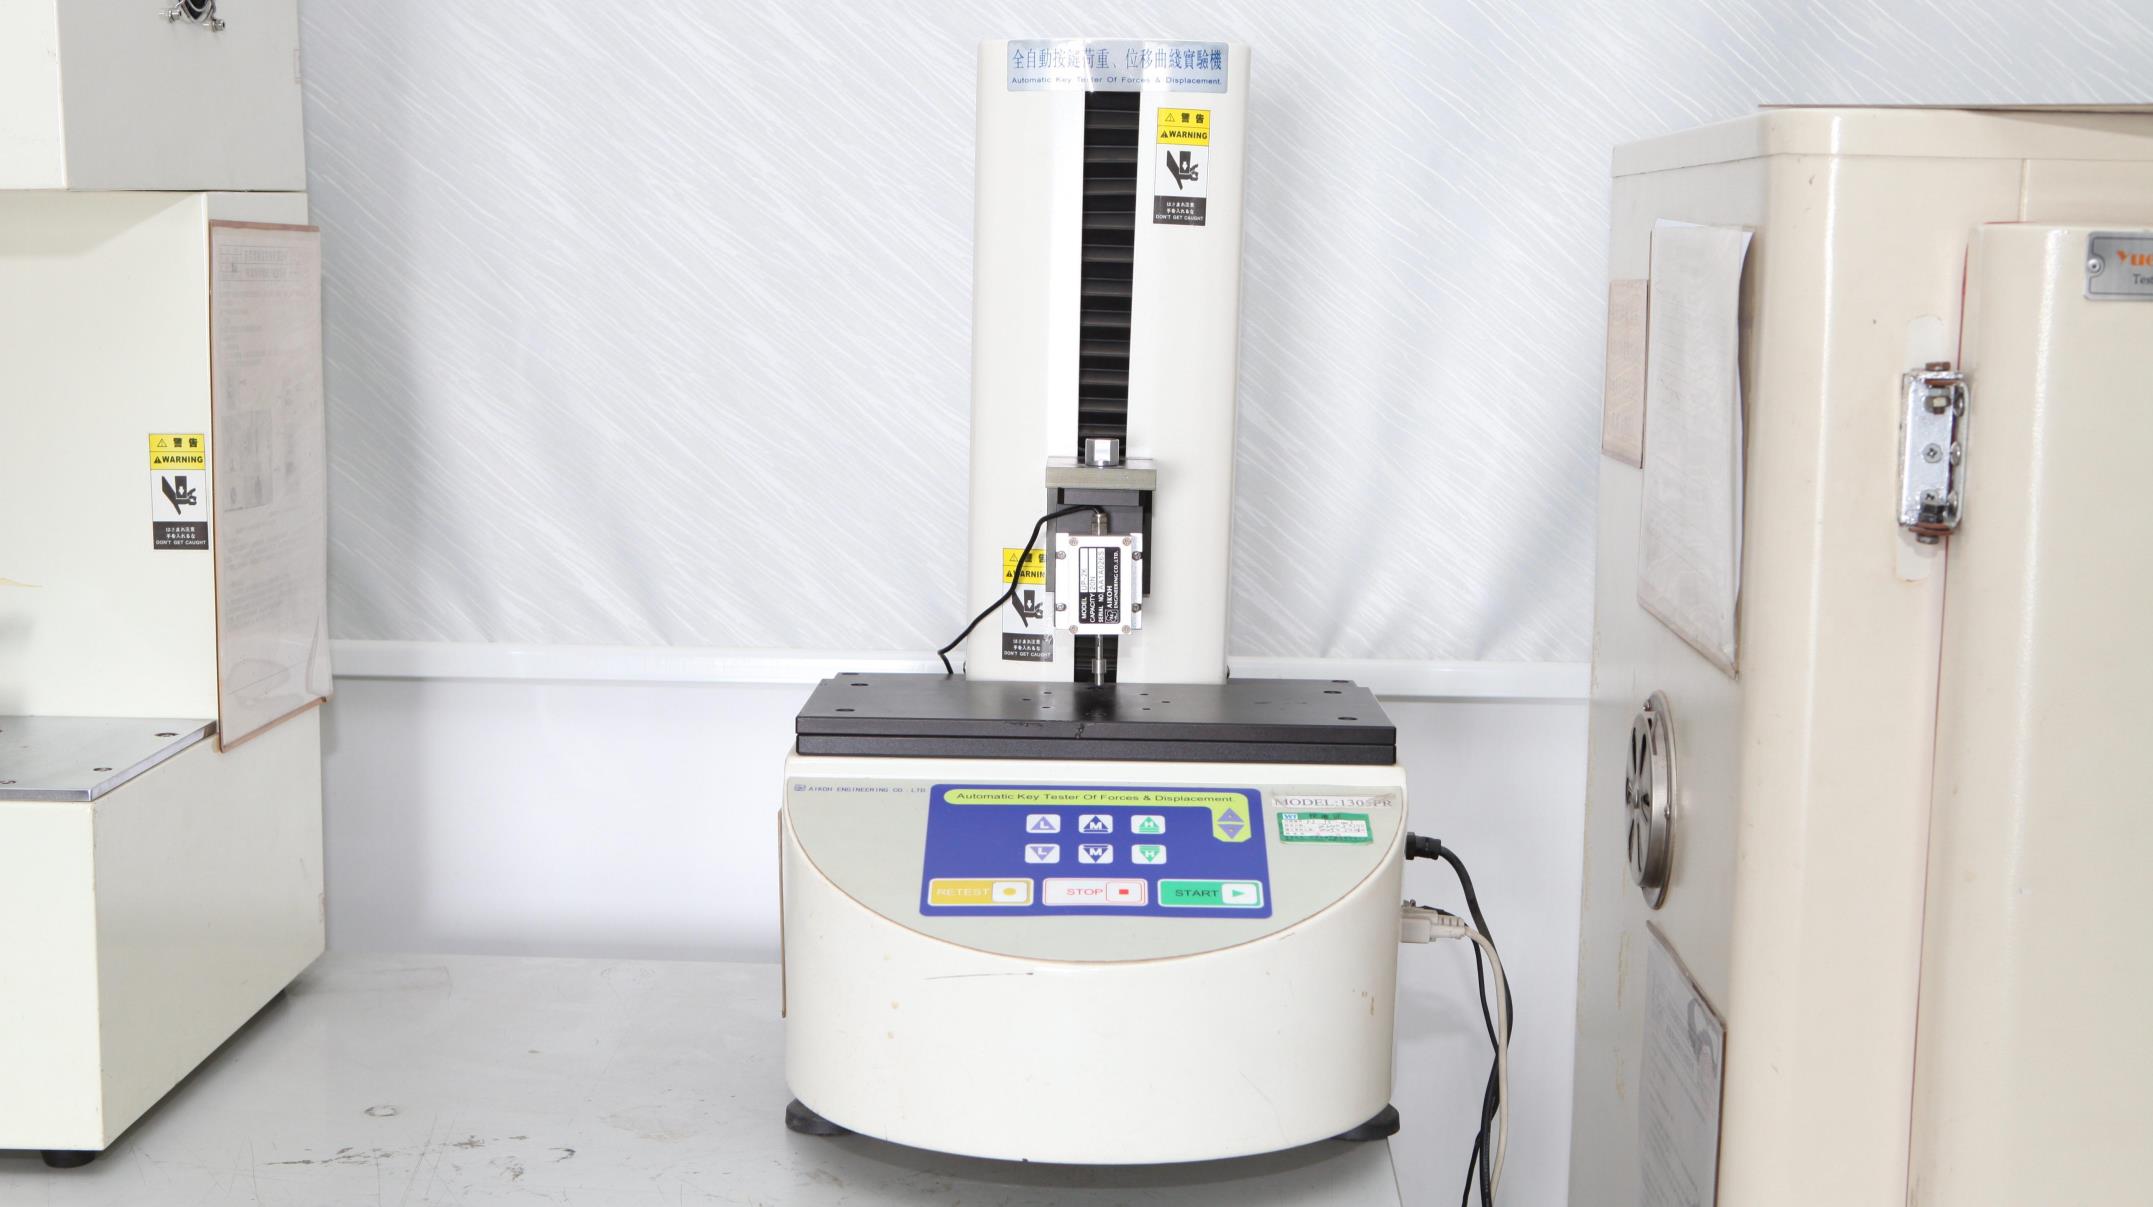
Computerized load plotting guarantees each dome switch meets target actuation force (200g-450g) and tactile snap feel.
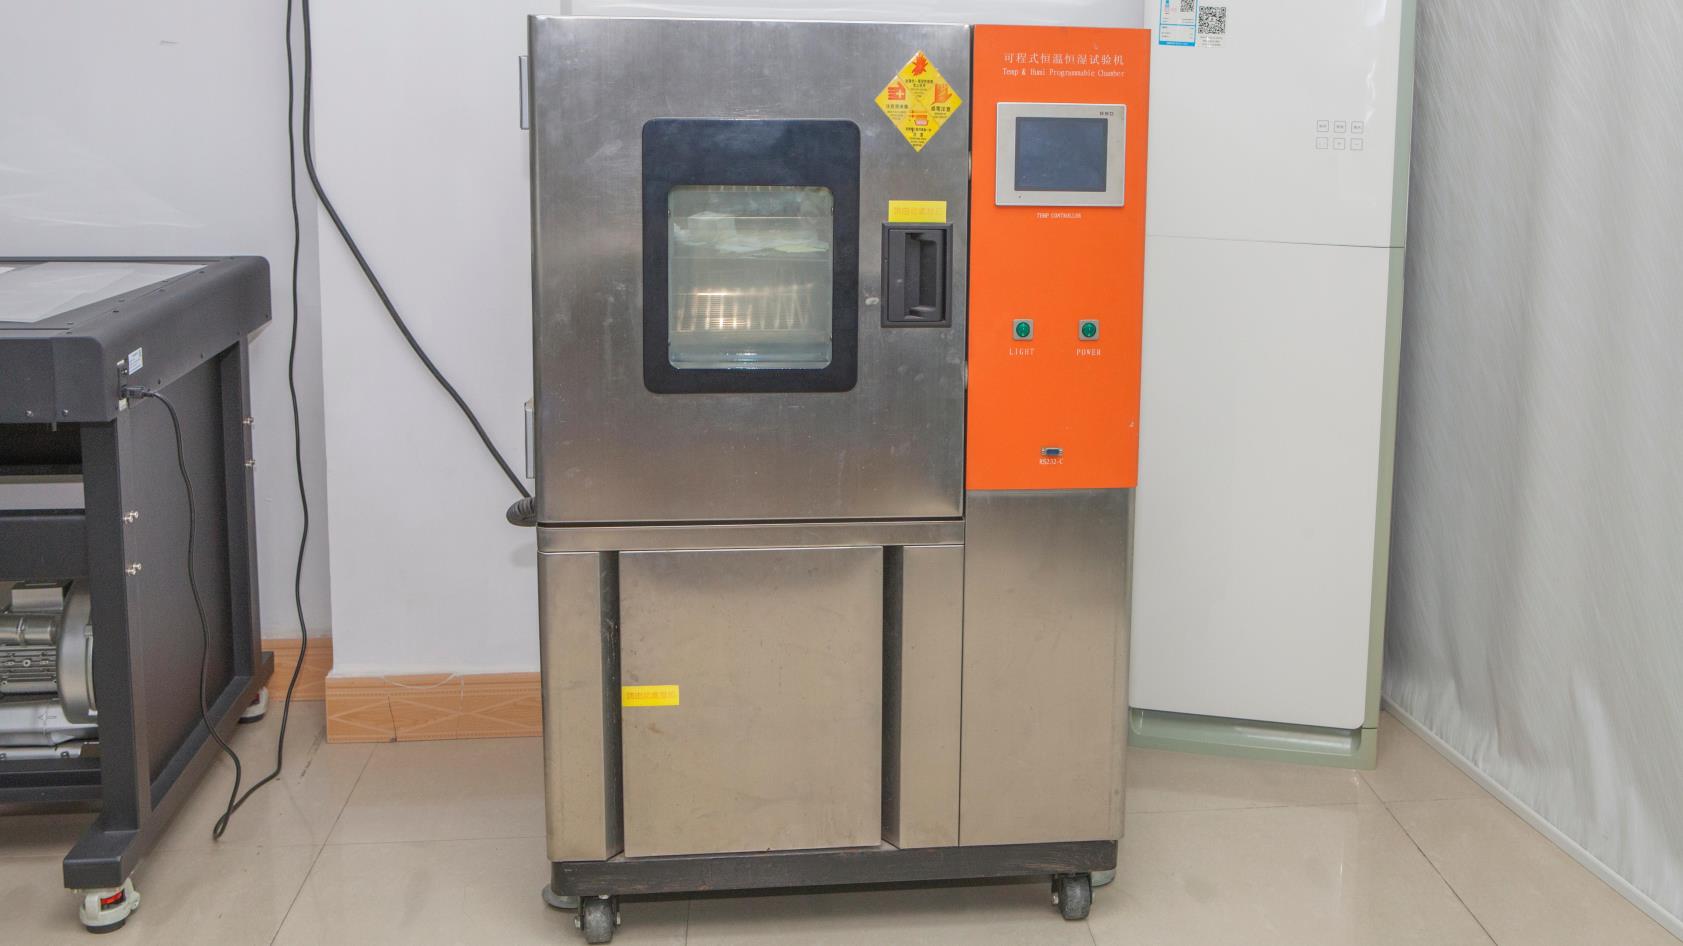
Accelerated life testing chambers verify adhesive seal integrity and conductor resistance under extreme humidity and thermal cycling.
Addressing compliance, technical qualification, shipping channels, and batch economics for Liverpool engineering buyers.