Standard & Custom Illuminated HMI Solutions
Explore our eight primary membrane switch and tactile panel architectures engineered to withstand demanding operating cycles, chemical washdowns, and harsh industrial environments.
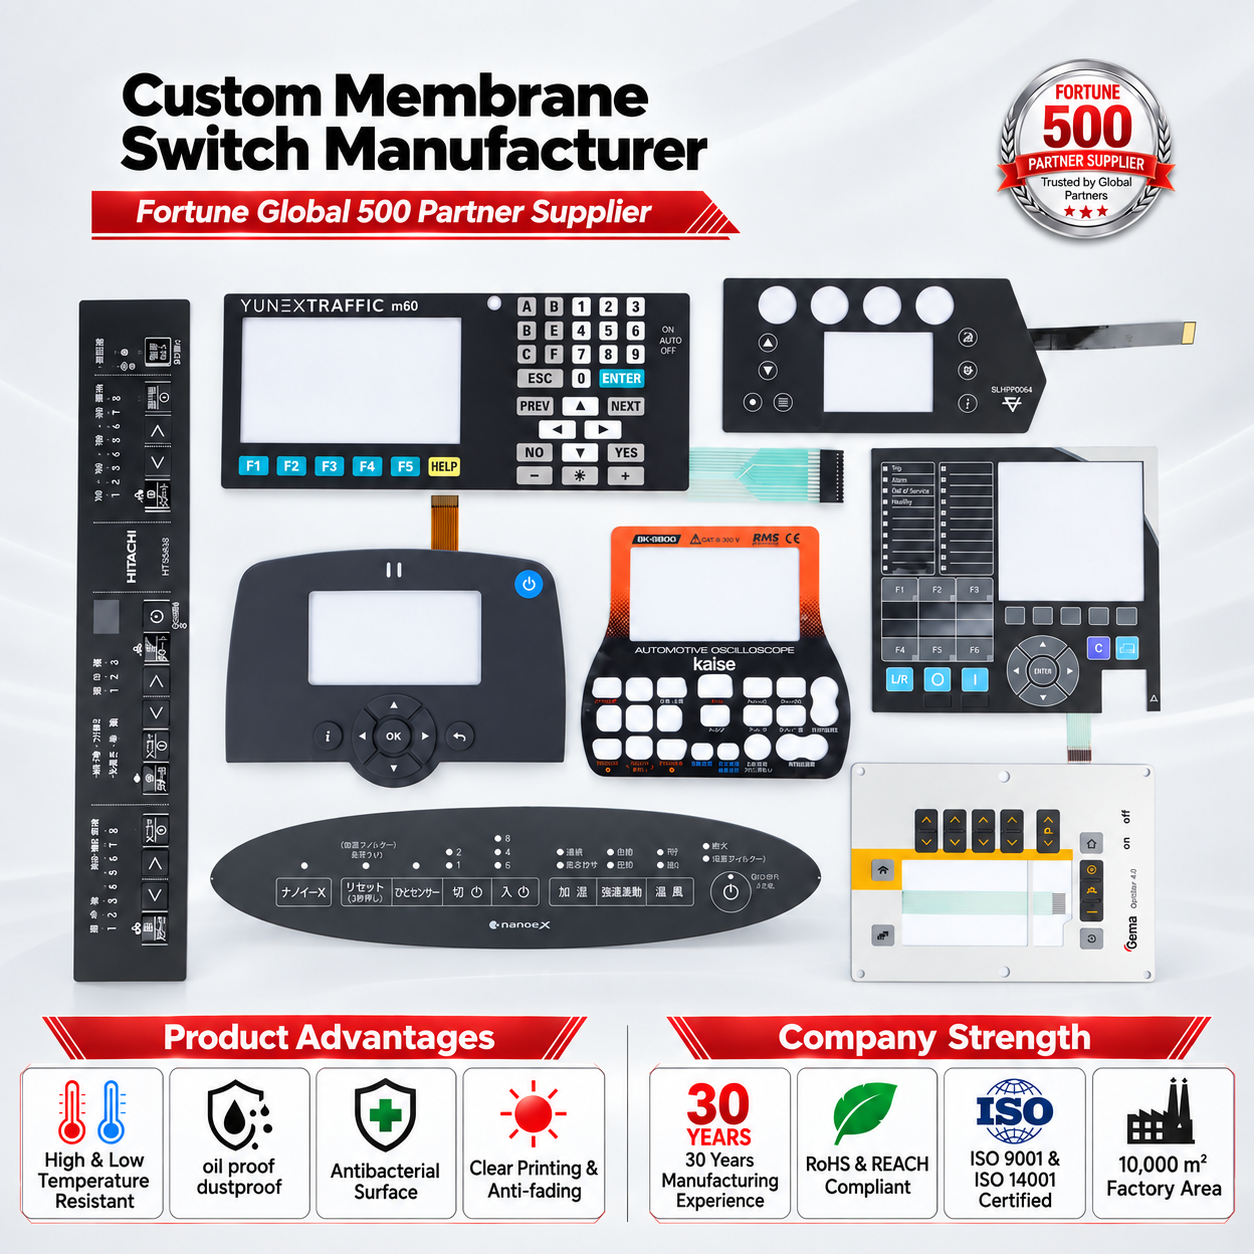
Backlighting Architectures for Human-Machine Interfaces
Modern electronic engineering requires precise optical uniformity without compromising tactile snap ratios, ingress ratings, or low power consumption targets.
Semantic Search Core Insight: Why Uniform Backlighting Matters in Northern UK Industrial Deployments
In low-light operating facilities across Greater Manchester, shift workers and laboratory clinicians depend on high-contrast visual cues to mitigate operational downtime and user fatigue. Integrating backlit membrane panels removes dependence on auxiliary cabinet luminaires while maintaining sealed, cleanroom-ready front geometries capable of resisting hospital sanitization agents and industrial cutting oils.
Light Guide Film (LGF) Integration
LGF technology utilizes micro-etched dot-matrix patterns across ultra-thin polycarbonate or TPU films (0.125mm to 0.25mm). By side-coupling miniature surface-mount LEDs located outside key actuation perimeters, light distributes across the overlay with over 85% luminance balance. This eliminates hotspotting while preserving tactile dome feel with actuation forces from 220g to 450g.
Surface Mount Discrete LED Placement
Direct integration of low-profile 0603 or 0805 SMD LEDs directly onto the flexible printed circuit (FPC) or silver-printed PET layers. Utilizing embossed light cavities and opaque baffle mask layers, discrete LEDs deliver targeted status annunciation, ring illumination, or multi-state feedback (e.g., green-ready, amber-warning, red-alarm) without light bleed across adjacent keys.
Electroluminescent (EL) Lamps & Fiber Optics
EL phosphor panels provide ultra-thin, continuous cold-light backlighting suitable for uniform legends and icons where low power consumption is balanced against 3,000 to 5,000-hour duty lifespans. Alternatively, woven optical fiber mats driven by remote high-flux LEDs eliminate thermal dissipation and electromagnetic emissions at the panel face, ideal for ATEX Zone 1 hazardous environments.
Comparative Illumination Matrix for Manchester Engineering Teams
| Backlighting Technology | Typical Profile Thickness | Luminance Uniformity | Actuation Interference | Operating Voltage | Lifespan (L70) |
|---|---|---|---|---|---|
| Light Guide Film (LGF) + Side LED | 0.2mm – 0.35mm | 80% – 90% (High) | Negligible (<0.05mm stroke dampening) | 2.8V – 3.4V DC | >50,000 Hours |
| Embedded SMD Point LEDs | 0.8mm – 1.6mm (Embossed) | Targeted spot only | Zero (Mounted off-center) | 2.0V – 3.3V DC | >50,000 Hours |
| Electroluminescent (EL) Foil | 0.15mm – 0.25mm | 90% – 95% (Perfect) | None (Flat layer) | 80V – 120V AC (Inverter required) | 3,000 – 6,000 Hours |
| Woven Optical Fiber Mat | 0.3mm – 0.5mm | 75% – 85% (Moderate) | Minimal | Driven by remote LED source | >60,000 Hours (LED dependent) |
Localized Applications in Greater Manchester & North West England
From the industrial corridors of Trafford Park to the health-tech innovation belts along Oxford Road, our backlit switches serve mission-critical installations across the region.
Trafford Park Logistics & Automation
Heavy materials handling equipment, automated sortation centers, and automated guided vehicles (AGVs) operating 24/7 across Europe's largest industrial estate demand vibration-tolerant, IP65-sealed keypads with high-visibility backlighting for low-light warehouses.
Oxford Road HealthTech Cluster
Manchester’s clinical trials facilities, NHS diagnostic environments, and biomedical instrumentation companies need antimicrobial, chemical-resistant polyester overlays (Autotex AM) with completely flush surfaces and backlit indicators that sterilize with harsh disinfectant agents without delamination.
North West Aerospace & Rail
Supplying Tier-1 aerospace systems across Lancashire, Rochdale, and Salford, our panels feature dead-front display windows, EMI/RFI aluminum shielding grids, and anti-glare finishes conforming to aviation cabin and rolling-stock interior human interface standards.
Food & Chemical Processing
Food processing plants around Rochdale and Cheshire chemical laboratories require IP67/IP69K perimeter-bonded silicone-membrane hybrids that resist pressurized steam jet washdowns, extreme temperature fluctuations, and volatile hydrocarbon solvents.
Emerging Design Trends for UK Equipment Manufacturers
British mechanical and electrical engineers are adopting next-generation human-machine interfaces that blend tactile feedback, compact spatial integration, and regulatory compliance.
Dead-Front Dynamic Symbology
By layering precision screen-printed translucent masking with selectively masked light blockers, inactive operational icons remain invisible against an opaque black or grey front bezel. When a system triggers a specific condition (e.g., thermal override or calibration mode), high-efficiency LEDs selectively illuminate only the relevant legend, guiding operators safely through automated workflows.
Post-Brexit UKCA & CE Dual Harmonization
Export-oriented Manchester OEMs producing machinery for both the UK domestic market and the European Union need complete supply-chain traceability. AXRU guarantees compliance with RoHS directive 2011/65/EU, REACH SVHC standards, and UKCA electrical safety guidelines, backed by laboratory testing certificates provided with every batch delivery.
Capacitive Sensing & Tactile Hybrids
Industrial machinery builders increasingly demand multi-input control layouts combining smooth, wipe-down capacitive touch areas for numerical inputs with crisp, stainless-steel snap domes for critical emergency functions (Stop, Start, Jog). This dual architecture delivers modern smartphone ergonomics alongside tactile mechanical confirmation.
Why UK OEMs Partner Direct with Dongguan AXRU Electronics
Eliminate distributor markups and engineering miscommunication. Work directly with an Intertek on-site verified manufacturing plant featuring end-to-end tooling, printing, lamination, and reliability testing under one roof.
Intertek On-Site Verified Plant
Our 10,000㎡ manufacturing campus in Dongguan, China operates under rigorous quality management guidelines. Verified on-site by Intertek, our 121 technicians oversee high-precision semi-automatic and automated screen-printing lines, climate-controlled cleanrooms, and computerized laser die-cutting systems.
Comprehensive In-House Reliability Lab
Every batch undergoes empirical stress validation: force-displacement profile recording for actuation consistency, automated key life testers guaranteeing up to 5,000,000 cycles, programmable temperature-humidity chambers (-40°C to +85°C), yellowing resistance UV fixtures, and rub-abrasion testers.
Rapid DFM & Prototype Engineering
UK buyers receive dedicated English-speaking engineering support. We turn around Design for Manufacturability (DFM) reviews within 24 hours—optimizing circuit traces, spacer venting channels, tail bend radius, and connector pinouts before production tooling cut.
Frequently Asked Questions by Manchester Buyers
Clear, direct answers regarding minimum orders, international airfreight logistics to the North West, tooling lead times, and British testing compliance.
What is the typical shipping lead time and air freight transit to Manchester?
What minimum order quantities (MOQ) apply for custom backlit membrane switches?
How do you guarantee IP65 or IP67 ingress protection against northern UK weather and washdowns?
Can AXRU supply UKCA and RoHS compliant materials for the UK market?
What file formats are required to initiate an engineering DFM quote?
How do you achieve tactile uniformity across large keypads with backlighting?
Ready to Engineer a Superior Backlit Interface for Your Next Build?
Consult directly with our senior HMI project engineers. We will analyze your layer stack-up, light transmission targets, IP sealing perimeter, and connector routing, delivering a fully documented DFM analysis and direct factory quotation within 24 hours.