Precision-Engineered Keypads & HMI Touch Modules
Tested for extreme environmental stability, optical clarity, and actuation durability. Discover our turnkey configurations delivered directly to system integrators across Cartago.
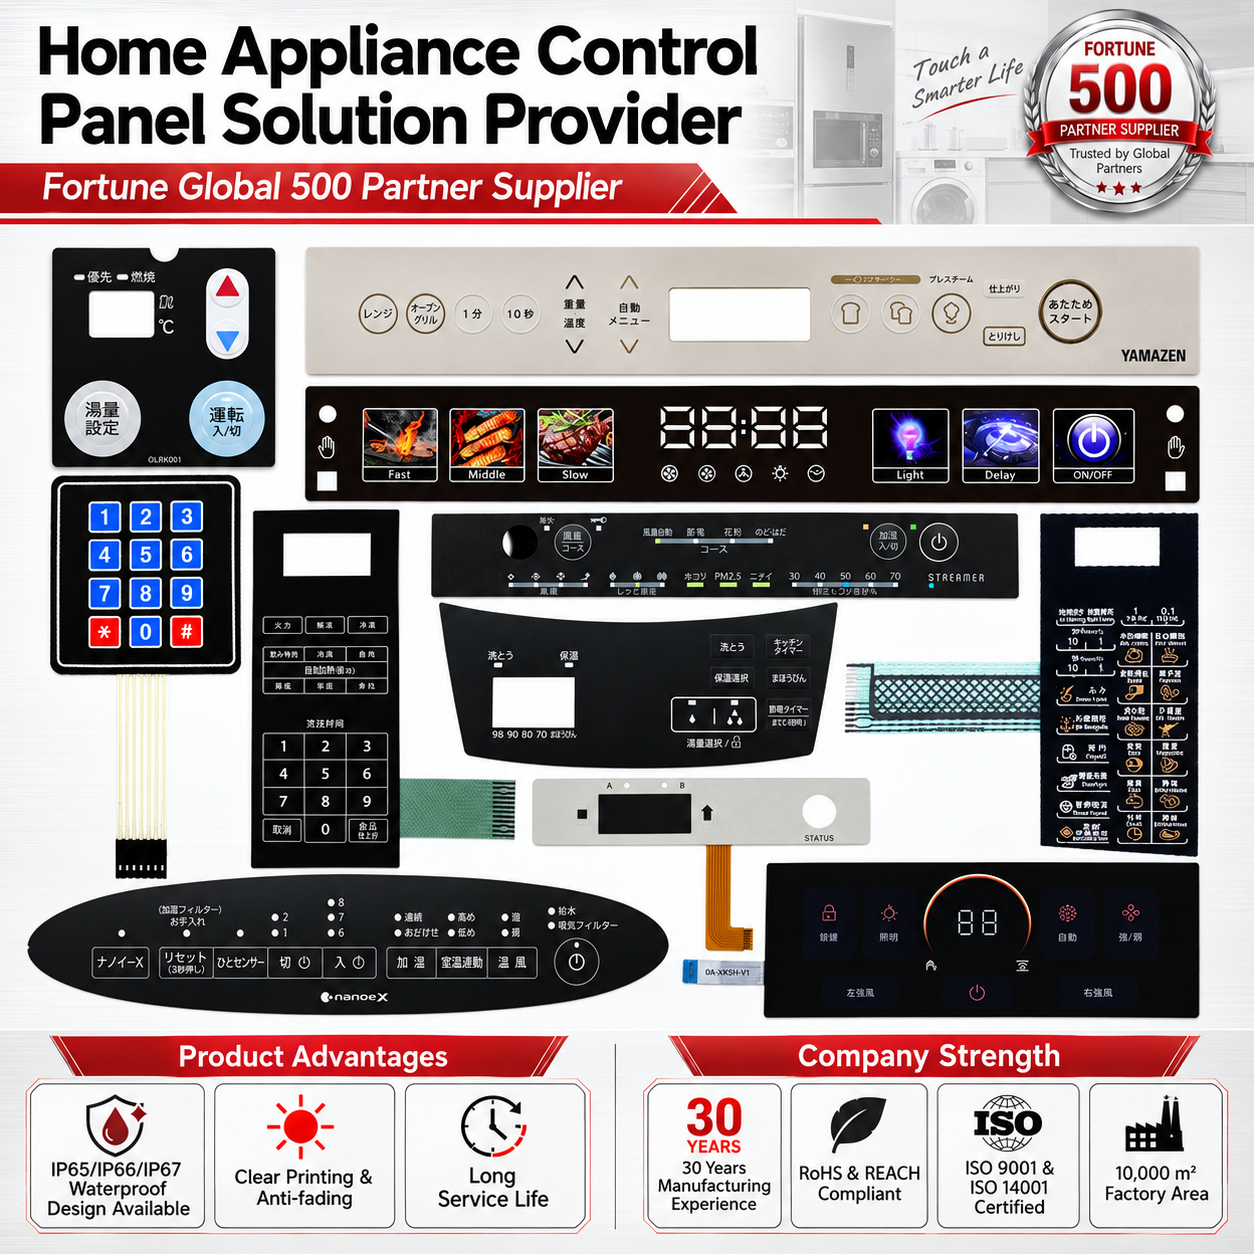
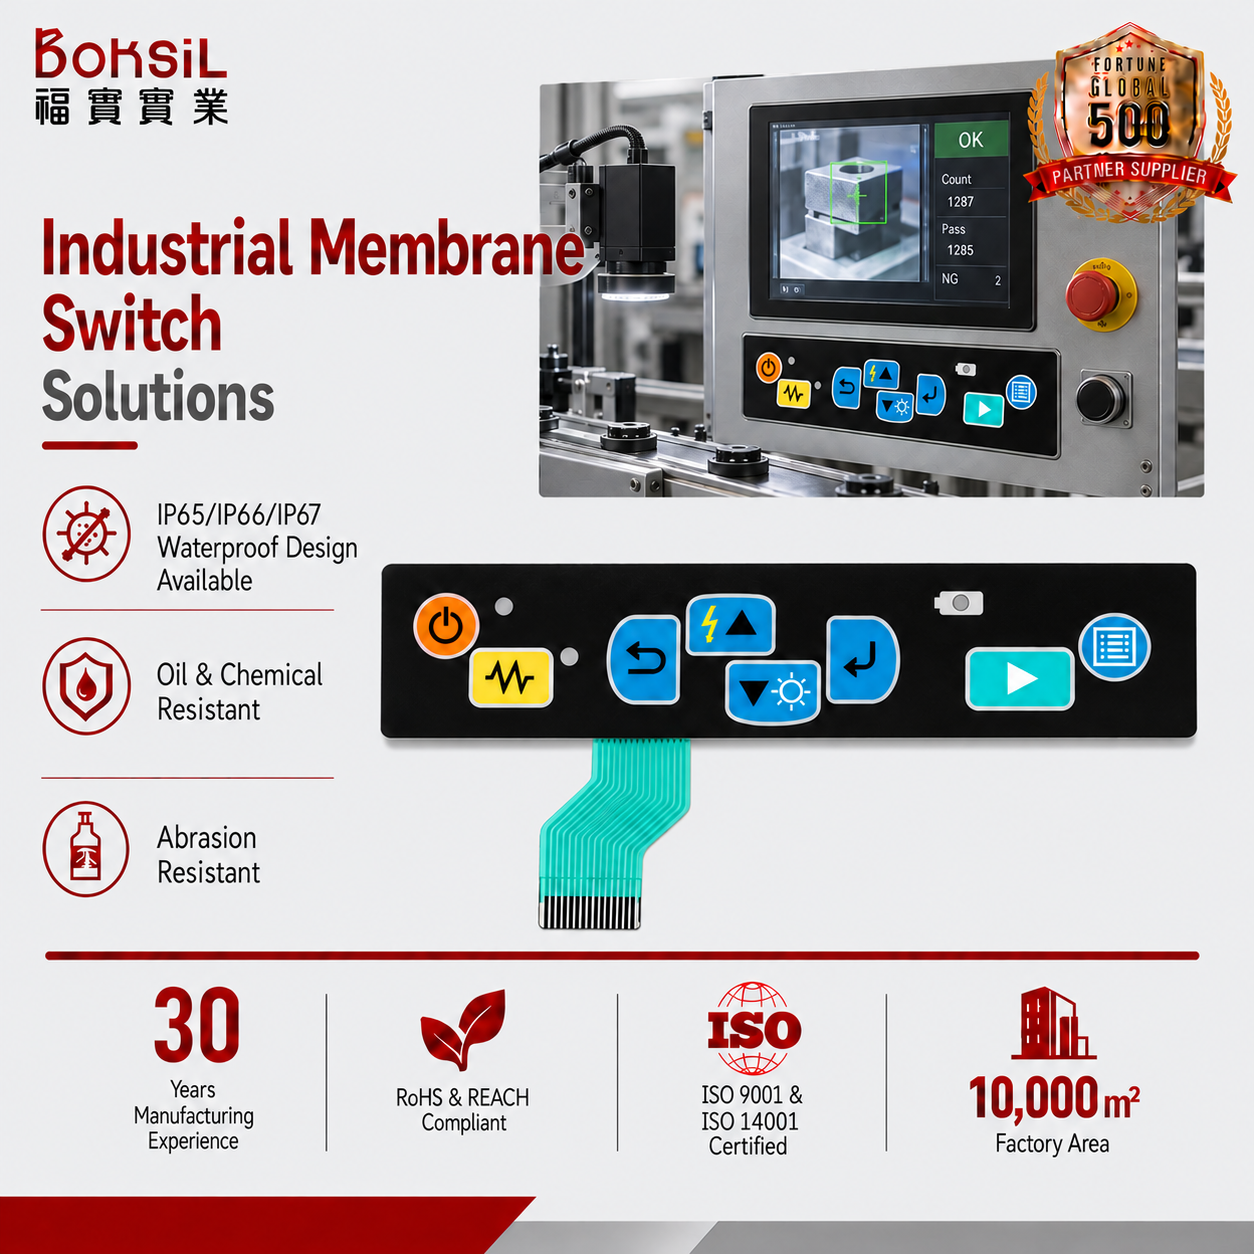
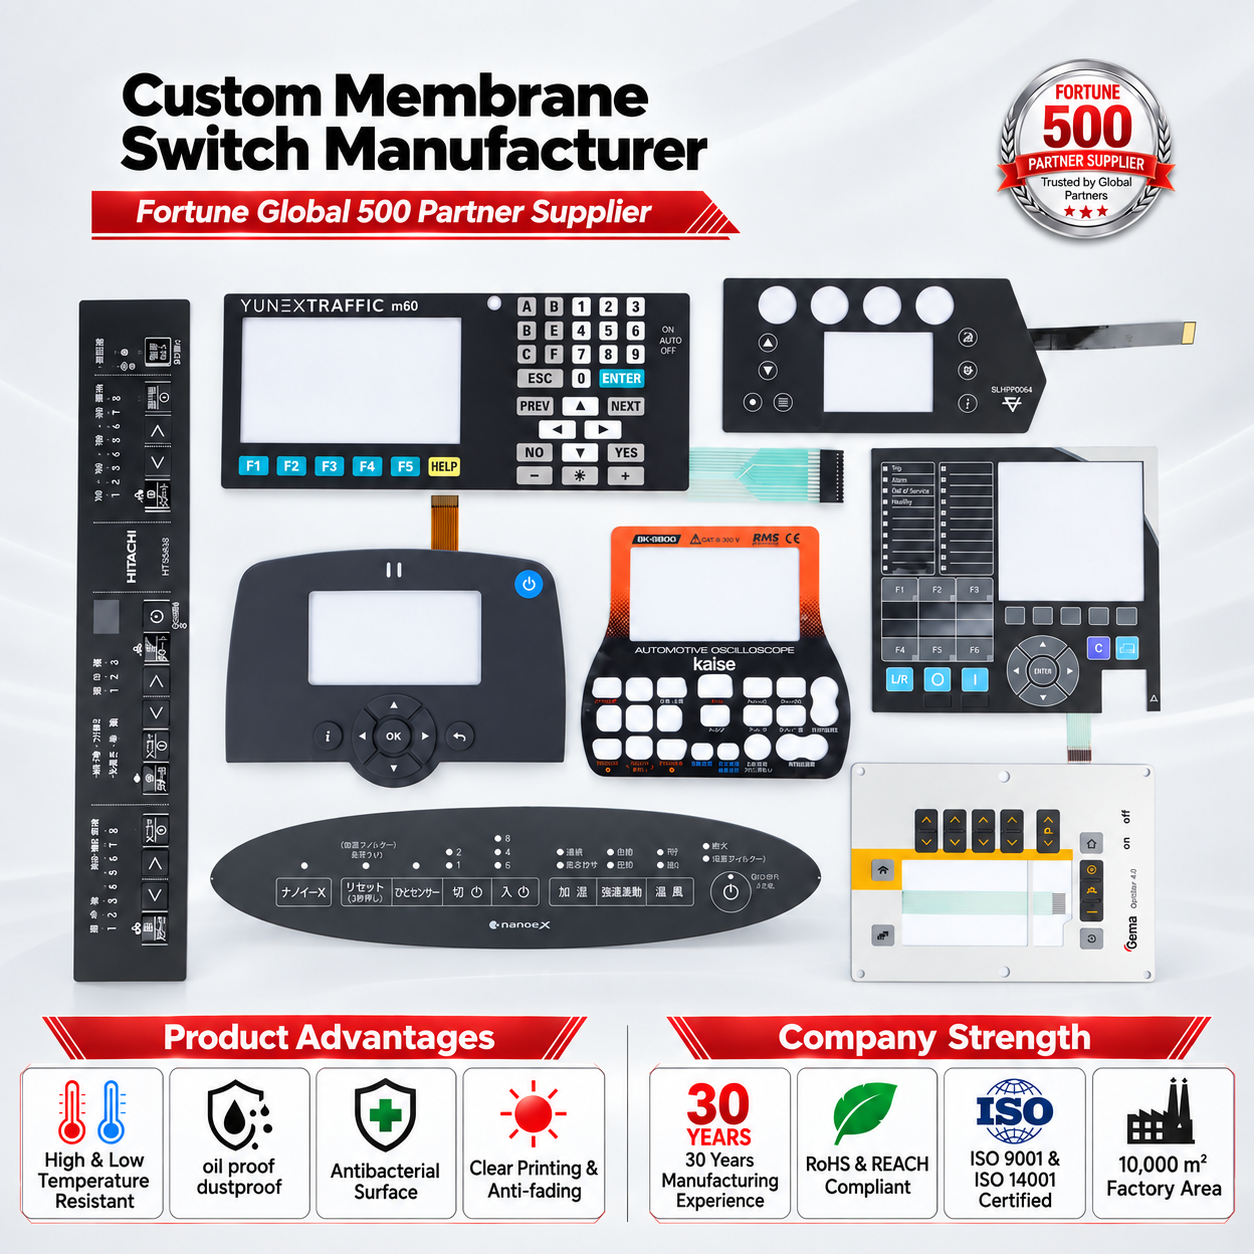
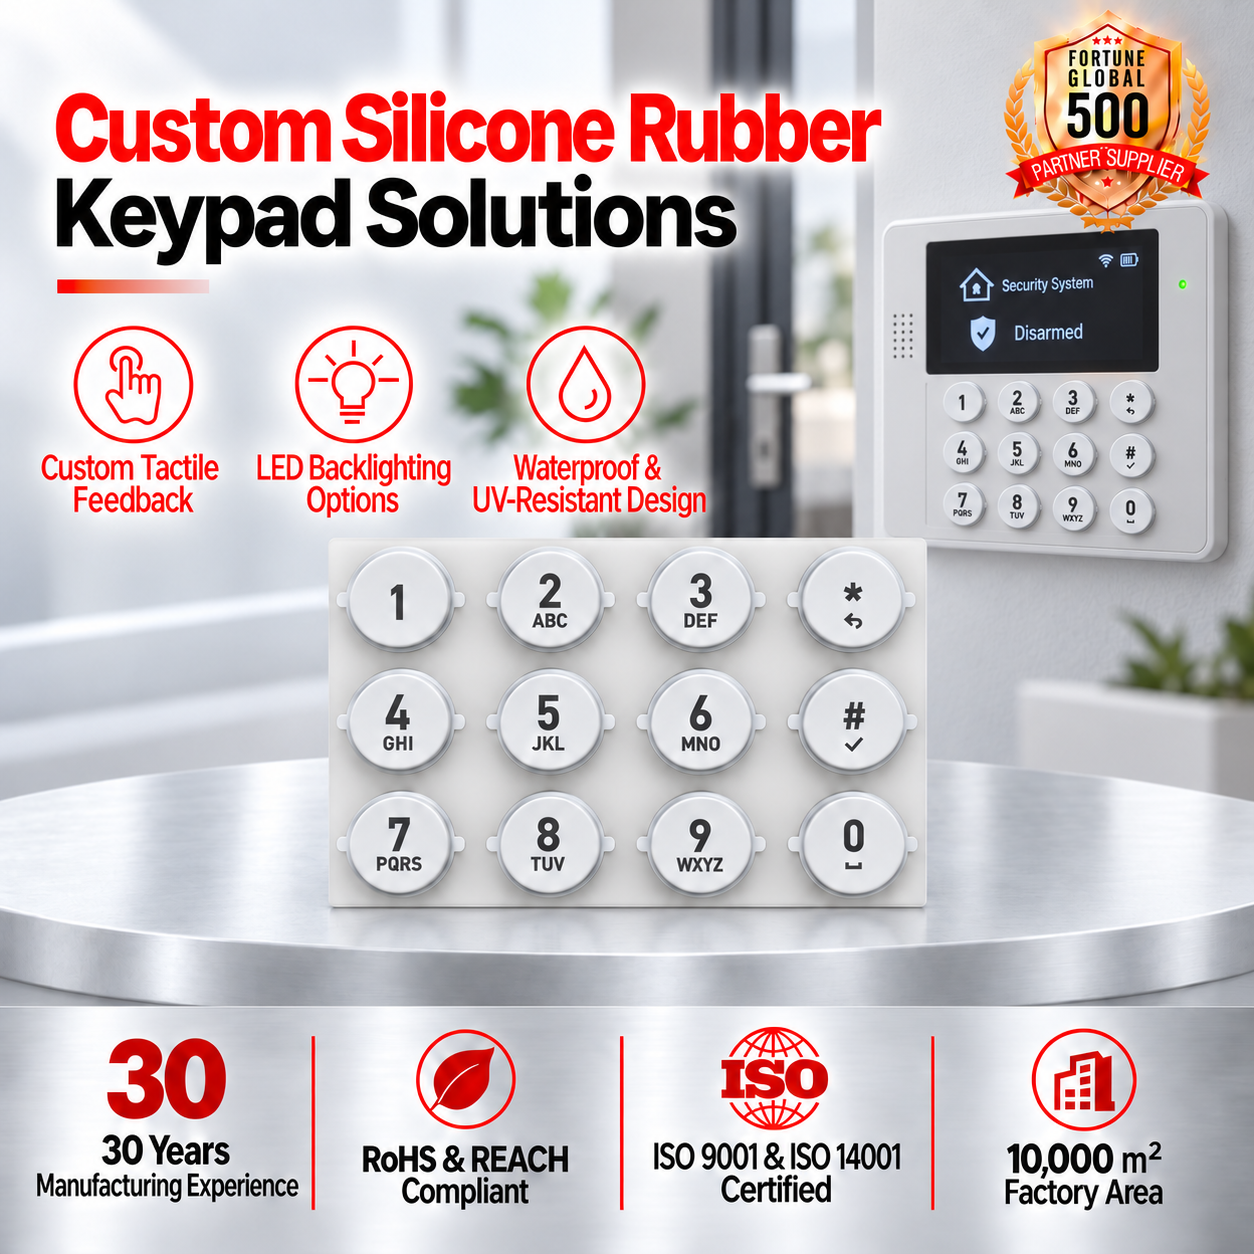
Engineering Membrane Keypads for Cartago's Infrastructure Ecosystem
Industrial deployment in the Cartago basin demands robust resistance to elevation fluctuations, microclimates, high ambient moisture, and continuous electrical transients.
High-Humidity & Thermal Cycle Integrity
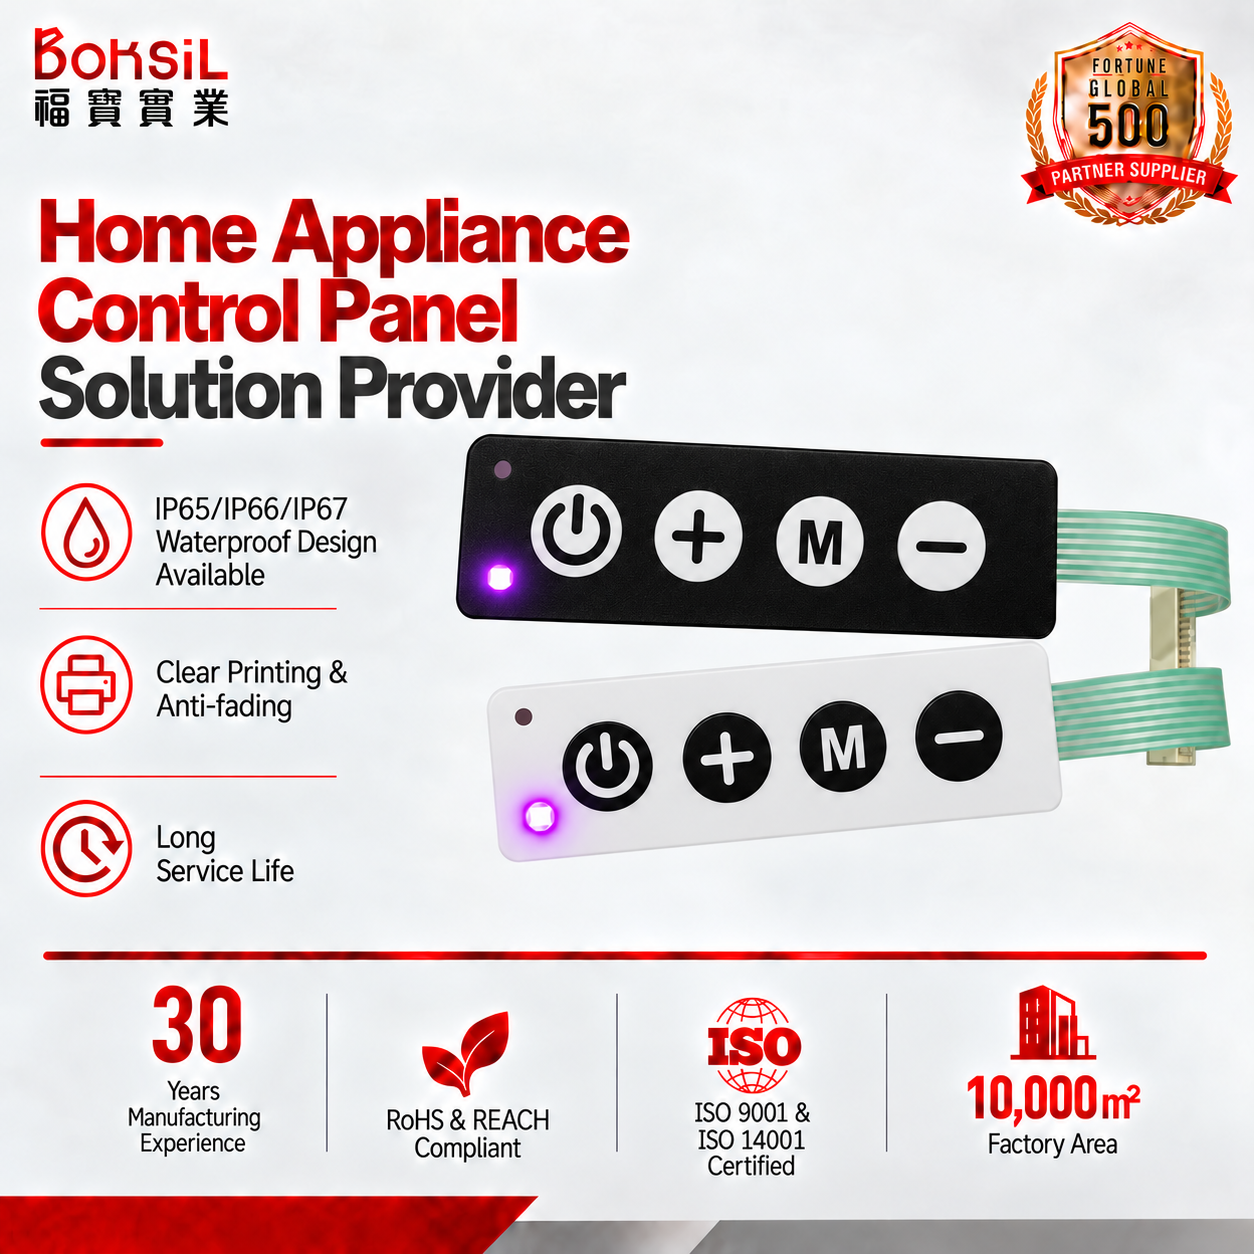
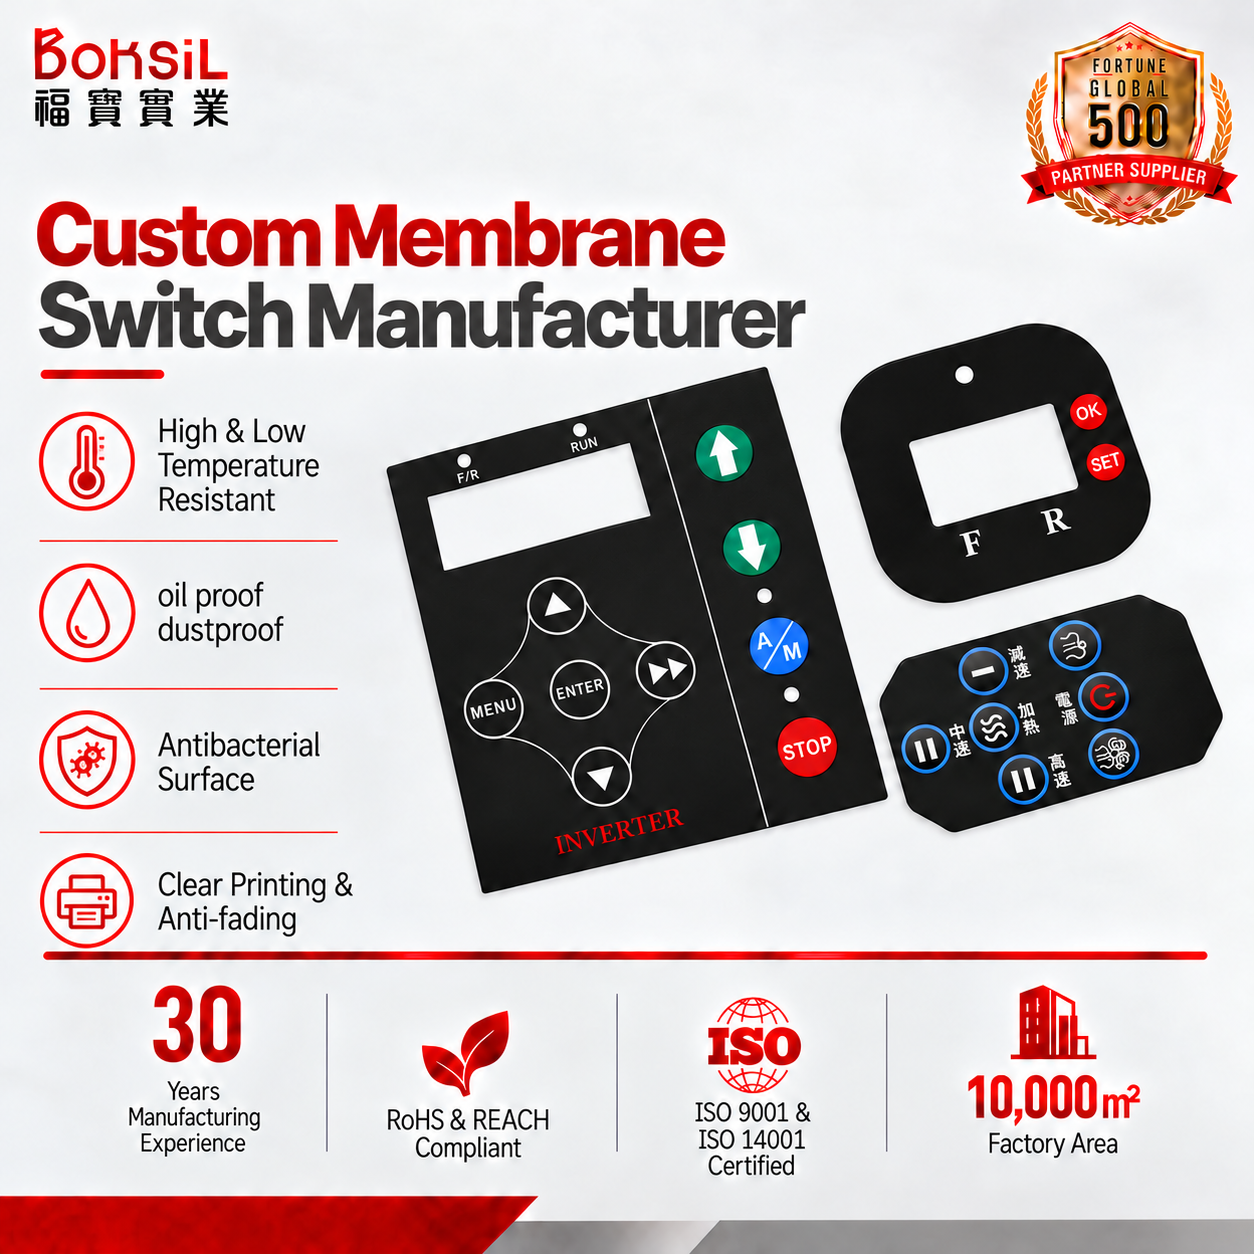
Cartago's tropical highland climate swings between warm afternoon sun and cold nighttime condensation. Our membrane switches deploy perimeter adhesive seals, hydrophobic micro-venting, and medical-grade PET films to prevent delamination and internal trace corrosion.
Transient Voltage & ESD Immunity
Outdoor traffic cabinets along major arterial roads face electromagnetic interference from power lines and lightning spikes. We integrate continuous aluminum foil or printed conductive carbon-silver shielding meshes to safeguard microcontrollers from electrostatic discharge up to 15kV.
Tactile Ergonomics for Field Technicians
Traffic technicians operating in high-stress roadside conditions demand definitive physical confirmation. Our stainless-steel metal domes, calibrated between 280g and 450g trip forces, provide crisp feedback even when handled with heavy industrial safety gloves.
Targeted Deployment Scenarios Across Cartago's Industrial & Urban Centers
From the bustling logistics hubs of the Central Valley to precision manufacturing zones, our interface switches maintain continuous operation.
Freight & Logistics Corridor Controls
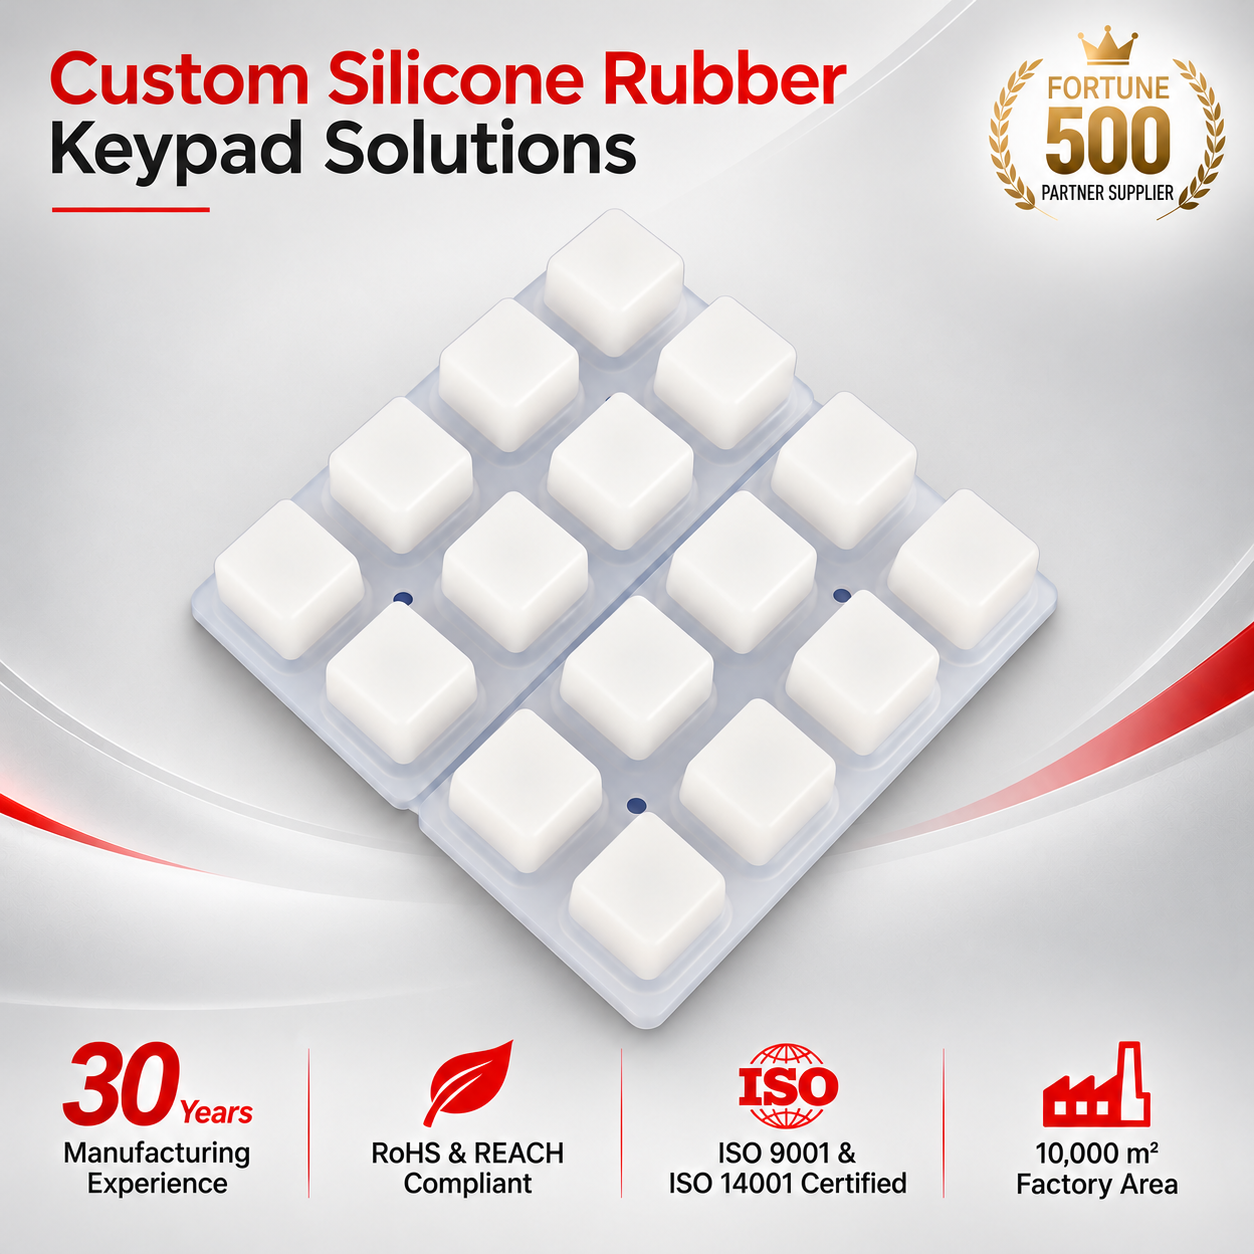
The transit corridors linking Cartago with national routes experience intense vibration and particulate exhaust. Our silicone rubber and sealed membrane keypad assemblies protect weigh stations, toll gate terminals, and barrier automation consoles from diesel grime and constant operation.
Free Trade Zone & Tech Park Automation
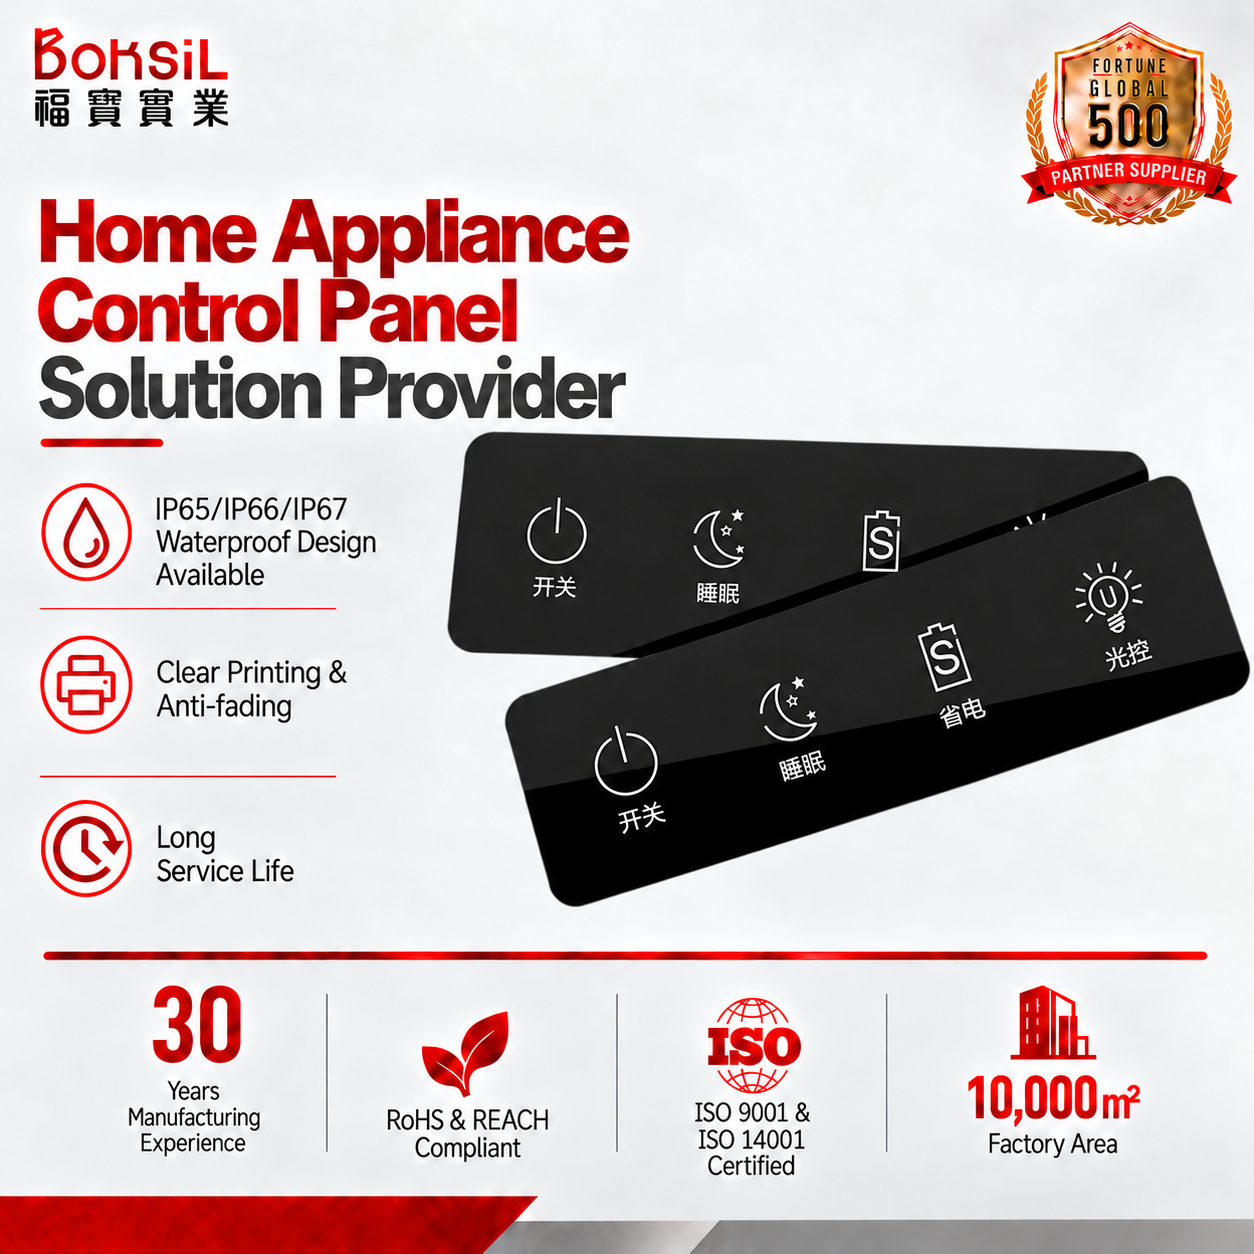
Cartago's expanding tech parks and life-science production clusters require immaculate control panels. We manufacture PMMA front panels and capacitive graphic overlays featuring selective texture contrasts, high optical transmittance, and chemical washdown resistance.
Municipal Traffic & Crosswalk Actuation
Pedestrian call buttons and roadside cabinet control units must survive direct sunlight, moisture, and vandalism. We supply anti-yellowing UV-resistant graphic overlays engineered with Lexan HP92W polycarbonate, backed by 3M 467MP/468MP high-tack performance adhesives.
HMI Substrate Architecture for Latin American Transportation Infrastructure
A technical overview comparing substrate specifications to guide procurement directors, hardware engineers, and systems integrators.
| Technology / Substrate | Environmental Sealing | Actuation Life Expectancy | UV & Chemical Resistance | Optimal Cartago Infrastructure Application |
|---|---|---|---|---|
| Polyester (Autotex PET) Membrane | IP65 to IP67 with perimeter adhesive barrier | 5,000,000+ switch operations | High chemical and abrasion resistance; zero micro-cracking | Standard traffic intersection controllers, internal cabinet diagnostic panels. |
| Polycarbonate (Lexan PC) Overlay | IP65 (Gasket mounted) | 1,000,000 switch operations | High optical clarity; requires hard-coat for outdoor UV stability | Cost-effective indoor monitoring consoles, display faceplates, utility stations. |
| Flexible Copper FPC Circuit | Hermetically sealed bond line | Over 10,000,000 cycles | Immune to silver migration; superior thermal dissipation | High-density connector pinouts, dense SMD LED matrix arrays, harsh humid nodes. |
| Silicone Rubber Keypad (P+R) | IP67 to IP68 continuous seal | 2,000,000 switch operations | Natural thermal resilience (-40°C to +150°C); ozone resistant | Handheld diagnostics, rugged outdoor push-to-walk buttons, high-abuse enclosures. |
Emerging Procurement & Modernization Trends in Cartago
Municipal infrastructure across Central America is undergoing modernization. System architects prioritize long-lifecycle components designed to reduce field service overhead.
Transition from Silver Conductive Ink to FPC
High relative humidity accelerates electrochemical silver migration under persistent DC bias. Engineering teams increasingly specify polyimide copper flexible printed circuits (FPC) to ensure uninterrupted decades of reliable conductivity.
Integrated Optical Light Guides (LGF)
Field maintenance at night requires uniform illumination without excessive power draw. Modern traffic cabinets utilize ultra-thin Light Guide Film (LGF) arrays, driving uniform light across status keys with minimal surface heat output.
Rigorous Intertek-Verified Validation
System bids and public transportation concessions demand comprehensive third-party testing. AXRU guarantees compliance through documented FAI reports, dynamic force-displacement profiling, and certified batch testing.
AXRU Electronics Co., Ltd. Technical Capabilities
Vertically integrated manufacturing direct from our 10,000㎡ plant, delivering OEM/ODM excellence to global industrial buyers.
Integrated Clean-Room Production
Screen printing, precision laser cutting, SMD soldering, and multilayer optical bonding are executed within our climate-controlled, dust-free manufacturing chambers, ensuring zero pinholes and flawless adhesion.
100% Comprehensive Inspection
Every individual keypad undergoes automated continuity testing, insulation resistance checking, switch contact bounce profiling, and cosmetic colorimetry matching against precise Pantone formulations.
Agile Prototyping & Scalable MOQ
We support engineering R&D with accessible low-volume production starting at an MOQ of 100 pieces. Dedicated DFM engineers assist your team with mechanical CAD conversions and rapid initial prototypes.
Frequently Asked Questions: Cartago Industrial Procurement
Essential guidance addressing engineering compliance, export logistics, and technical customization for local purchasers.
Q: What engineering documentation is required for custom tooling?
We work directly from mechanical 2D/3D files (DXF, DWG, STEP), vector artwork files (Adobe Illustrator with specified Pantone codes), schematic pinout matrices, and connector tail pitch tolerances. If you only possess an existing field unit, our team can reverse-engineer stack-up layers and electrical tracks.
Q: How do your keypads survive outdoor solar exposure and UV radiation?
We specify premium weatherable materials such as Autotex XE (UV-stabilized polyester) or UV-stabilized Lexan polycarbonate treated with advanced anti-glare hard coats. These materials resist yellowing, gloss fading, and embrittlement under intense tropical sunlight.
Q: What packaging safeguards are used for long-distance international transit?
All finished keypads are packed in anti-static ESD shielding bags, desiccated to prevent atmospheric humidity absorption, and secured in custom shock-absorbing foam trays within multi-wall corrugated export containers to guarantee undamaged delivery to Cartago.
Q: What is the standard sample and mass-production lead time?
Prototyping and engineering validation samples are completed within 7 to 10 working days following DFM drawing sign-off. Full mass-production runs typically dispatch within 15 to 20 working days, backed by priority air or consolidated ocean freight routing.
Upgrade Your Infrastructure Reliability with AXRU HMIs
Consult with our senior HMI project engineers today to evaluate custom stack-up configurations, receive a comprehensive DFM assessment, and secure factory-direct pricing for your next Cartago installation.