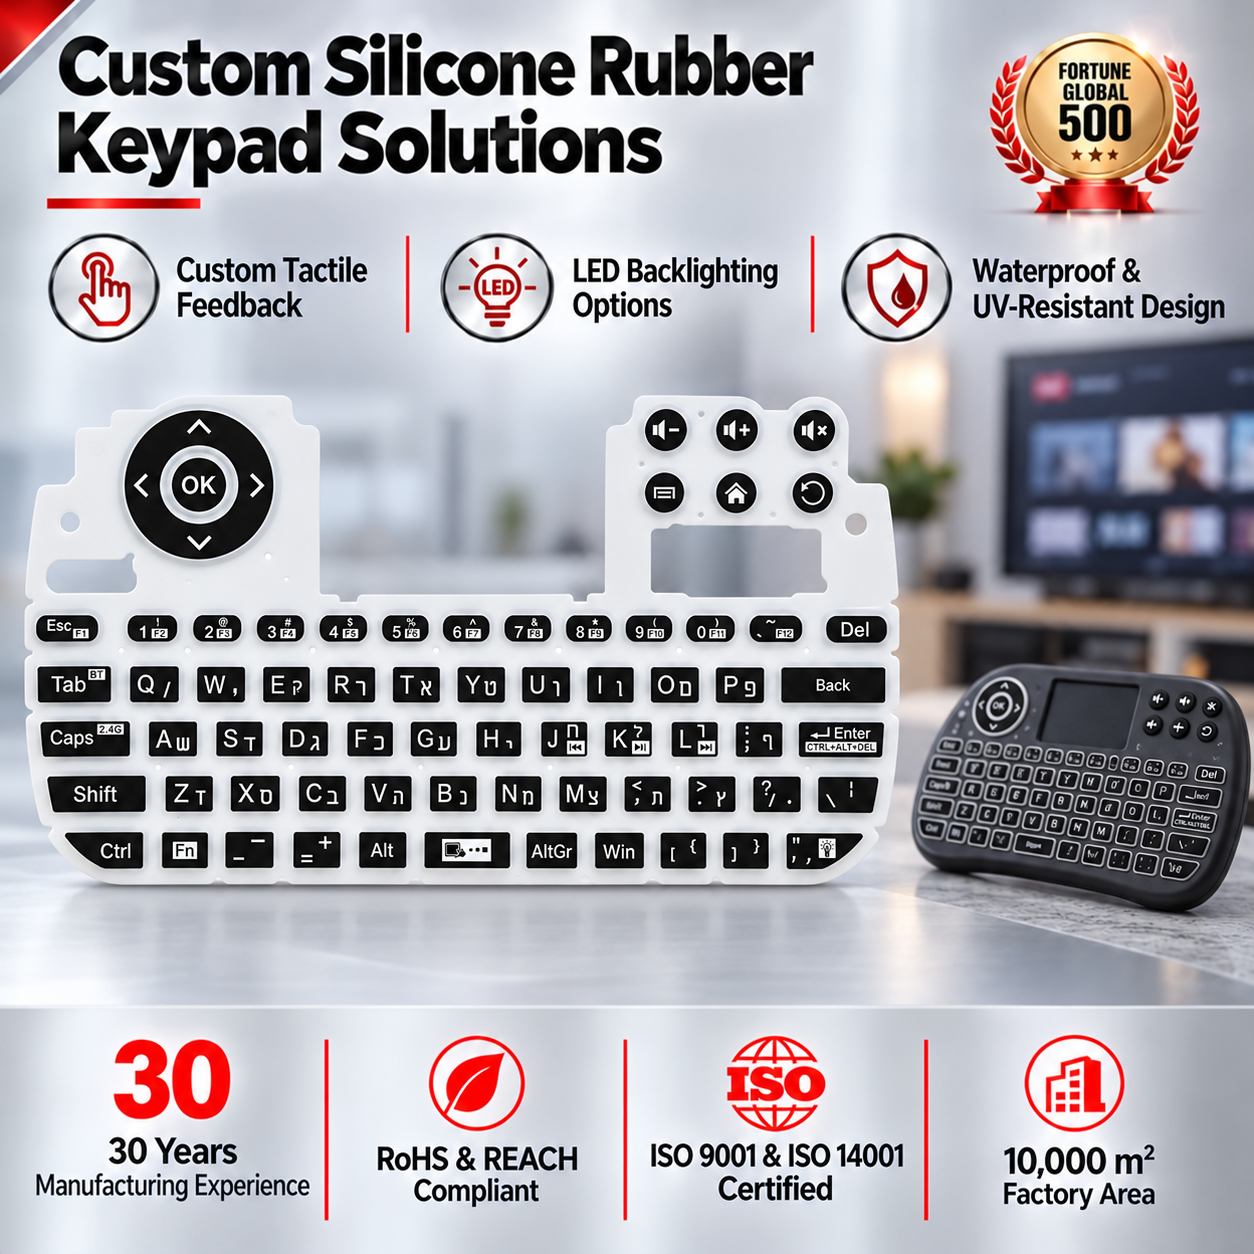
Mini Wireless QWERTY Silicone Rubber Keypad Customizable Soft Touch Elastomer Premium Feel Hotkey Button Matrix OEM
- Substrate: Conductive Silicone
- Actuation: Soft-Touch Tactile Pill
- Application: Handheld Terminals
Explore precision-fabricated membrane keypads, graphic overlays, force-sensitive resistors, and tactile elastomer assemblies built to survive sub-zero temperatures, harsh washdowns, and continuous operation.
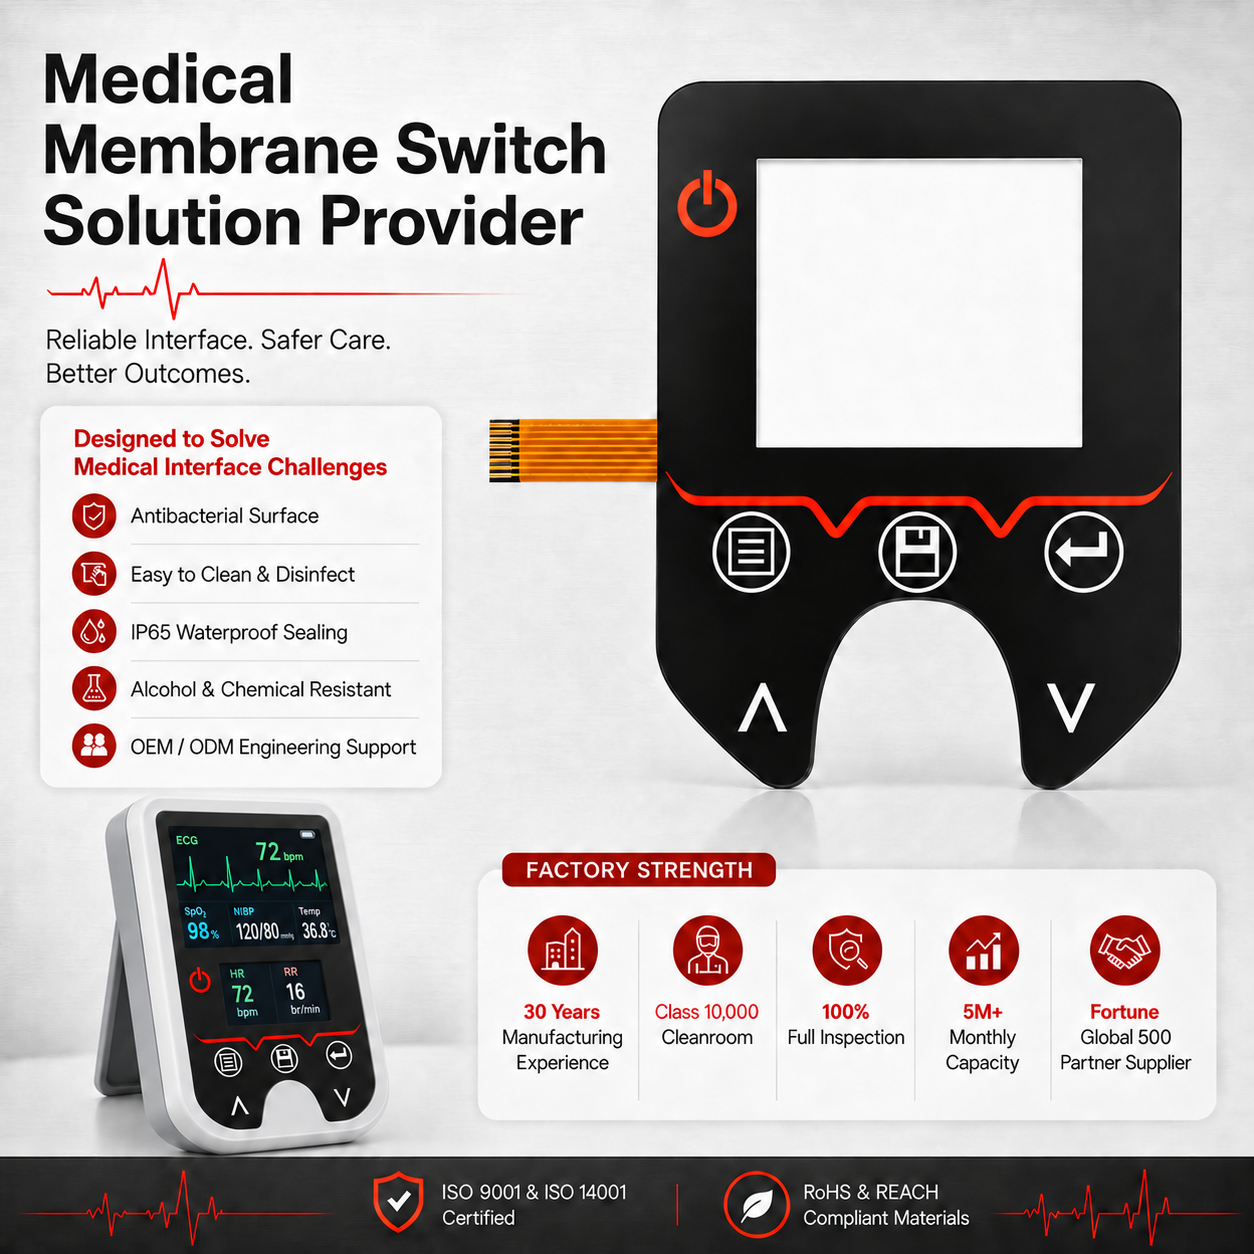
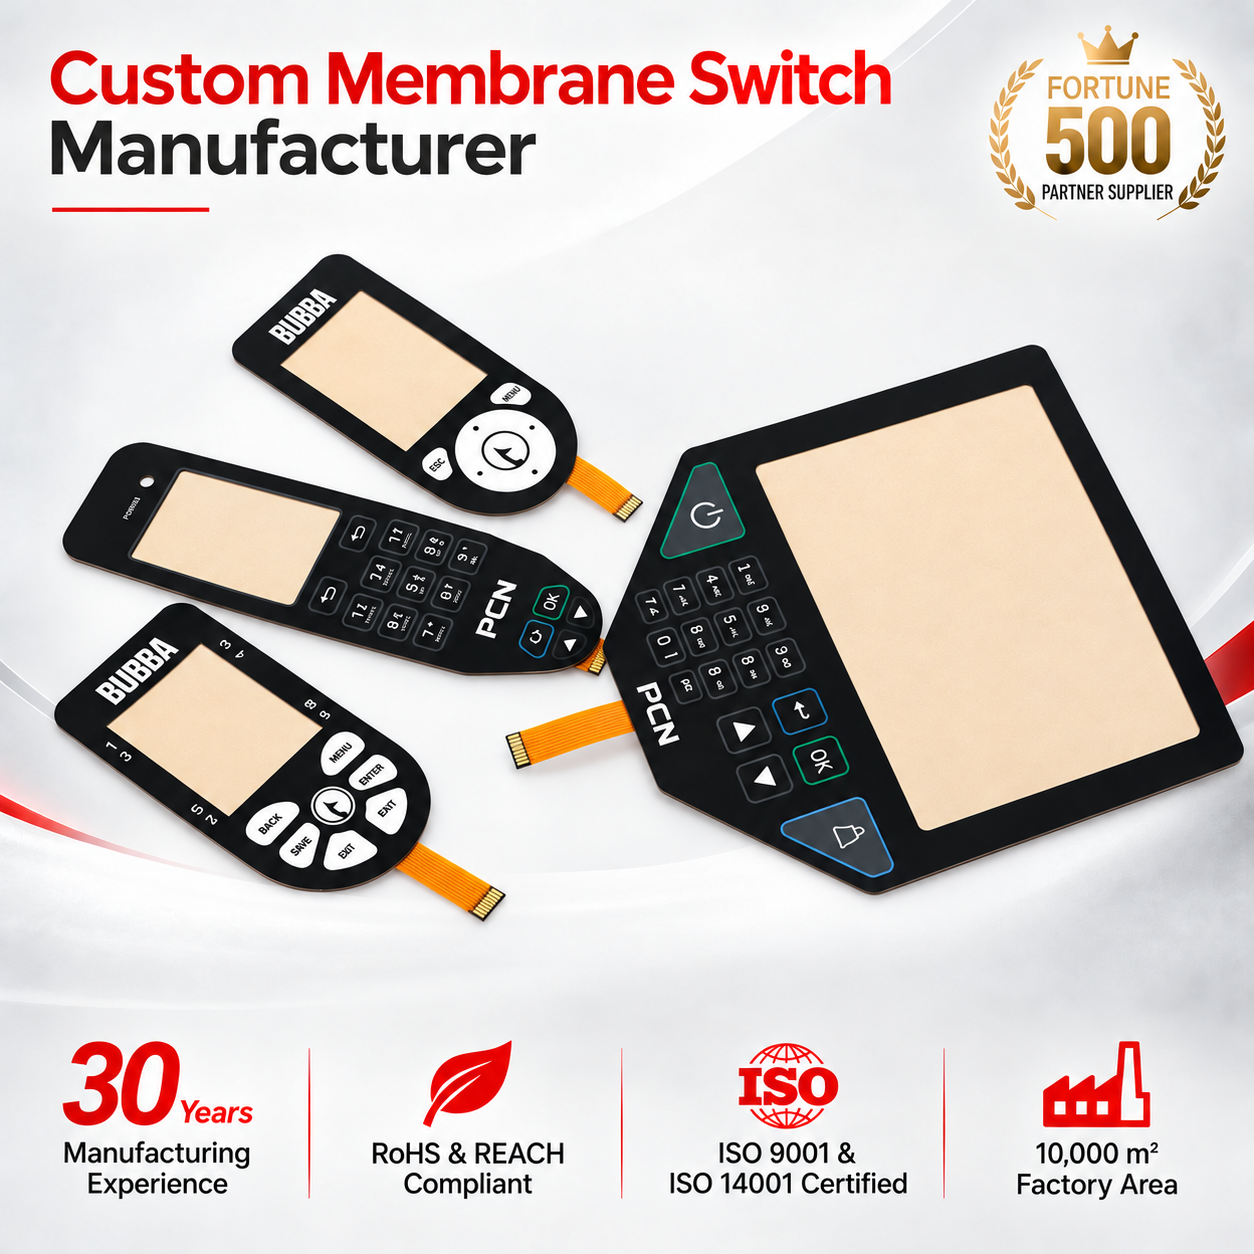
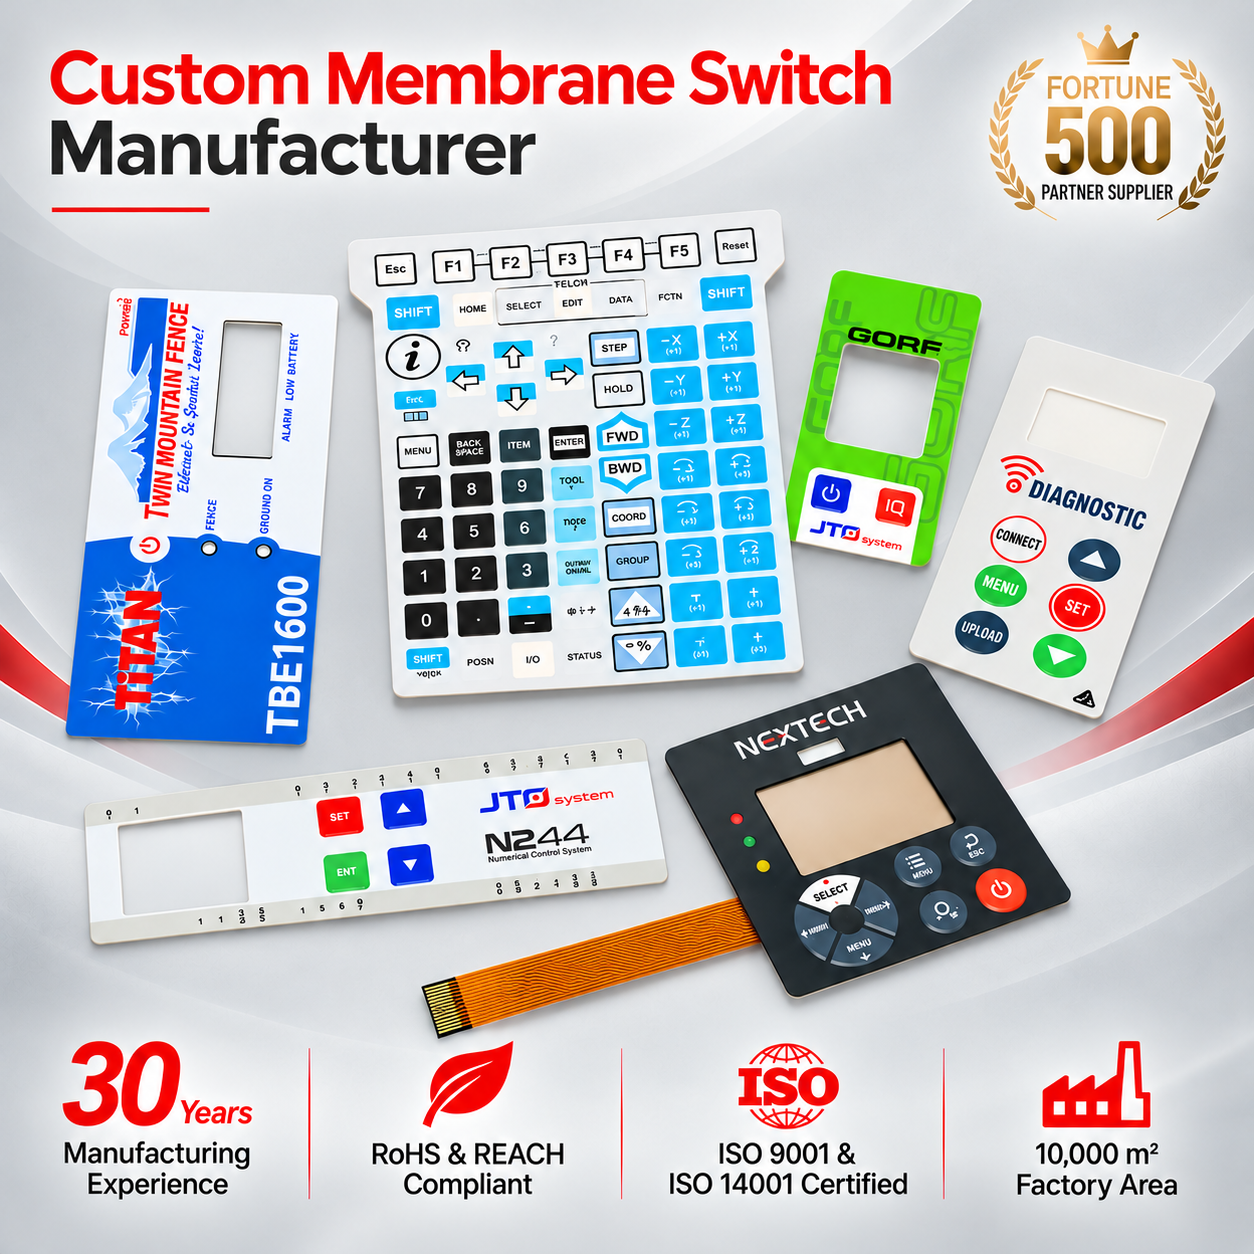
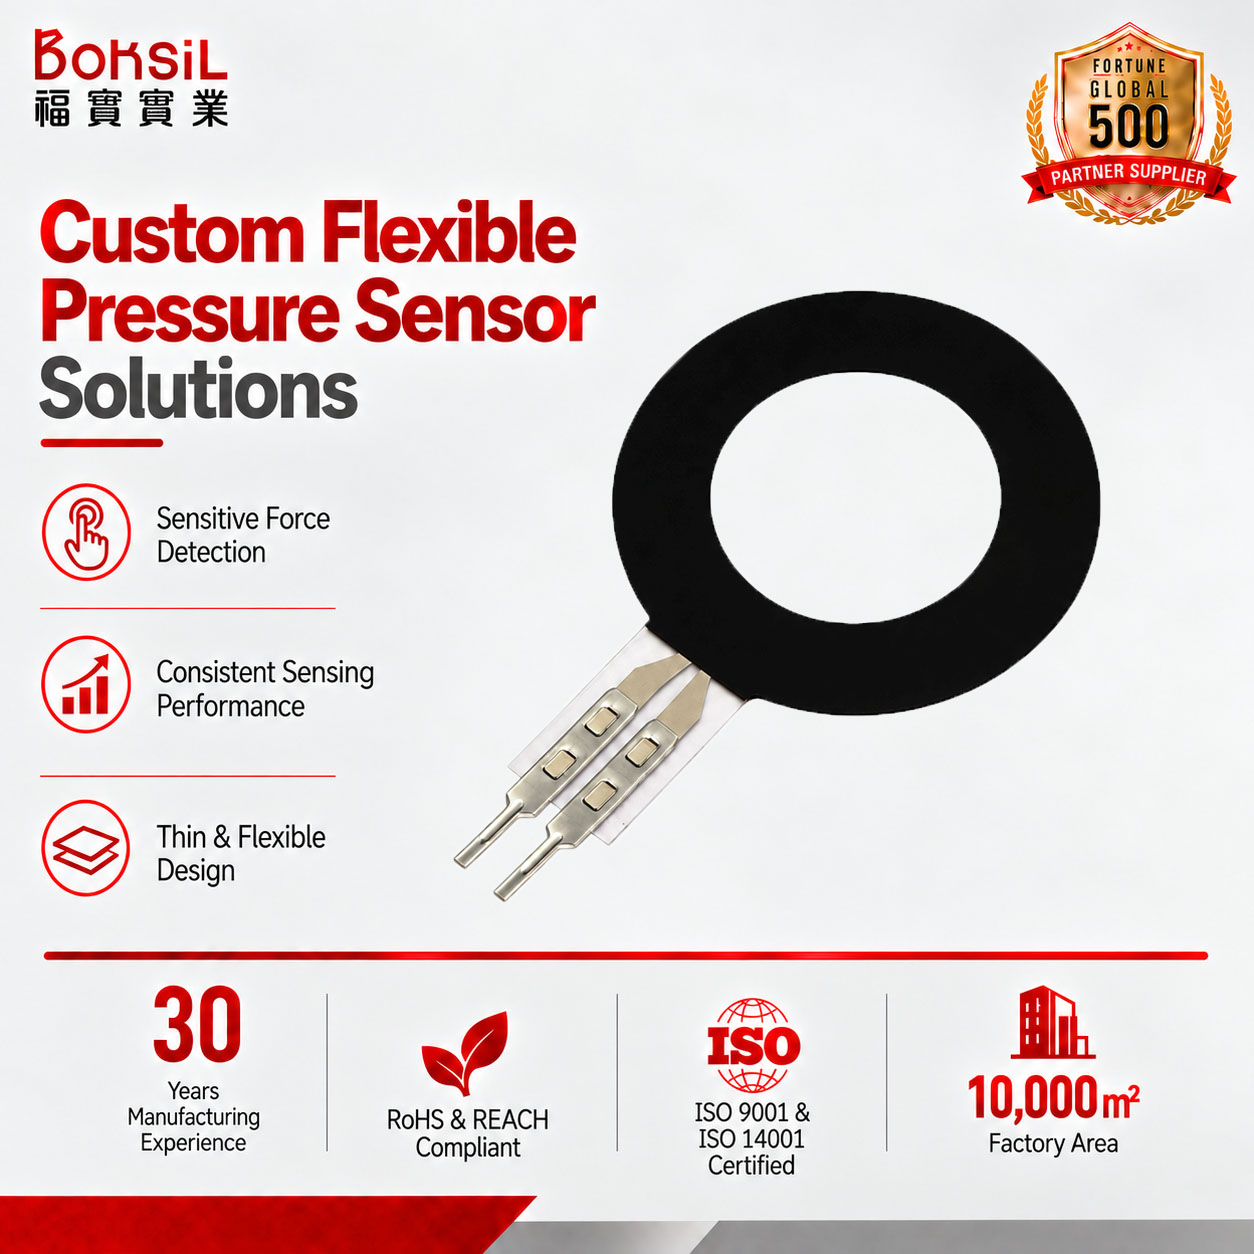
From the high-precision aerospace manufacturing corridor of Saint-Laurent and Longueuil to the world-class medtech clusters of Laval and the life-sciences corridor of Montreal, human-machine interface panels demand uncompromising engineering standards.
Montreal winters introduce drastic thermal shocks ranging from -35°C outdoor industrial conditions to +23°C heated facilities. Typical adhesives suffer shear failure and embrittlement under these extremes. Our specialized stack-ups employ high-shear 3M 467MP/468MP laminates and pre-conditioned Autotex polyester films that resist differential expansion and prevent bubble formation over millions of actuations.
Montreal's booming biotech and biomedical device enterprises (concentrated around Technoparc Montréal) require front panels that withstand continuous sterilization via isopropyl alcohol, bleach, quaternary ammonium, and vaporized hydrogen peroxide. Utilizing micro-textured, anti-microbial biaxially oriented PET guarantees optical clarity for displays while securing continuous IP65/IP67 perimeter washdown sealing.
Greater Montreal stands as one of the world's premier aerospace hubs alongside Toulouse and Seattle. Interface switches integrated into ground-support instrumentation, avionics test bays, and Bombardier/Alstom transit rolling-stock components necessitate gold-plated stainless steel metal domes with positive tactile snap-ratios that function faultlessly under sustained mechanical harmonic resonance.
A rigorous comparative analysis of the primary domestic fabricators and premier direct-factory offshore exporters delivering HMI solutions to Quebec's advanced manufacturing sector.
| Supplier Entity | Operation Base | Core Capabilities & Technology Stack | Lead Time & MOQ Profile | Market Suitability |
|---|---|---|---|---|
| Dongguan AXRU Electronics Co., Ltd. | Direct Manufacturer (Dongguan, CN) / Global Export | 10,000㎡ plant; In-house screen/digital printing, copper FPC/silver PET circuits, cleanroom dome arrays, capacitive touch, IMD & silicone molding. Intertek verified. | Prototypes: 5–7 days Mass Prod: 12–15 days MOQ: 100 pcs |
Best Overall Value: Direct factory pricing, zero middleman markups, deep DFM support, and unmatched flexibility for Montreal OEMs scaling from low to high volumes. |
| eptca (Electronic Products Tracking / Cadence) | Local QC / Regional Sourcing (Montreal Region, QC) | Local contract manufacturing coordination, quick turnaround on design consultation, focus on cable assemblies and interface integration. | Prototypes: 2–3 weeks Production: 4–6 weeks MOQ: Variable |
Proximity advantage for urgent rapid-response design iterations within Quebec borders, balanced against higher unit pricing. |
| Sylmepron Inc. | Quebec, Canada (Domestic Converter) | Industrial silk-screen printing, nameplates, front panels, metal tags, and basic flat membrane overlays for heavy machinery. | Prototypes: 1–2 weeks Production: 3–5 weeks MOQ: Mid to High |
Solid choice for basic graphic overlays and ruggedized machine nameplates requiring strict domestic content sourcing. |
| Nelson-Miller Inc. | Headquarters USA / Manufacturing Global | Broad HMI solutions, touchscreens, optical bonding, backlighting films, and complex medical user-interfaces. | Prototypes: 3–4 weeks Production: 6–8 weeks MOQ: High volume preference |
Enterprise-tier solution for multi-million-dollar programs with extended procurement windows and heavy administrative budgets. |
| XY-Global Precision | Direct Exporter (China) to NA | Membrane keypad matrix, CNC parts, injection tooling, simple membrane overlays for domestic electronic appliances. | Prototypes: 7–10 days Production: 2–3 weeks MOQ: 500 pcs |
General hardware enclosure supplier providing membrane panels as a companion accessory to plastic/die-cast casings. |
| PentaTouch Engineering | Ontario / Serving Eastern Canada | Custom tactile membrane keypads, graphic overlays, antimicrobial medical faces, sub-assembly integration. | Prototypes: 2–3 weeks Production: 4–5 weeks MOQ: Moderate |
Regional supplier with solid technical knowledge of Canadian electrical safety standards (CSA) and rail transit needs. |
| Cixi Membrane Switch Works | Direct Manufacturer (Ningbo, CN) | High-volume low-cost membrane matrix keypads, PVC graphic overlays, household appliance button arrays. | Prototypes: 10–12 days Production: 3 weeks MOQ: 1,000 pcs |
Cost-effective for high-volume, price-sensitive consumer goods where fine-pitch circuitry and harsh-environment durability are secondary. |
| Lustre-Art (Visual Interfaces) | Montreal, QC | Specialized fine-line screen printing, cosmetic front bezels, automotive dials, and polycarbonate industrial fascias. | Prototypes: 10 days Production: 3–4 weeks MOQ: Low-to-mid |
Excellent local artisan craftsmanship for visual faceplates and architectural control faceplates within Quebec. |
| Synergy HMI Solutions | USA / Canadian Distribution Channel | Capacitive sensor foils, backlighting light guide films (LGF), rugged military-grade tactile keypads. | Prototypes: 4 weeks Production: 6–8 weeks MOQ: Strictly High |
Specialized high-end solutions for aerospace and defense clients with dedicated ITAR or defense-procurement constraints. |
| KeeTouch Technologies | Direct Manufacturer (Shenzhen, CN) | Industrial touch displays, surface acoustic wave panels, companion membrane function buttons. | Prototypes: 2 weeks Production: 3–4 weeks MOQ: 300 pcs |
Suitable for kiosk builders and interactive terminals requiring display hardware married to auxiliary membrane switch arrays. |
The convergence of artificial intelligence, edge IoT computing, and advanced polymer chemistry is radically redefining what Canadian engineering teams require from human-machine interfaces.
Traditional bulky electro-luminescent (EL) lamps and discrete fiber optics are being replaced by ultra-thin 0.125mm Light Guide Films (LGF). Driven by side-firing surface-mount micro-LEDs, LGF channels uniform, glare-free luminescence across discrete button icons, ideal for ambient-lit medical operatory suites and night-shift transport operations in Montreal.
While screen-printed conductive silver ink on polyester remains the standard for cost-effective matrix routing, high-density Montreal tech designs increasingly leverage Flexible Printed Circuits (FPC). Copper-clad polyimide accommodates ultra-fine pitch (down to 0.5mm), facilitates reliable reflow soldering of active IC drivers, and eliminates the risk of silver ion migration under humid conditions.
In post-pandemic healthcare environments, surface sanitization is aggressive. New HMI architectures fuse inorganic, nano-silver antibacterial additives directly into the textured polyester top coat (such as Autotex AM). Because the anti-microbial agent is distributed throughout the hard-coat matrix rather than just sprayed on top, it never leaches out under repeated chemical wiping.
Rather than binary on/off switching, modern robotics and industrial machinery controllers engineered across Quebec require dynamic pressure feedback. FSR films printed with variable-resistance piezoresistive carbon links translate mechanical squeeze force into analog voltage gradients, enabling smooth proportional speed control in mobile machinery.
Why do tier-1 Canadian manufacturers bypass trading brokers and contract assemblers to partner directly with AXRU Electronics? In-house vertical control from DFM to final automated inspection.
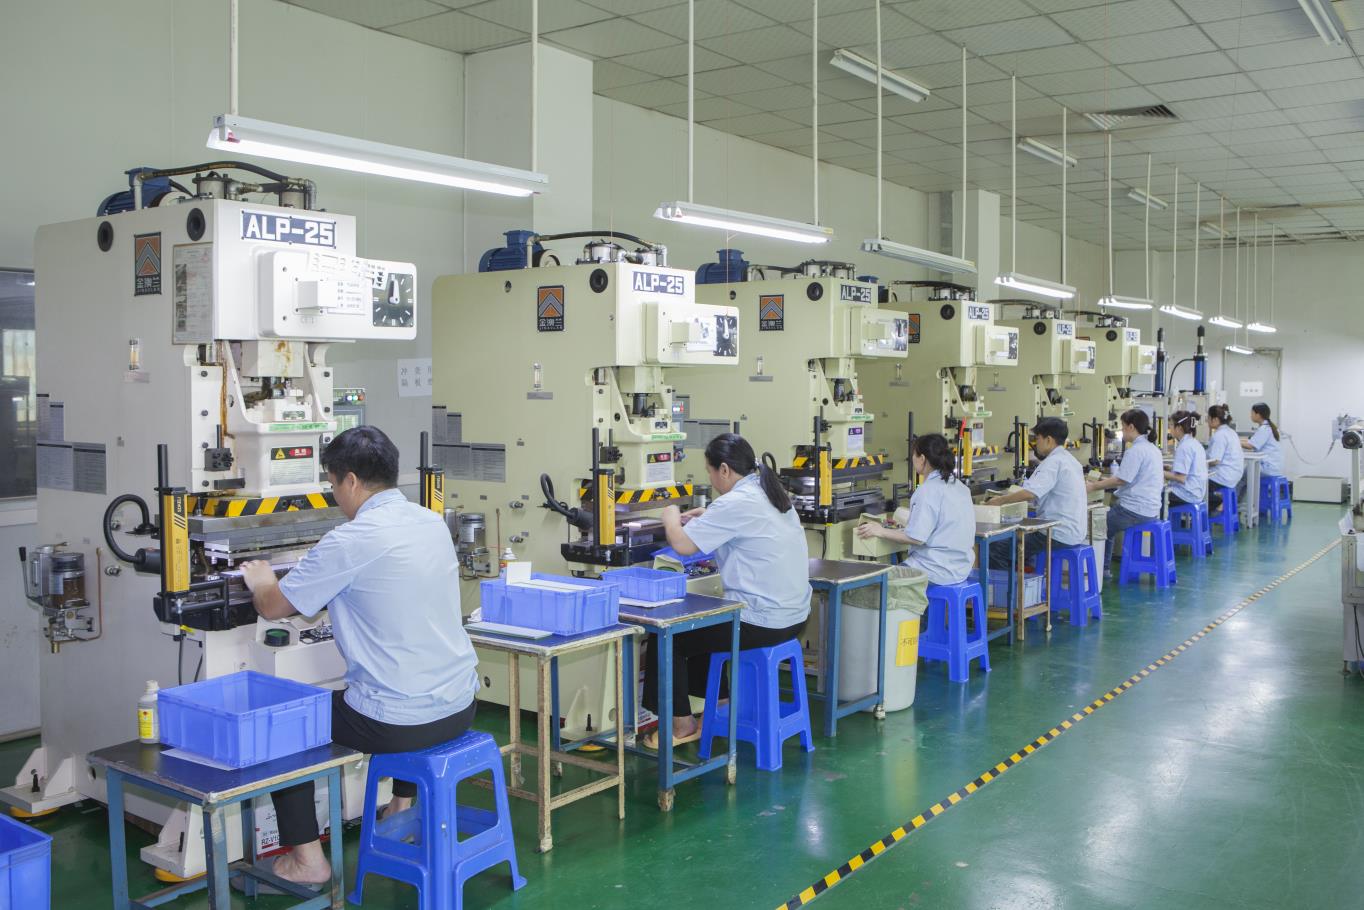
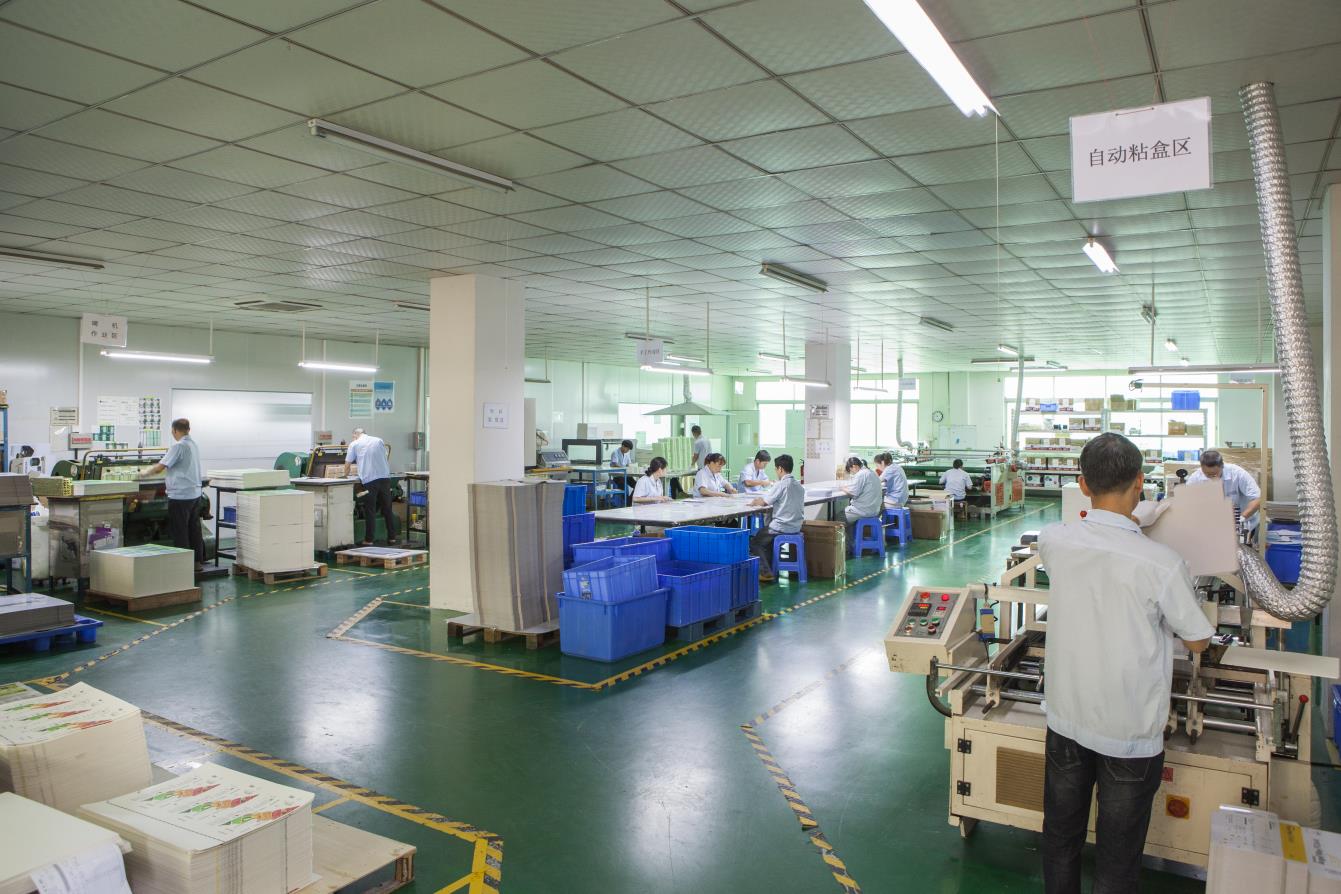
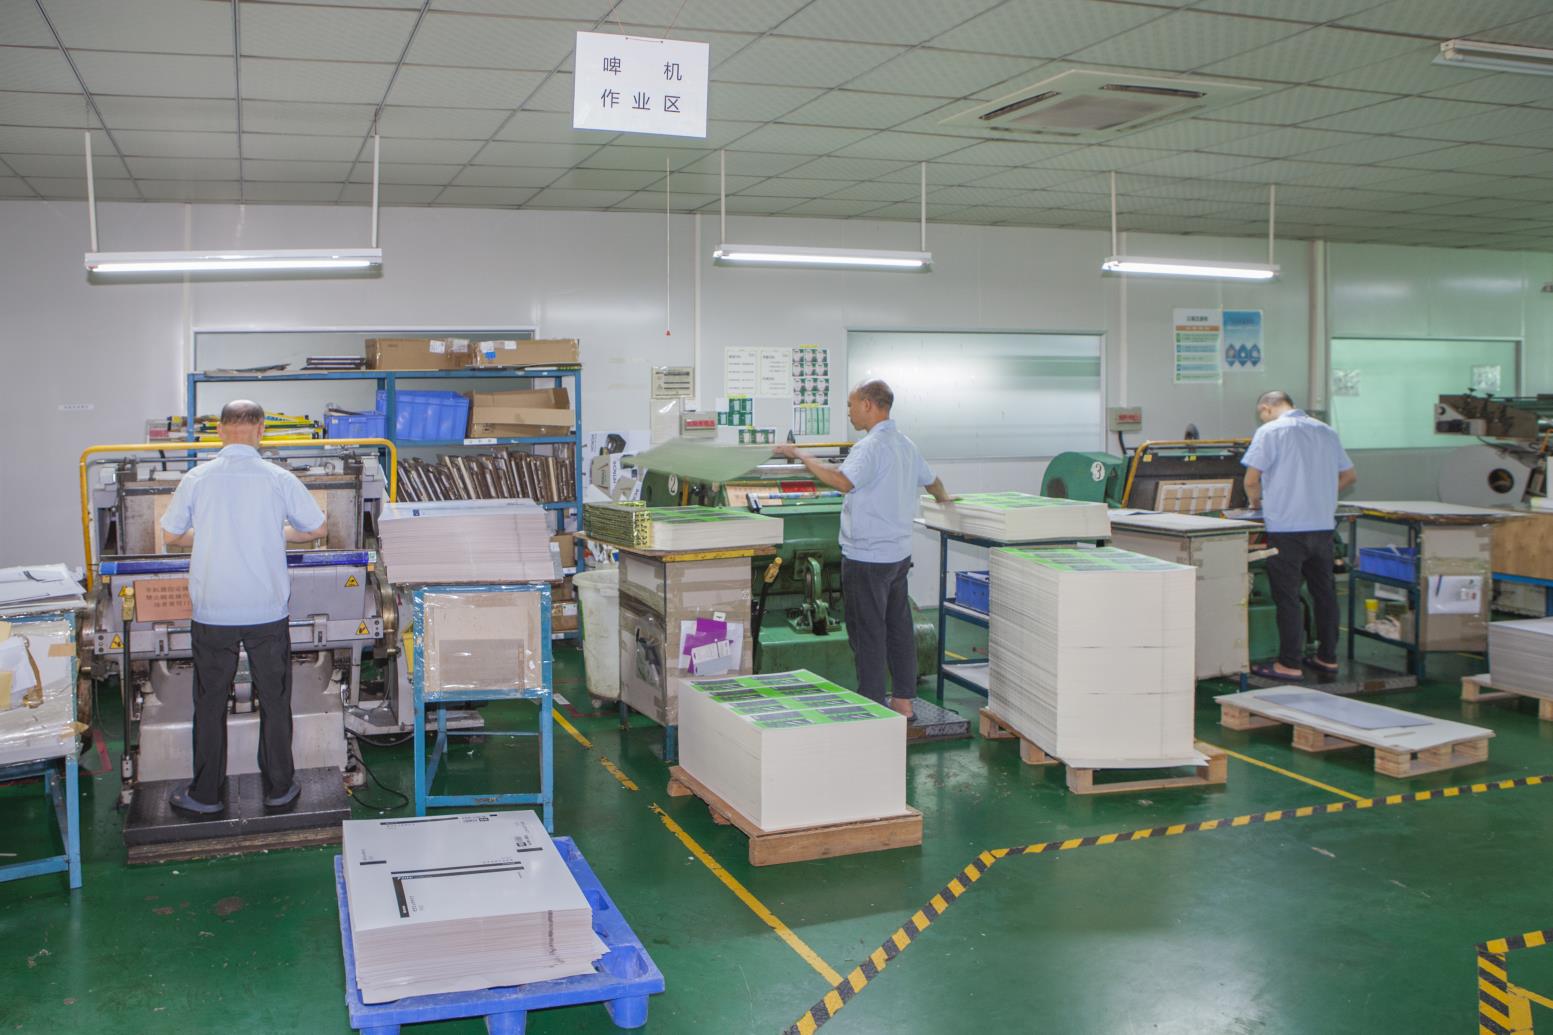
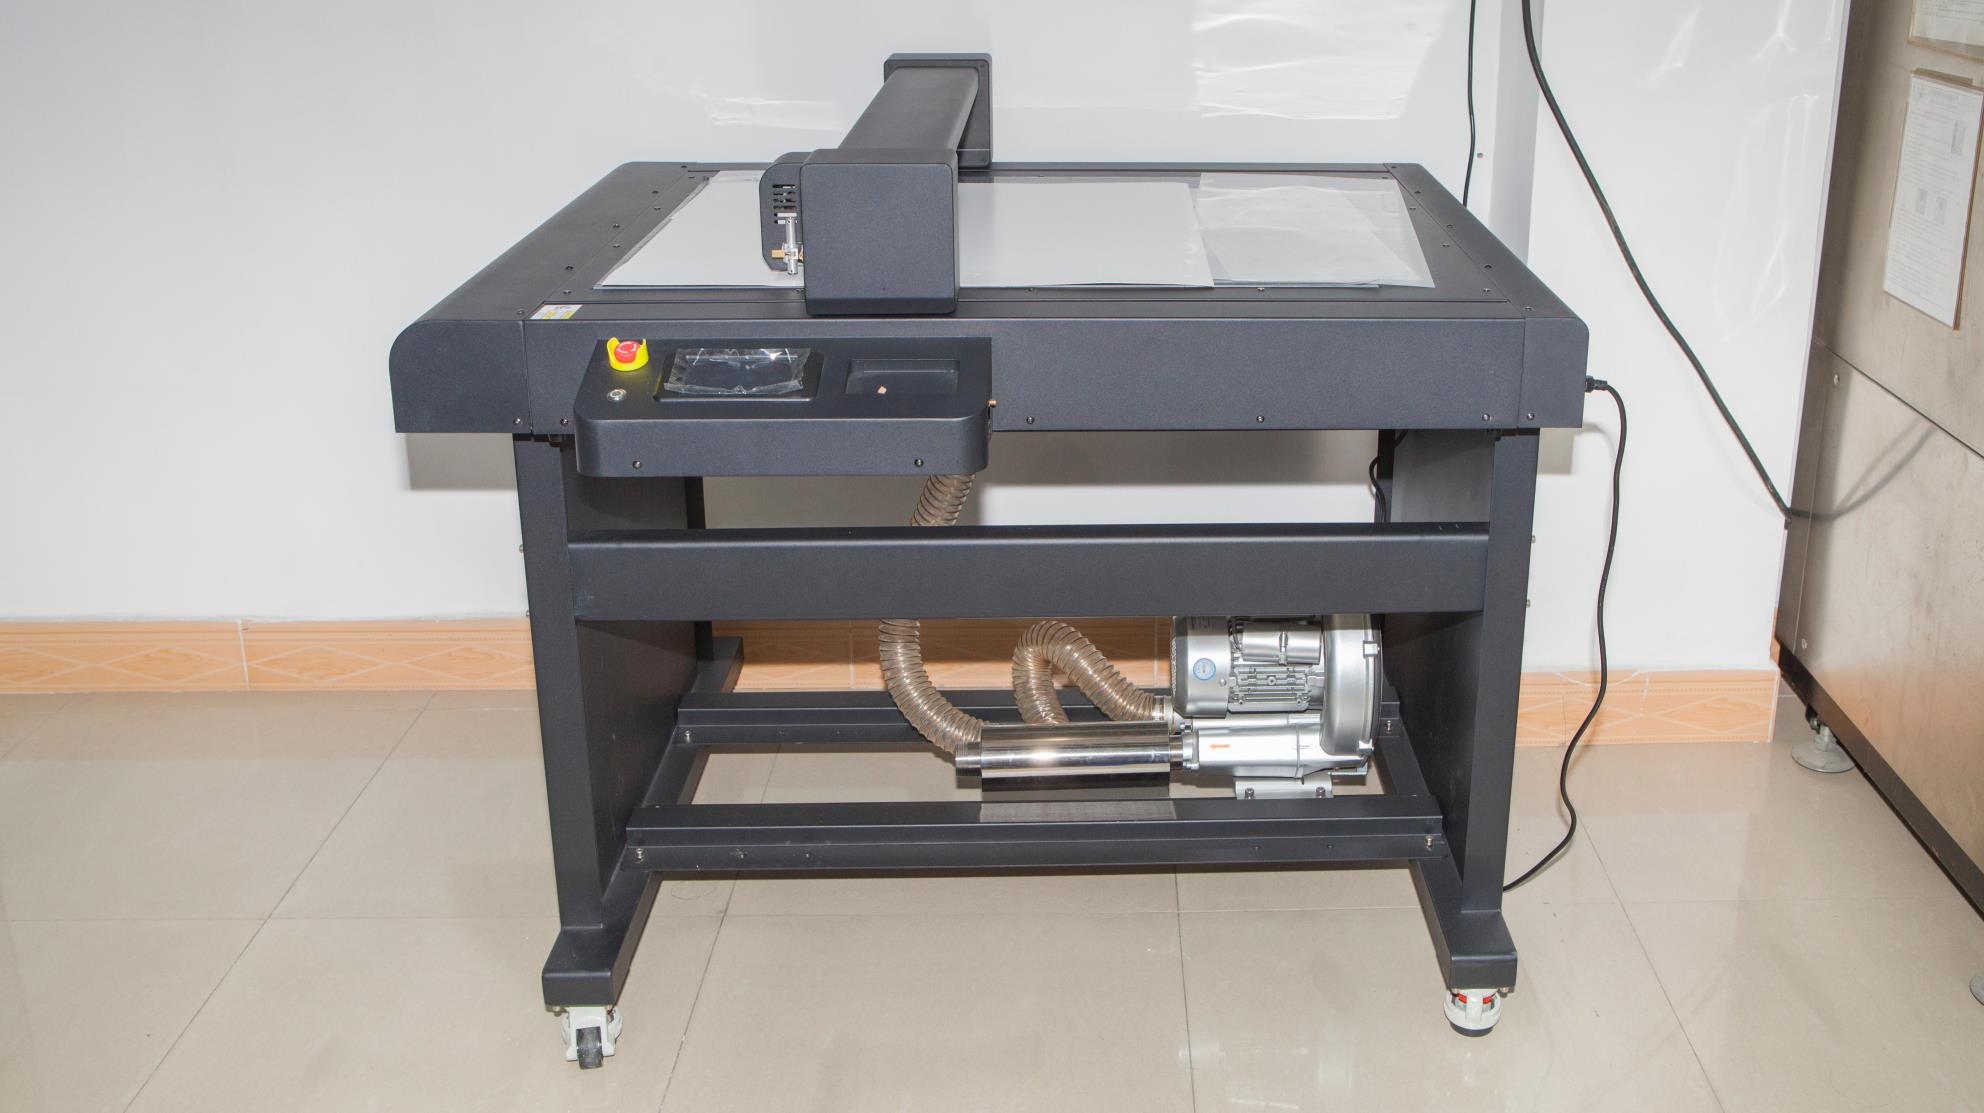
Every membrane switch stack-up built for export to North America is subjected to rigorous qualification across our 9+ proprietary reliability stations.
Pneumatic cycling probes cycle metal dome keys through 1,000,000 to 5,000,000 actuations at calibrated angles, constantly monitoring contact bounce and snap degradation.
Automated force-displacement dynamometers graph actuation curves to ensure tactile ratios fall consistently between 45%–60%, giving every key a satisfying, uniform feel.
Our environmental chambers subject finished assemblies to thermal stress tests (-40°C to +85°C) and 95% relative humidity for 240 hours to guarantee adhesive cohesion and tail seal integrity.
Rotary crockmeters run repeated mechanical abrasion cycles utilizing isopropyl alcohol, acetone, and synthetic perspiration to verify second-surface ink permanence.
Calibrated electronic pull testers measure tail bonding force and spacer-to-substrate peel strength in accordance with ASTM D903 standards.
Xenon arc exposure verifies that our polycarbonate and polyester window formulations retain pristine optical transparency (>92%) without yellowing or haze under prolonged sun exposure.
Real-world technical, logistical, and commercial answers for purchasing managers, electrical engineers, and contract manufacturing specialists.