Engineered Interface Systems for Demanding Field Deployments
Explore precision-fabricated graphic overlays, tactile dome matrices, and conductive elastomer assemblies optimized for rapid integration and harsh-duty cycles.
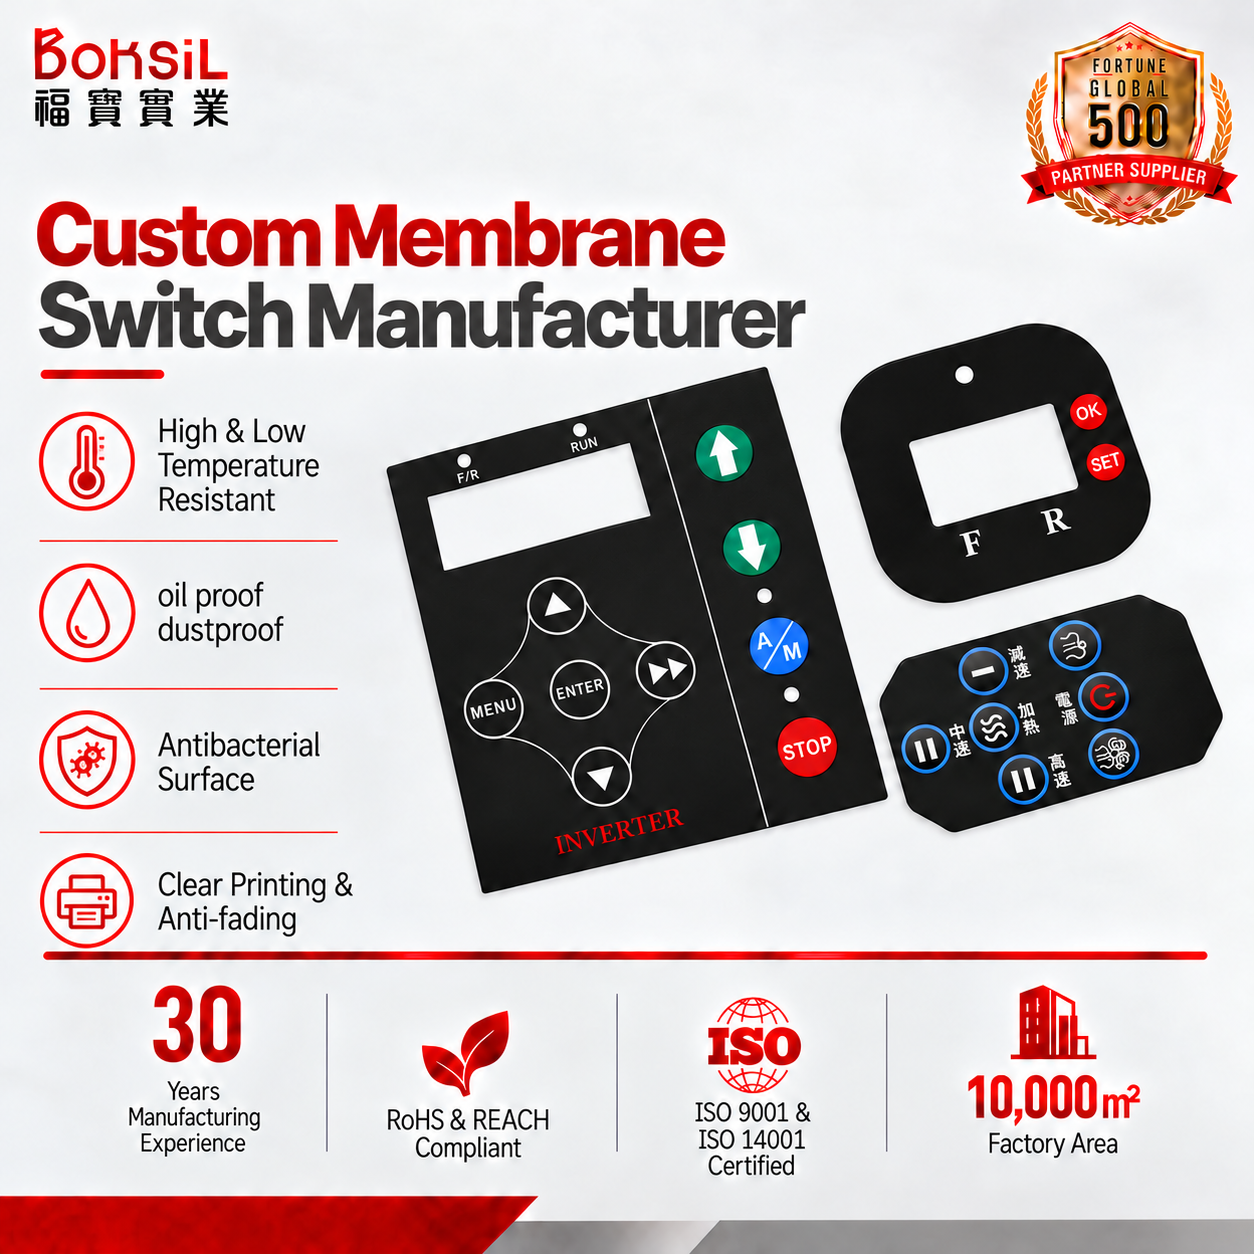
Front Control Electronic Panel Polycarbonate Overlay
Sub-surface screen-printed Autotype polyester/polycarbonate overlays offering high chemical resistance and customized selective texturing.
Product Details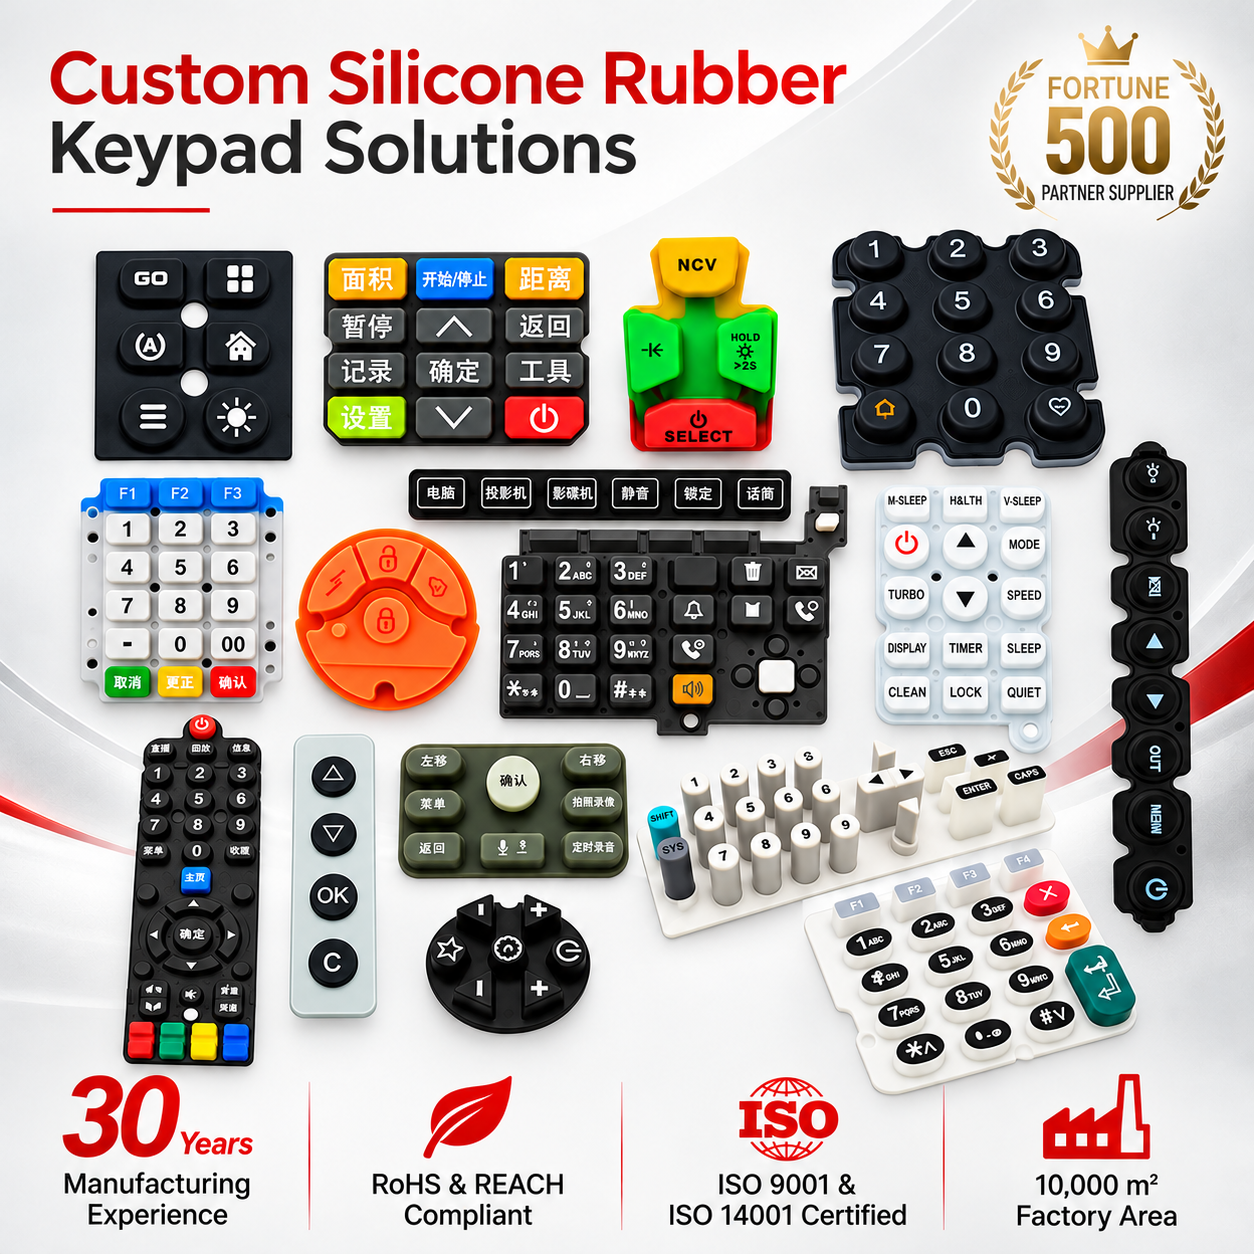
Conductive Silicone Rubber PTT Push-Button Keypads
Compression-molded multi-color elastomer keypads featuring low contact resistance carbon pills and laser-etched backlight legends.
Product Details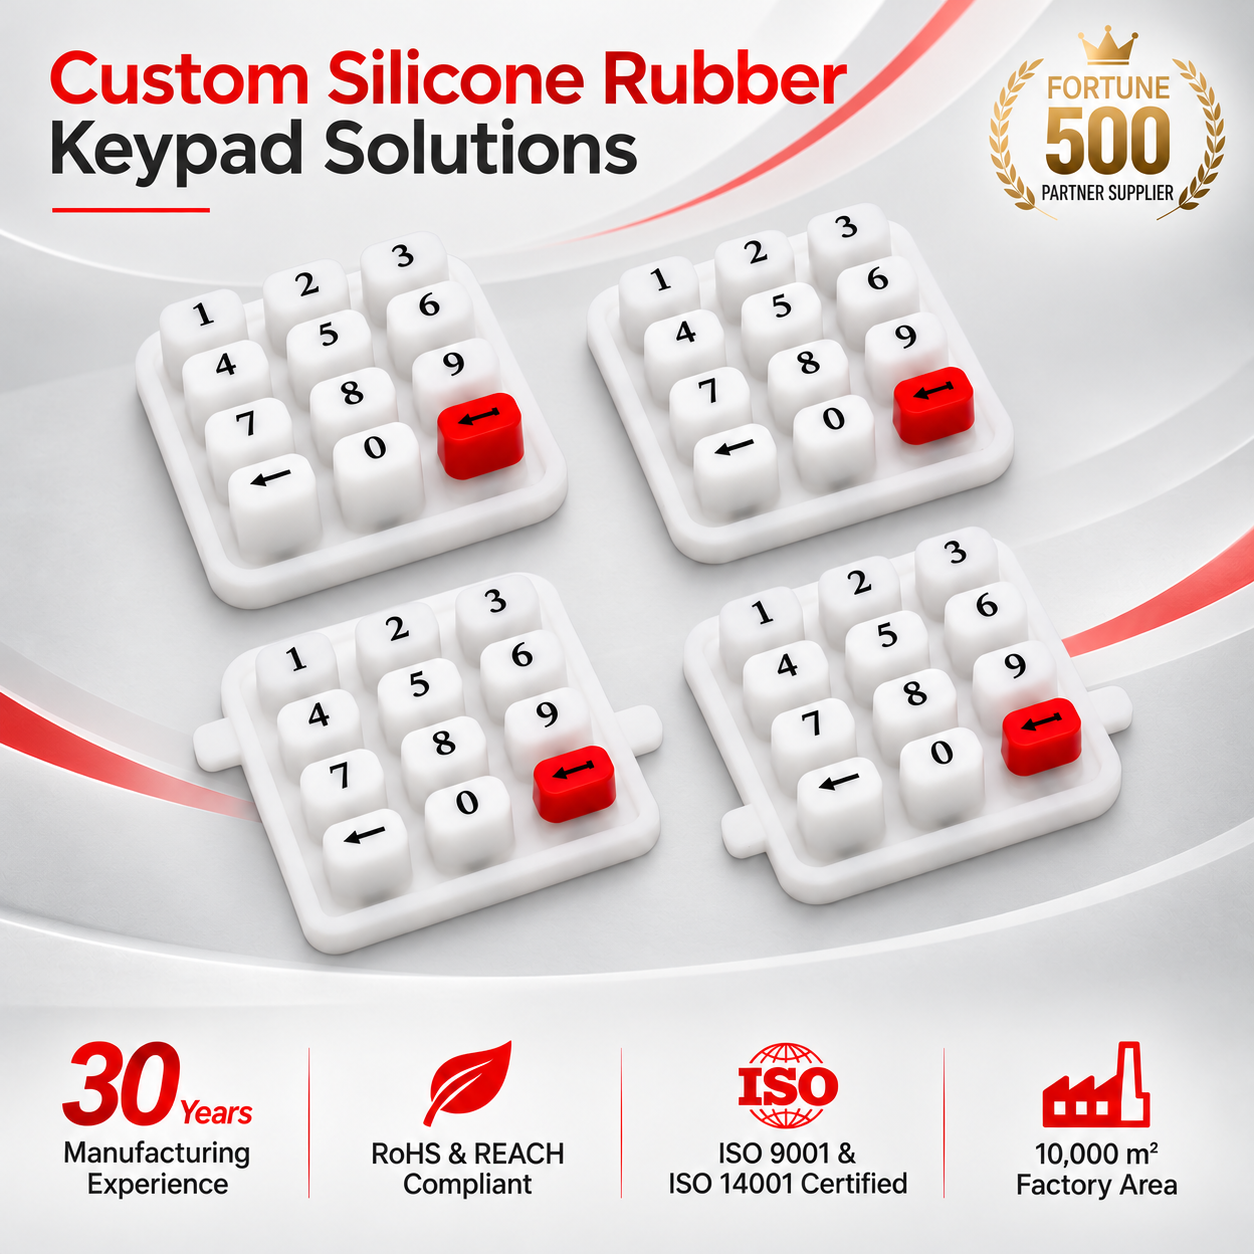
Waterproof Epoxy Coated Silicone Rubber Keypad
Low-profile design with domed epoxy encapsulation offering exceptional wear resistance, smooth tactile travel, and complete IP67 seal integrity.
Product Details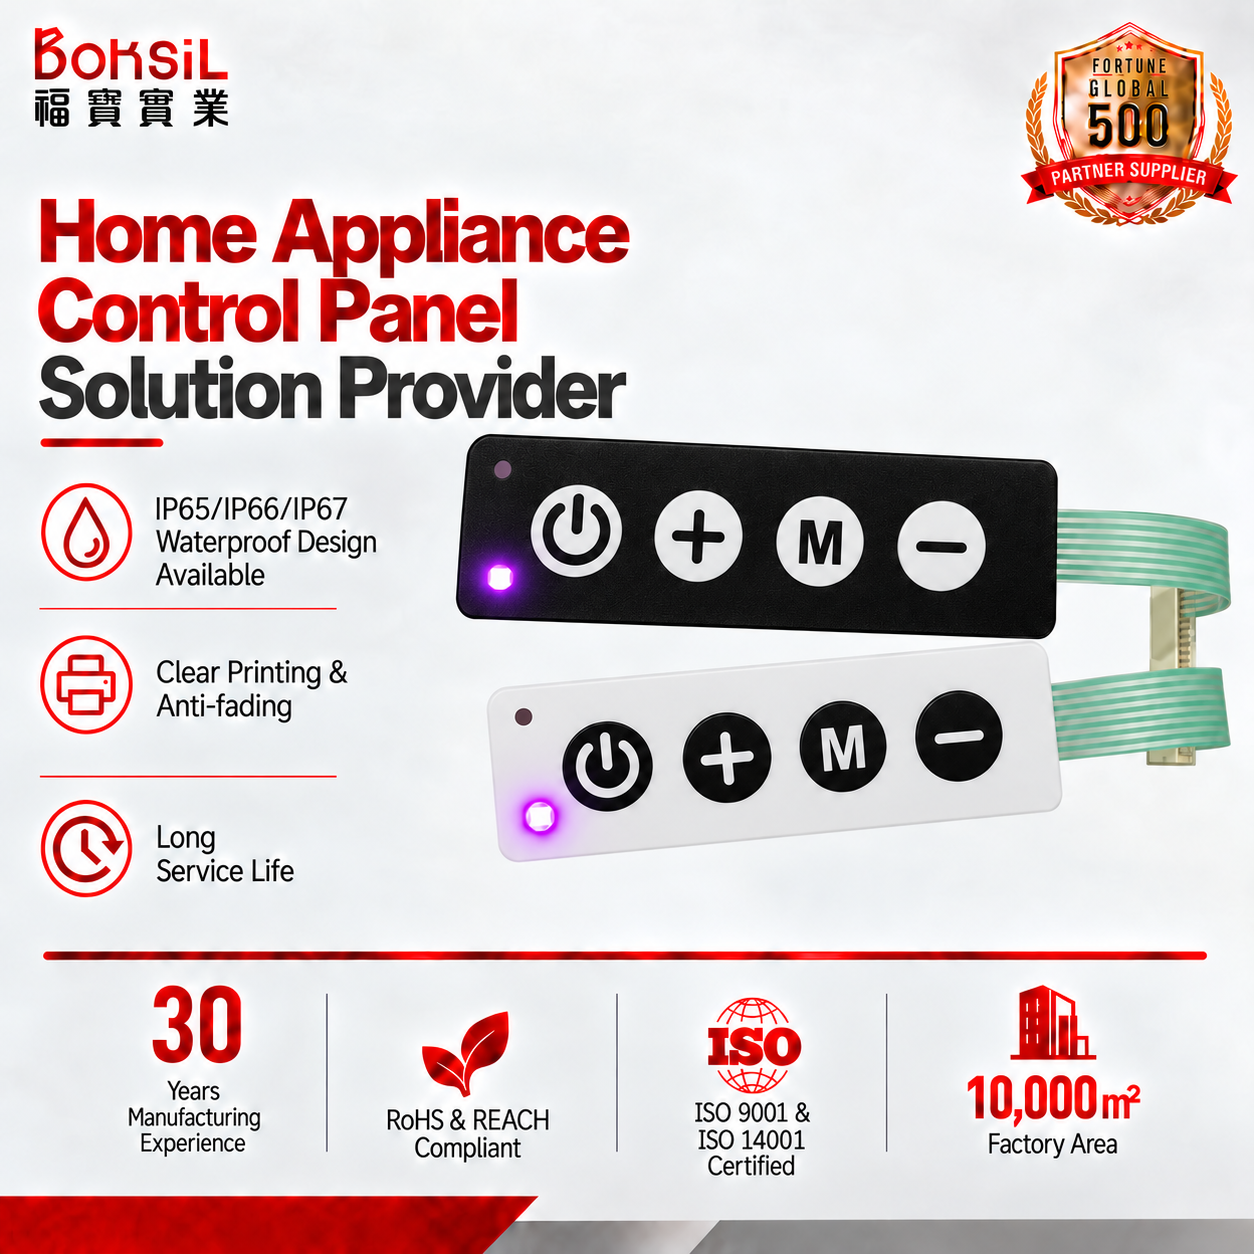
4-Button LED Embedded Tactile Membrane Switch
Integrated surface-mount micro-LEDs and precision snap metal domes providing crisp feedback and status verification for smart instrumentation.
Product Details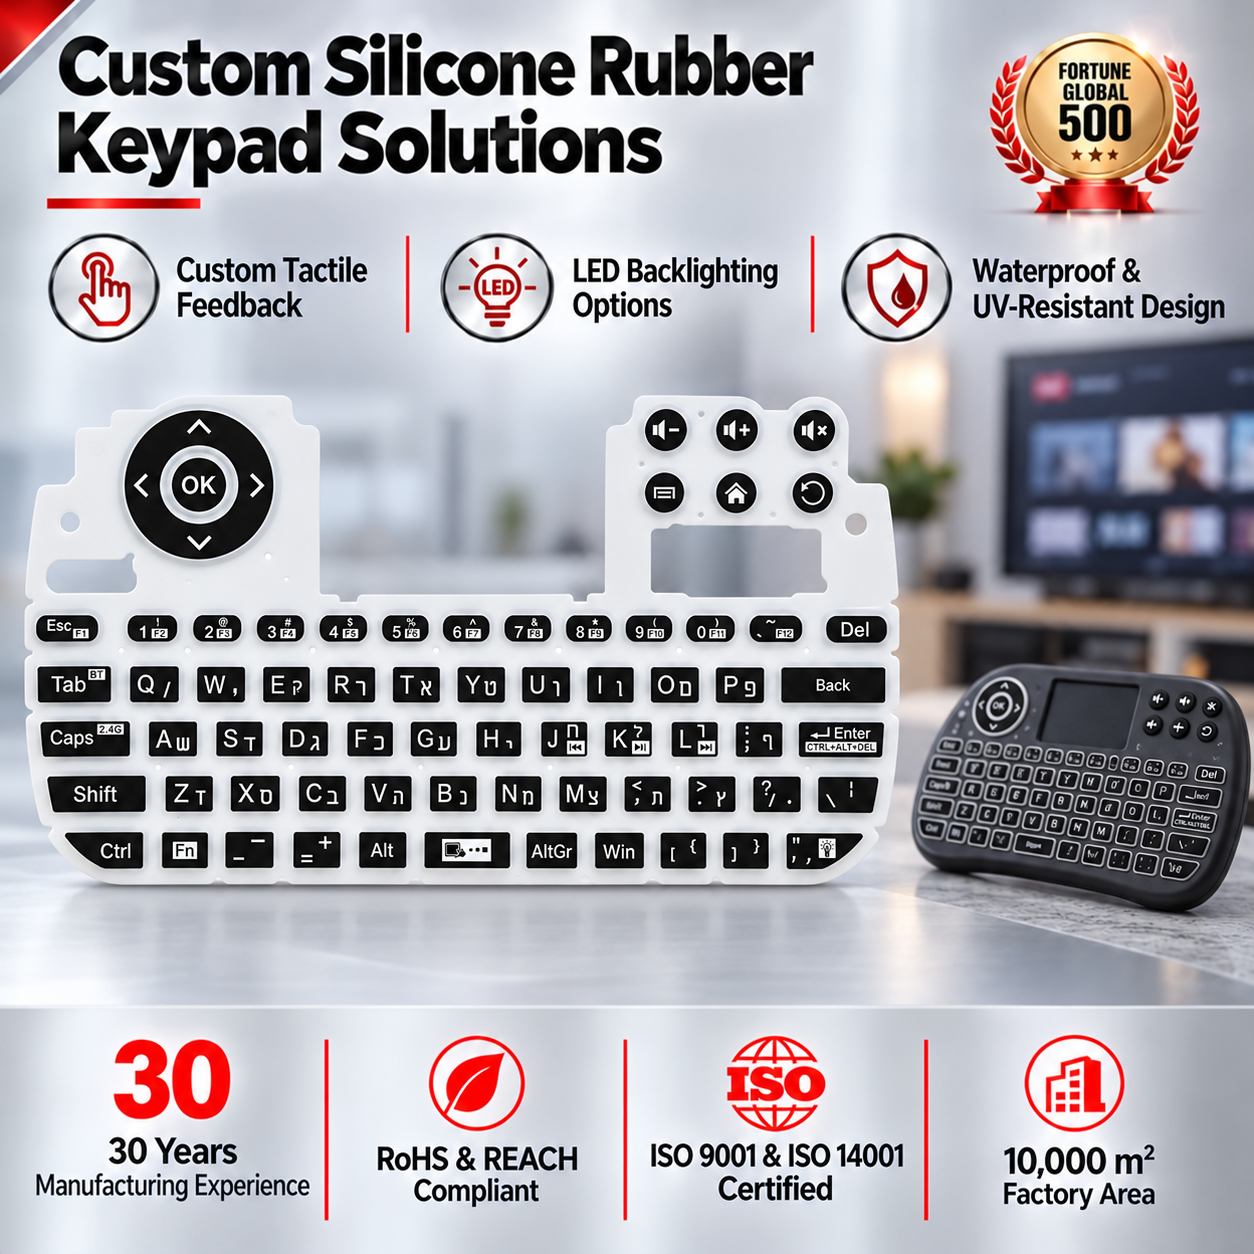
Mini Wireless QWERTY Soft-Touch Elastomer Keypad
High-density custom hotkey button matrix with polyurethane spray coating, engineered for rugged field handhelds and mobile telemetry remotes.
Product Details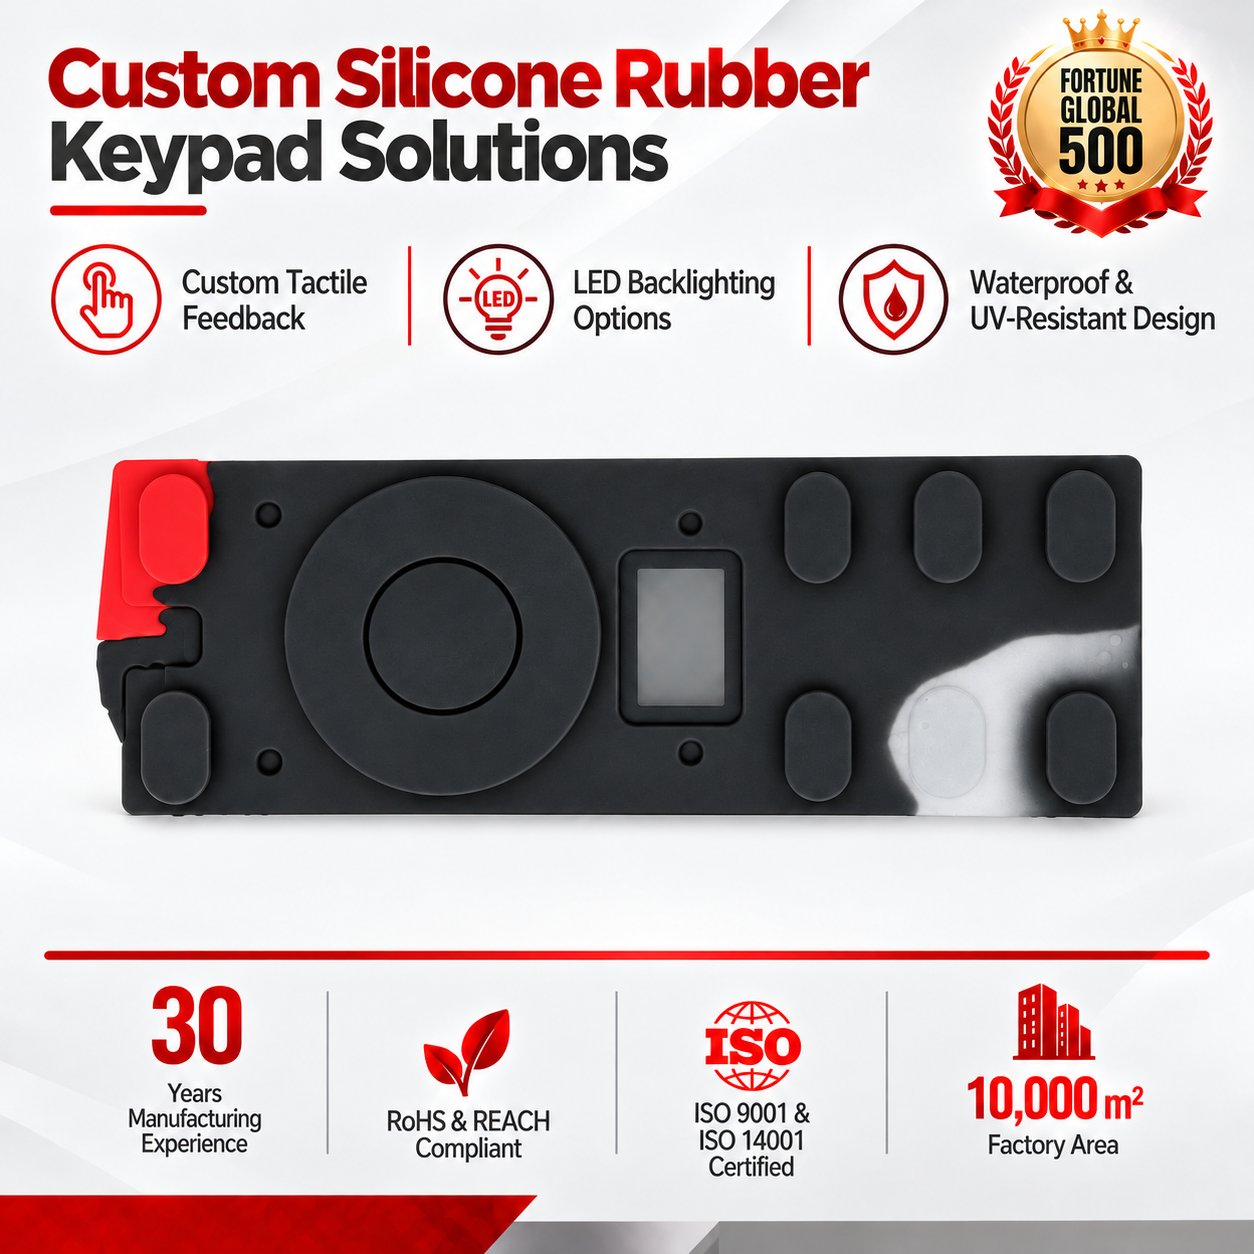
Industrial Embossed Circular Button Keypad Panel
Heavy-duty dual-hardness silicone membrane panel with raised positive perimeter stops, suited for harsh Australian processing facilities.
Product Details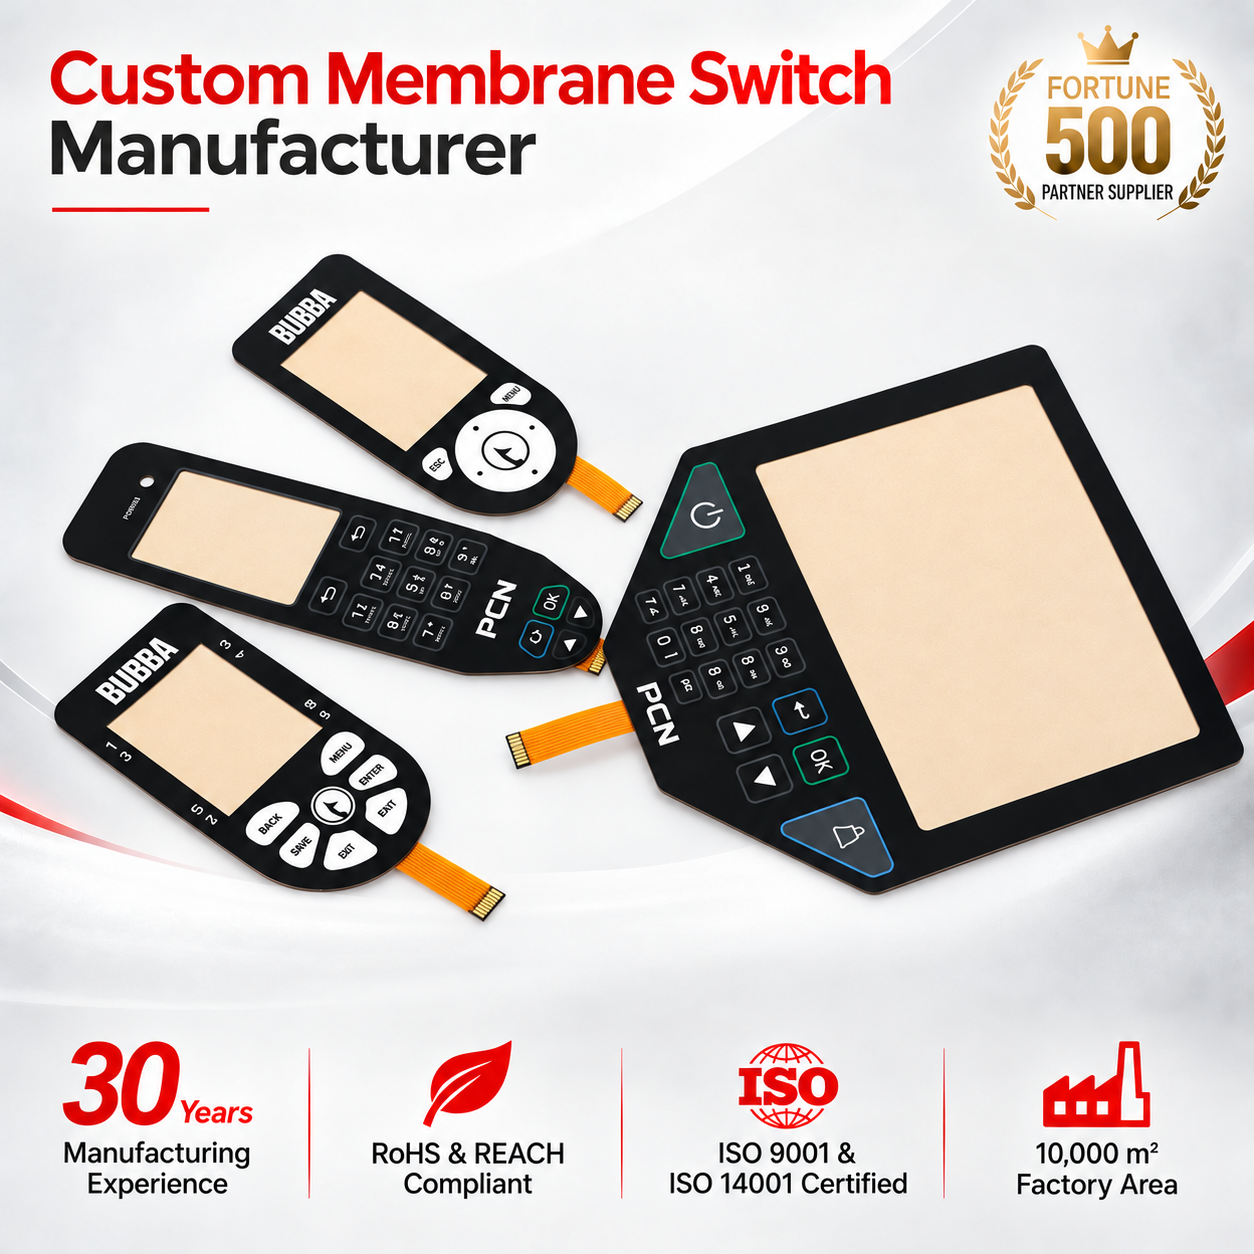
3M Adhesive Tactile Metal Dome Graphic Overlay
Engineered with genuine 3M 467MP/468MP high-tack acrylic adhesives and stainless alloy domes offering over 1,000,000 actuation cycles.
Product Details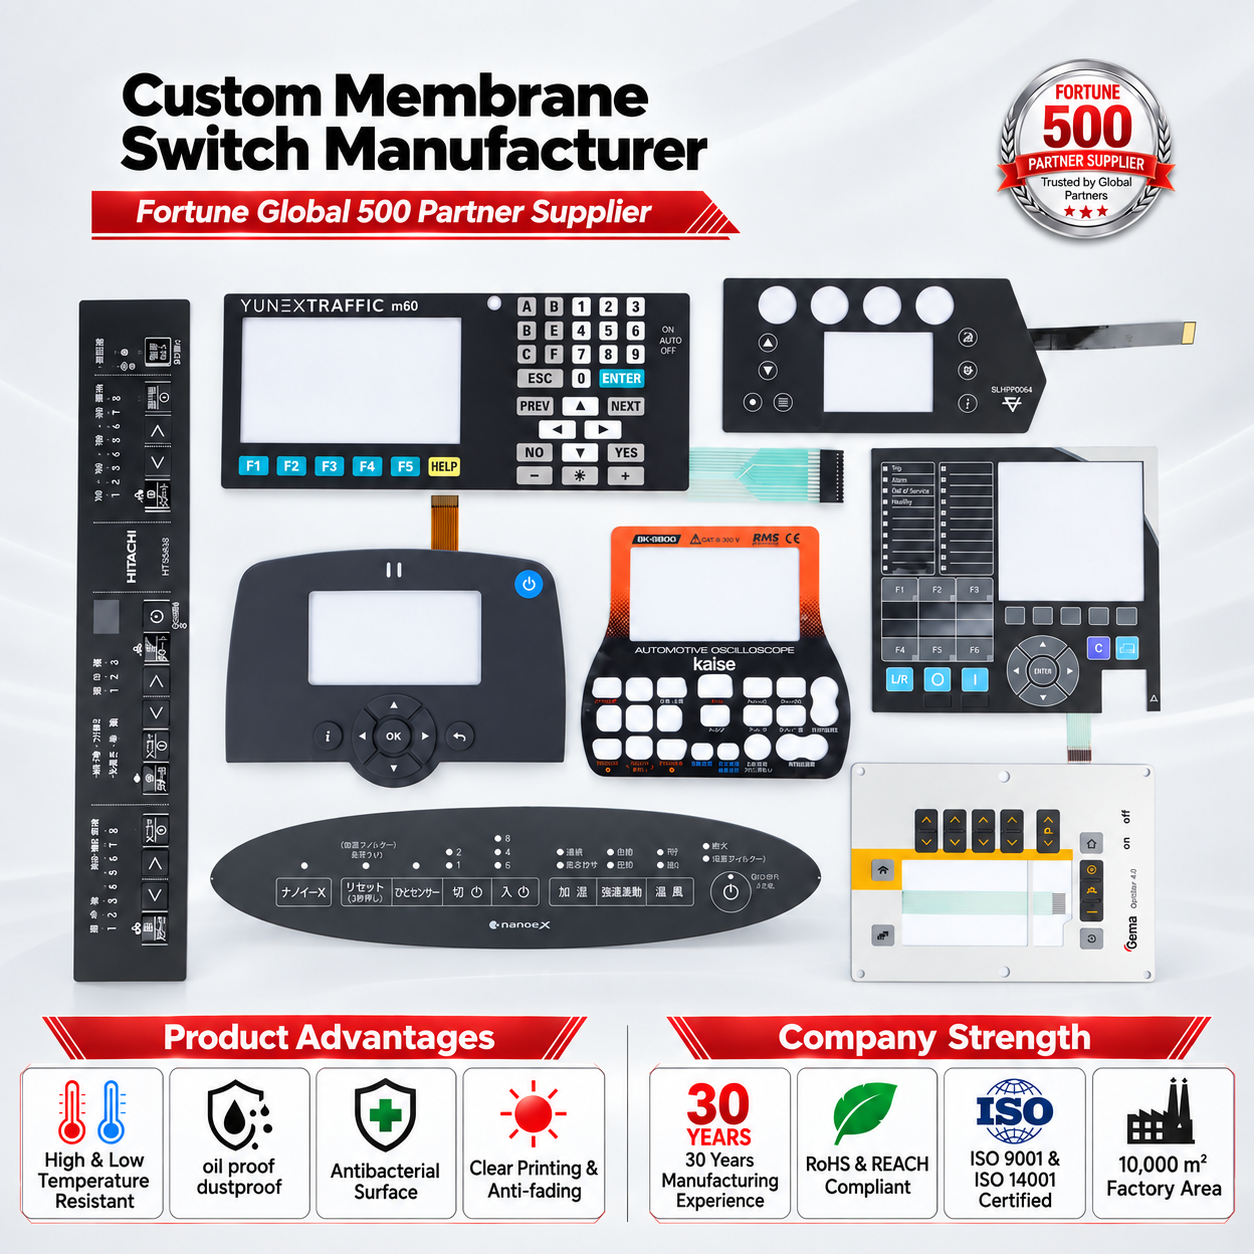
Waterproof FPC Circuit Medical Membrane Touch Panel
Flexible Polyimide Copper (FPC) core with dense pitch ZIF terminations, antimicrobial surface coats, and complete washdown protection.
Product DetailsApplication Scenarios Across Key Australian Sectors
Australia's geographical expanse and heavy industrial heritage require user interfaces that withstand solar radiation, salinity, mineral dust, and rigorous hygiene sanitisation.
Mining, Quarrying & Resources
Deployed throughout the Pilbara and Bowen Basin, our sealed membrane front panels endure abrasive iron ore dust, severe mechanical vibration, and continuous desert UV exposure. We supply heavy-gauge, anti-glare polyester facings for surface fleet telematics, drill rigs, and underground extraction switchgear.
Medical & Life Sciences Devices
Supplying biomedical device builders in Victoria and New South Wales with custom clean-room fabricated touch panels. Utilising medical-grade antimicrobial PET substrates that resist harsh hospital disinfectant sprays, hospital-grade bleaches, and continuous wipe-downs without hazing or print loss.
Agriculture, AgTech & Irrigation
Engineered for solar pumps, grain silo telemetry consoles, and automated tractor cabins across regional Queensland and South Australia. Integrated perimeter gaskets prevent liquid ingress from tropical torrential downpours, while wide-temperature adhesives prevent layer peeling under 45°C+ summer peaks.
Marine, Offshore & Coastal Defense
Naval shipboard monitoring panels, harbor cranes, and maritime navigation systems operating in corrosive, salt-laden coastal conditions. Our multi-layer IP67 and IP68 constructions employ solid perimeter RTV adhesive rings and corrosion-proof gold-plated metal domes to stop electrolytic corrosion.
EV Chargers & Outdoor Kiosks
Fuel dispensers, public smart meters, and municipal EV charging stations situated in direct Australian sunlight. Engineered with specialized UV-stabilised hard-coated film that guarantees over five years of exterior exposure without graphic yellowing, brittleness, or optical degradation.
Food Processing & Cold Storage
Facilities across regional Australia requiring continuous IP66/IP69K high-pressure washdowns and sub-zero functionality down to -40°C. Our silicone elastomer keypads and closed-cell spacer systems withstand thermal shocks without inner condensation or tactile failure.
Emerging HMI Engineering Trends in Australia
The transition from mechanical pushbutton banks to intelligent, sealed human-machine interfaces is accelerating across ANZ original equipment manufacturers (OEMs).
1. Adoption of Hybrid Capacitive & Tactile Inputs
Industrial designers are shifting from traditional standalone membranes to hybrid control panels. Designers incorporate capacitive touch sensing zones alongside positive metal dome snap keys for critical emergency-stop and high-priority input routines, ensuring glove-friendly operation in dirty workshop environments.
2. High-Durability Backlighting (LGF & Side-Emitting LEDs)
Outdoor readability during blinding Australian midday sun and crisp illumination at night has pushed demand towards ultra-thin Light Guide Film (LGF) assemblies. LGF distributes uniform illumination from minimal SMD LEDs, reducing overall power draw in off-grid solar-powered remote stations.
3. Rigorous EMI/RFI Shielding Standards
With strict Australian Communications and Media Authority (ACMA) RCM compliance, machinery builders must suppress electromagnetic interference. We print high-density conductive grid planes or laminate aluminum foil layers within the overlay stack-up to prevent signal crosstalk.
Enterprise Advantages for Australian OEM Procurement
Operating a vertically integrated 10,000㎡ facility verified by Intertek, Dongguan AXRU Electronics Co., Ltd. eliminates middleman markups and technical misalignments.
In-House DFM Engineering
Direct access to our 121-person engineering staff. Full design-for-manufacturability reviews covering circuit routing, connector pitch, venting channels, and dome travel tolerances.
Intertek Verified Quality
Factory-direct transparency. On-site certified quality management systems adhering strictly to ISO 9001:2015 frameworks with traceable raw material batches.
Comprehensive Test Rig Suite
In-house reliability validation: Key life testers (up to 5M actuations), computerized force-displacement testers, thermal cycling chambers, and UV weathering testers.
Fortune 500 Supply Proven
Over a decade of direct tier-one export experience. Serving leading brand names across mining instrumentation, consumer appliances, and medical monitoring.
Agile MOQs & Rapid Samples
Supporting prototyping, NPI runs, and mid-volume industrial batches from 100 units, backed by dedicated sample line tooling with 5-7 business day prototype dispatch.
Frequently Asked Questions by Australian Engineers & Buyers
Key technical, logistic, and material considerations for Australian manufacturers sourcing custom front panel overlays and membrane switches from our facility.