Precision-Fabricated Keypads & Circuit Assemblies
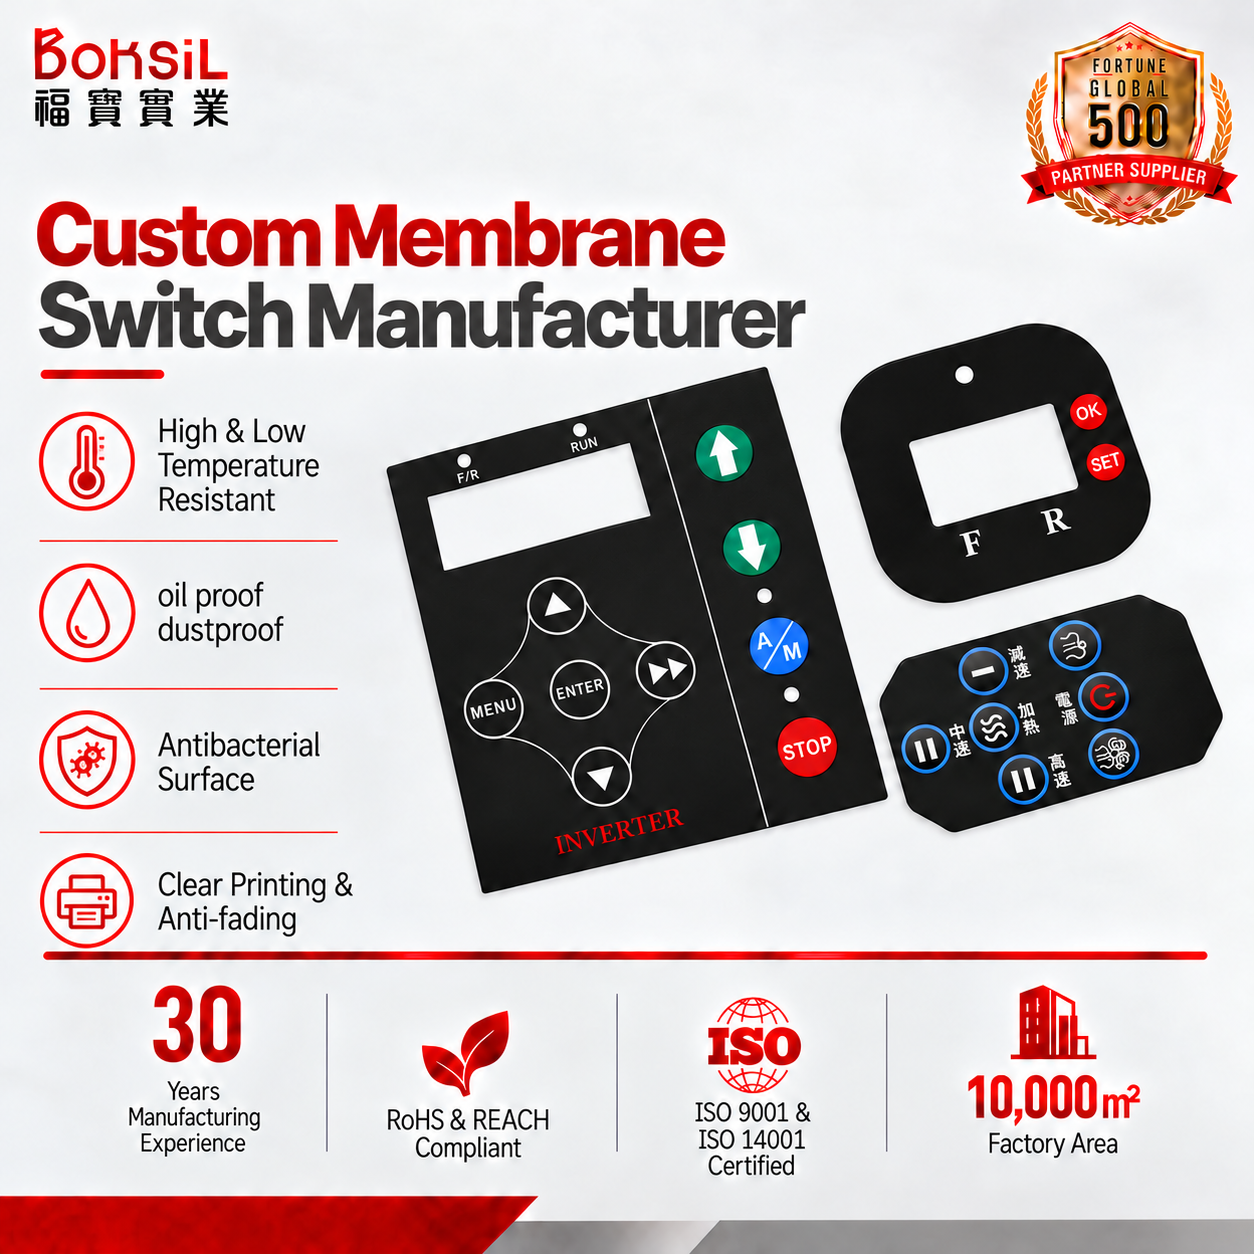
Direct factory production with 100% optical and electrical testing. Engineered to endure Canadian climate extremes and harsh industrial washdowns.
Regional Integration
HMI Engineering for the Greater Toronto Area Manufacturing Hub
The Greater Toronto Area (GTA)—spanning North York, Mississauga, Markham, and Vaughan—represents Canada’s premier nexus for precision hardware, biomedical instruments, and specialized automation. Sourcing high-performance membrane circuits requires matching design tolerances to rigorous sub-zero environments, chemical exposures, and electromagnetic mandates.
Medical & Life Sciences
Toronto's Discovery District and regional diagnostic laboratories demand human-machine interfaces that comply with cleanroom hygiene protocols. Our antimicrobial PET graphic overlays, combined with chemically inert silicone rubber elastomer keypads, offer impermeable IP67 barrier resistance against bleach, isopropyl alcohol, and hospital-grade germicides without graphic degradation or optical haze.
Robotics & Automation
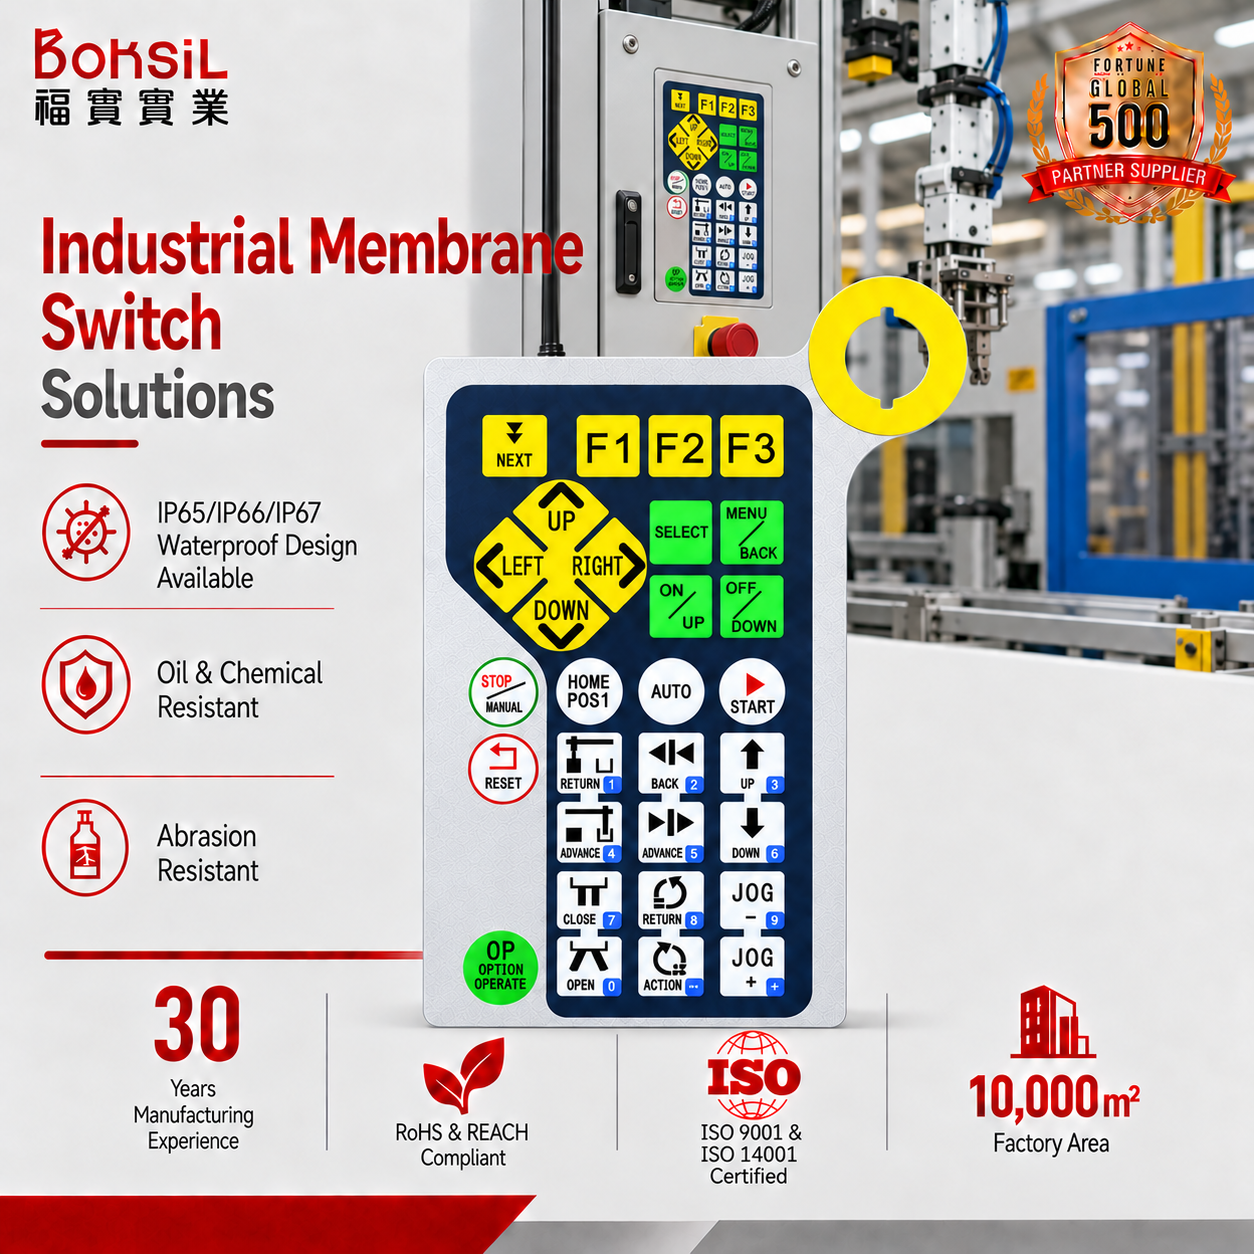
From automated packaging facilities in Brampton to automotive assembly equipment in Oshawa, industrial control cabinets require reliable inputs. We engineer metal dome tactile membrane panels tested up to 5,000,000 actuations. Built with rugged polycarbonate sub-surface printing, these systems resist particulate egress, vibration harmonics, and heavy hydraulic washdowns.
Outdoor & Cold Climate Infrastructure
Southern Ontario’s severe seasonal thermal differentials—from -30°C winter conditions to humid summer heat—challenge traditional flexible printed electronic switches. We engineer specialized circuit stack-ups utilizing optical-grade 3M adhesive layers (such as 3M 467MP / 468MP) and cold-stable conductive silver-on-polyester inks that prevent interlayer delamination, micro-cracking, and electrical opens.
Technical Advancements
Emerging HMI Engineering Trends Across Ontario OEM Sectors
Transitioning from standard mechanical switches to intelligent thin-film interfaces requires structural and electrical innovation. We lead three fundamental technological shifts serving advanced Canadian equipment builders.
Capacitive Sensing Integration
Toronto product designers are increasingly converging traditional tactile feedback with capacitive touch controls under continuous acrylic or tempered-glass front fascias. Our hybrid manufacturing lines integrate printed capacitive electrode tracks with integrated backlighting and In-Mold Decoration (IMD), establishing seamless, IP68 flush interfaces suitable for food-contact machinery and medical diagnostic stations.
EMC/ESD Shielding for Heavy Industry
With modern plant floors deploying high-frequency motor drives and wireless IoT telemetry, electrical noise immunity is mandatory. We laminate continuous copper grid or printed carbon shielding planes directly within the membrane switch sandwich, shunting static discharges up to 15kV away from sensitive host logic boards, maintaining full CSA and CE EMC compliance.
Precision Backlighting & Dead-Front Inks
Modern HMIs rely on selective information disclosure. Utilizing ultra-thin Light Guide Film (LGF), embedded micro SMD LEDs, and calibrated translucent dead-front screen inks, switch legends remain completely invisible until energized. This reduces operator visual fatigue in low-light industrial cabs and commercial transportation systems across Canadian transit arteries.
Intertek-Verified Facility
Direct Factory Manufacturing: Dongguan AXRU Electronics Co., Ltd.
Operating a dedicated 10,000㎡ industrial complex with 121 skilled technicians, AXRU eliminates non-manufacturing middlemen. We engineer our tooling, formulate circuit traces, print multi-pass graphics, and conduct comprehensive reliability testing under one verified management system.
- 100% Automated Electrical Continuity Check
- Force vs. Displacement Curve Analysis
- Programmable Climatic Simulation Chambers
- Automated Flatbed Precision Die-Cutting
- Mechanical Key Cycle Endurance Rigs
- Taber Abrasion & Solvent Decolorization Testing
Procurement Intelligence
Frequently Asked Questions for Toronto & Canadian Buyers
Direct answers covering cross-border logistics, design optimization, material selections, and quality compliance for Canadian hardware engineering teams.
What design documentation is required for an engineering quote?
To produce an authoritative Design for Manufacturability (DFM) review and accurate quotation, please provide your 2D CAD mechanical outline (in DXF, DWG, or vector PDF format), graphic overlay vector art (in Adobe Illustrator with designated Pantone PMS codes), circuit matrix schematic, tail exit location, and termination pitch (commonly 1.0mm, 1.27mm, or 2.54mm pitch female Berg/FCI connectors or bare ZIF tails). If an engineering drawing is not yet finalized, our team can reverse-engineer from an existing physical sample.
How do membrane switches perform in sub-zero Canadian winter conditions?
Standard commercial polyester membranes can suffer from brittle fracture and adhesive crystallization when exposed to deep Canadian freezes below -20°C. For sub-zero reliability down to -40°C, we specify premium biaxially oriented polyethylene terephthalate (PET) films, specialized cross-linked acrylic adhesive transfer tapes (e.g., 3M 200MP series), and nickel-plated stainless steel tactile domes rated for consistent snap ratios across extreme thermal transitions.
What are typical prototype and mass-production lead times to Toronto?
Our rapid-prototyping sample cell can deliver first-article functional samples within 7 to 10 business days following DFM approval. Mass production typically requires 15 to 20 working days depending on tooling complexity. Consignments are exported directly to Pearson International Airport (YYZ) or door-to-door across the GTA via expedited air courier (DHL, FedEx, UPS) within 3 to 5 business days, complete with commercial customs documentation.
What are the minimum order quantities (MOQ) for custom tooling?
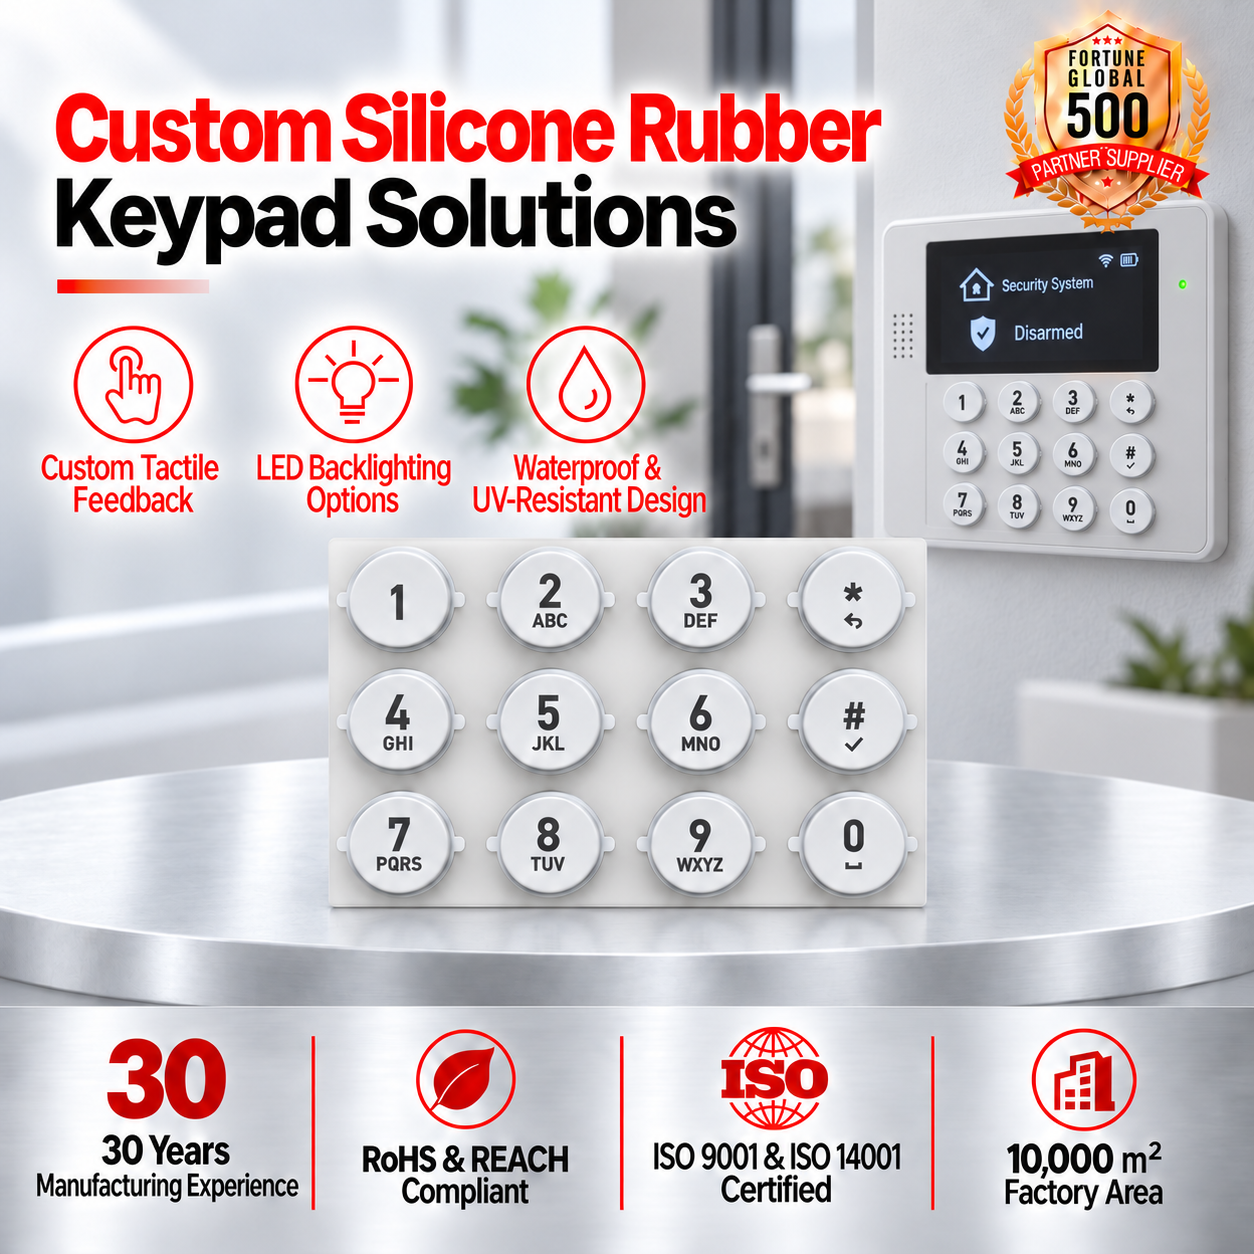
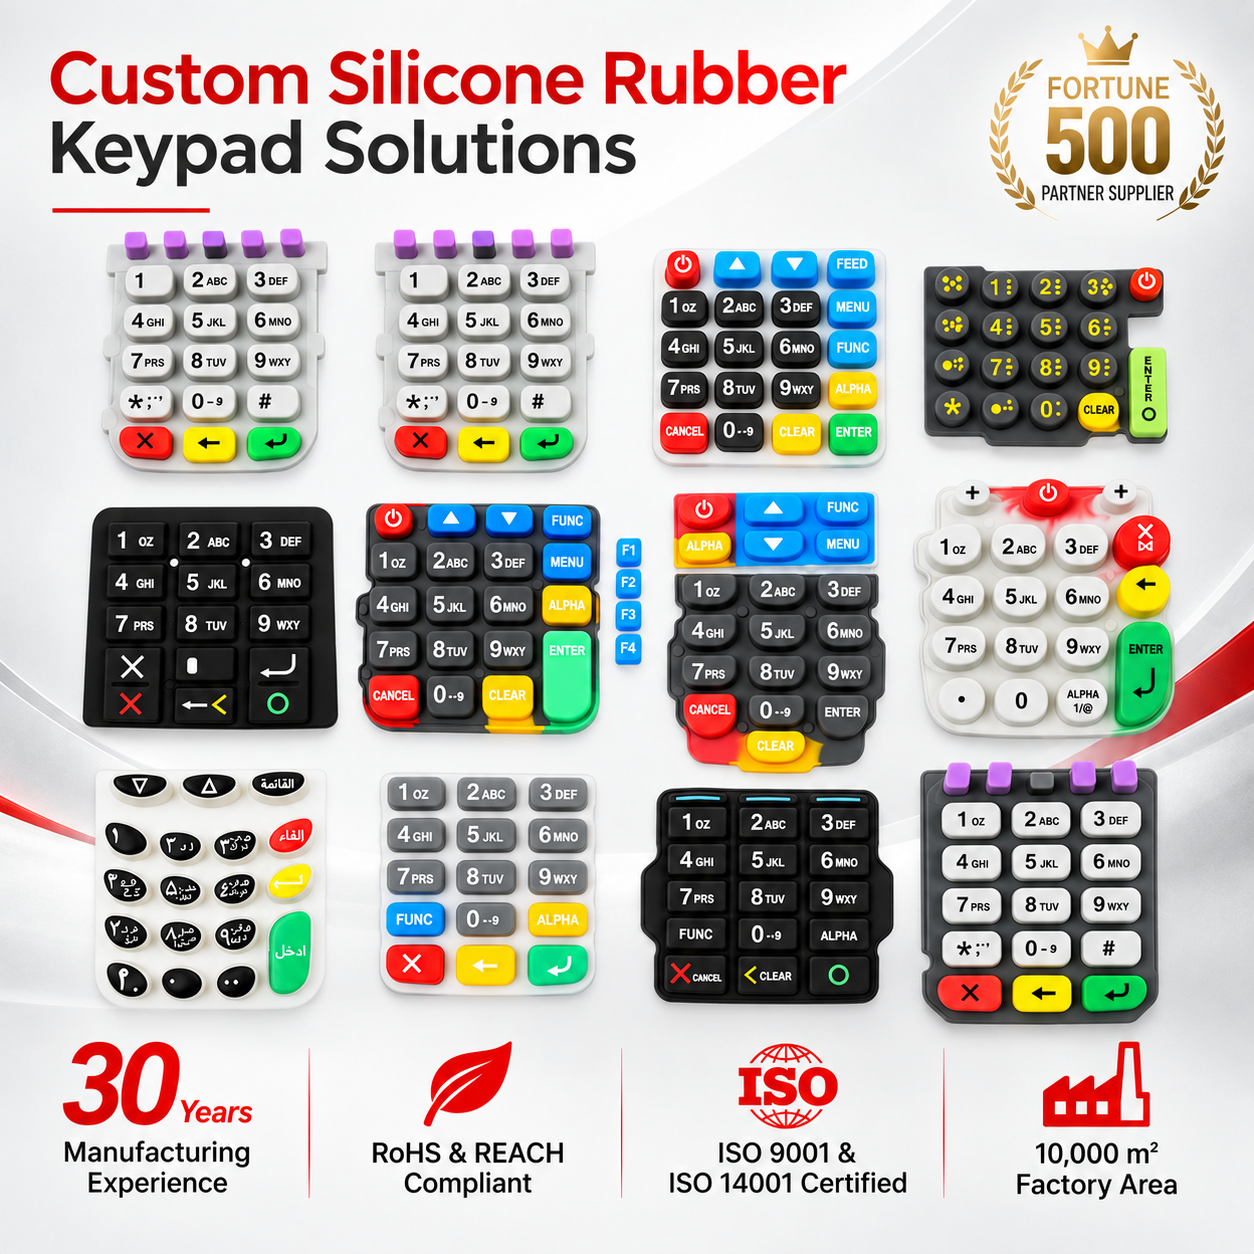
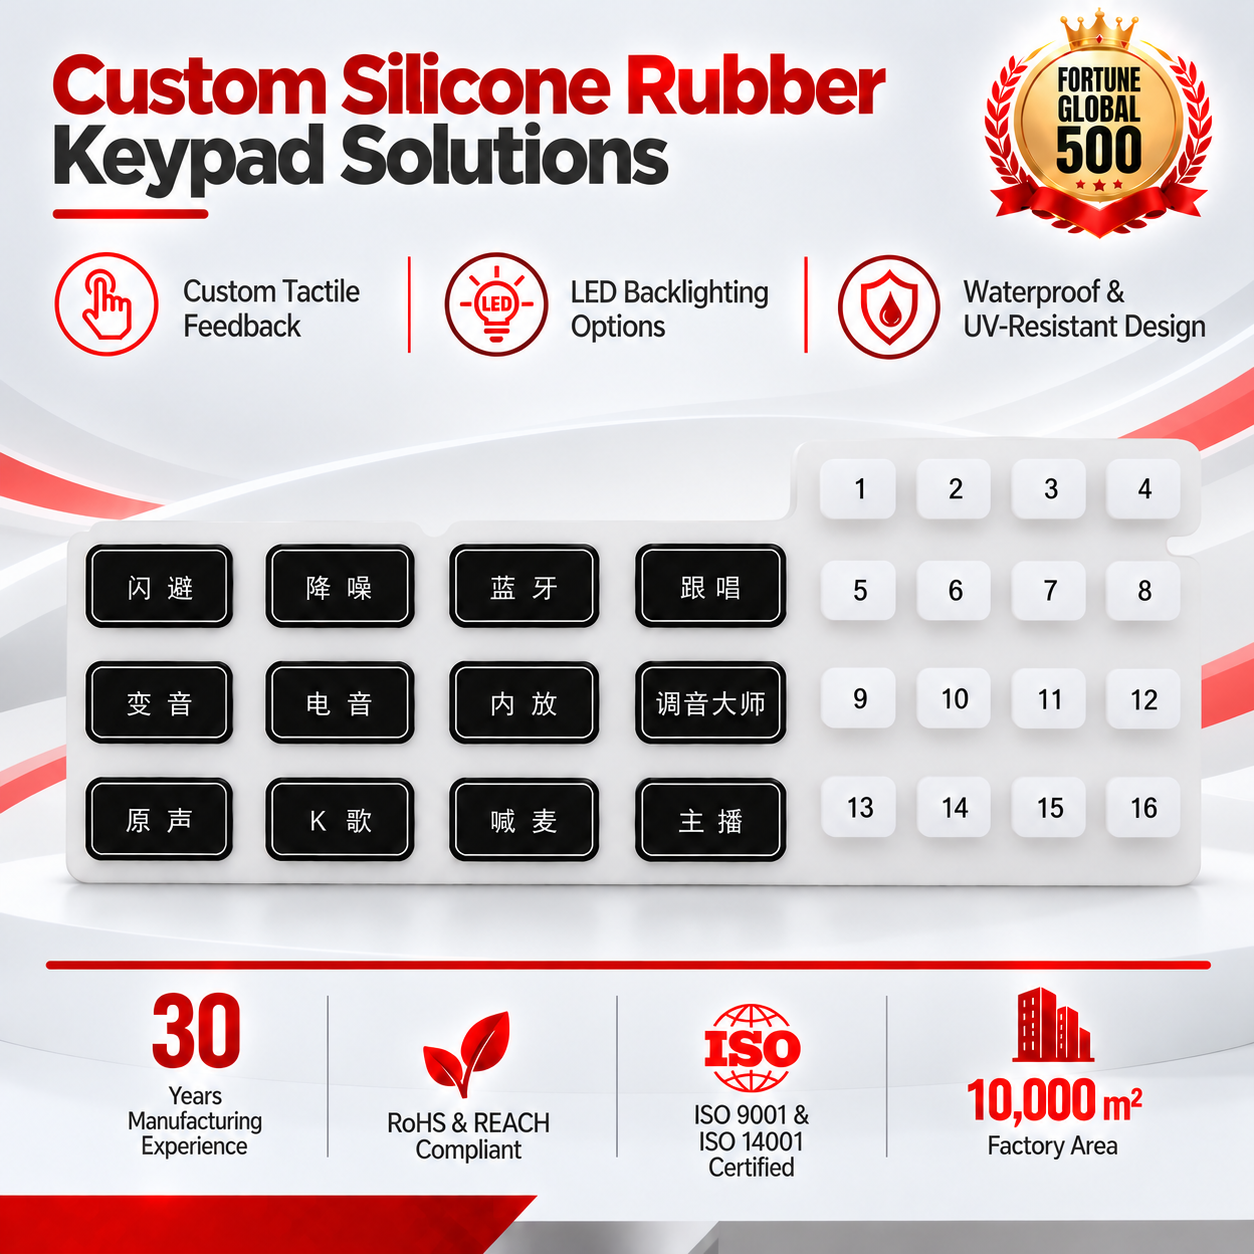
Unlike conventional contract assemblers demanding thousands of units, our baseline production run starts at just 100 units for fully custom membrane switches, graphic overlays, and silicone keypads. This allows early-stage Canadian startups, medical device pilots, and low-volume industrial OEMs to access production tooling and scale on demand.
Can you manufacture membrane switches meeting IP65 to IP67 standards?
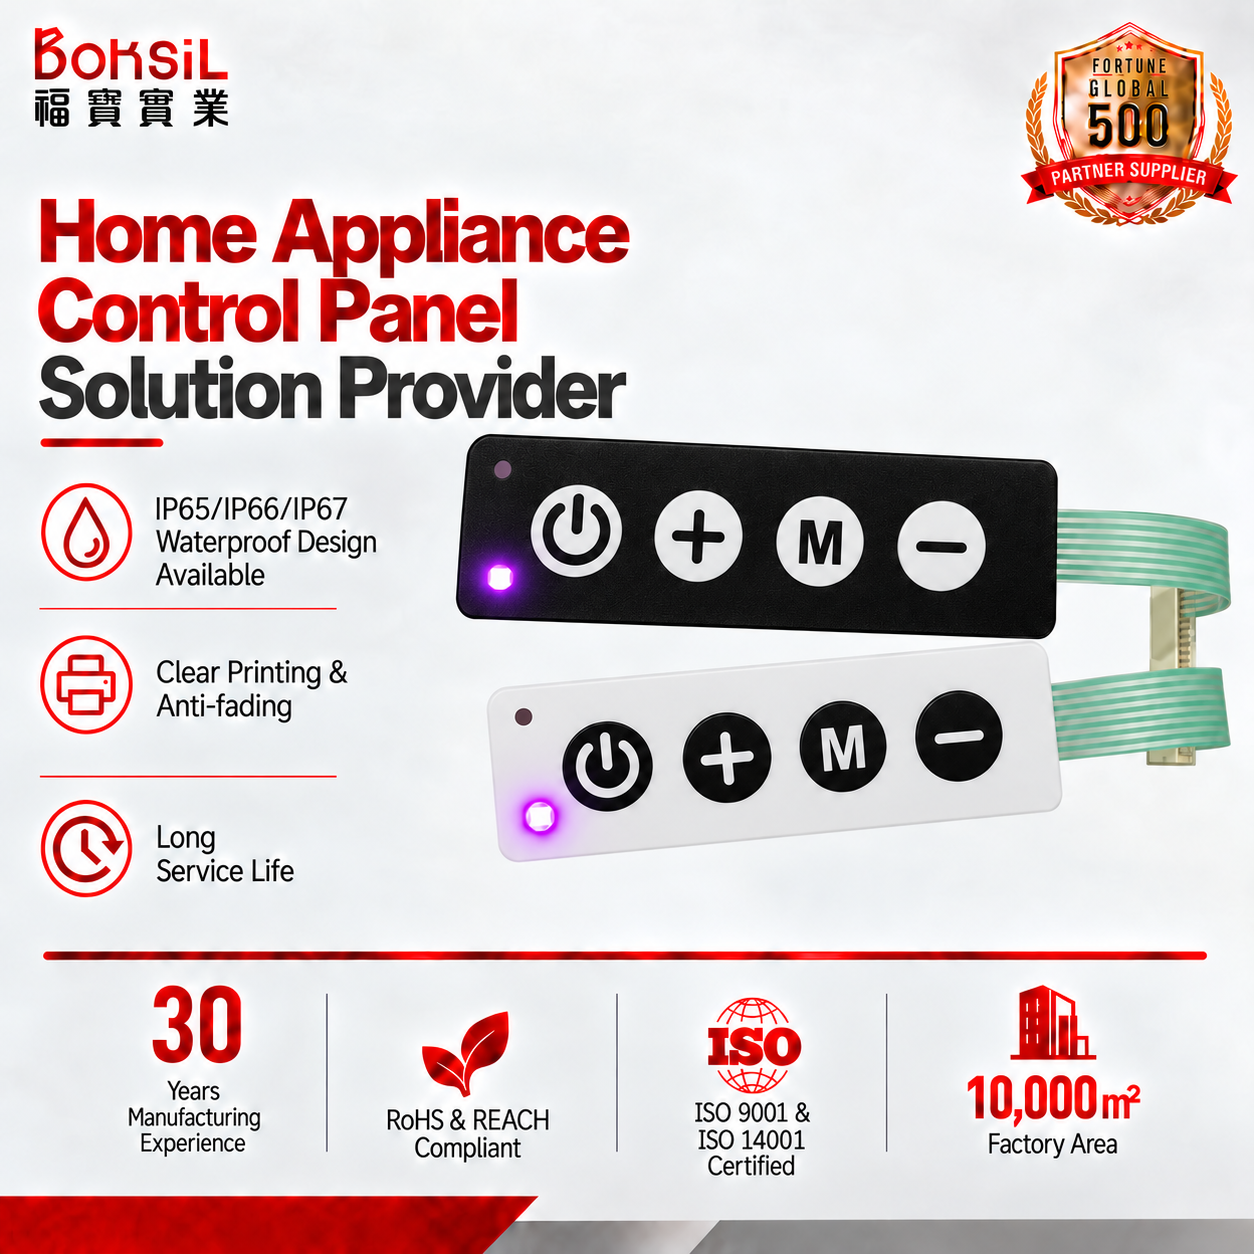
Yes. Environmental sealing is accomplished via an uninterrupted perimeter adhesive gasket that encapsulates both the internal circuit layer and the tail conduit. This perimeter seal isolates the circuit matrix and metal domes from pressurized moisture, airborne contaminants, and corrosive liquids. Assemblies undergo pressure-decay and environmental chamber validation to ensure ingress protection.
How does AXRU assure electrical trace conductivity over high-cycle lifespans?
We print flex traces using silver inks with precise solid contents, followed by controlled infrared curing to prevent solvent entrapment. Trace layouts are engineered to maintain loop resistances below 100 ohms (or lower via copper flex circuit FPC technology). Furthermore, carbon overprinting is applied to switch contact pads to prevent silver migration and galvanic corrosion over millions of actuations.