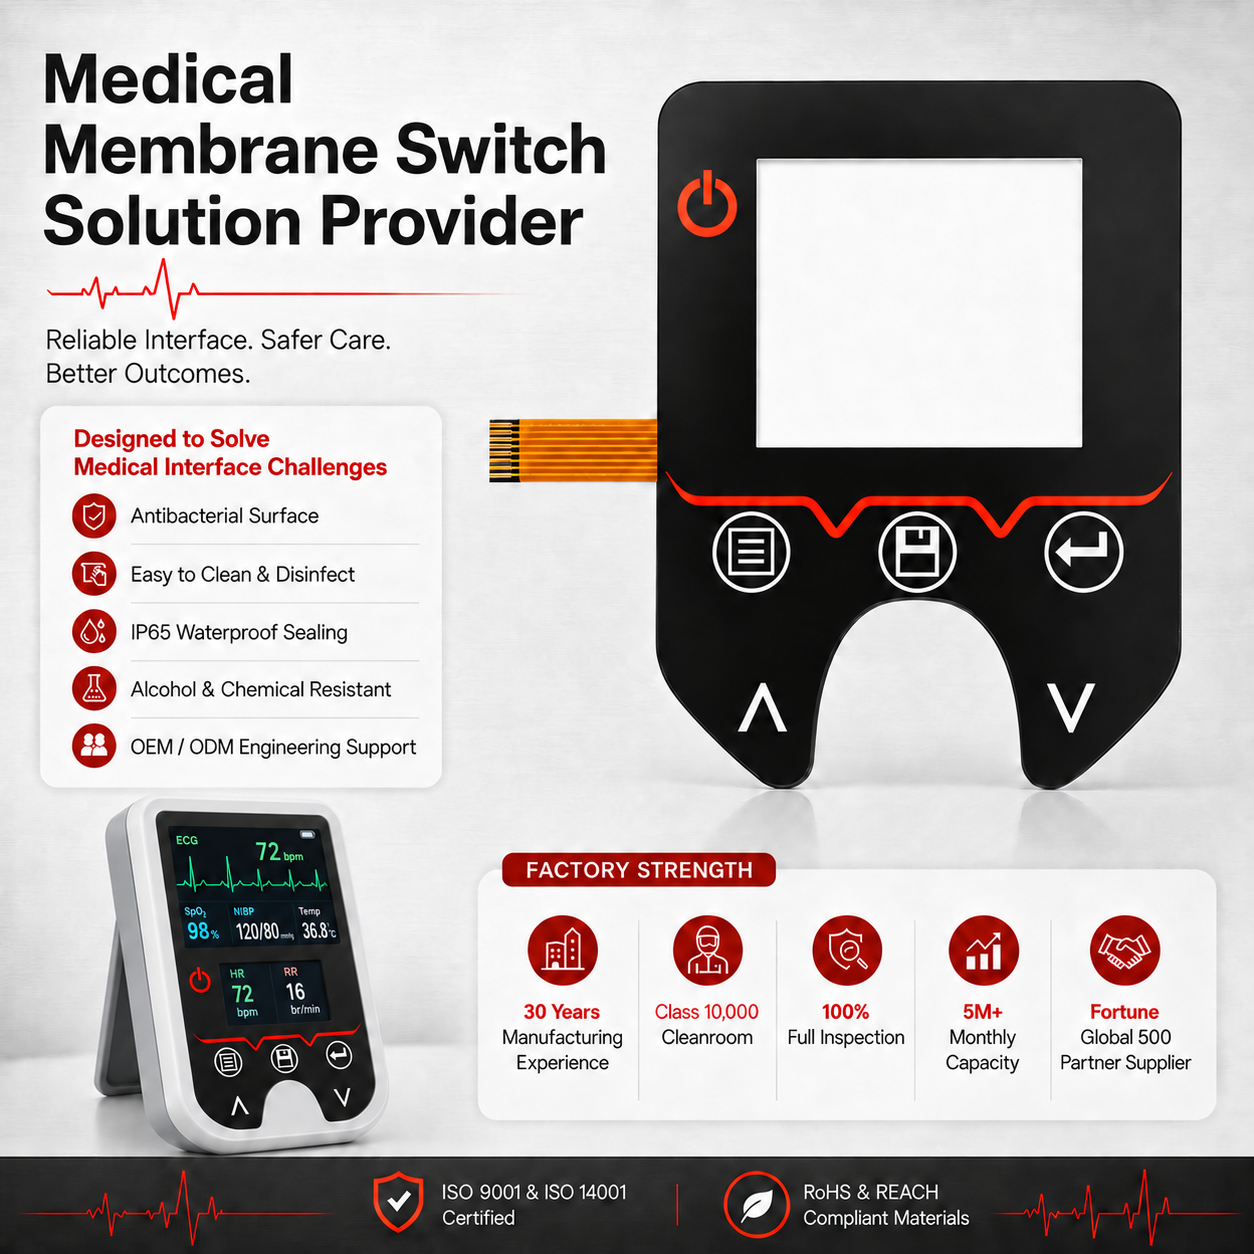
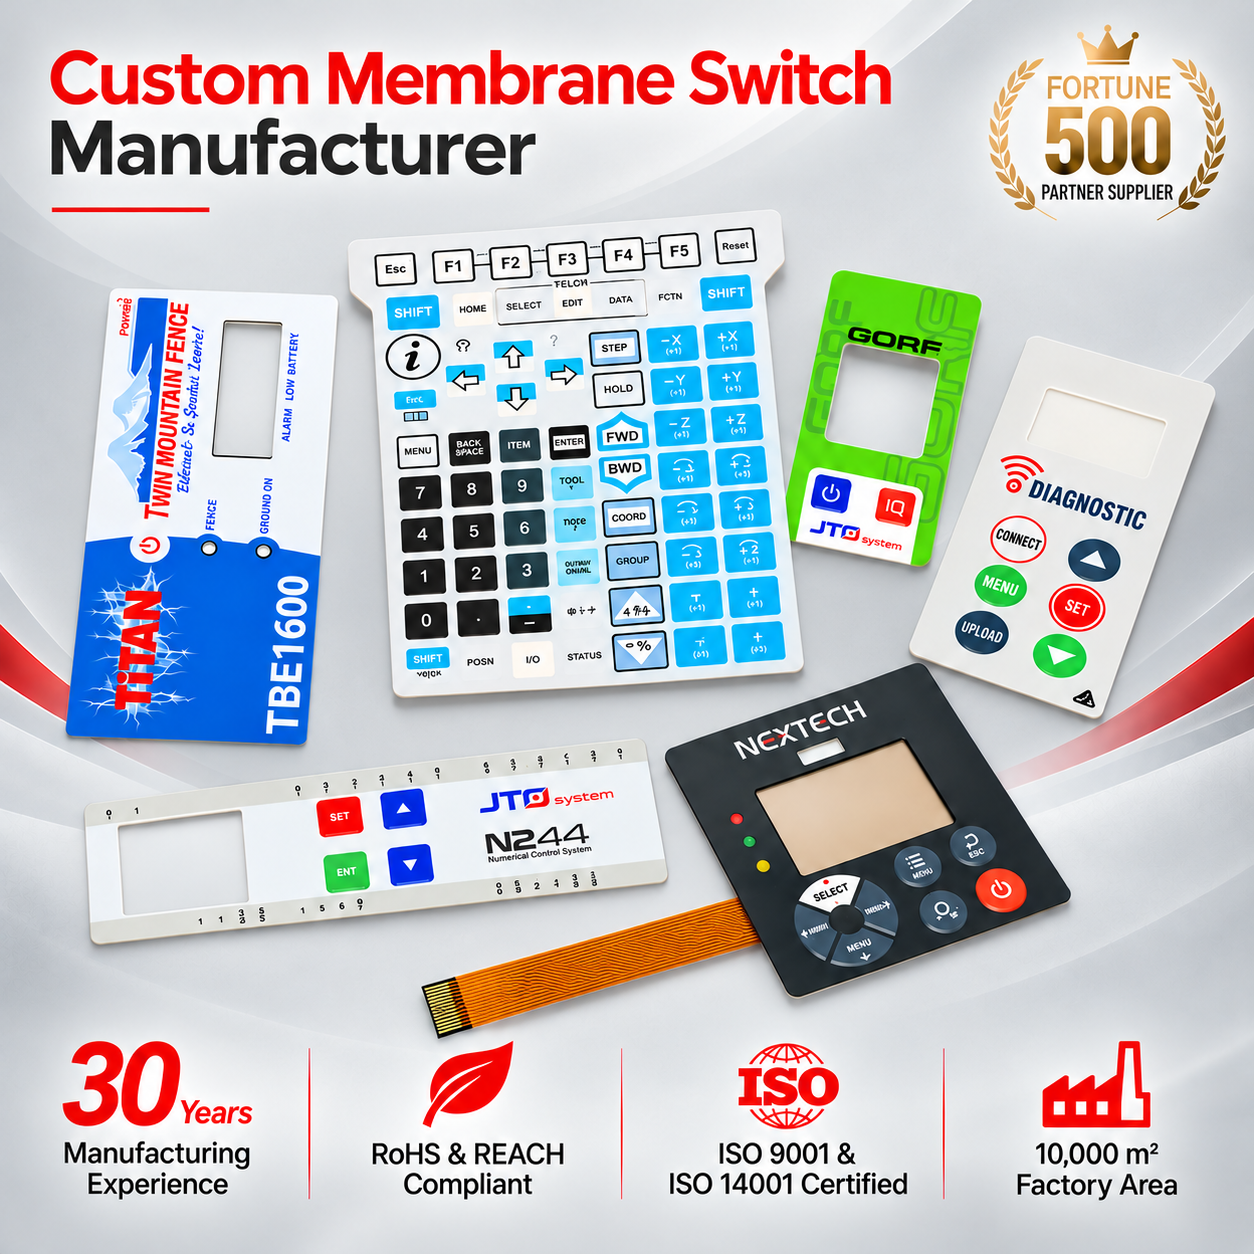
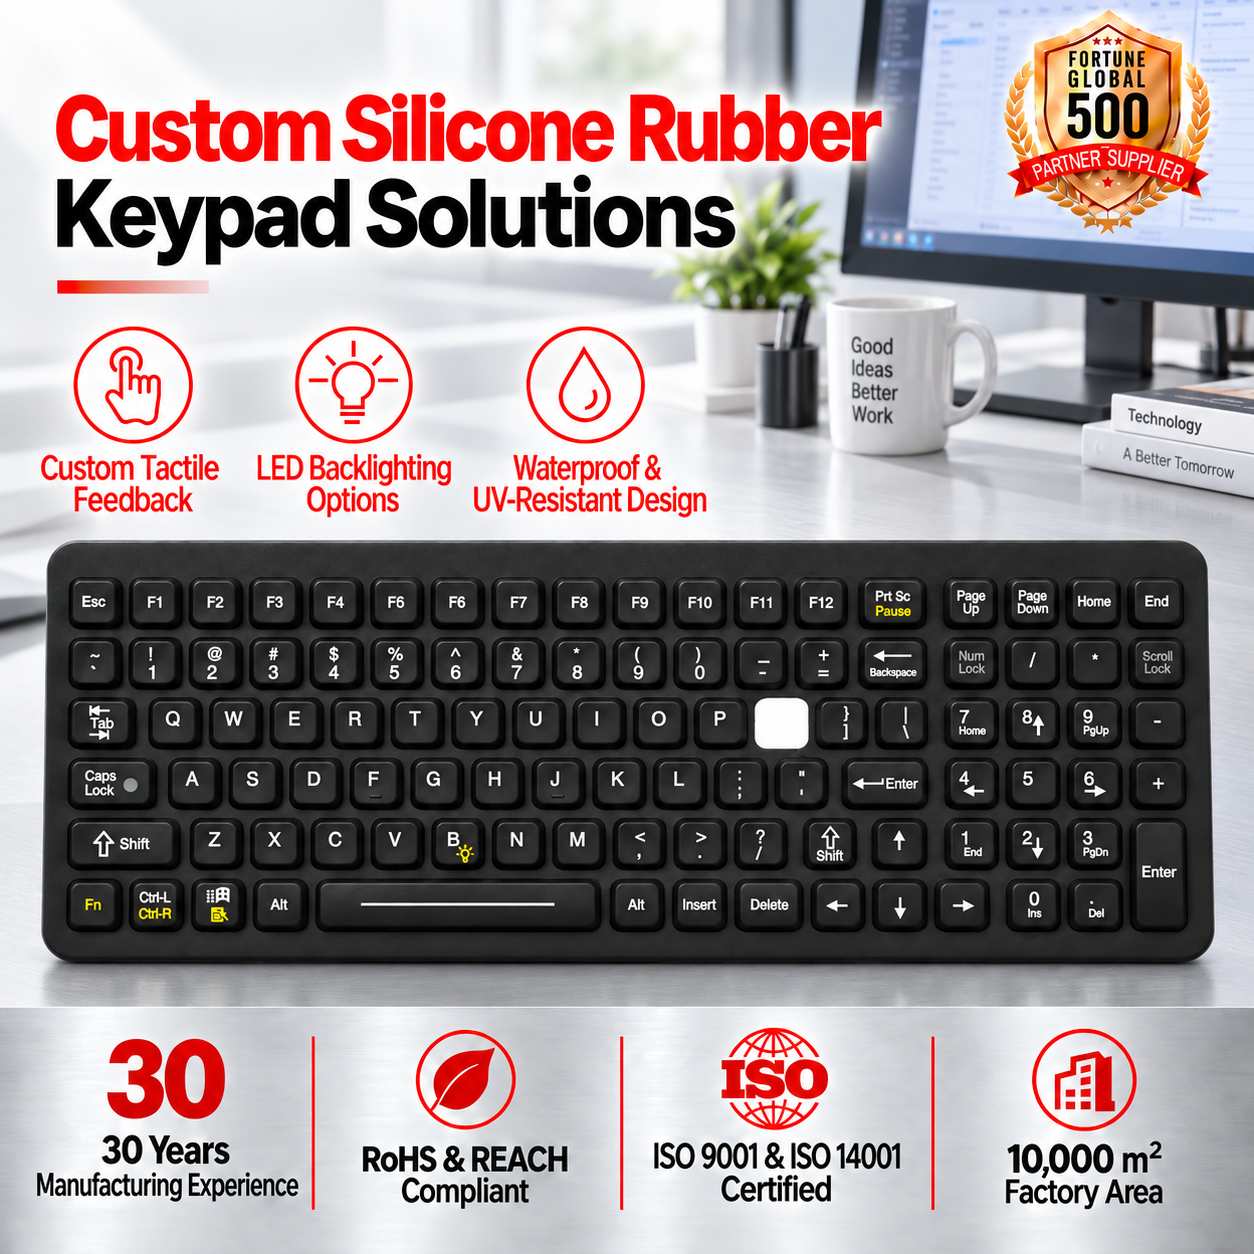
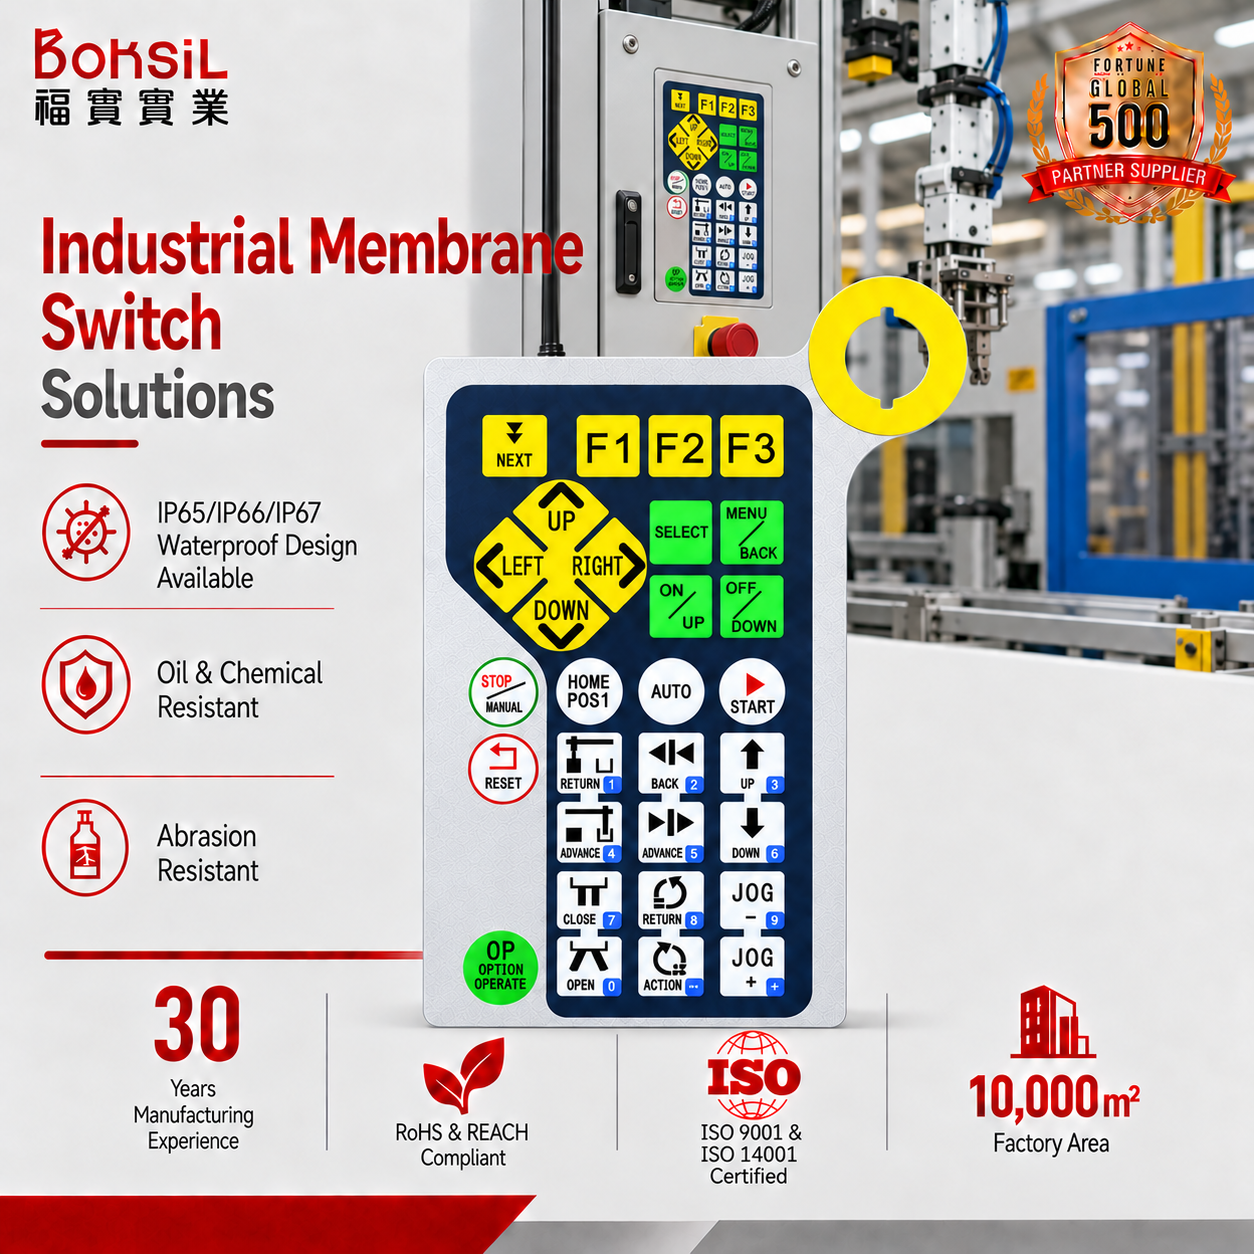
Medical Equipment Membrane Switch Manufacturer & Exporter serving Bequia
ISO-Compliant, Hermetically Sealed Tactile Human-Machine Interfaces Built for Tropical Island Resilience, Marine Salt Spray, and Clinical Sterilization Protocols.
Export Catalog
Engineered Medical & Industrial HMI Solutions
From cleanroom-fabricated antimicrobial front panels to rugged marine elastomeric keypads, our products deliver multi-layer ingress defense, tactical feedback, and extended duty cycles.
Interface Architecture for High-Salinity & Humid Climates
Deploying sensitive medical diagnostic consoles and emergency healthcare devices in maritime island territories like Bequia presents extreme engineering hurdles. Our multi-layer construction mitigates humidity infiltration, salt-induced galvanic oxidation, and rigorous clinical disinfectants.
Hermetic Perimeter Barrier Technology
Traditional open-vented membrane keypads suffer rapid moisture ingress in Caribbean ambient relative humidities exceeding 85%. AXRU engineers internal micro-channel equalization combined with 3M 200MP/300LSE acrylic perimeter sealing matrices. This maintains crisp snap-dome actuation force without permitting saline-laden airborne vapor to cause silver migration or intermittent track shorts.
Hospital-Grade Chemical Hard-Coating
Sterilization regimens in island triage clinics and maritime ambulances involve harsh active agents, including isopropyl alcohol, quaternary ammonium, glutaraldehyde, and accelerated hydrogen peroxide. We utilize biaxially-oriented, textured polyester (PET) treated with antimicrobial nano-silver fluoropolymer coatings that prevent hazing, cracking, or ink degradation under continuous hospital wash-downs.
Copper FPC & Nickel-Gold Anti-Corrosion
Where high-density tail routing or ultra-low circuit resistance is required for patient biometric monitors, silver flake printed on PET can degrade in marine atmospheres. We offer Polyimide Flexible Printed Circuits (FPC) with rolled annealed copper tracks, electrolytic nickel barrier plating, and immersion gold (ENIG) terminal fingers to achieve zero corrosion and million-cycle contact stability.
Island Operational Scenarios
Field-Proven Deployment Across Bequia Infrastructure
From Port Elizabeth clinics to private yacht med-bays and Grenadine inter-island medical transfer craft, our HMI panels operate reliably where standard commercial electronics fail.
Point-of-Care Clinic Diagnostics
Installed on hematology analyzers, centrifuges, and ECG diagnostic terminals in community health clinics, delivering hygienic wipe-down fronts that protect sensitive internal electronics from condensation.
Emergency & Rescue Vessel HMI
Powering defibrillators and oxygen therapy units on maritime transit vessels shuttling between Bequia and Kingstown, handling rough tactile operation, salt spray, and extreme temperature fluctuations.
Dialysis & Reverse Osmosis Treatment
Precision interface overlays controlling water purification and clinical hemodialysis sub-assemblies, engineered with leak-proof gaskets to prevent chemical fluid ingress during continuous operation.
Decentralized Cold Chain Vaccine Storage
Microprocessor control keypads for solar-assisted medical refrigeration containers across remote island coves, ensuring zero false triggers and imperviousness to tropical insect ingress.
Caribbean Healthcare Horizon
Regional Trends Reshaping Medical Device Procurement in Bequia
An evolving healthcare ecosystem in Saint Vincent and the Grenadines drives modernization towards ruggedized, decentralized, and marine-resilient clinical instrumentation.
Telemedicine & Rapid Decentralized Care
Island healthcare networks are shifting from centralized urban hospitals to distributed smart diagnostic hubs. This surge demands portable medical hardware with intuitive tactile membrane switches that allow local nursing staff to execute multi-parameter vitals testing swiftly without complex digital menu latency.
Marine-Grade Hybrid HMI Consolidation
Yacht tourism and marine hospitality expansion around Admiralty Bay necessitate onboard medical bays equipped with devices capable of enduring long-term open-air maritime exposure. Procurement teams favor hybrid silicone-rubber sealed membrane designs that blend IP67 waterproof protection with backlighting for nocturnal emergencies.
Stricter Global Compliance Verification
Caribbean bio-equipment refurbishers and public procurement boards are mandating full traceable certifications (RoHS, REACH, ISO 9001, and UL 94 flammability standards) on all imported replacement sub-assemblies, eliminating substandard generic replacement parts that cause premature equipment failure.
Enterprise Advantage
Why Global OEM Buyers & Importers Trust AXRU
From single prototypes to container-scale mass production, our fully integrated 10,000㎡ manufacturing facility in Dongguan, China guarantees engineering accountability at every production stage.
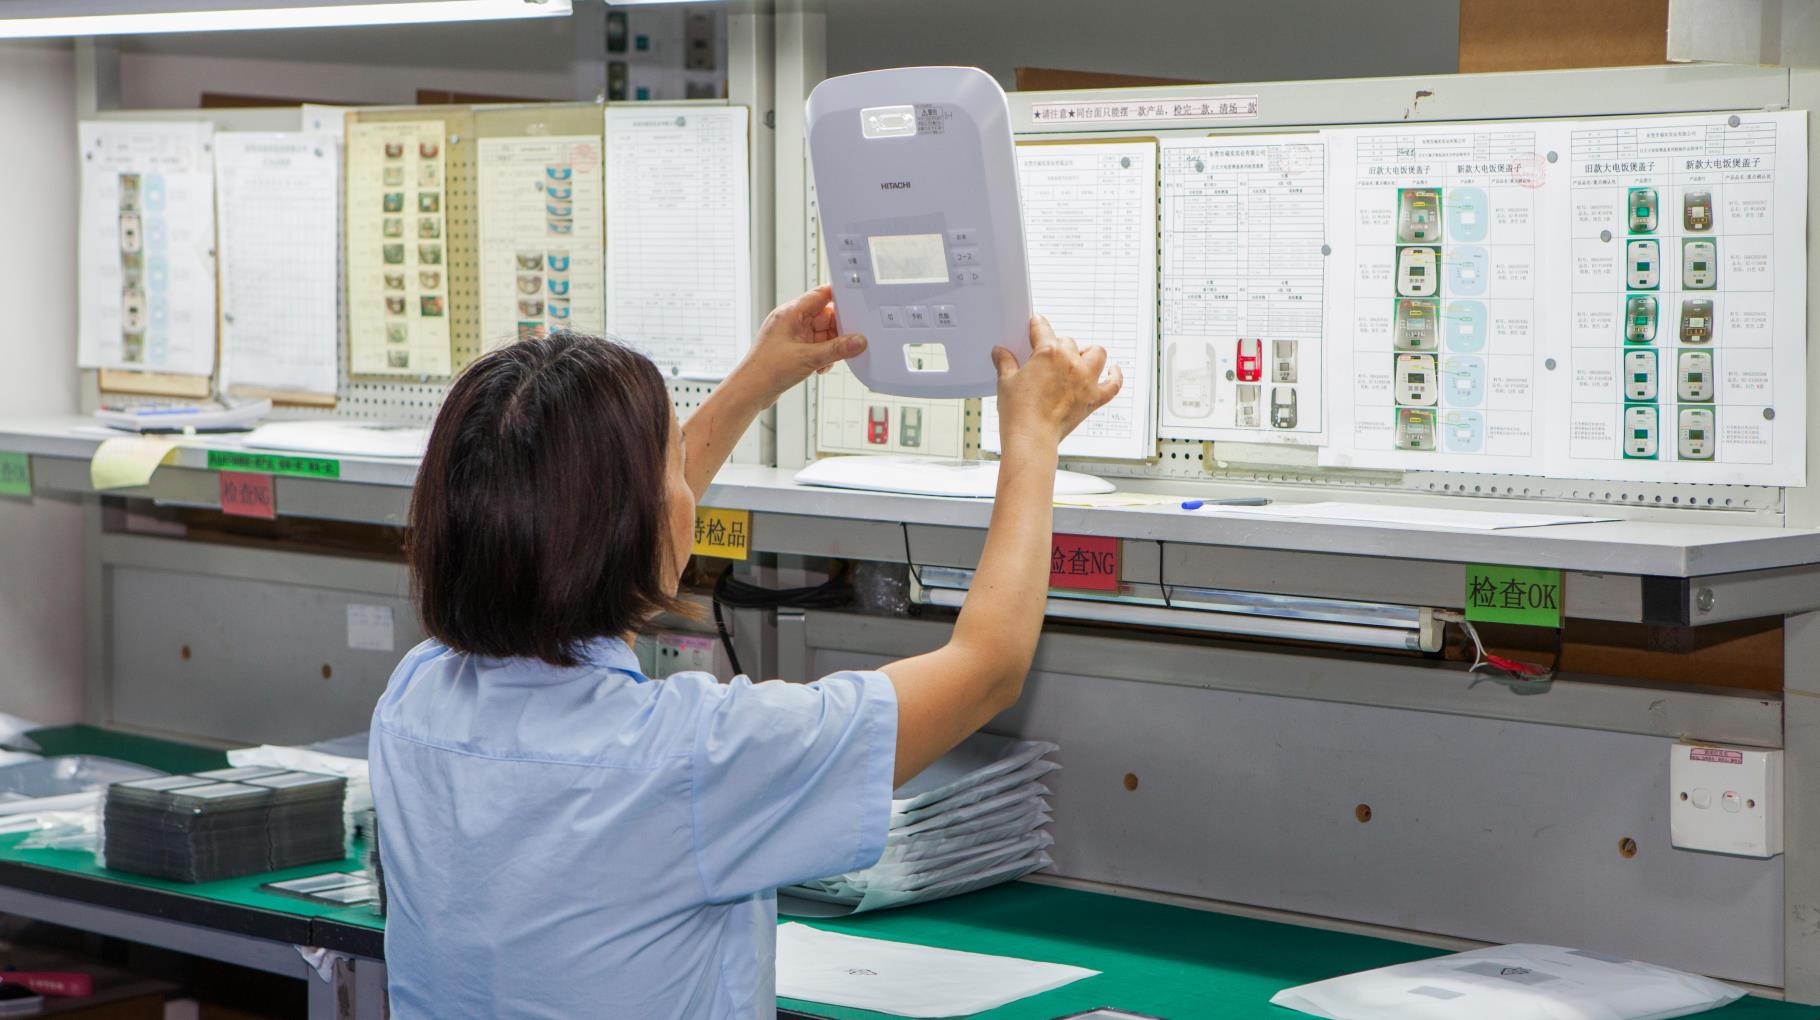
We do not outsource core processes. Printing, laser patterning, dome placement, laminating, and environmental stress profiling are executed under strictly monitored climate conditions. Our reliability laboratory simulates decades of operational stress, ensuring membrane assemblies exported to remote destinations perform without fail.
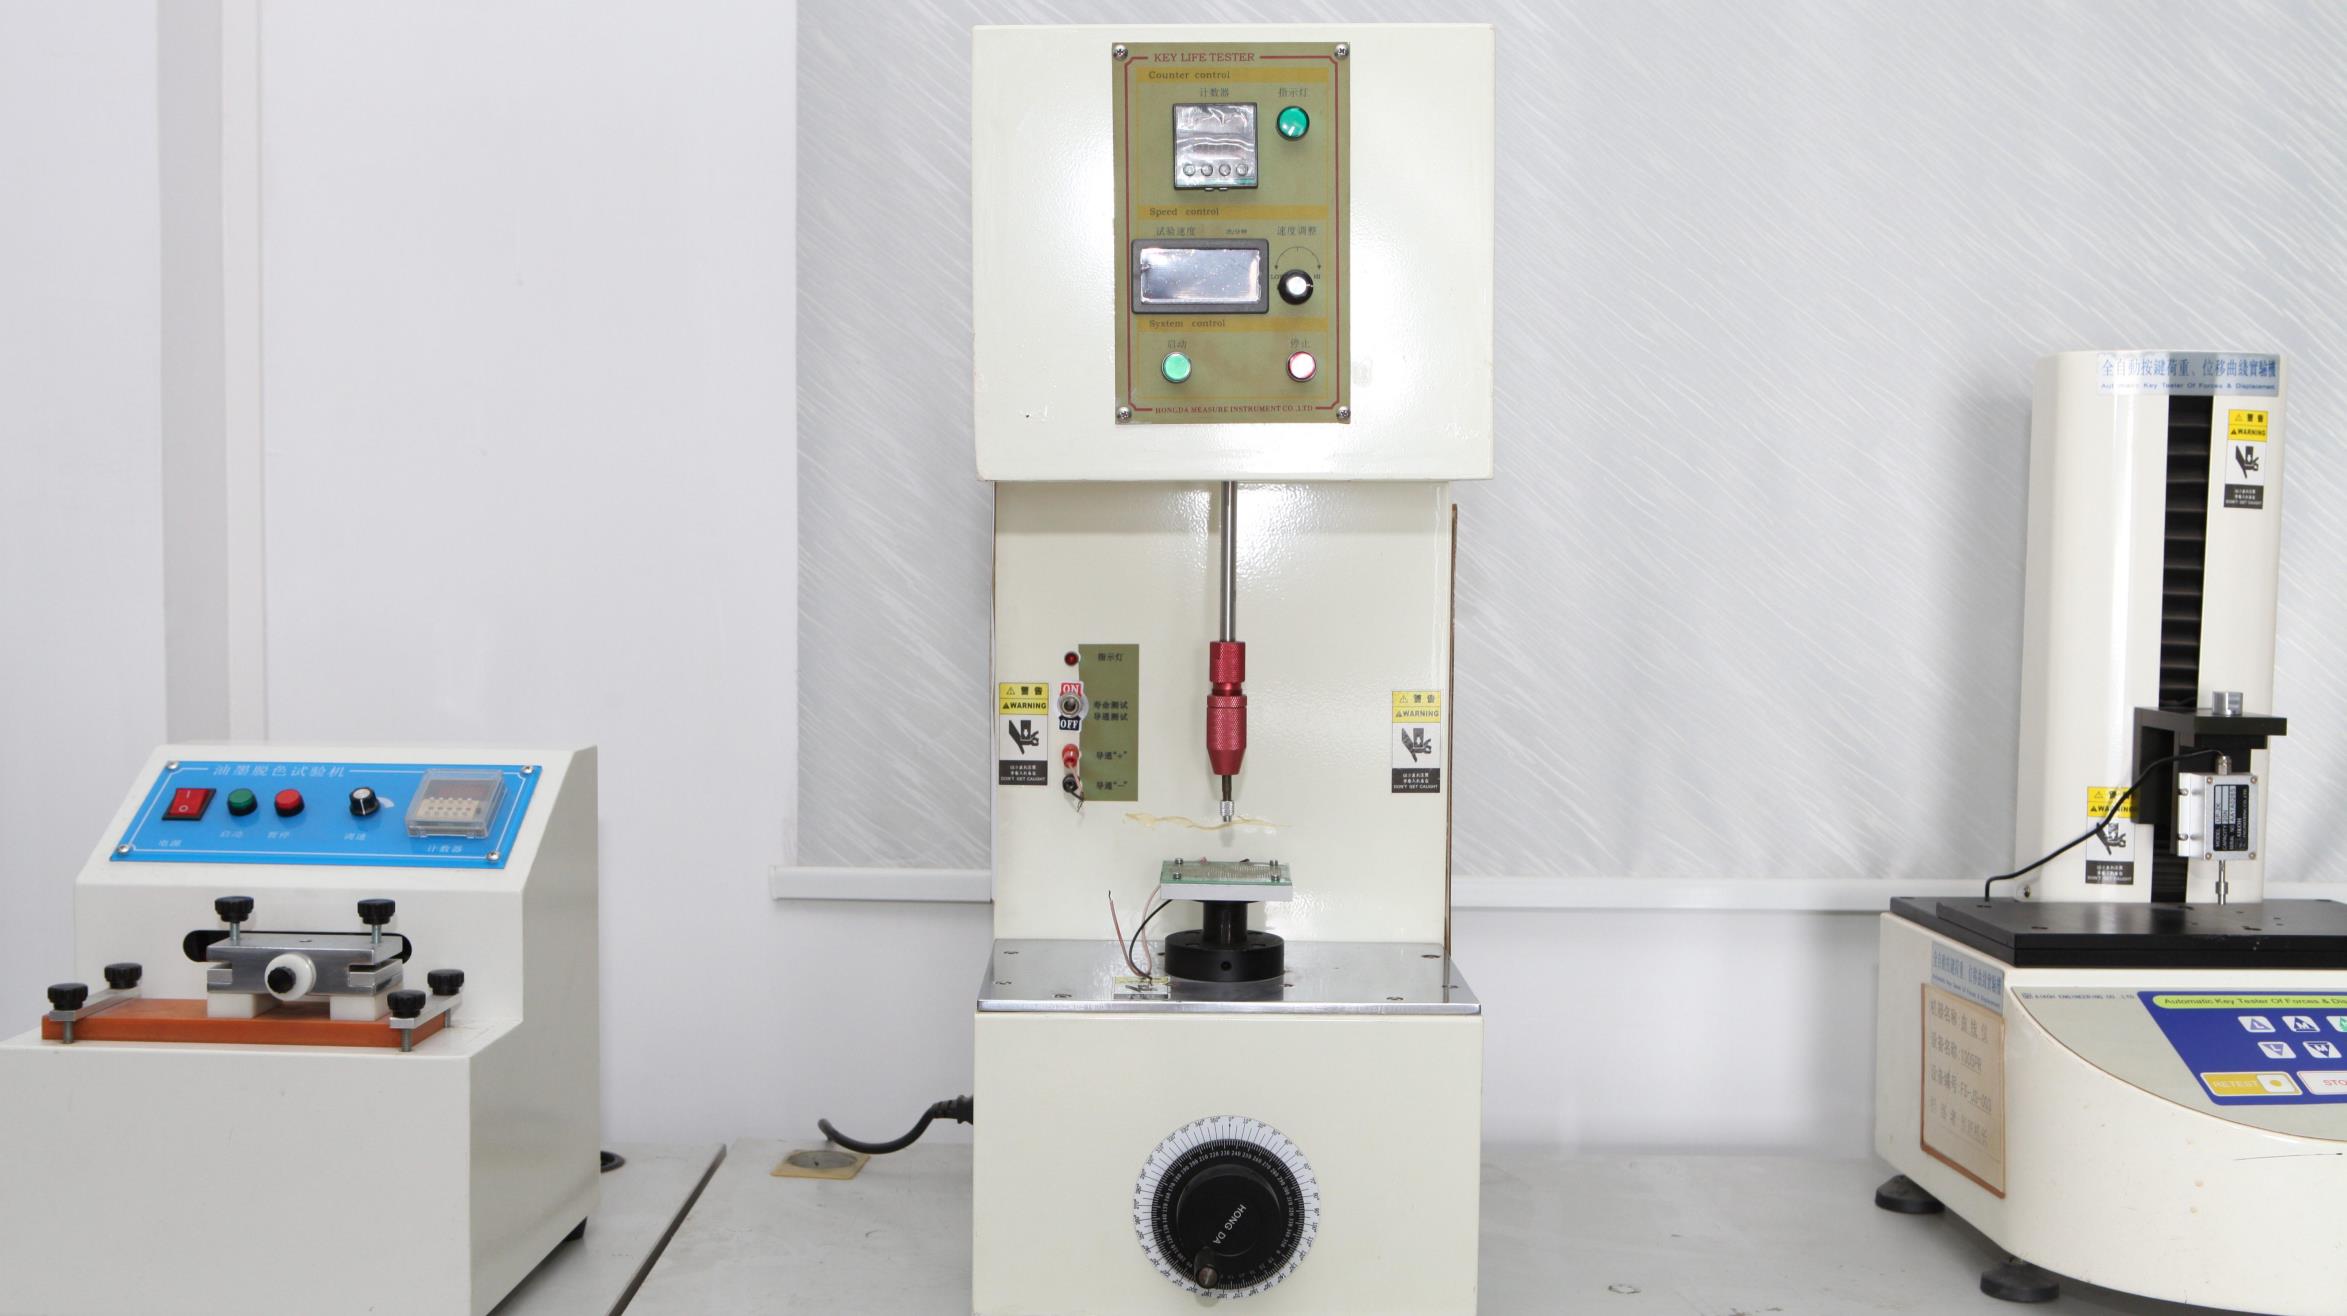
Key Actuation Life Testing: Automated pneumatic testers cycle metal domes beyond 3,000,000 strokes to verify snap ratio stability and spring back integrity.
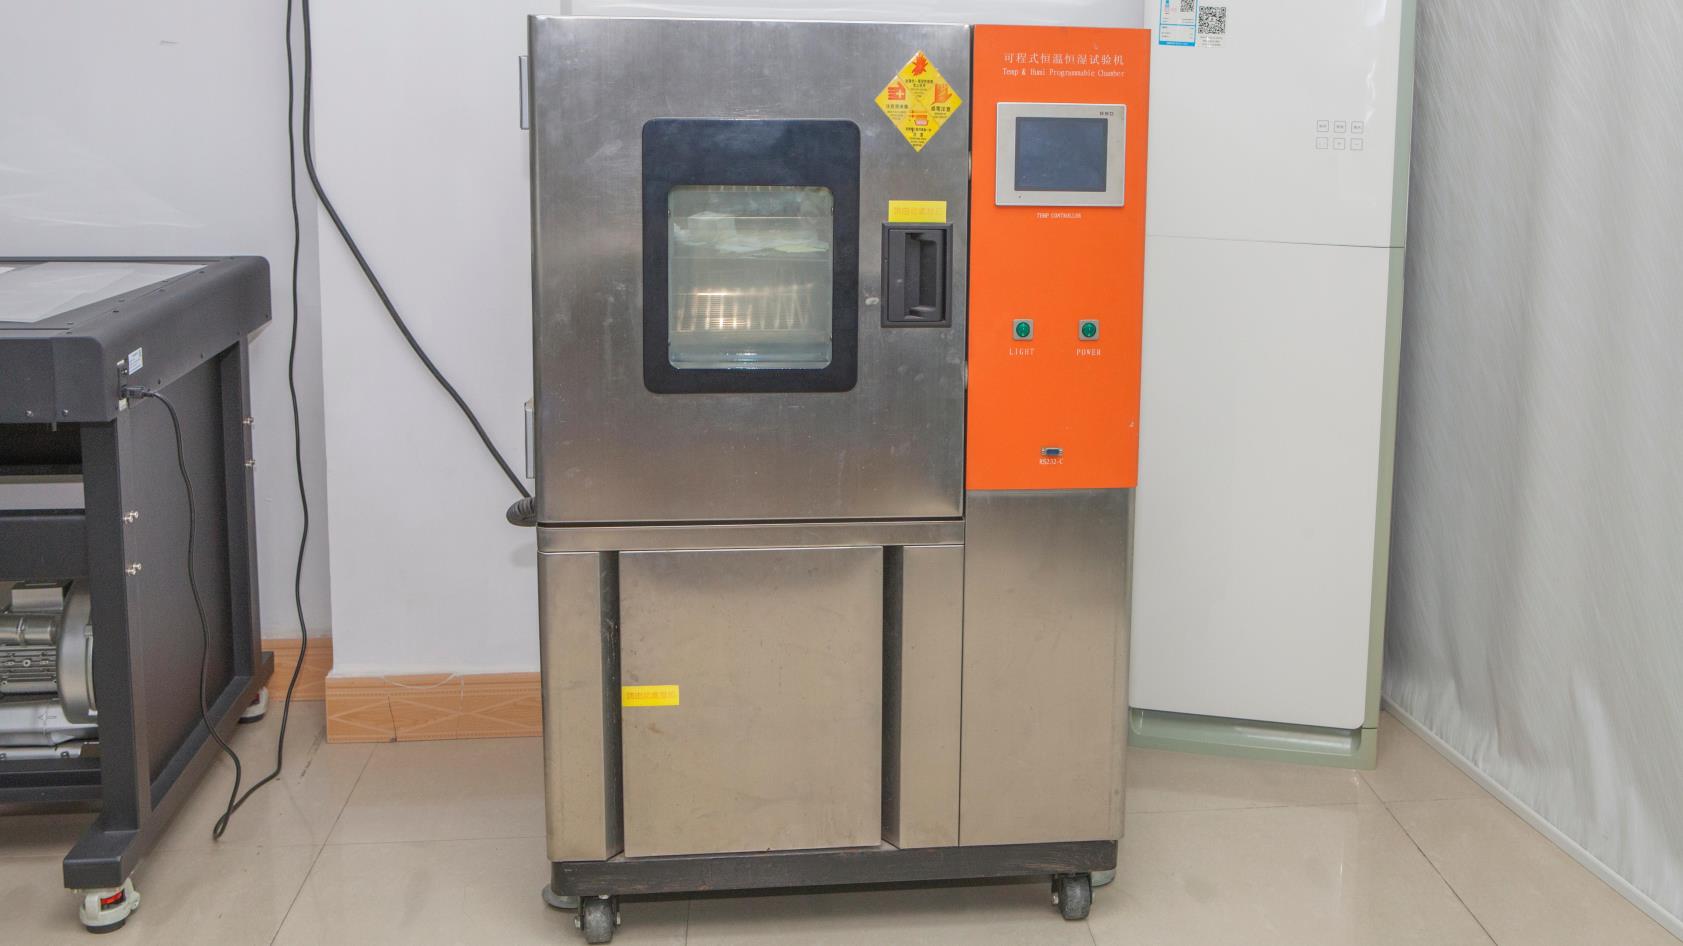
Programmable Humidity & Temp Chambers: Thermal cycling from -40°C to +85°C at 95% RH ensures zero delamination in tropical environments like Bequia.
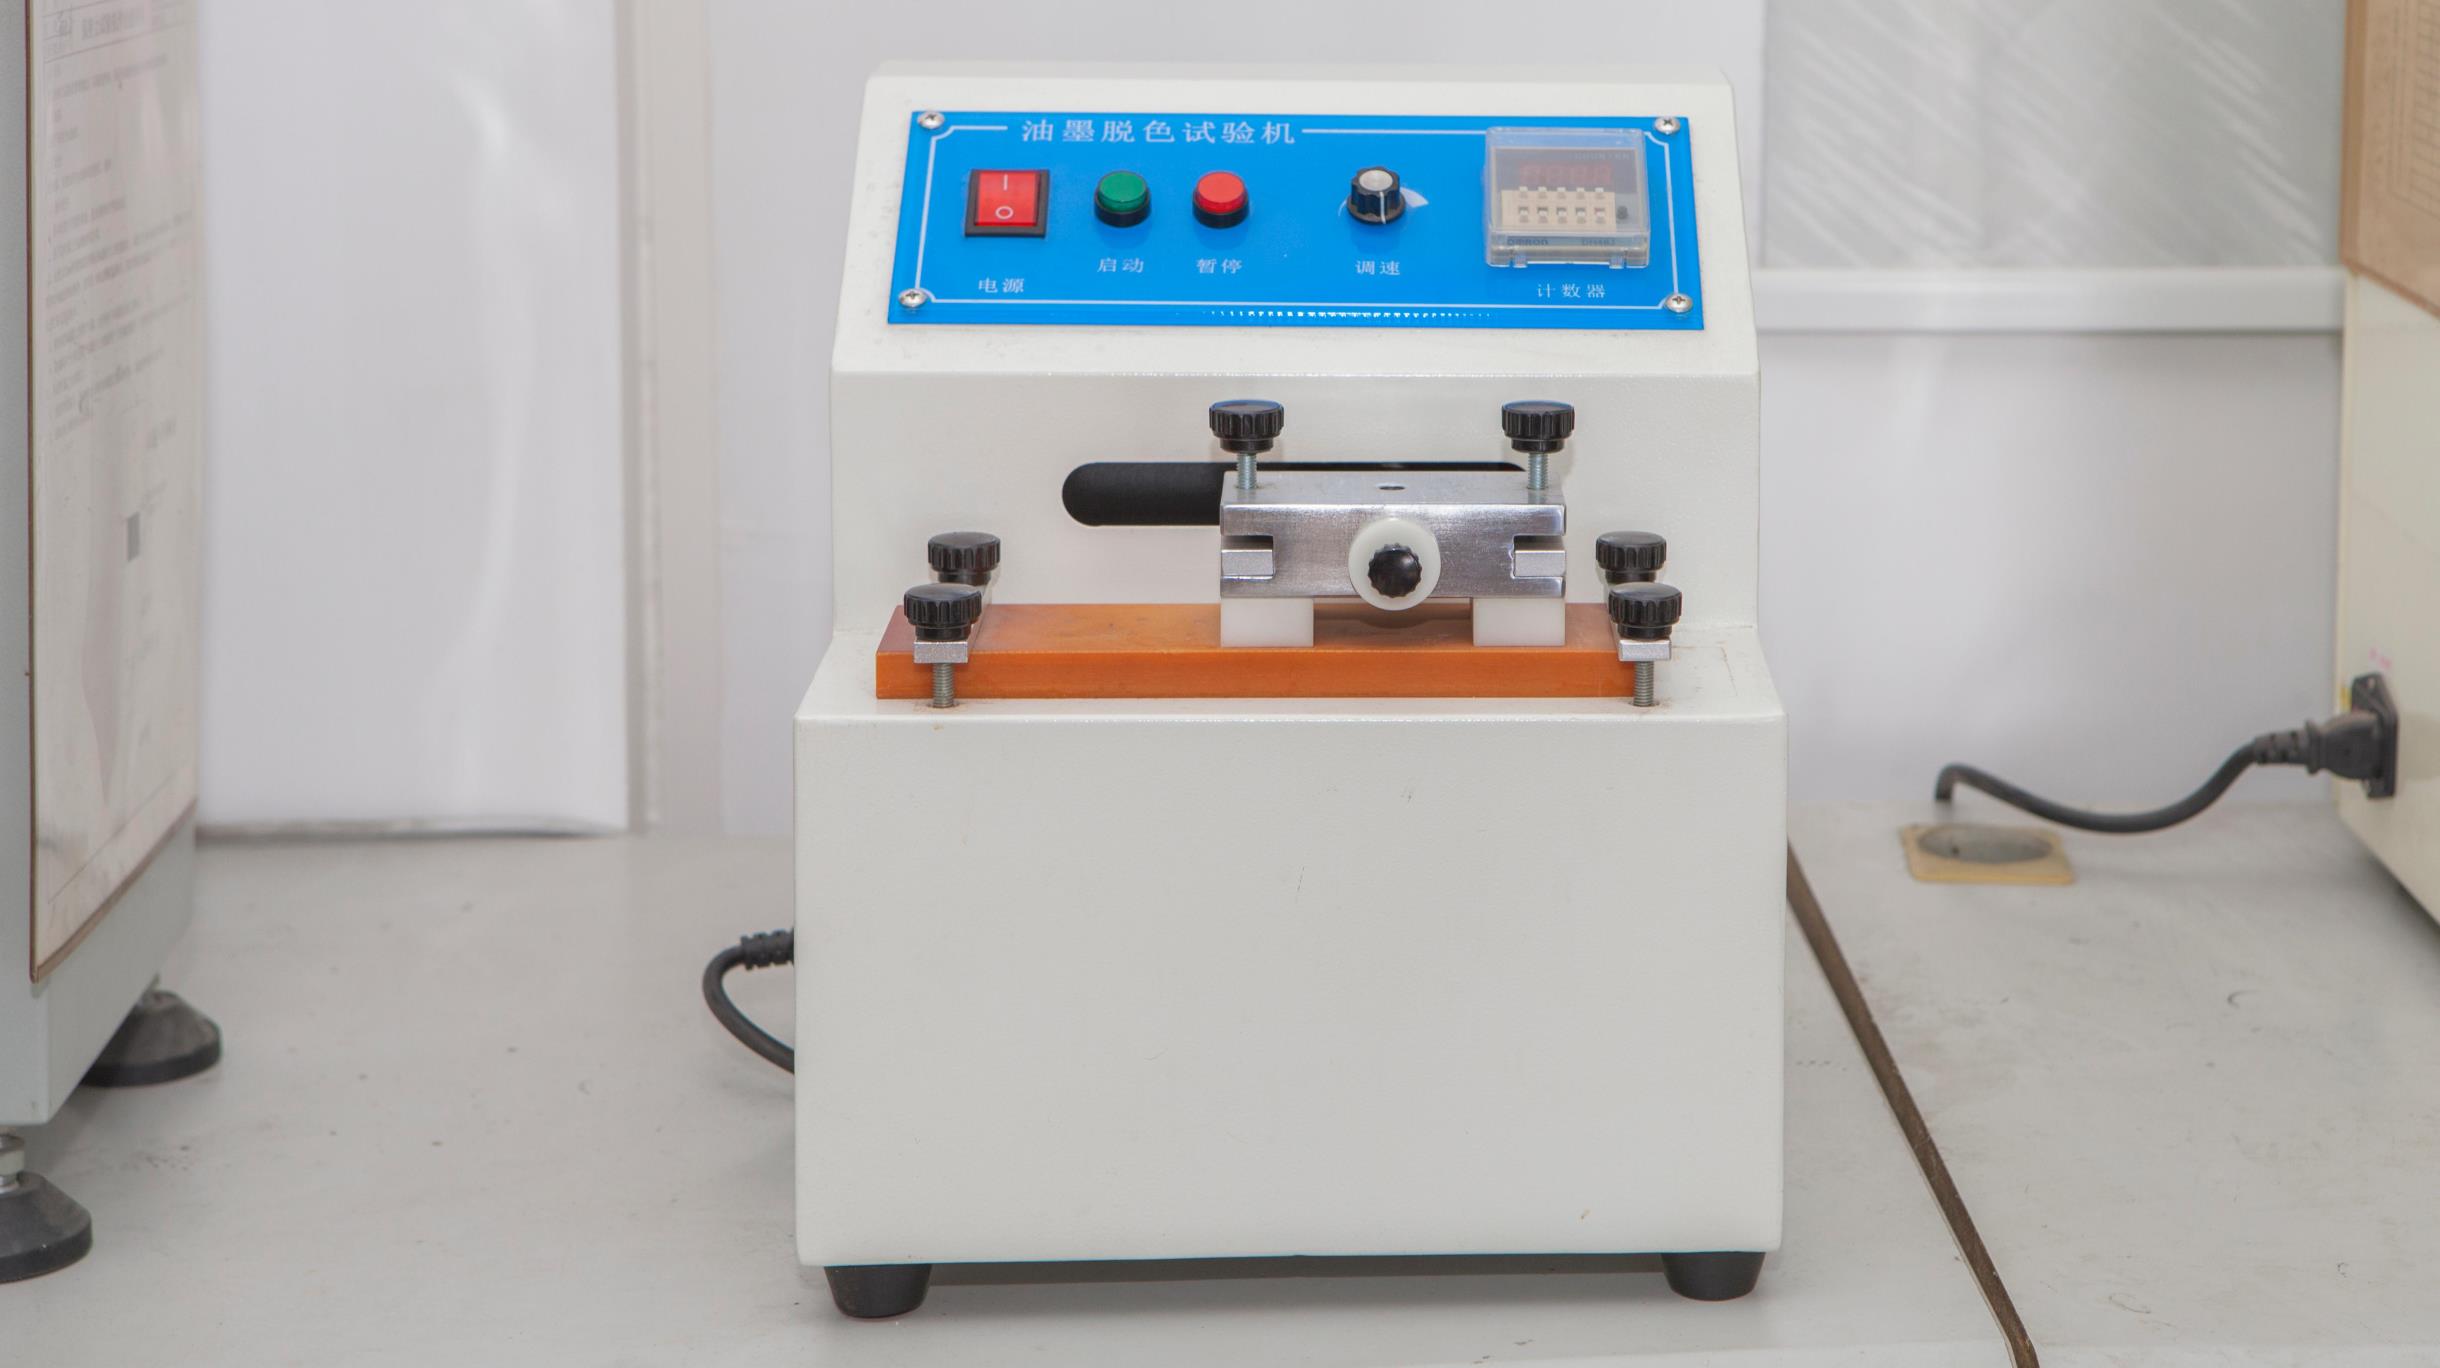
Ink Decolorization & UV Abrasion: Verified via Taber abrasers and UV weathering chambers to prevent yellowing or legend erasure from aggressive cleaning.
Tensile & Adhesive Shear Tests: Verifying high-tack adhesive bonding to stainless steel, aluminum, ABS, and polycarbonate enclosures.
Frequently Asked Questions for Bequia & Caribbean Buyers
Answers to common logistical, engineering, and quality queries regarding custom medical interface procurement, international freight, and bespoke engineering.
Can AXRU manufacture replacement membrane switch panels for imported hospital devices in Bequia?
Yes. Healthcare providers and biomedical maintenance engineers often face obsolete OEM inventory or prohibitive replacement costs from original equipment manufacturers. AXRU offers full reverse engineering capabilities. By providing a photo, dimensions, or a physical failed sample unit, our technical team reconstructs the circuit schematic, matches overlay Pantone colors, and delivers identical or upgraded IP65/IP67 membrane switch replacements starting from low volumes.
How do your membrane switches resist tropical marine humidity and airborne salt?
Standard commercial switches fail in Caribbean coastal zones due to hygroscopic moisture drawing saline particles into the circuit, leading to dendritic silver growth and short circuits. We utilize perimeter gasket sealing adhesives (such as 3M 300LSE or 468MP), impermeable Autotype polyester graphic films, and optional dielectric overcoats over silver traces. For maximum durability, we build copper-etched FPC or gold-plated contacts that completely eliminate oxidation vulnerabilities.
What is the typical Minimum Order Quantity (MOQ) and sample lead time?
We support regional development and specialized low-volume equipment builds with an accessible MOQ of just 100 pieces for custom membrane switches and silicone keypads. Rapid prototyping and engineering functional samples are completed within 7 to 10 working days, accompanied by complete First Article Inspection (FAI) reports prior to mass tooling release.
How are products packaged and shipped securely to Saint Vincent and the Grenadines?
All shipments destined for maritime transit receive multi-layer anti-static (ESD) protection and hermetically vacuum-sealed moisture barrier packaging with integrated silica desiccant packs. We ship globally via expedited air express (DHL, FedEx, UPS) directly to J.F. Mitchell Airport in Bequia or via consolidated maritime air cargo arriving in Kingstown, complete with export customs paperwork, commercial invoices, and RoHS/REACH certificates of compliance.
What technical drawings or design files do we need to provide to obtain an engineering quote?
To provide an accurate Design for Manufacturability (DFM) assessment and pricing, please share: 1) Graphic artwork in vector format (.AI, .CorelDraw, or .PDF) indicating Pantone/RAL colors; 2) Mechanical drawing (.DXF, .DWG, or .STEP) with key embossing, overall outline, display window positions, and tail length; 3) Circuit pinout schematic and connector type (e.g., female housing, solder tabs, ZIF connector); 4) Environmental requirements such as IP rating, operating temperature, and medical chemical exposure conditions.
Ready to Engineer or Upgrade Your Medical Equipment Interface?
Connect directly with our senior HMI engineering team. Receive comprehensive DFM analysis, material recommendations, and a transparent quotation within 24 hours.