Industrial Keyboard Overlays & Custom HMI Assemblies
Tested for coastal saline climates, heavy sanitization regimens, and over 1,000,000 actuations. Built to exact OEM specifications.
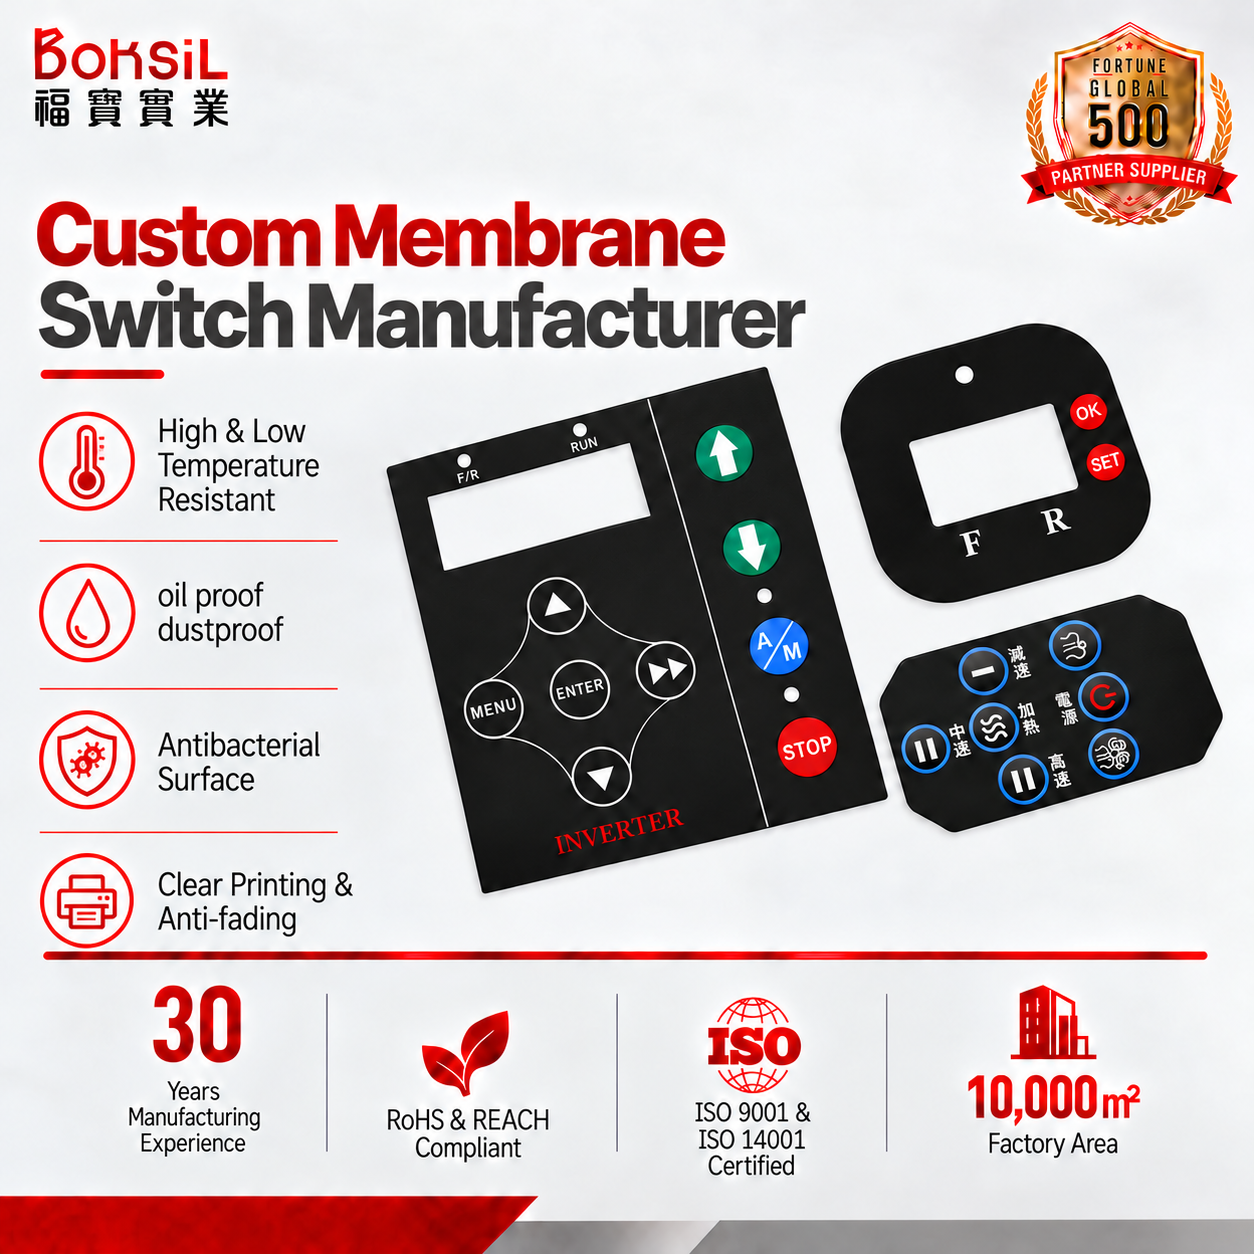
OEM/ODM Front Control Polycarbonate Graphic Overlay
- SubstrateLexan™ Polycarbonate (0.175–0.5mm)
- Adhesive Layer3M™ 467MP / 468MP High Tack
- UV StabilityFade-Resistant Sub-surface Printing
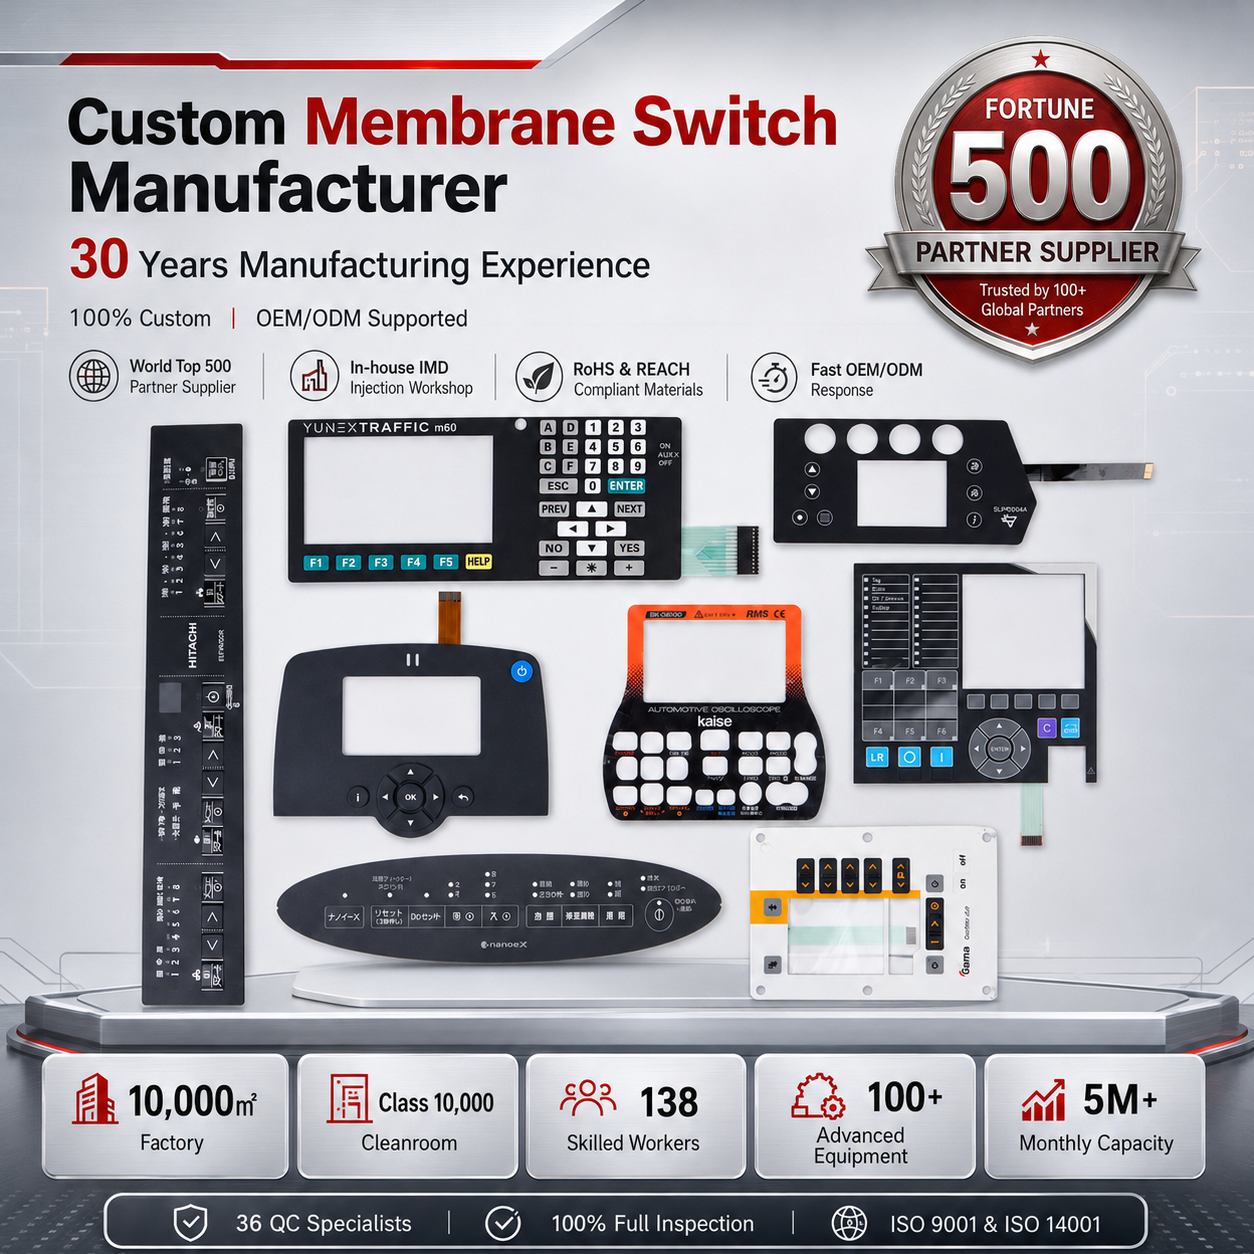
Waterproof FPC Appliance & Medical Membrane Switch
- Sealing GradeIP67 Watertight Perimeter Gasket
- CircuitryFlexible Copper FPC Tail
- Contact ReliabilityGold-Plated Metal Domes
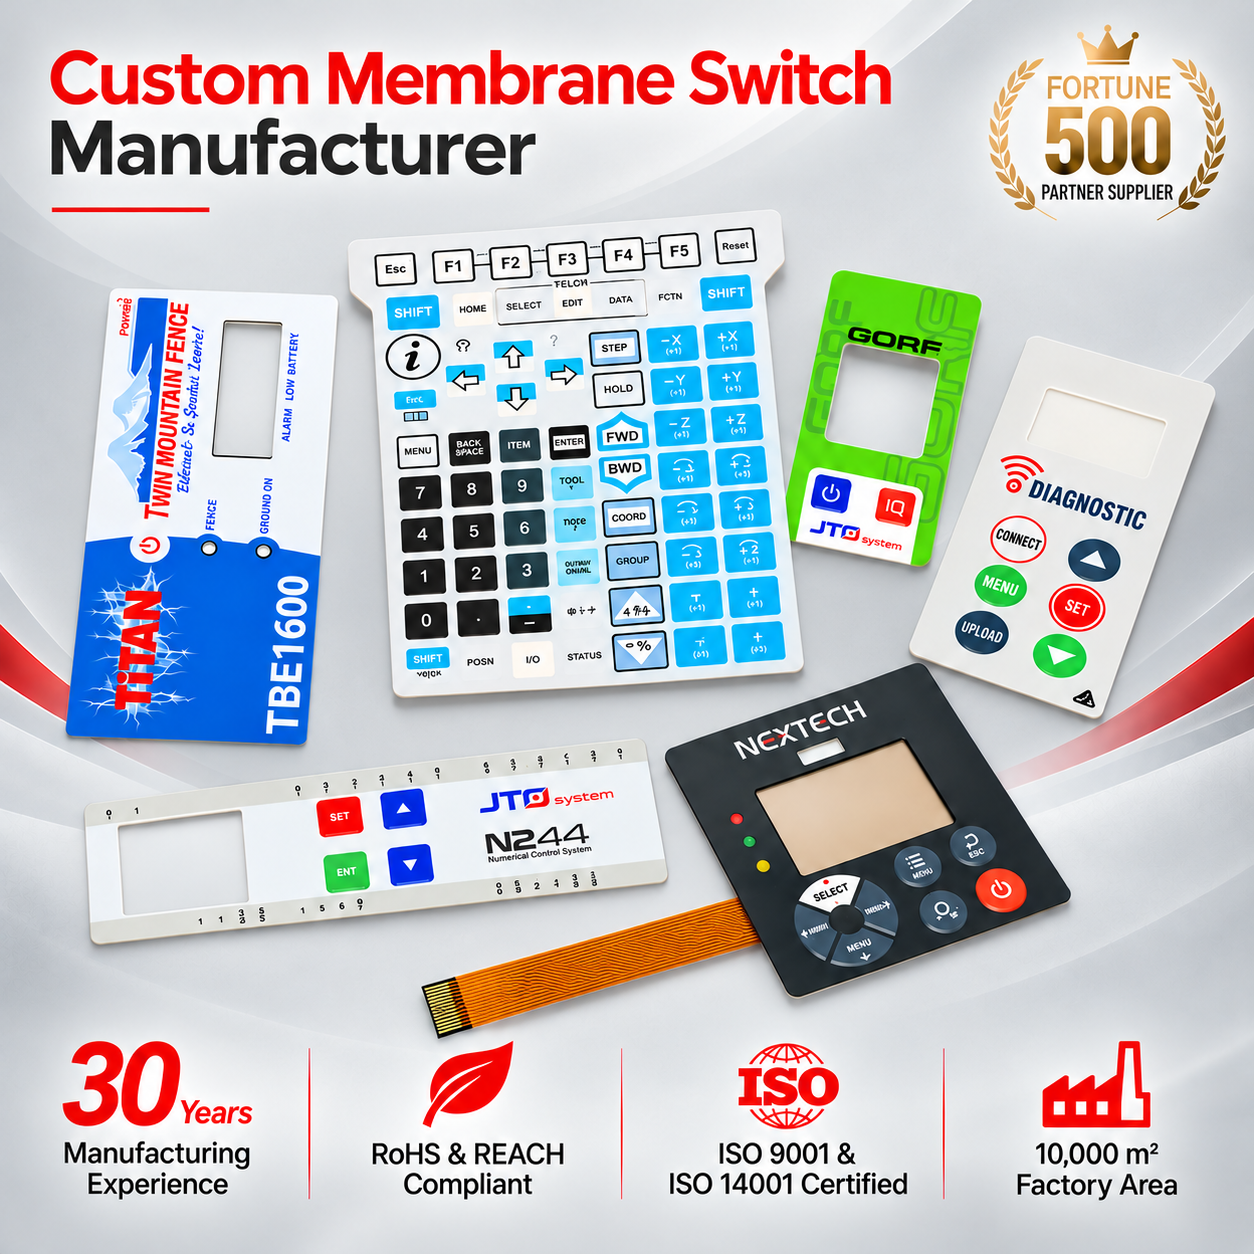
Embossed Tactile Button Flat Industrial Panel
- Tactile FeelPillow & Rim Embossing Options
- Cycle Endurance> 2.5 Million Cycles
- Chemical DefenseOils, Ketones & Mild Acids
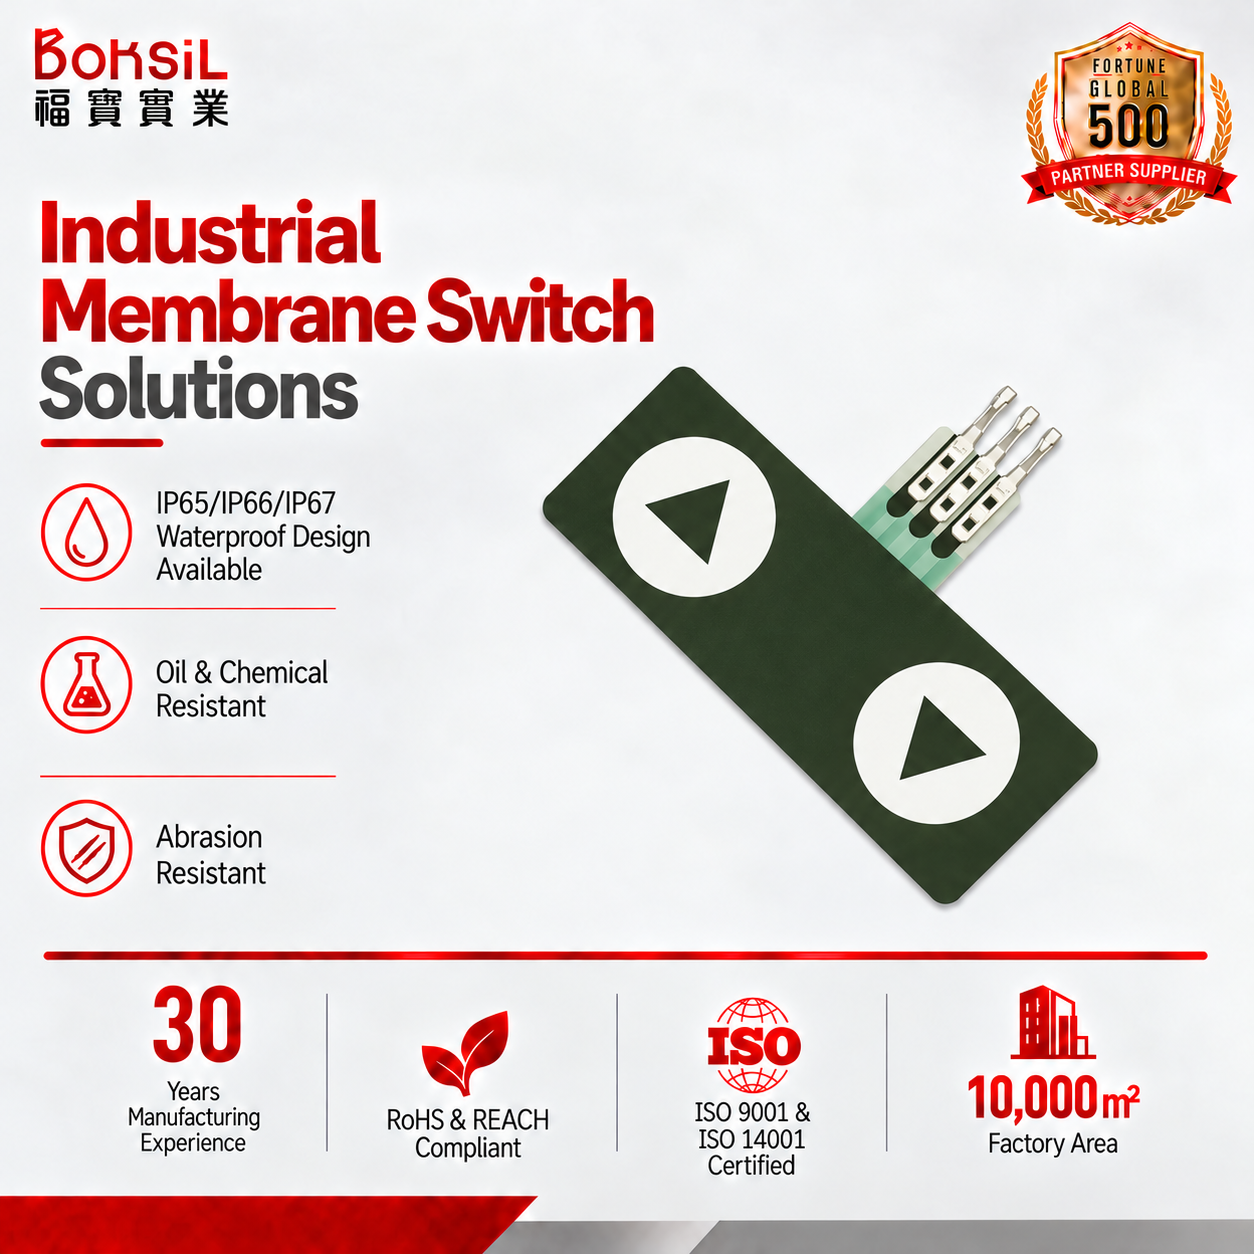
Custom 2-Button Industrial Overlay with FPC Circuit
- LayoutDual Actuator / Power & Mode
- Tail Connector1.0mm / 2.54mm Pitch ZIF/Molex
- ProtectionESD Shielding Layer Integrated
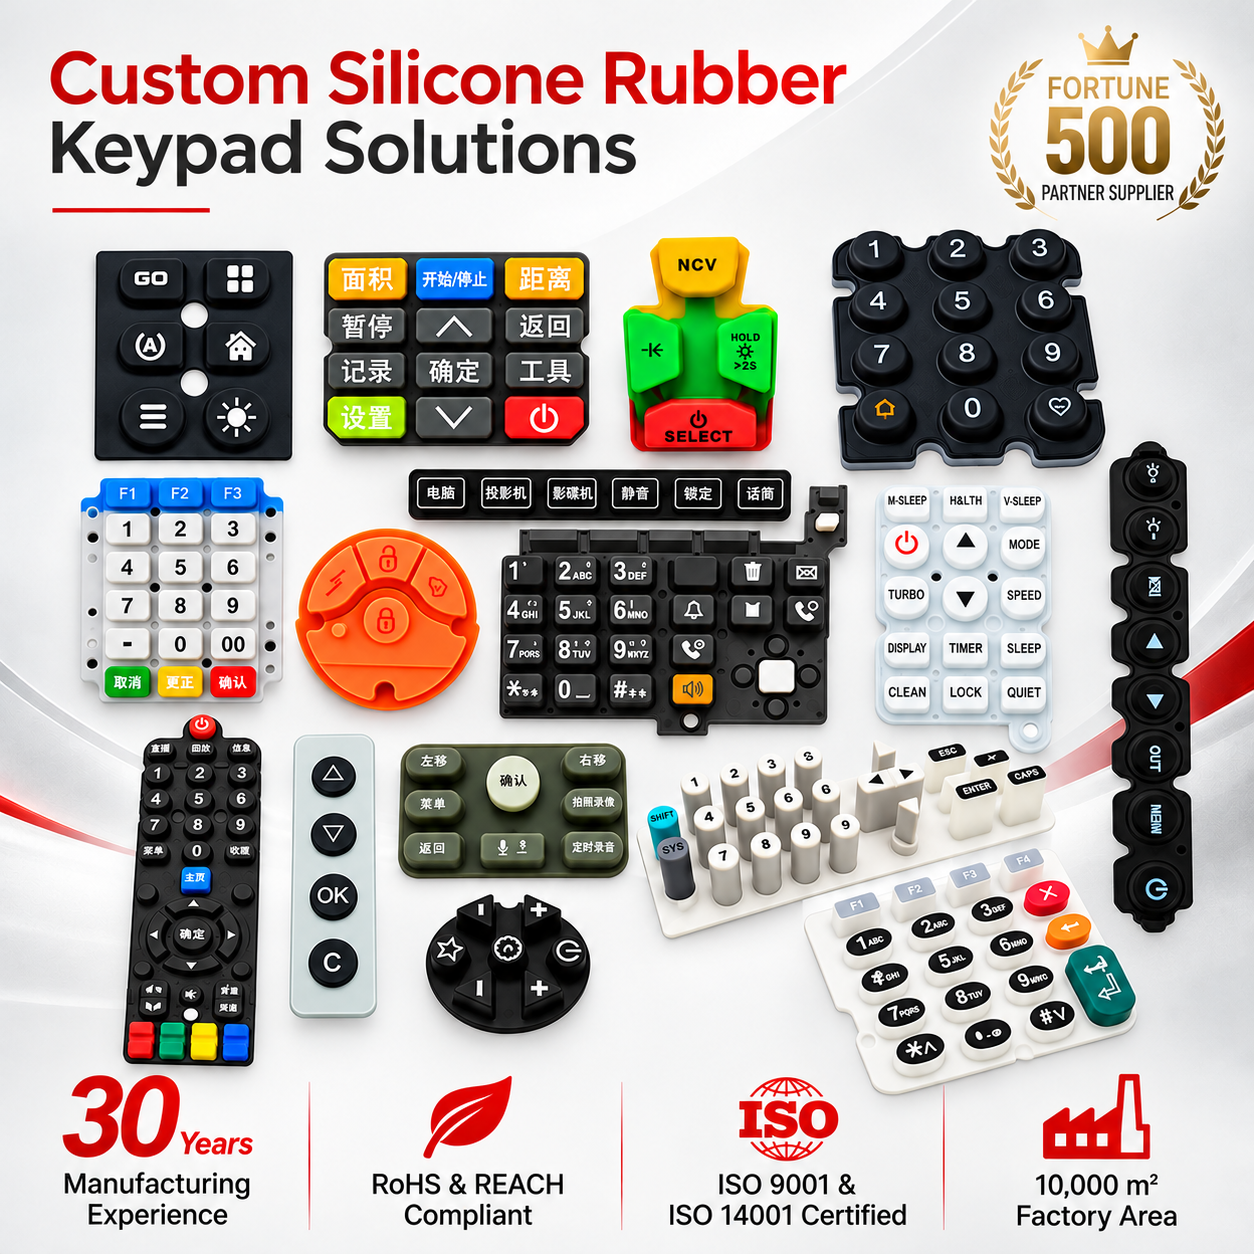
Multi-Color Conductive Silicone Rubber PTT Keypad
- MaterialSilicone Elastomer (Shore 45-70A)
- Contact TypeLow-Resistance Carbon Pill
- CoatingAbrasion-Proof PU / Epoxy Finish
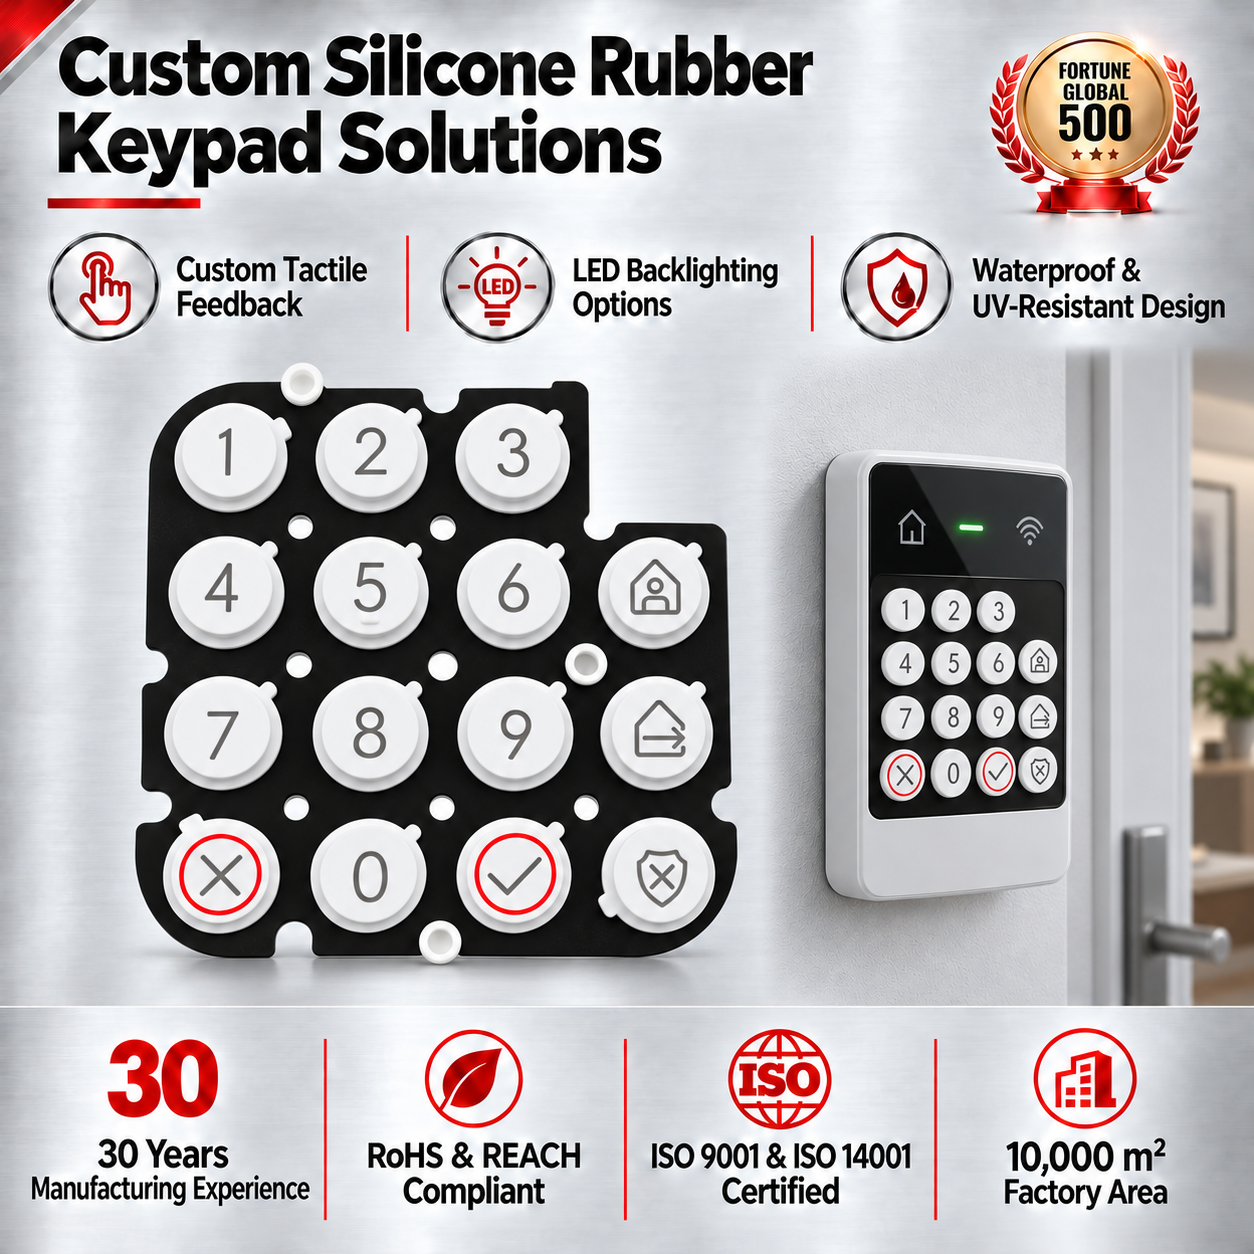
Numeric Appliance Silicone Keypad Overlay
- Key StyleLaser Etched / Backlit Ready
- Thermal Range-40°C to +125°C Resilience
- ApplicationCommercial Kitchens & POS
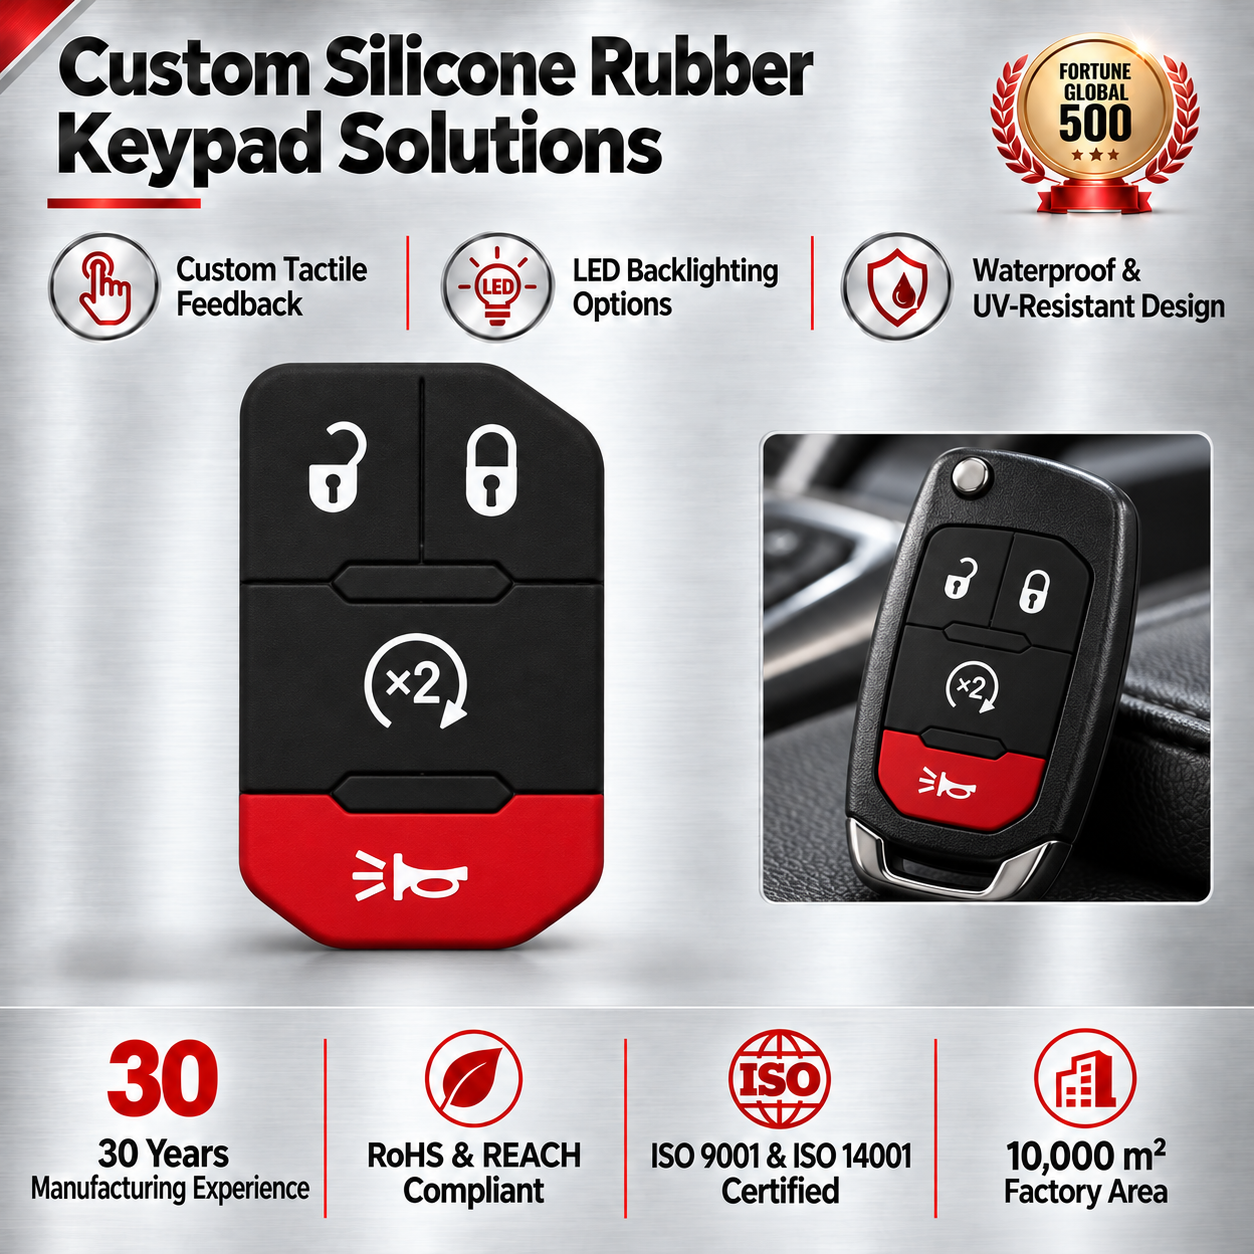
Waterproof 4-Button Silicone Enclosure Overlay
- ResilienceTear-Resistant Liquid Silicone
- PrintingSilkscreen with Protective Overcoat
- Ingress RatingIP68 Hermetic Compression Fit
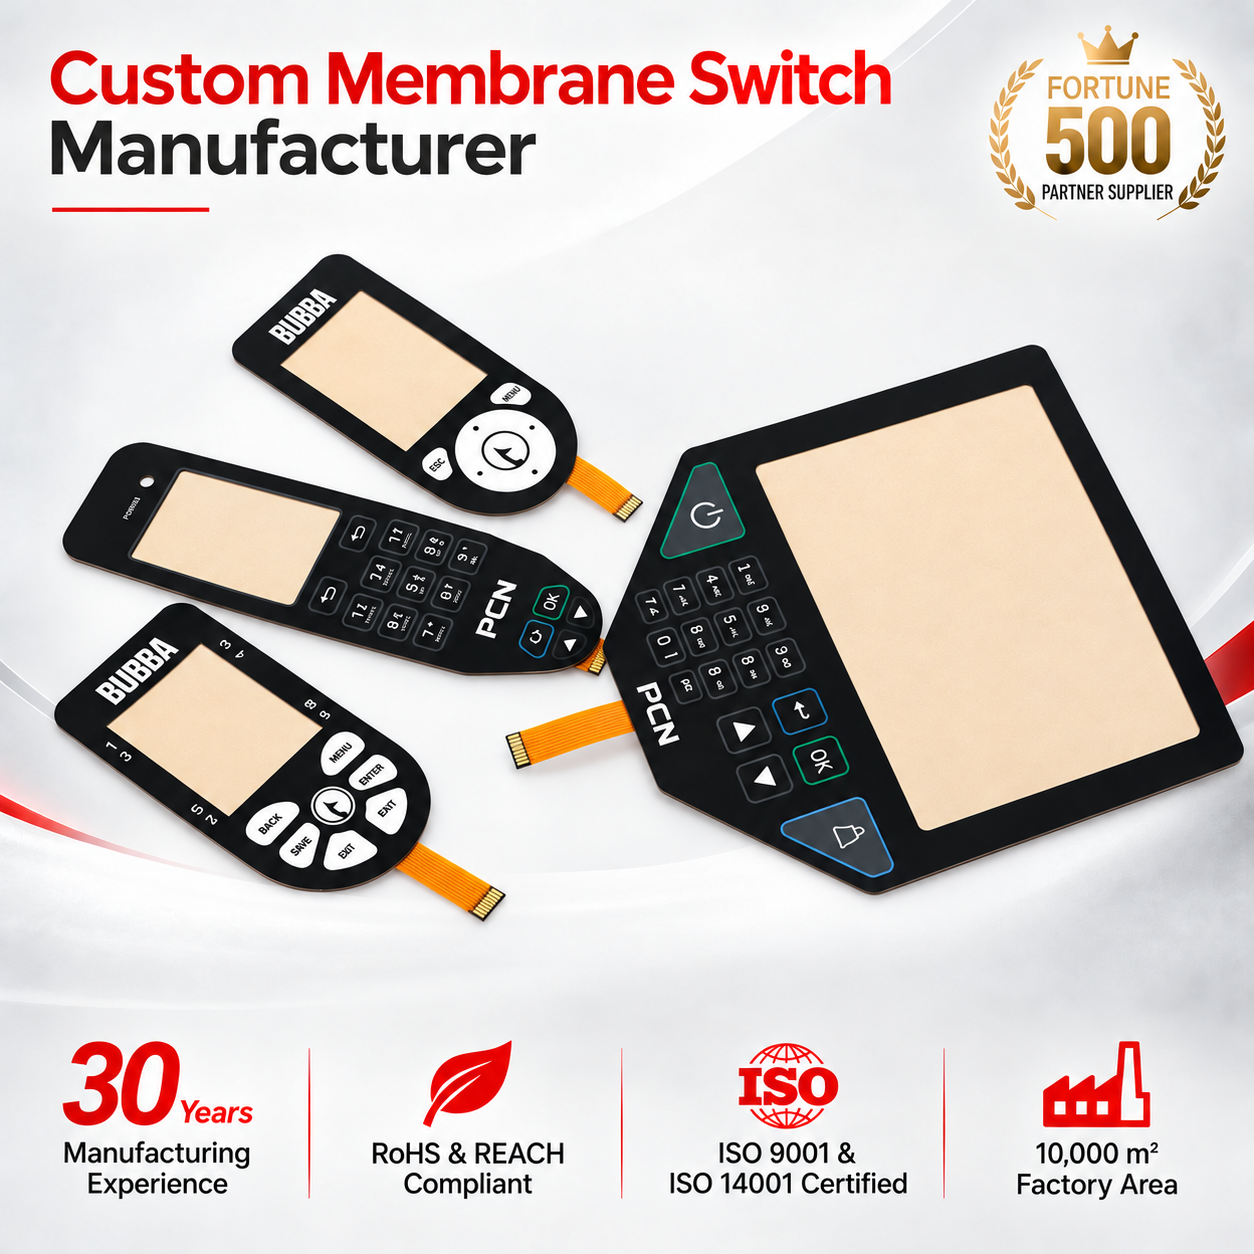
Tactile Metal Dome Graphic Overlay (3M™ Backing)
- Actuation Force280g – 420g Crisp Click Feedback
- Adhesive Layer3M™ 300LSE for LSE Plastics
- Contact MaterialNickel/Gold Plated Stainless Steel
1. Technical Specification: Engineering Keyboard Overlays for Maritime & Tropical Environments
In industrial human-machine interfaces (HMI), the keyboard overlay is the primary physical interface between human operators and mission-critical hardware. When serving operating environments like Nadi, Fiji—the aviation, logistics, and tourism nexus of the South Pacific—standard consumer-grade membrane materials fail catastrophically. The confluence of ambient maritime salt mist (NaCl aerosol), sustained relative humidity hovering between 78% and 94%, intense tropical ultraviolet irradiation (UV Index often peaking above 11+), and aggressive chemical washdowns used in food sanitation and aviation maintenance requires specialized polymer engineering.
As an ISO-certified, Fortune 500-qualified manufacturing partner, Dongguan AXRU Electronics Co., Ltd. provides customized keyboard overlays engineered down to the molecular layer. The performance of a front panel control system relies upon a harmonized stack-up of graphic foils, graphic inks, spacer layers, circuit traces, tactile domes, and structural pressure-sensitive adhesives (PSA).
"Failure in high-humidity maritime regions like Nadi rarely begins at the surface—it originates through capillary moisture ingress at the adhesive perimeter, leading to silver migration across circuit traces or delamination of poorly matched PET-to-acrylic bonds under high UV exposure."
| Material / Component | Autotex® XE Polyester (PET) | Lexan™ 8010 Polycarbonate (PC) | Silicone Elastomer Matrix | Acrylic Front Plate (PMMA) |
|---|---|---|---|---|
| Primary Utility | Extreme duty, chemical & UV flex fatigue | High optical clarity, rigid gauge windows | Deep mechanical travel, tactile washdown | Display protective lenses, touch capacitive |
| Flex Fatigue Life | > 5,000,000 switch cycles | Approx. 100,000 switch cycles | > 1,000,000 cycles | Static (Non-flexing structural window) |
| UV Radiation Resistance | Exceptional (Weatherable XE formulation) | Moderate (Prone to yellowing without coating) | Outstanding natural UV inertness | High natural optical transmission & UV inertness |
| Chemical / Solvent Resistance | Alcohols, Ketones, Diesel, Saline Sprays | Moderate; sensitive to aromatic hydrocarbons | High resistance to greases and mild detergents | Resistant to cleaning solvents; scratch susceptible |
| Operating Temperature | -40°C to +85°C | -40°C to +105°C | -50°C to +180°C | -20°C to +70°C |
For engineering teams developing terminals for the Nadi market, the specification choice between Autotex® XE biaxially oriented PET and Lexan™ PC is foundational. Lexan™ offers optical depth and high tensile impact resistance, making it an excellent candidate for static dead-front panels, display bezels, and indoor electronic housings. Conversely, Autotex® XE PET features an engineered UV-cured hardcoat chemically bonded to the polyester base. This chemical barrier prevents embrittlement and micro-cracking caused by equatorial sun exposure while enabling high-definition pillow, perimeter, or dome embossing that withstands millions of tactile cycles without fatigue.
2. Localized Application Scenarios Across Nadi and the Western Division of Fiji
Nadi is not merely a world-renowned tropical resort destination; it is the economic engine of Western Viti Levu, housing Nadi International Airport (NAN), the Civil Aviation Authority of Fiji (CAAF), heavy transport hubs connecting Lautoka's commercial shipping port, the sugar refining belt, and luxury resort infrastructures across Denarau Island. In each of these operational environments, HMI keyboard overlays must operate uninterrupted under extreme physical constraints.
Aviation Ground Support Equipment (GSE) & ATC
Nadi International Airport relies on baggage handling systems, pushback tractor controls, aircraft ground power units (GPU), and outdoor mobile refueling terminals. Overlays require IP67 perimeter sealing, high-visibility anti-glare finishes, and immunity to jet fuel (Jet A-1) and hydraulic fluid spills.
Marine, Denarau Marina & Port Infrastructure
Operating near Port Denarau and Nadi Bay exposes bridge controls, superyacht tender consoles, desalination pump controllers, and fish handling cold-chain monitors to continuous salt fog. We deploy 3M™ 300LSE adhesive with perimeter potting to block sodium chloride crusting and contact corrosion.
Resort Automation, POS & Commercial Kitchens
Luxury resorts across the Mamanuca archipelago and Nadi coastline run 24/7 HVAC automation, laundry machines, commercial ovens, and outdoor pool chlorination systems. Overlays feature antimicrobial hard-coats that endure heavy biocidal washdowns and humidity without graphic fading.
Beyond tourism and aviation, Nadi acts as the procurement gateway for agro-industrial infrastructure, including sugar cane processing electronics, beverage bottling facilities, and remote solar micro-grid monitoring stations across the outer islands. Solar inverters deployed under direct sun exposure in Fiji experience housing temperatures up to 65°C combined with humid air. Our engineered overlays integrate micro-venting Gore® membranes or dual-perimeter channel adhesives that equalize internal atmospheric pressure during day-to-night thermal cycling without admitting tropical rain or vapor condensation.
3. Technology Trends Driving HMI Procurement in the Nadi & Pacific Island Markets
The regional market across Fiji and neighboring Pacific island nations (Vanuatu, Samoa, Tonga) is transitioning away from electro-mechanical toggle switches and unsealed modular keypads toward fully enclosed, hygienic, and intelligent surface controls. Several structural trends characterize this modernization wave:
Capacitive Touch Overlays
Transition from physical tactile travel to solid-state capacitive sensing beneath 2mm tempered glass or acrylic. Elimination of mechanical gaps entirely stops ingress of tropical moisture, dust, and insects.
Anti-Microbial Nanocoatings
Silver-ion embedded top hardcoats deployed across medical diagnostic units and commercial food service front panels in resorts, inhibiting bacterial reproduction by 99.9% over extended operational lifespans.
Optically Clear Adhesive Lamination
OCA lamination of graphic overlays directly to OLED and TFT displays. By eliminating air gaps, sun reflections are drastically reduced, delivering critical daylight readability for marine deck equipment.
Ultra-Rugged P+R Silicone Keypads
Plastic keycap + Rubber base (P+R) designs combining the pleasant aesthetic of hard plastic keys with the hermetic sealing and tactile snap of a compression-molded silicone elastomer membrane.
Furthermore, local procurement managers in Nadi are increasingly prioritizing sustainable supply chain lifecycles. Rather than importing low-grade replacement switches every 12 to 18 months, engineering directors at large resorts and industrial sites are standardizing on automotive-grade overlay specifications that guarantee 5 to 7 years of field service life, radically lowering total cost of ownership (TCO).
4. Manufacturing Authority: Why OEM Buyers Choose Dongguan AXRU Electronics Co., Ltd.
When contracting keyboard overlay and membrane switch production, OEM purchasers require demonstrable technical authority, scalable floor capacity, and indisputable testing verification. Headquartered in the global electronics center of Dongguan, China, AXRU Electronics operates a comprehensive 10,000㎡ manufacturing plant verified on-site by Intertek. We do not broker production; all core manufacturing—from Class 10,000 cleanroom silkscreen printing to automatic metal-dome sorting, laser die-cutting, and 100% automated electrical continuity testing—is handled within our own facility.
Our in-house reliability laboratory simulates every stress vector that hardware will encounter in coastal Pacific deployments like Nadi. Before any mass-production shipment departs our factory gates, production lots undergo validation on specialized analytical test rigs:
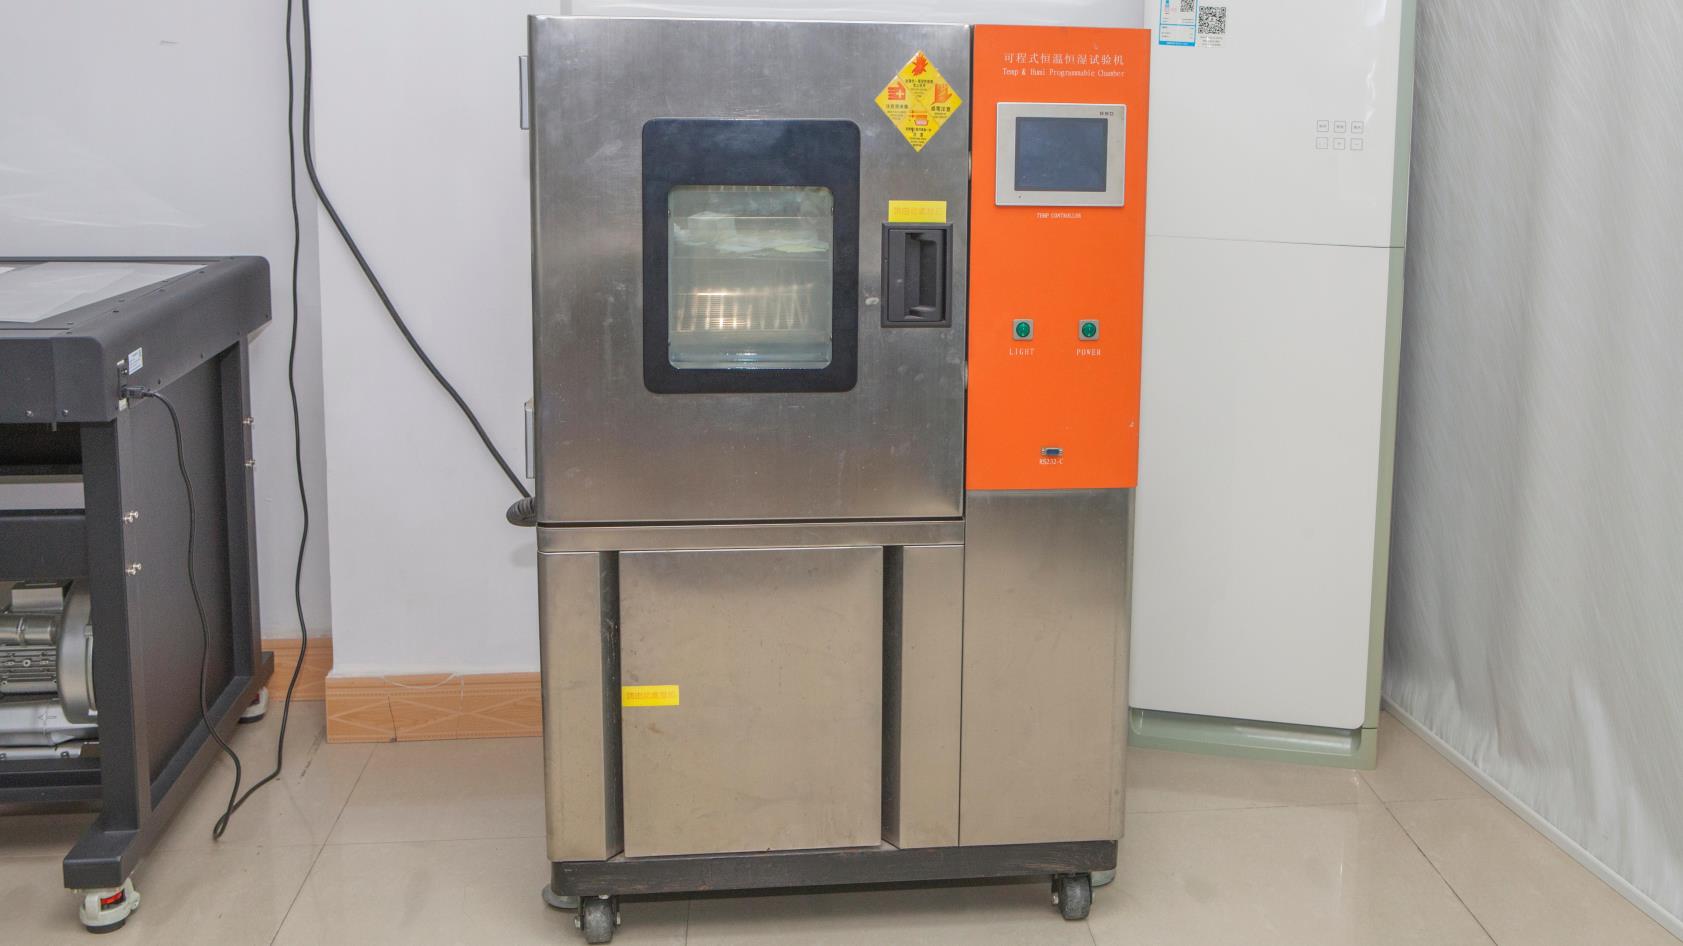
Programmable Temp & Humidity Chamber
Cycles overlays through -40°C to +150°C and up to 98% RH to guarantee zero adhesive delamination or silver trace corrosion under sustained tropical conditions.
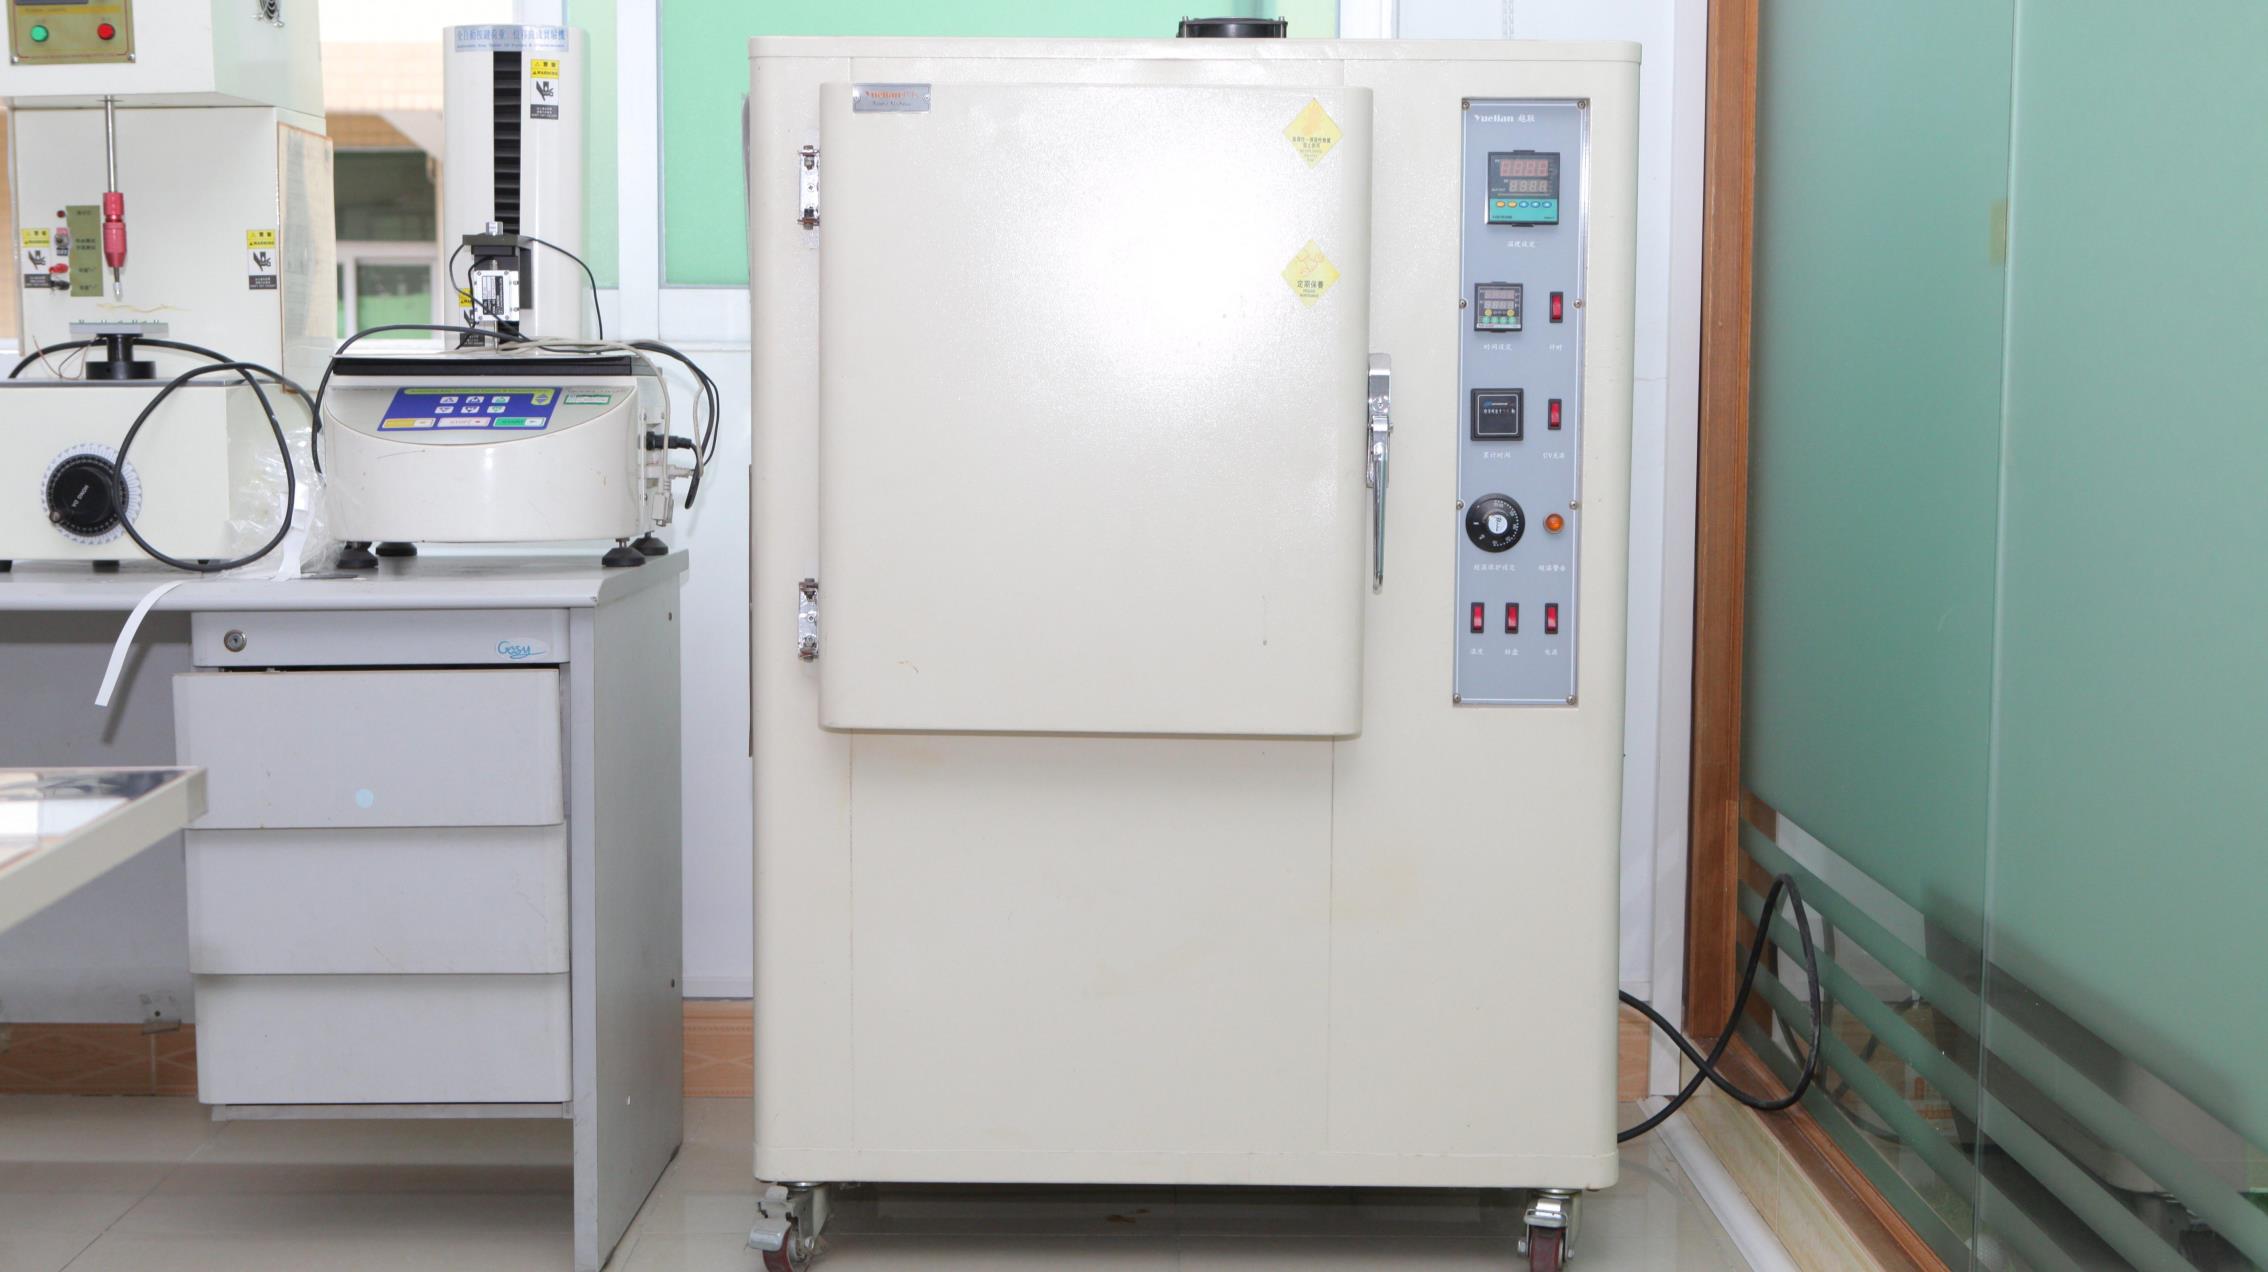
UV Yellowing Resistance Chamber
Accelerated solar spectrum UV radiation chamber validating that inks, clear display windows, and textured PET hardcoats remain non-yellowing and legible.
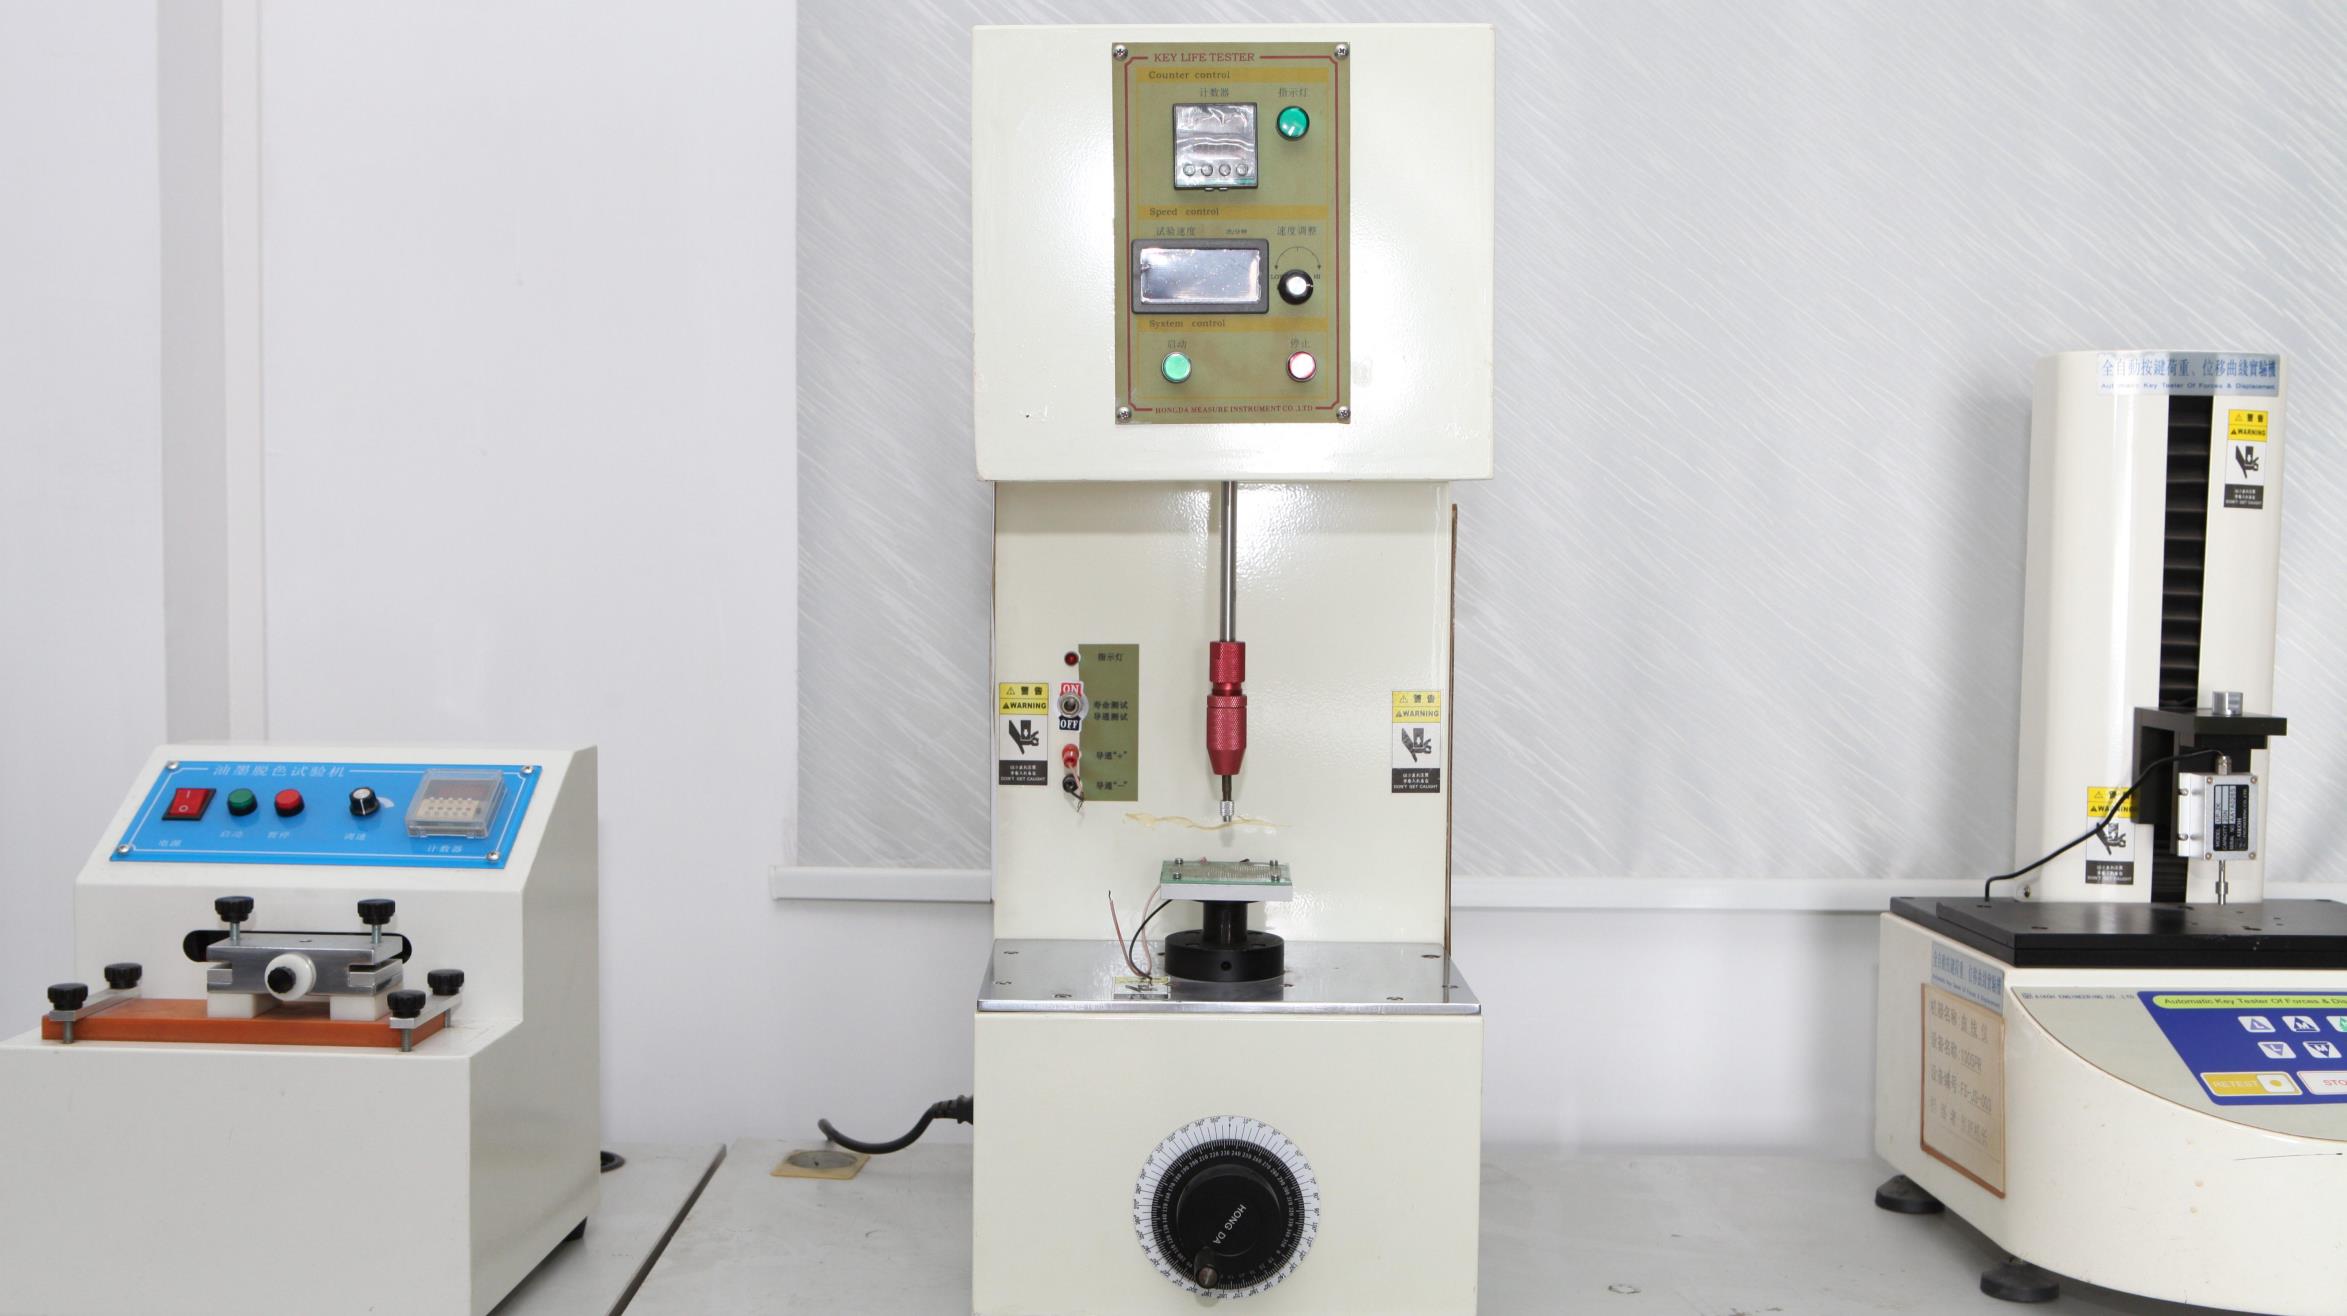
Pneumatic Key Life Actuation Tester
Repetitive mechanical cycling of metal domes and embossed buttons at up to 5 strokes per second to confirm tactile snap retention past 1 to 5 million cycles.
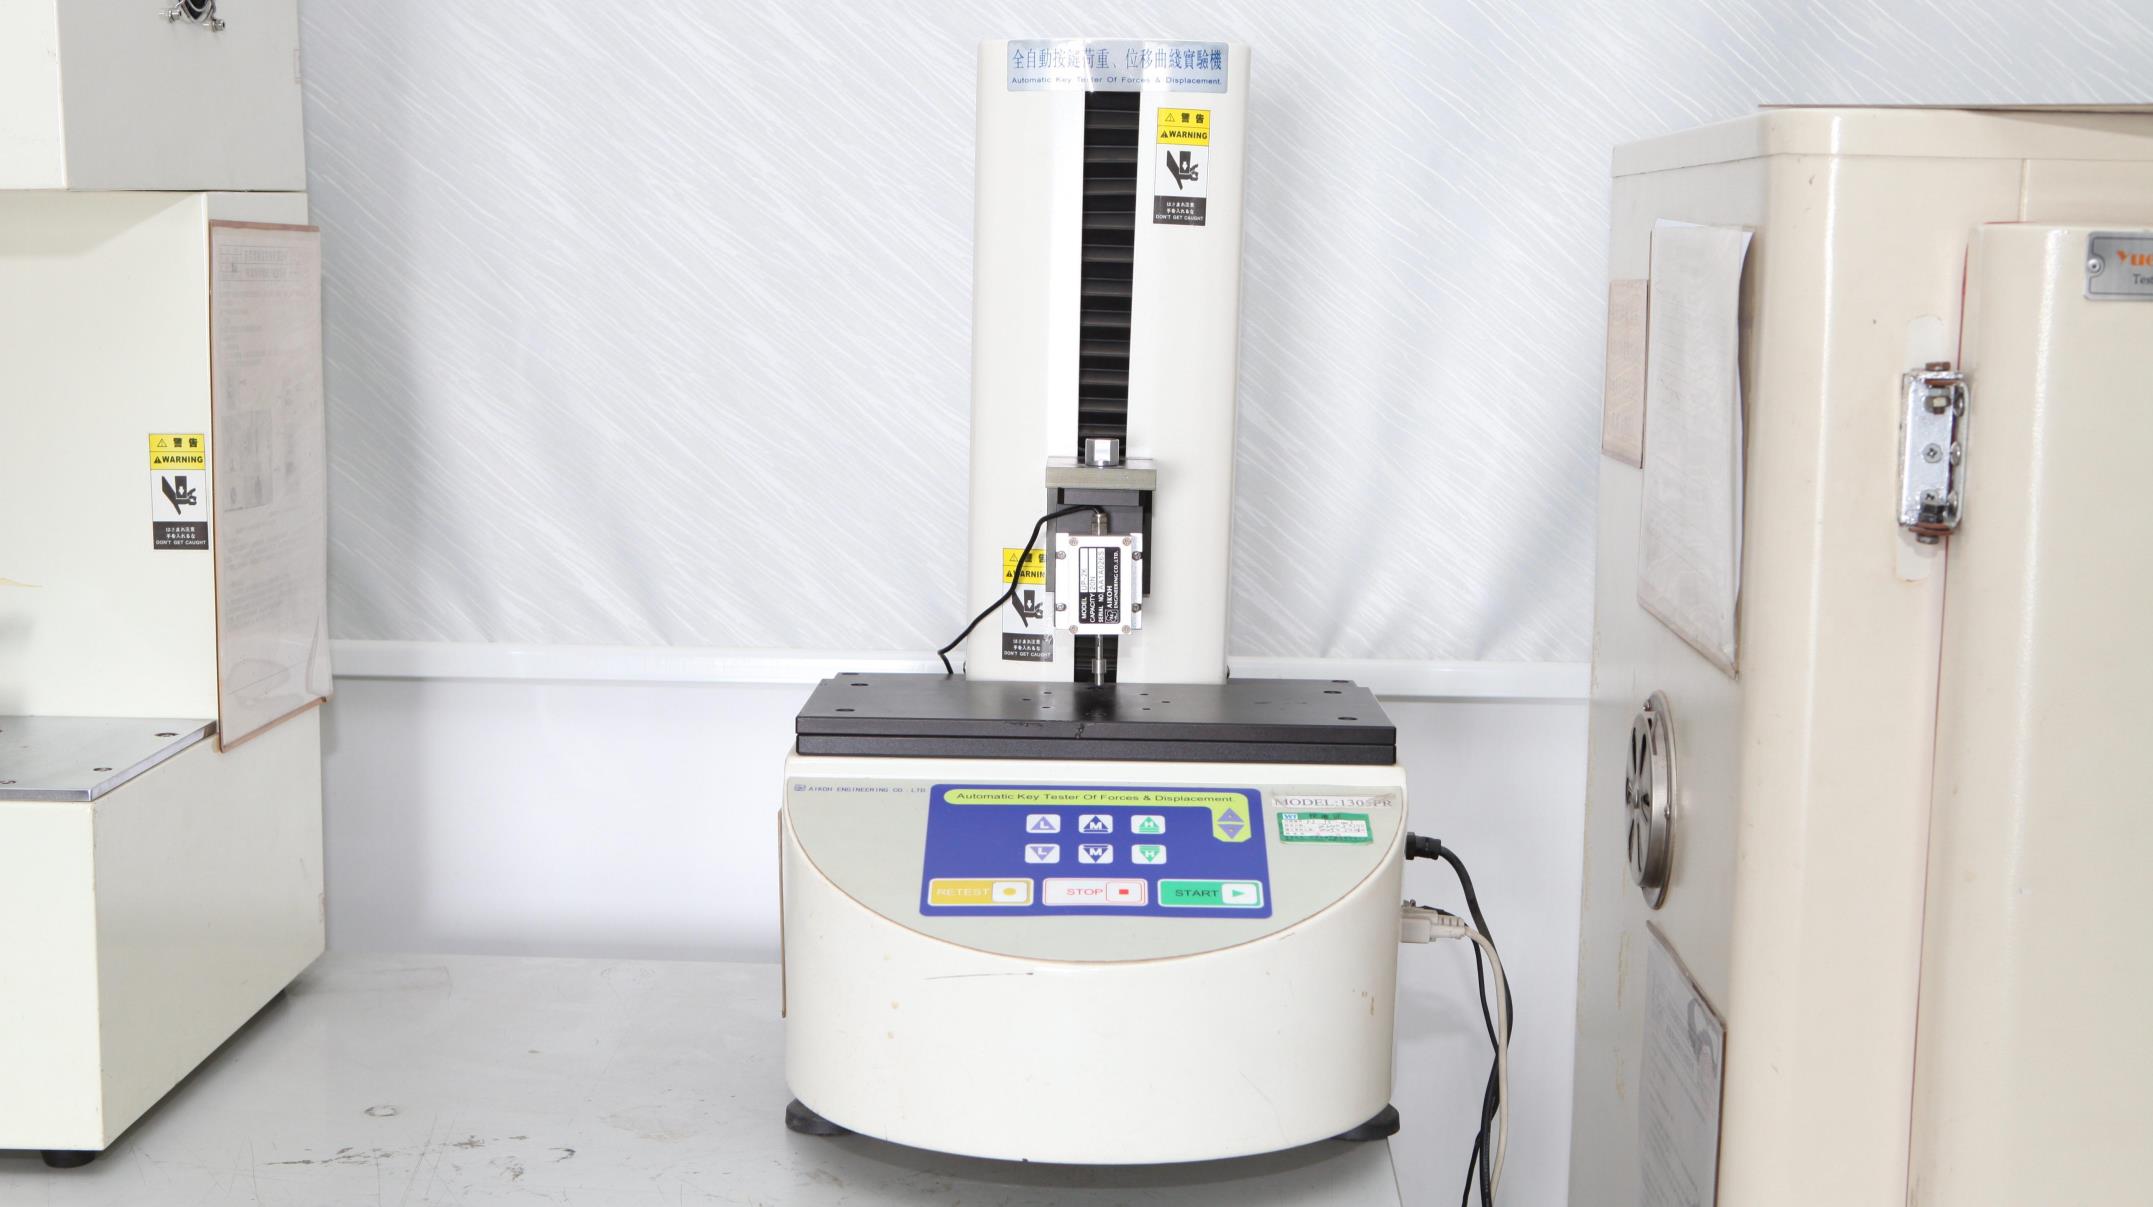
Force & Displacement Curve Plotter
Precise mapping of switch actuation force, tactile ratio, return force, and travel depth to ensure consistent click feel across multi-key panels.
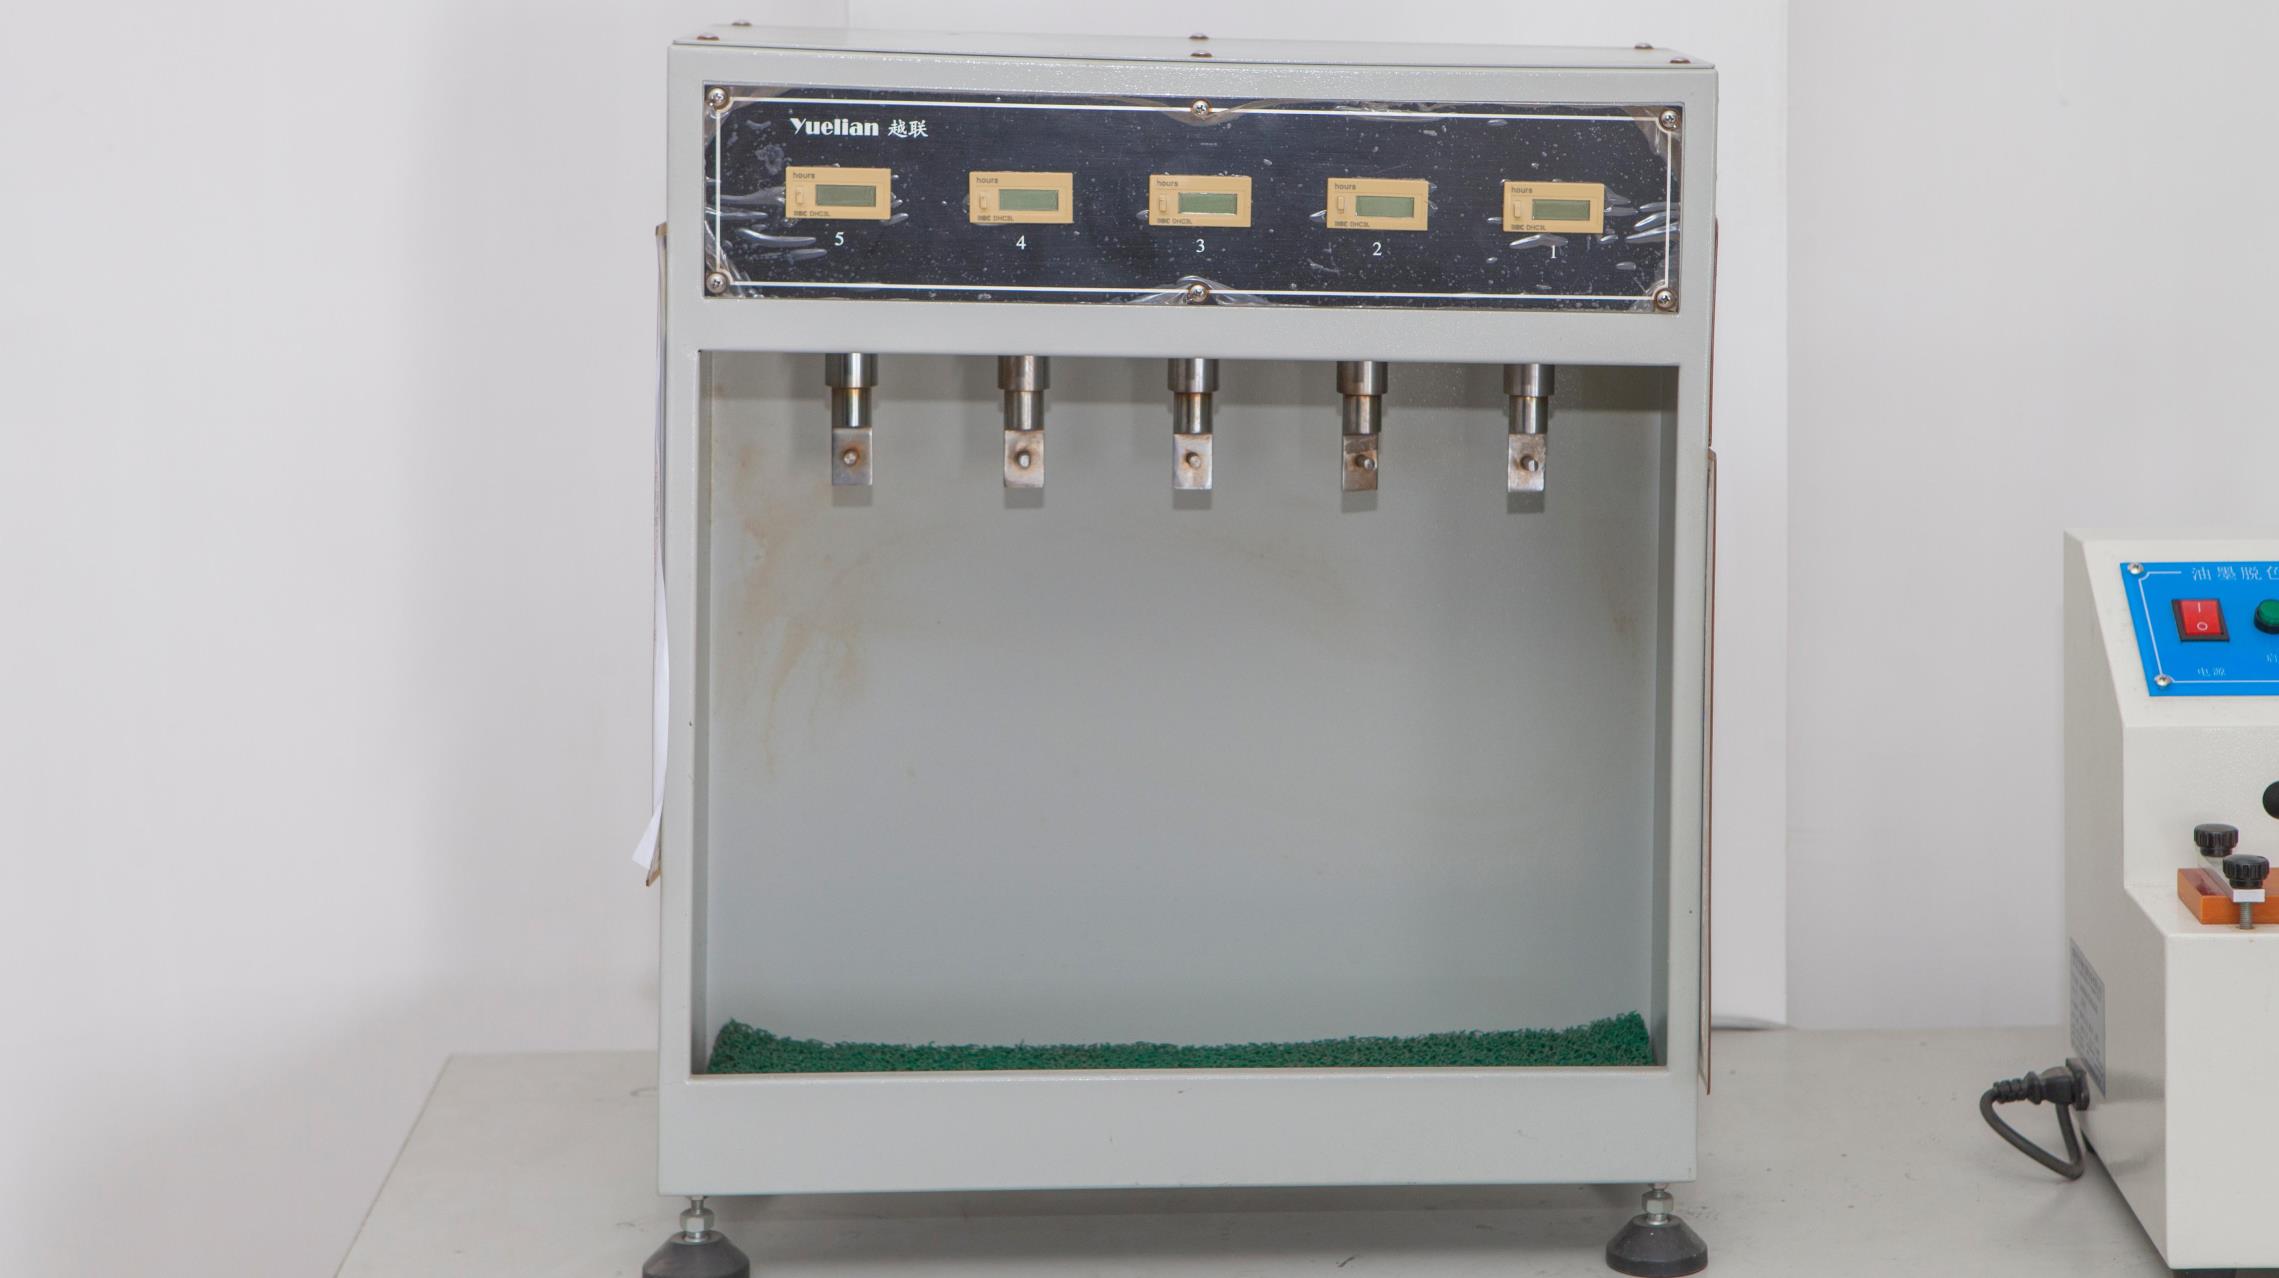
Adhesive Peel & Tensile Tester
Verifies 90° and 180° peel adhesion of 3M™ transfer tapes to aluminium, stainless steel, polycarbonate, and powder-coated cast enclosures.
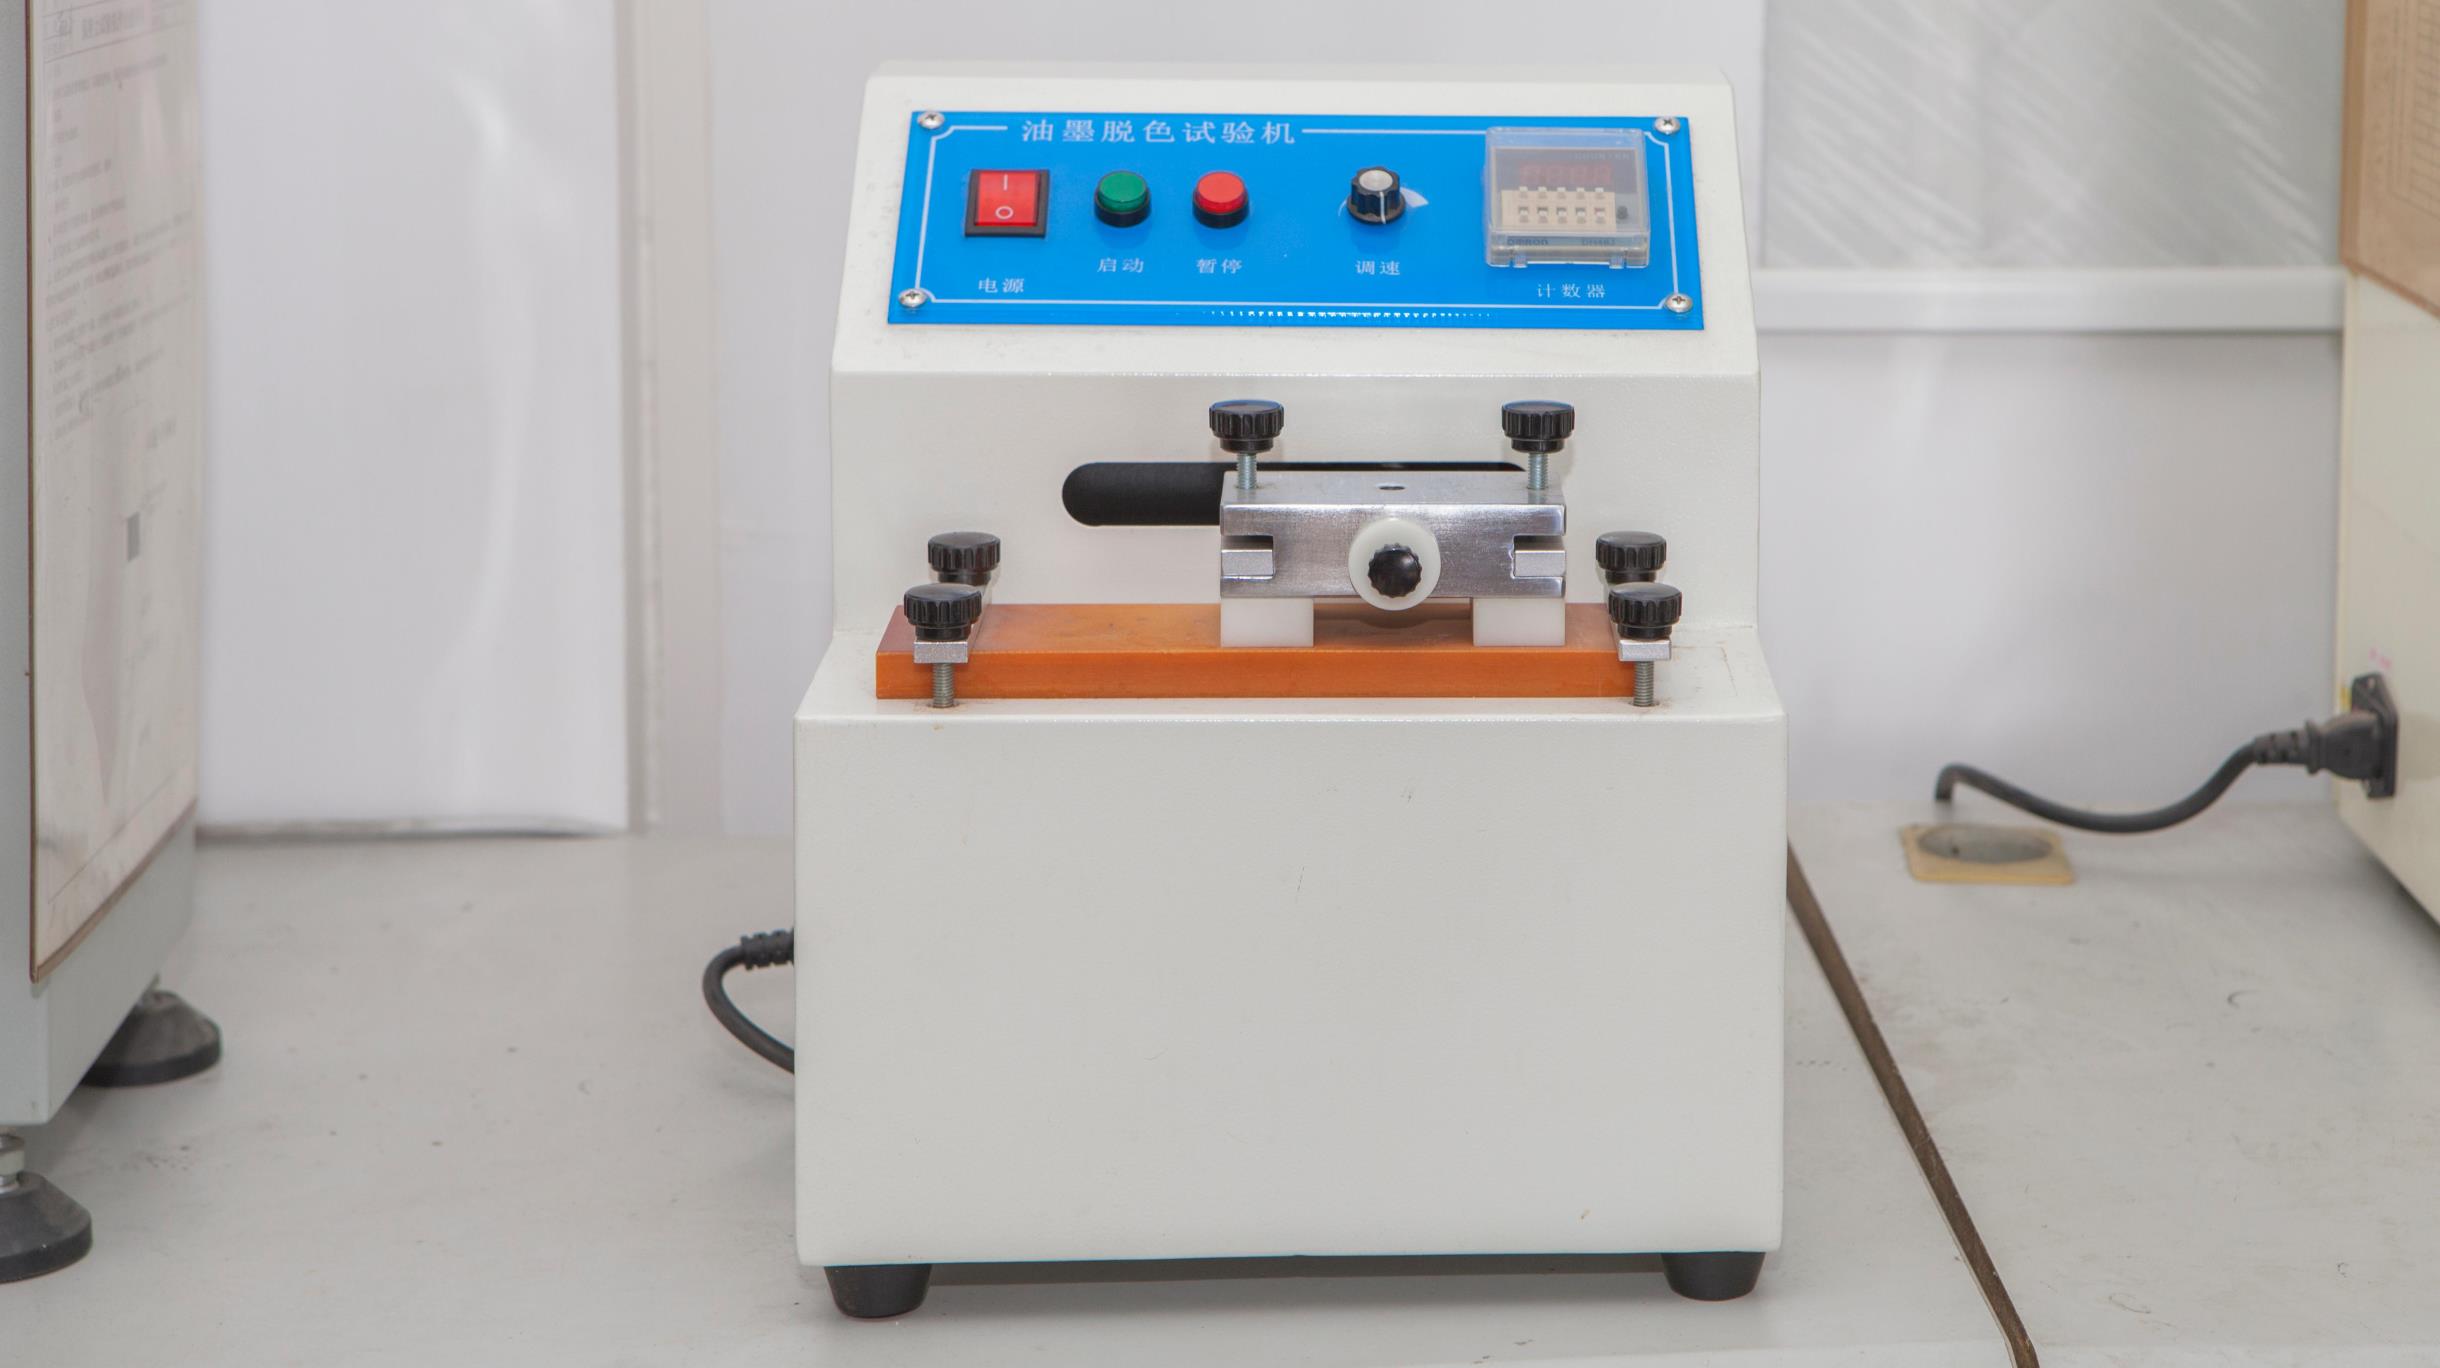
Solvent & Abrasion Rub Tester
Tests surface graphics against alcohol, MEK, bleach, and artificial perspiration rubs to guarantee legends never erase during intensive industrial washdowns.
With our engineering team directly reviewing your CAD drawings, stack-up thicknesses, tail pitches, and electrical pinouts, we provide rapid Design for Manufacturing (DFM) feedback within 24 hours. Whether you require rapid prototyping of 10 samples for pilot verification in Nadi or 50,000 units for OEM production, AXRU provides factory-direct transparency, competitive pricing, and rigorous quality assurance.
5. Frequently Asked Questions for Nadi & Pacific Regional Procurement
Common engineering, logistics, and supply chain queries encountered when specifying and purchasing custom keyboard overlays and membrane panels for Fiji deployments:
Partner with an Established Keyboard Overlay Manufacturer for Nadi Projects
Consult directly with our HMI project engineers. Submit your engineering drawing or component sample today for a complimentary DFM analysis, material stack-up recommendation, and firm factory quotation within 24 hours.