Tactile Keypad
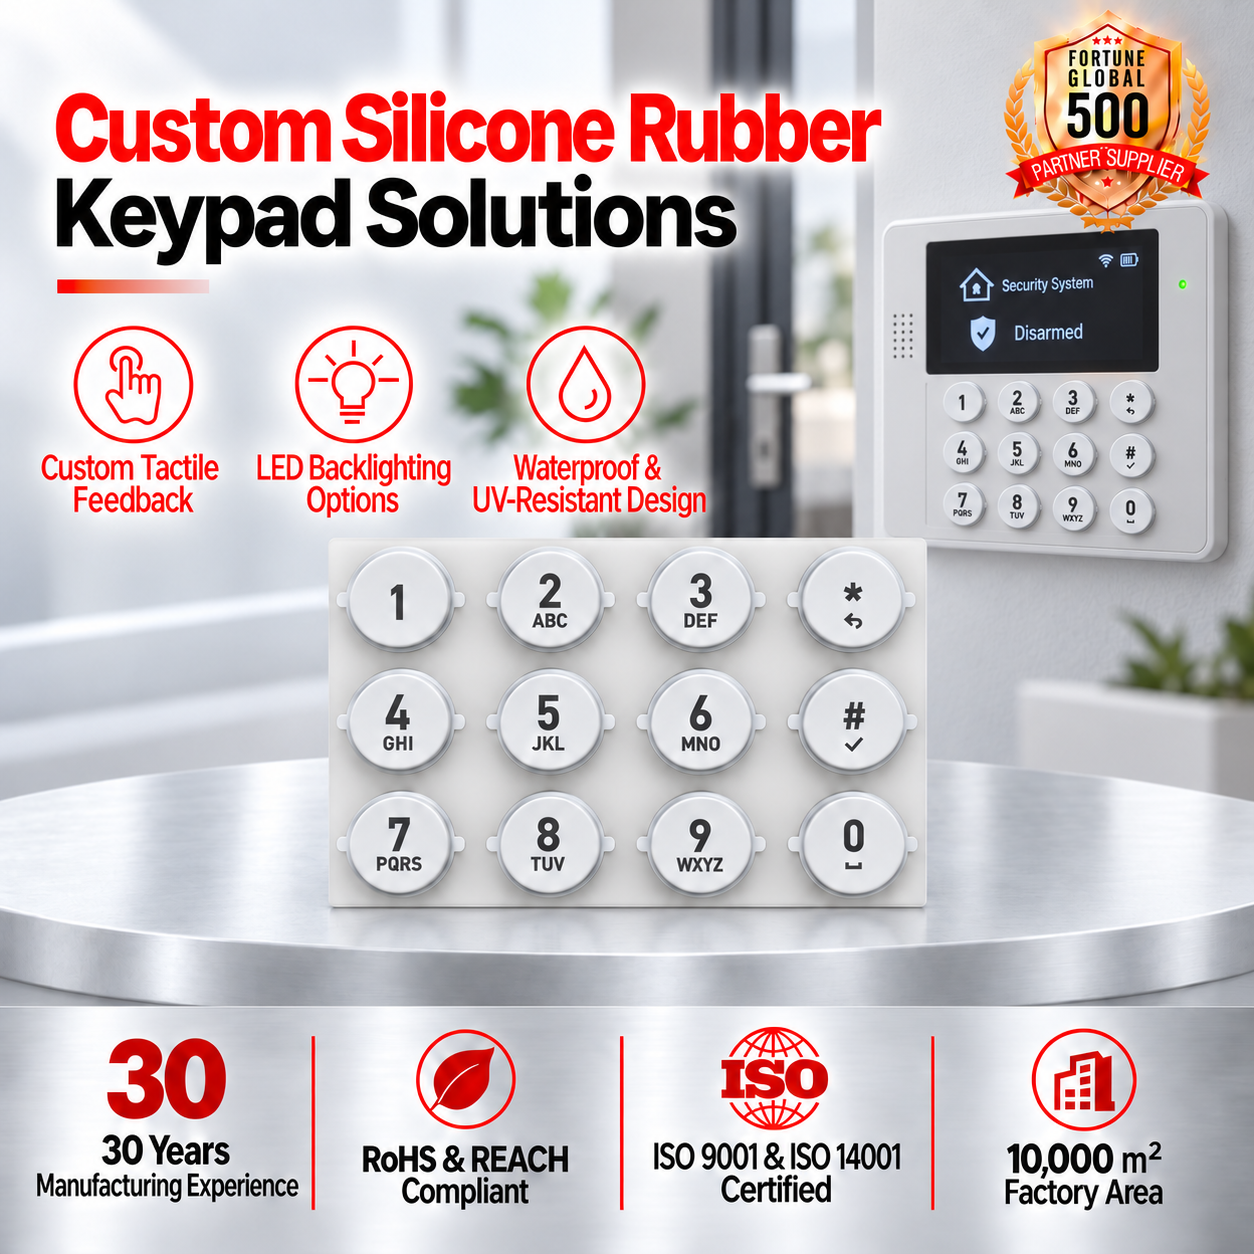
Custom OEM Silicone Rubber Keypad 3x4 Numeric 12 Keys Round Plastic Button P+R
- Key Travel: 0.8–1.5 mm
- Contact Pill: Conductive Carbon
- Enclosure Fit: Plastic + Rubber (P+R)
Engineered for seamless integration with precision injection molding enclosures, capacitive touch microcontrollers, and extreme environmental barriers. Recommended for OEM and ODM projects across the Republic of Moldova and the wider EU nearshoring corridors.
A technical evaluation of resin-film bonding dynamics, chemical barrier protection, and thermodynamic stability for precision electronics manufacturers supplying Eastern European and international markets.
In modern industrial electronics, equipment housings in Chișinău and throughout Moldova are evolving past traditional sheet-metal stampings and post-molding pad printing. Secondary surface finishing inevitably suffers from surface abrasion, solvent stripping, and environmental delamination when subjected to harsh agricultural oils, sanitizing chemicals, or outdoor thermal cycles. In-Mold Decoration (IMD), incorporating In-Mold Labeling (IML) and In-Mold Electronics (IME), resolves these failure mechanisms by encapsulating graphic inks and conductive traces permanently between a resilient polymeric film and an injection-molded structural thermoplastic core.
At Dongguan AXRU Electronics Co., Ltd., our engineering methodology treats the IMD front panel not as a decorative veneer, but as a multifunctional structural barrier. Utilizing premium optical-grade polycarbonate (PC), optical polymethyl methacrylate (PMMA), and bi-axially oriented polyester (PET) carriers, the visual graphics are reverse screen-printed inside cleanroom environments onto the second surface. During high-pressure thermoforming and secondary injection molding, the carrier foil fuses seamlessly with injected ABS, PC/ABS alloys, or polypropylene (PP). The ink system is locked inside the mold under precise melt-front velocities, eliminating paint degradation, scratch wear, and ink particulate emissions during long-term field operation.
Selecting the appropriate polymer blend represents the foundation of IMD structural longevity. For applications within Chișinău's industrial automation corridors, including sub-assembly plants within Free Economic Zone (FEZ) Bălți subzones, mechanical designers must match thermal expansion coefficients ($\alpha$) between the top film and the injected resin to avoid post-cooling warping:
| HMI Interface Metric | AXRU Precision IMD / IML | Conventional Membrane Switch | Standard Pad Printing / Silk Screen |
|---|---|---|---|
| Graphic Ingress Protection | Permanent encapsulation; ink on second surface cannot be scraped or scratched off | Protected beneath overlay film, relies on rim adhesive gaskets | Exposed on first surface; prone to scratching, wiping wear, and solvent attack |
| Dimensional Geometry | True 3D contours, compound curves, ergonomic recessing, and molded bosses | Predominantly flat 2D or limited 2.5D embossed bubble keycaps | Limited to flat or gently radiused rigid substrates |
| Chemical & UV Resilience | Tested to 500+ hours UV exposure (yellowing resistant); impervious to IPA/detergents | High with textured PET; vulnerable along exposed perimeter borders | Low; rapid fading, flaking, and abrasion degradation within 12–24 months |
| Integration of Light & Capacitive Touch | Integrated dead-front windows, light guide diffusers, and molded-in capacitive electrodes | Requires discrete SMD LEDs, fiber-optic layers, or external backlight guides | Requires auxiliary display modules, external bezels, and mechanical pushbuttons |
| Typical Mold Life / Part Lifecycle | Engineered for >500,000 shot mold tooling; part lifecycle matches host equipment (10+ yrs) | Die-cut tool life >100,000 hits; switch assembly life 1–5 million cycles | Tool wear negligible, but recurring manual print labor and high reject scrap rates |
Our engineering headquarters controls mold design, high-pressure forming die manufacture, and trim-die fabrication. We run advanced Moldflow simulations to calculate gate shear stress, melt temperatures, and shrinkage dynamics, preventing wash-out of screen-printed inks during injection cycles.
We formulate specialized semi-translucent translucent and tint inks engineered for dead-front indicator icons and display viewports. Icons remain invisibly dark until backlit by precision SMD LEDs, eliminating clutter and producing sleek modern control panels for medical and high-end automotive cockpits.
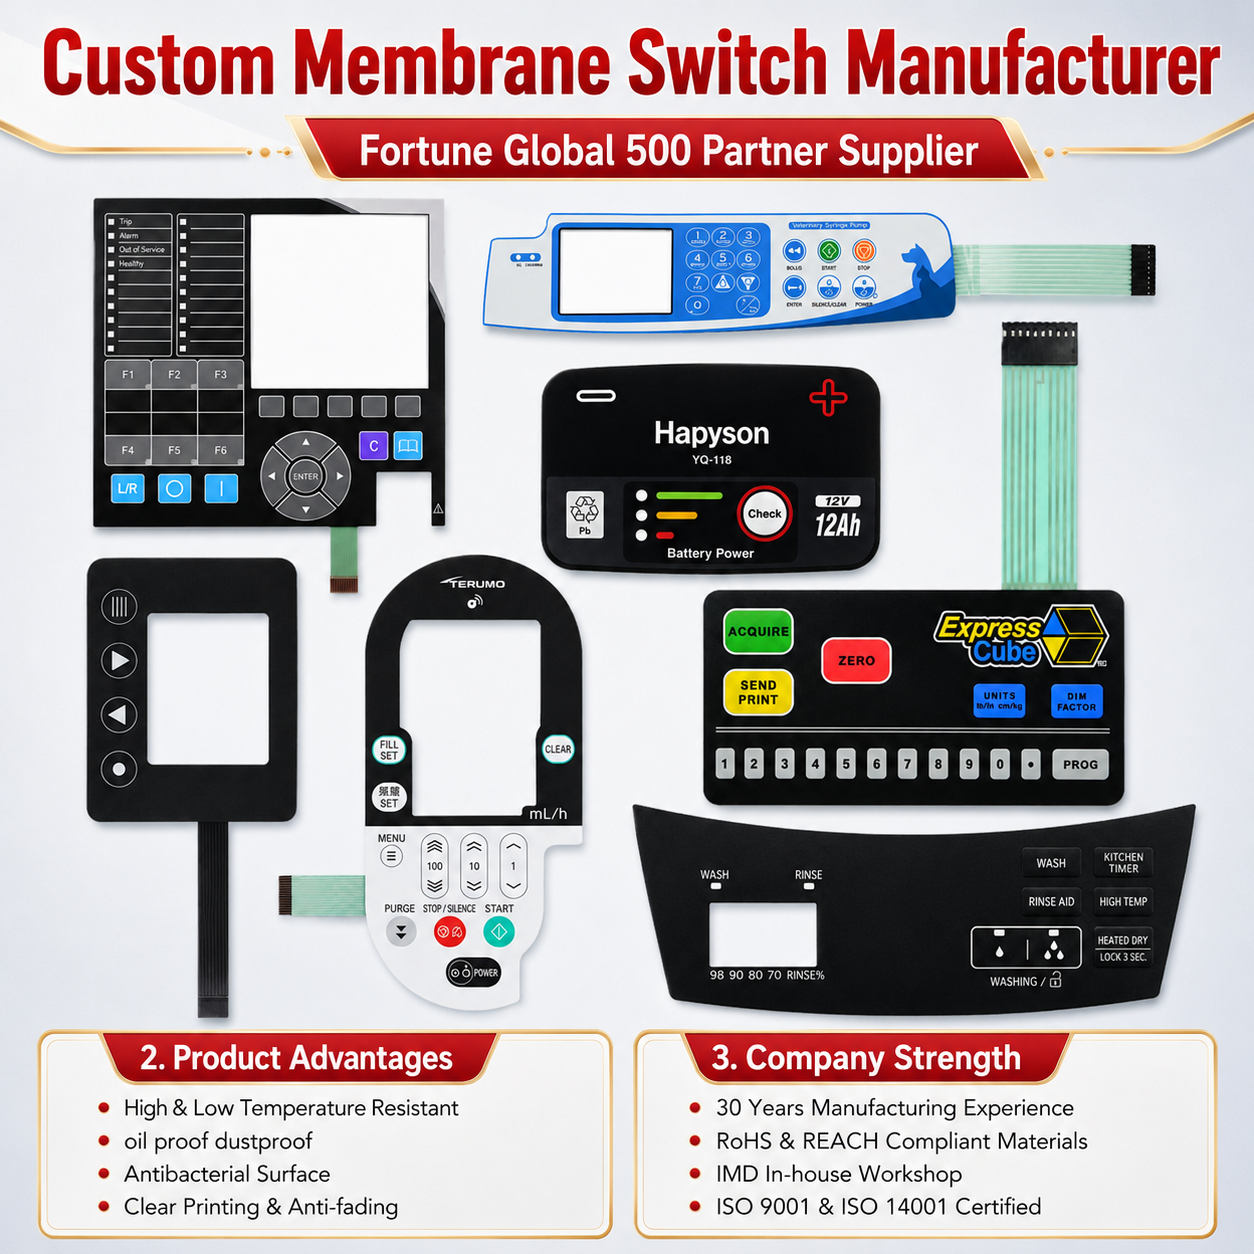
AXRU harmonizes IMD front foils with tactile metal domes (snap ratio >50%), conductive carbon elastomer membranes, or capacitive sensor films. This delivers crisp tactile feedback coupled with the clean, smooth aesthetics of an unbroken monolithic housing.
As the Republic of Moldova accelerates its integration into the European Union manufacturing supply chain, Chișinău has emerged as an agile center for automotive wire harnessing, electronic sub-assembly (EMS), intelligent metering, and agro-industrial machinery. Here is how AXRU's IMD and keypad solutions integrate directly with local production sectors.
Chișinău acts as a strategic manufacturing base for Tier-1 automotive cable and harness providers shipping into Romania, Germany, and Poland. Our IMD panels provide scratch-resistant, UV-stable gauge faceplates, center console buttons, and HVAC bezels tailored to ISO/TS automotive standards with flawless night-illumination balance.
Moldova's energy transition has stimulated localized manufacturing of smart electric meters, gas volume correctors, and water monitoring devices. We build rugged, IP67-sealed IMD front fascias with anti-tamper optical display windows that withstand continuous freeze-thaw cycles from -35°C to +75°C.
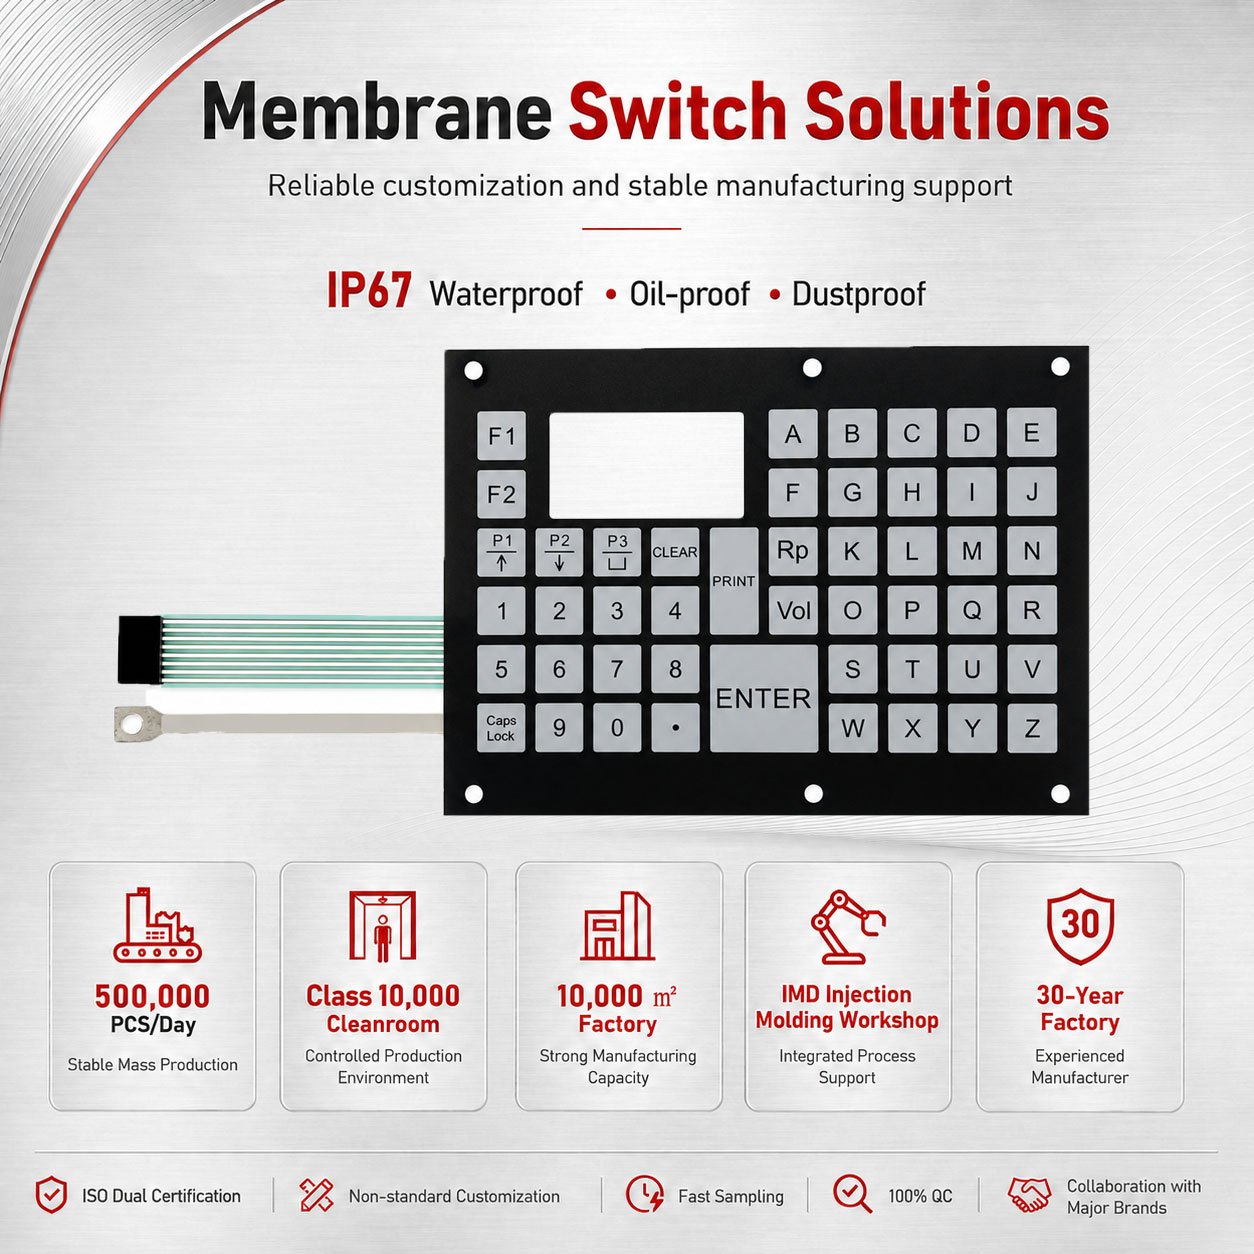
Surrounding Chișinău's wine, fruit processing, and grain processing infrastructure, automated packaging lines and tractors require HMIs impervious to moisture washdowns and organic acids. AXRU’s sealed membrane and IMD consoles eliminate food-trap crevices and withstand high-pressure water jets.
Expanding across municipal Chișinău and European transit corridors, modern AC and DC fast chargers demand vandal-proof IK08-IK10 front panels with integrated RFID reader zones and touchscreen overlays that remain responsive in damp or sub-zero operating environments.
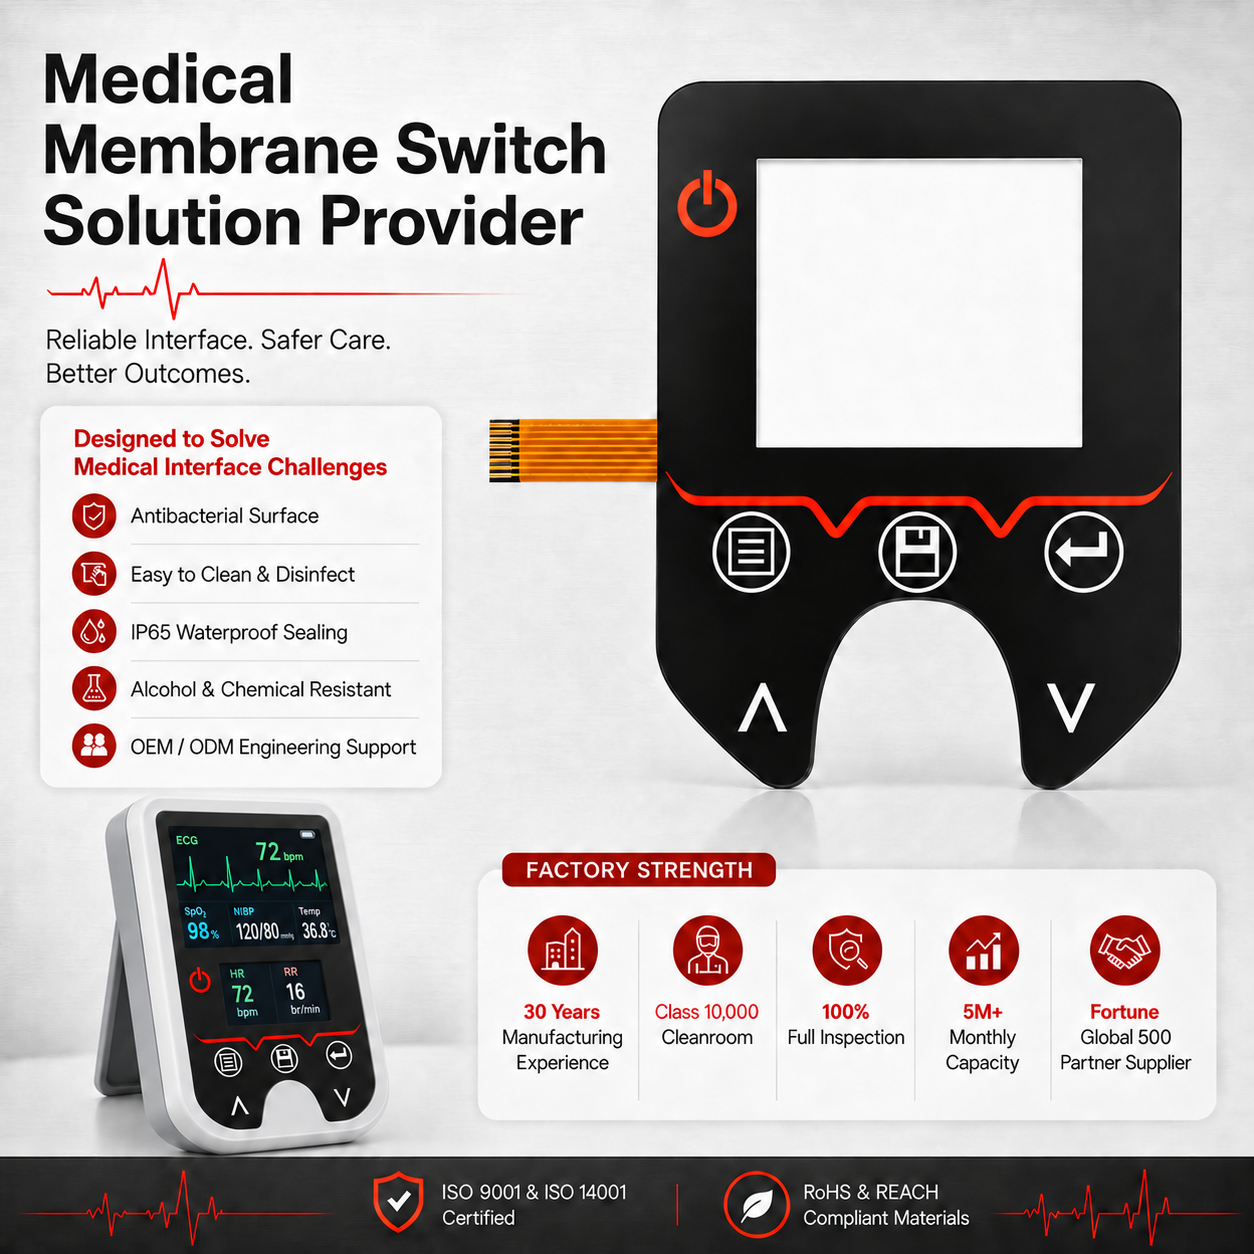
Medical equipment assemblers operating in the Chișinău area leverage our cleanroom-produced front overlays featuring antimicrobial textures. The surface resists harsh hospital chemical wipe-downs, sodium hypochlorite, and isopropyl alcohol disinfection protocols without ink hazing.
We provide streamlined air express (via Chișinău International Airport - KIV) and bonded multimodal freight (via the Black Sea Port of Constanța / overland road corridors). All documentation is formatted for straightforward customs clearance under Moldovan TARIC and CE declarations.
The transition toward smart connectivity, nearshoring resilience, and sustainable materials is reshaping how Moldovan purchasing directors select interface manufacturers.
Western European OEMs increasingly contract electronics manufacturing to Moldova. Sourcing IMD components with full RoHS, REACH, and UL94 compliance ensures zero regulatory frictions upon final export to DACH and EU markets.
Mechanical switches are giving way to capacitive touch sensors printed directly onto the IMD film with conductive silver traces. This shrinks enclosure thickness by up to 60% while eliminating mechanical contact wear.
Continental European climate extremes require automotive and utility panels to withstand intense UV exposure in summer and prolonged sub-zero temperatures in winter without crazing, peeling, or micro-cracking.
Chișinău product developers demand rapid pilot runs. AXRU’s dedicated sample-making line allows custom functional prototypes to be validated in days before opening high-volume multi-cavity injection tooling.
Operating a 10,000㎡ manufacturing plant assessed on-site by Intertek. Every stage—from film screen printing and dome array placement to environmental stress validation—is executed strictly in-house.
No outsourced core processes. Complete engineering control over yield, dimensional tolerances, and delivery dates.
Many suppliers broker orders across fragmented sub-tier workshops, resulting in inconsistent adhesive cure cycles, color mismatch across production batches, and disputed warranty liabilities. At AXRU Electronics, our 121-person workforce operates within an integrated manufacturing complex equipped with cleanrooms, flatbed CNC die-cutting, automated silk-screen printing presses, and an in-house reliability laboratory.
Our customers include Fortune 500 equipment builders and specialized industrial manufacturers worldwide. Every product shipped to Chișinău is accompanied by rigorous batch test certifications, covering electrical pin continuity, contact resistance, actuation force curves, and peel strength documentation.
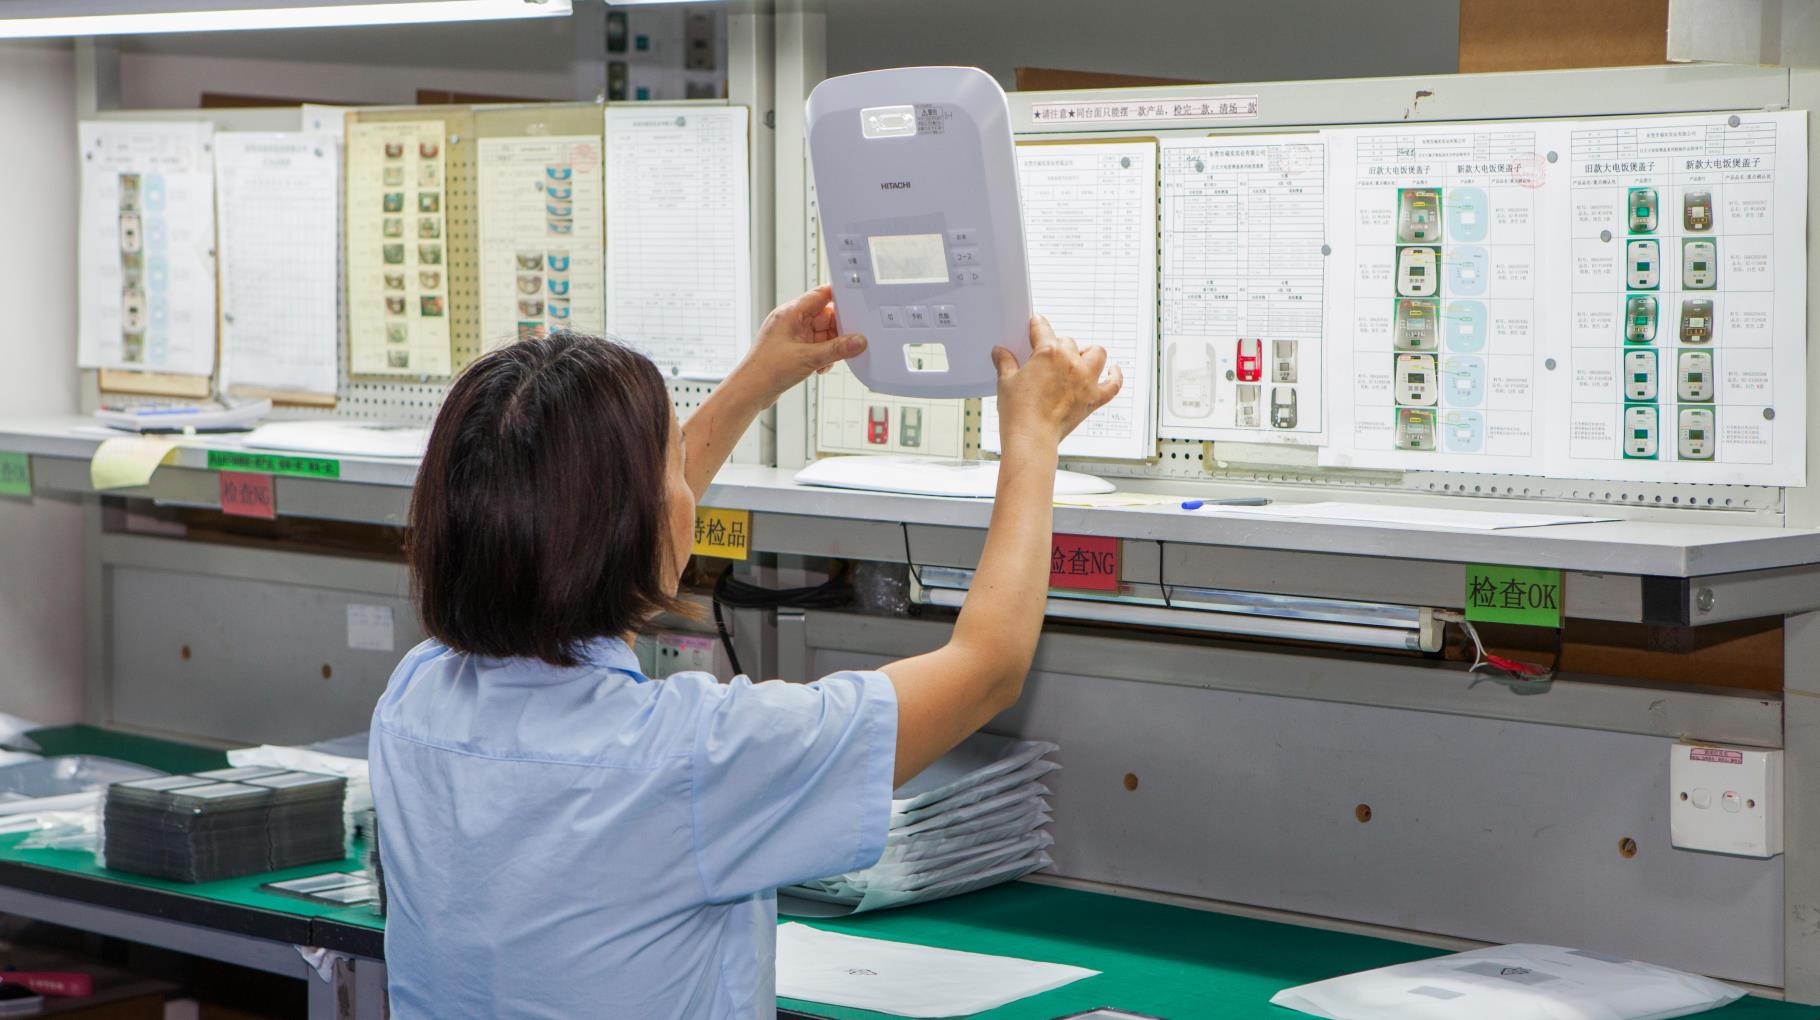
Every single membrane switch and IMD circuit is checked for continuity, insulation impedance (>100MΩ at 100V DC), contact resistance (<100Ω), and short circuits.
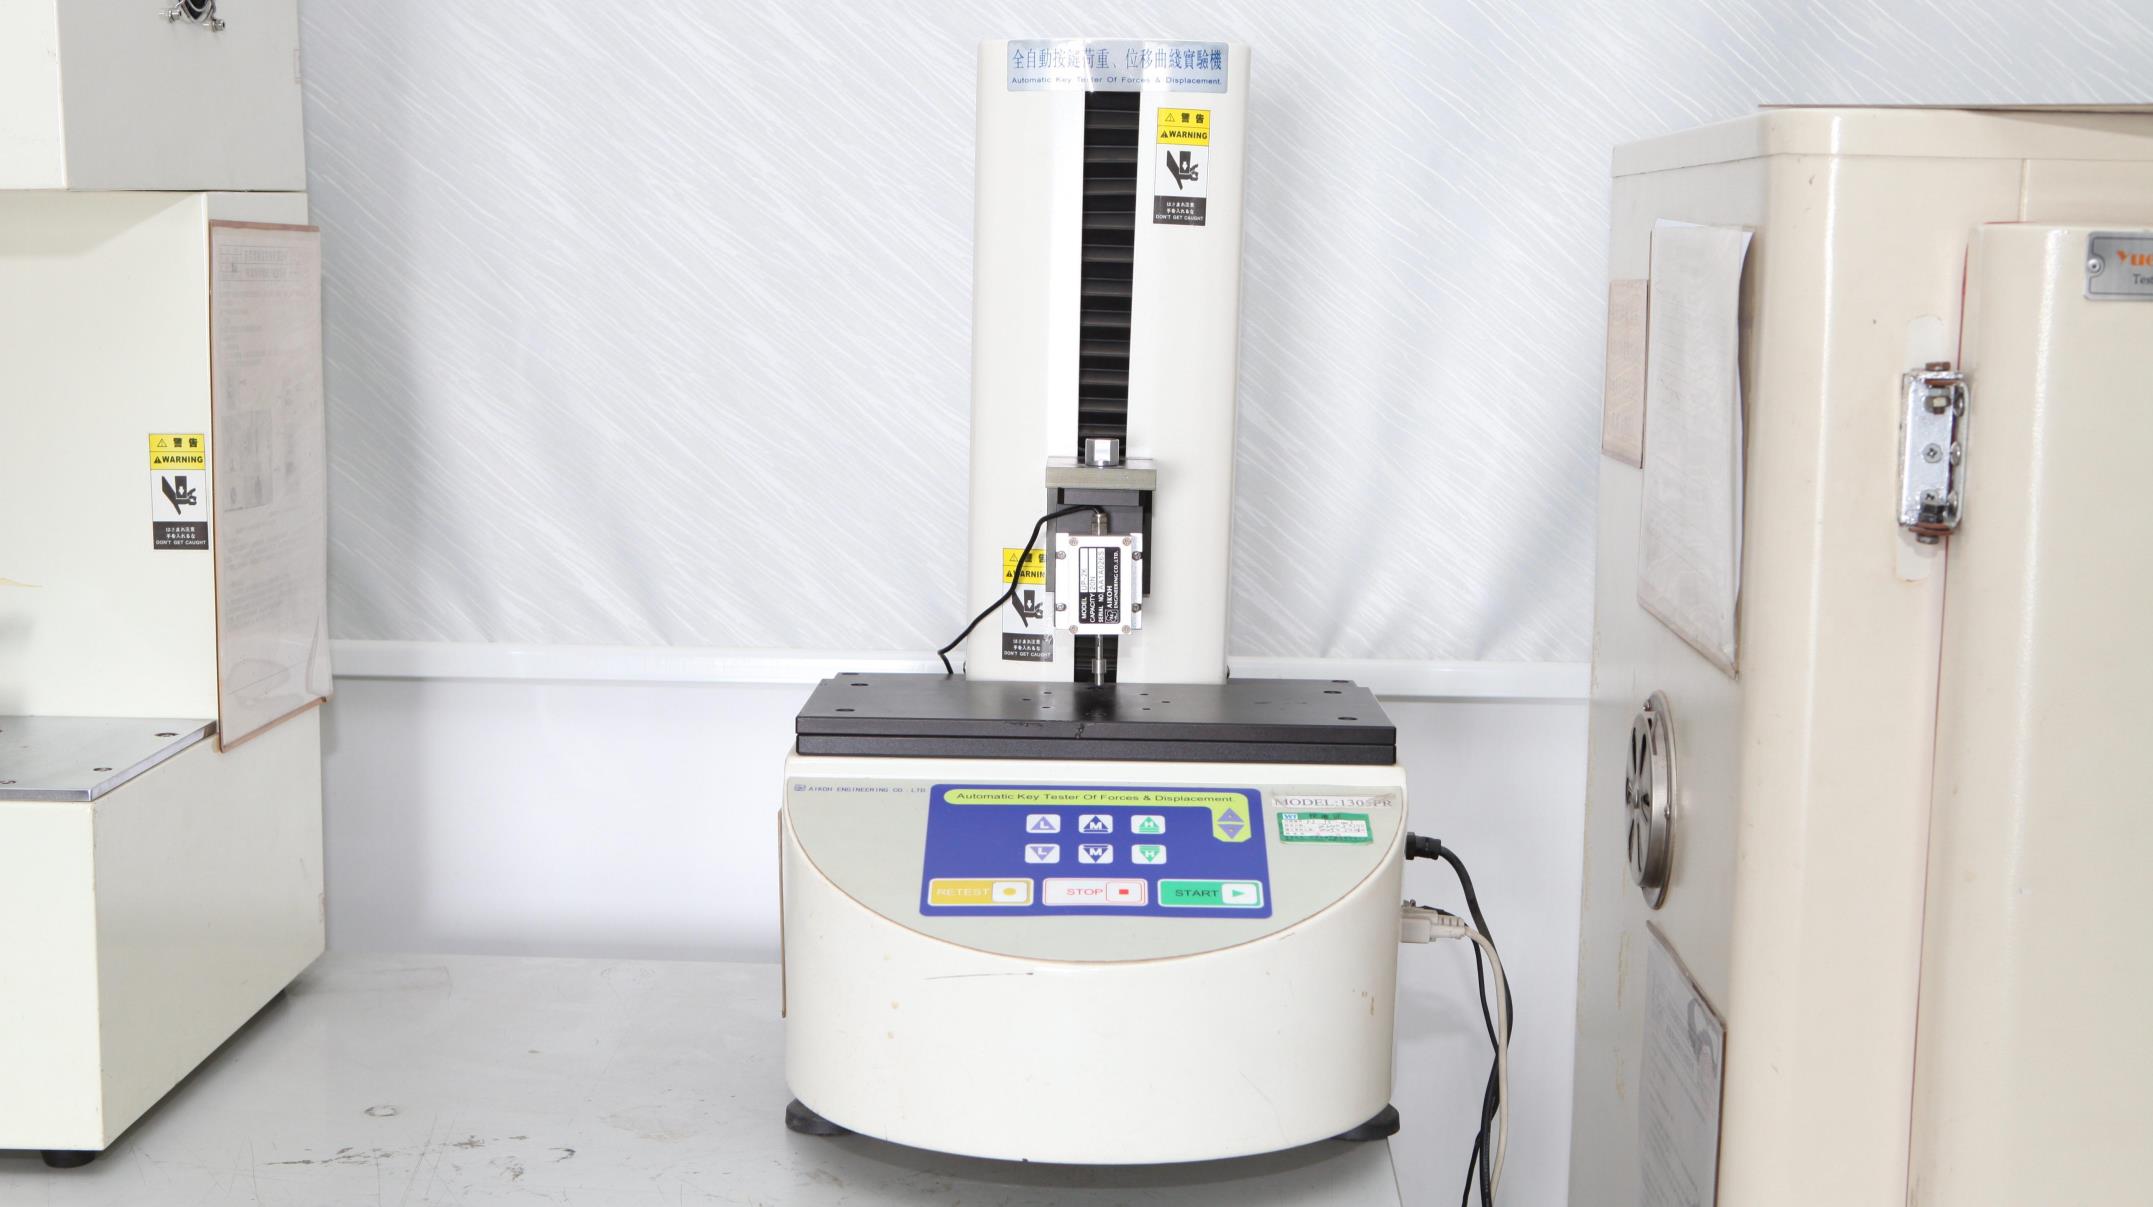
Automated stroke displacement probes plot actuation travel, peak tactile force, and release snap ratio to guarantee consistent tactile feel across all keypads.
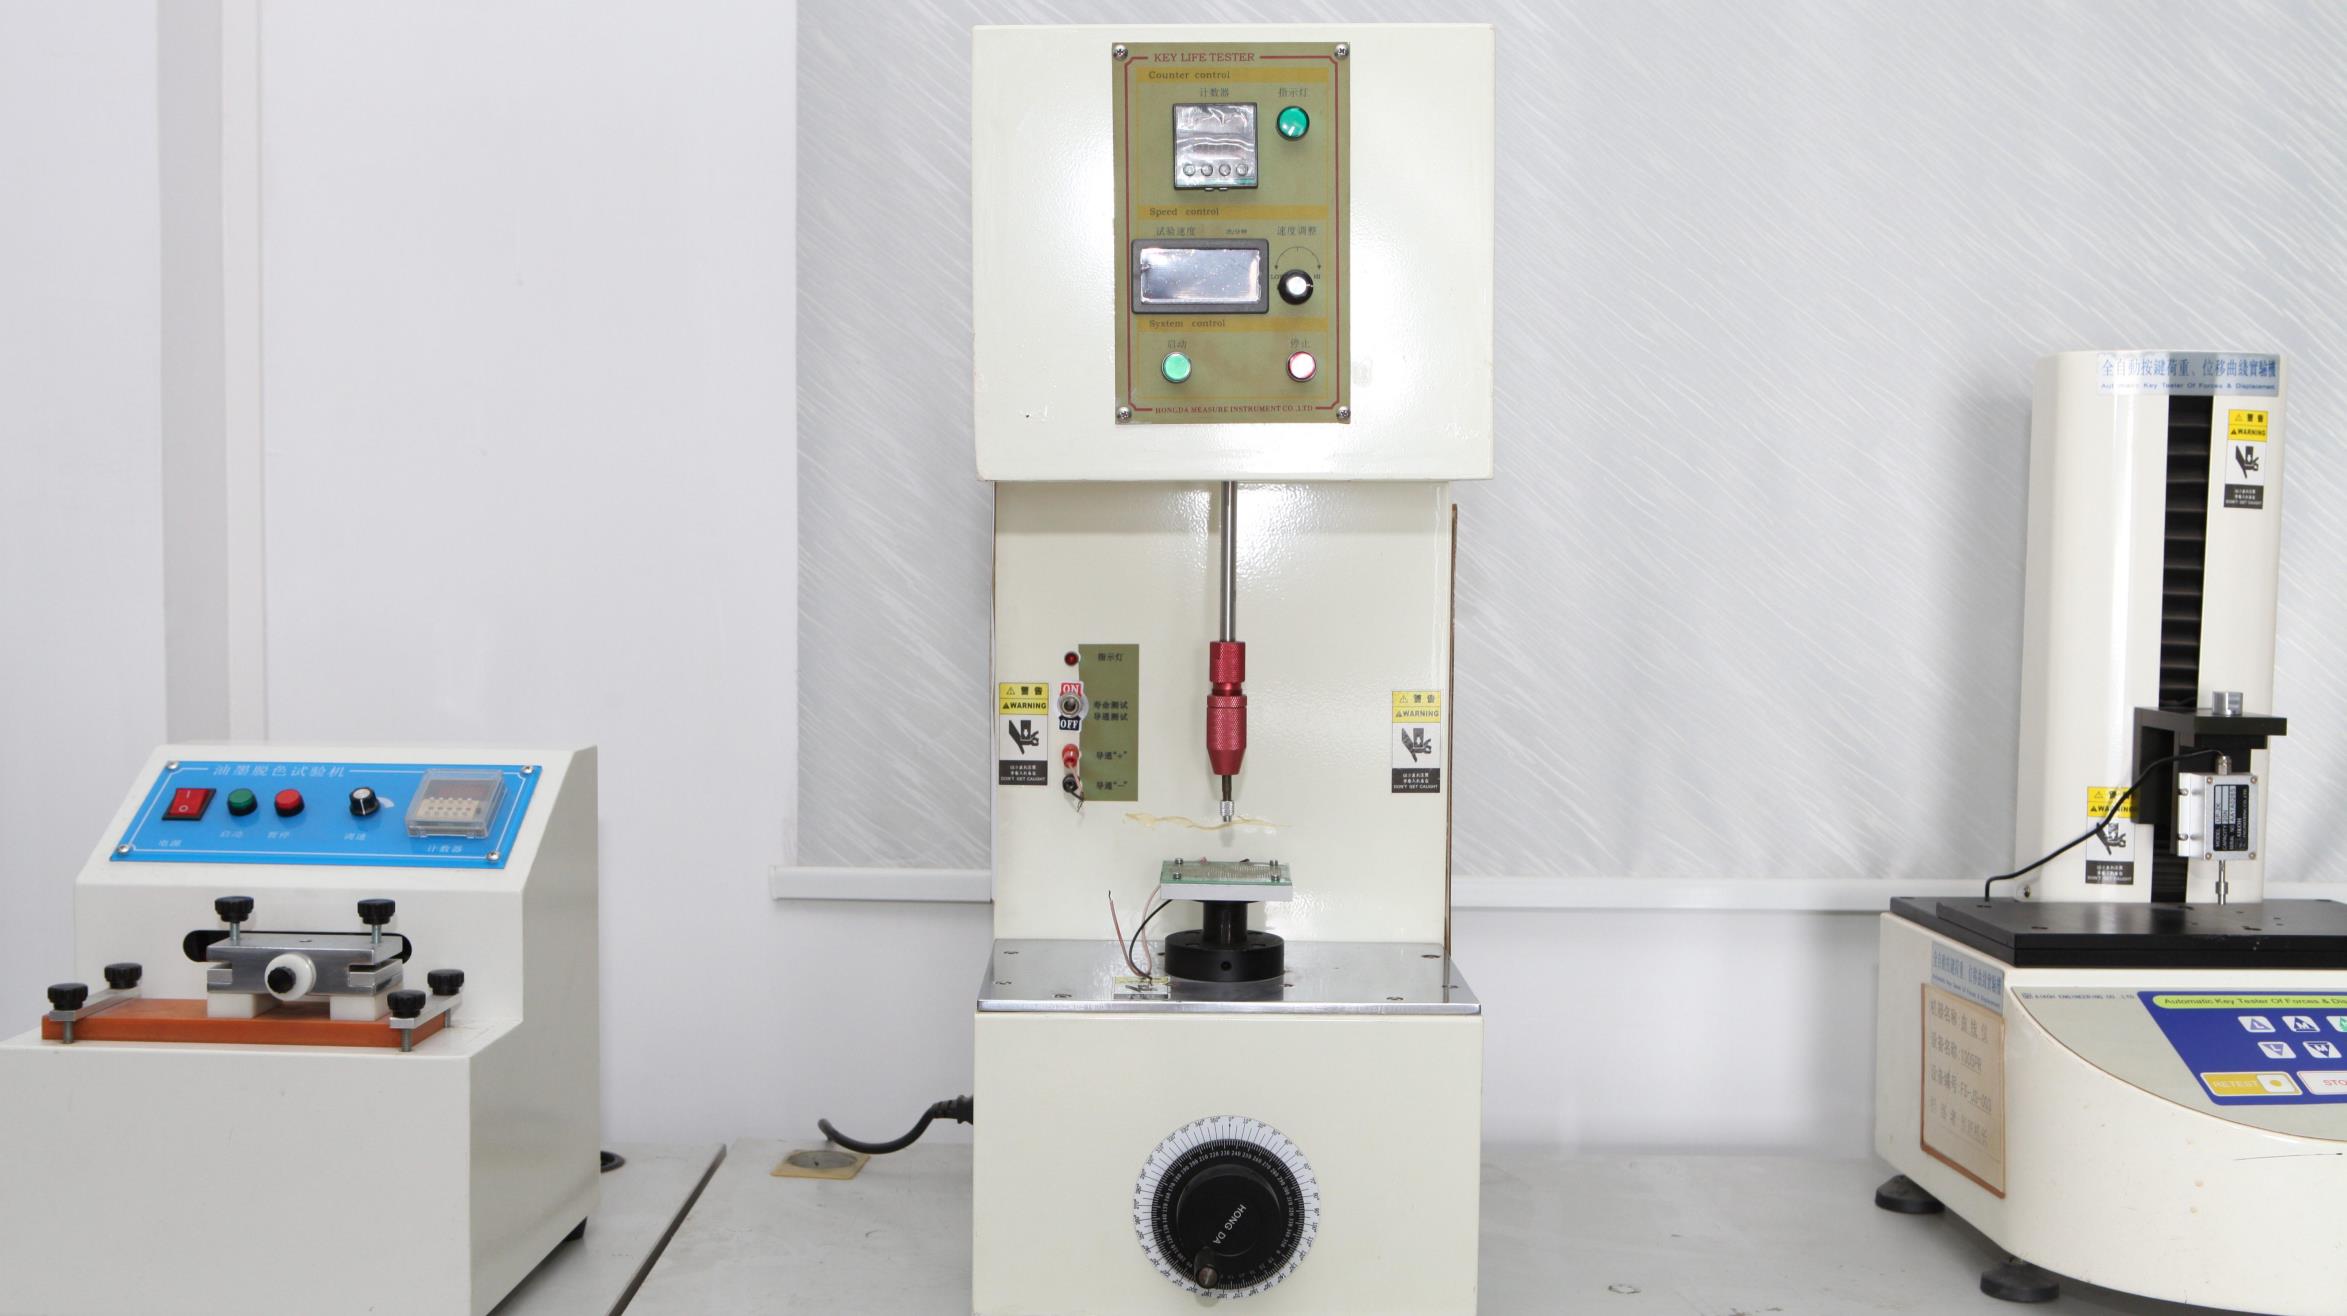
Pneumatic cycling rigs actuate tactile switches from 1,000,000 to 5,000,000 continuous hits under calibrated load to verify spring steel dome resilience.
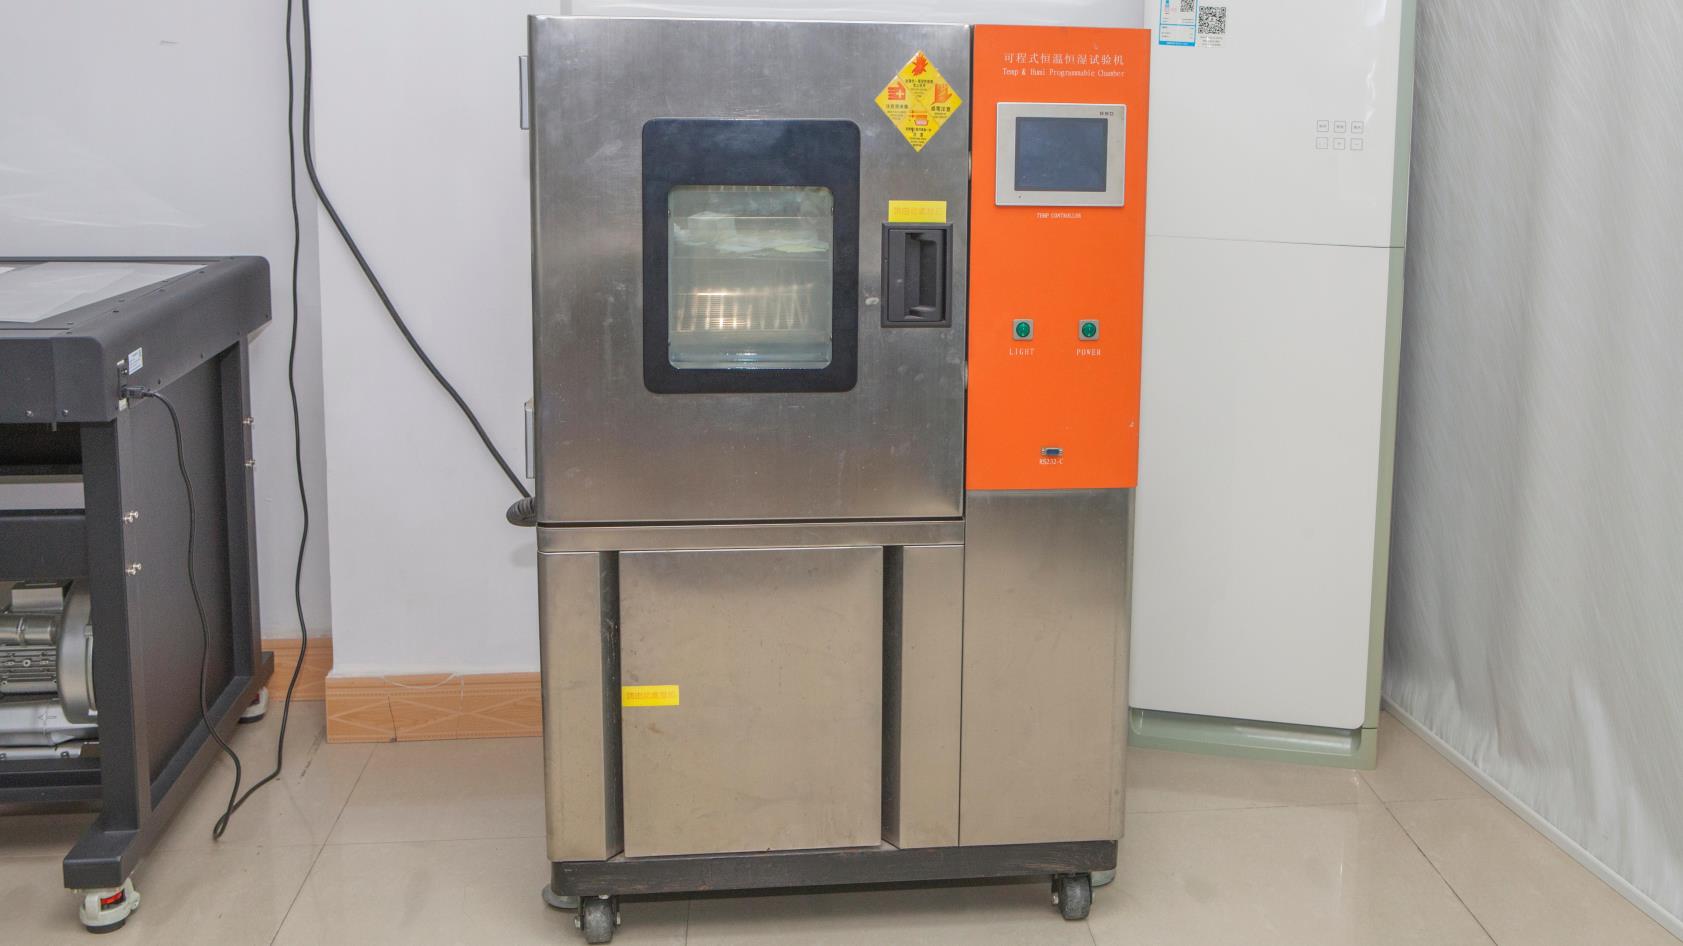
Accelerated weathering simulations cycling between -40°C and +85°C at up to 95% relative humidity to prove adhesive bonding integrity and zero perimeter delamination.
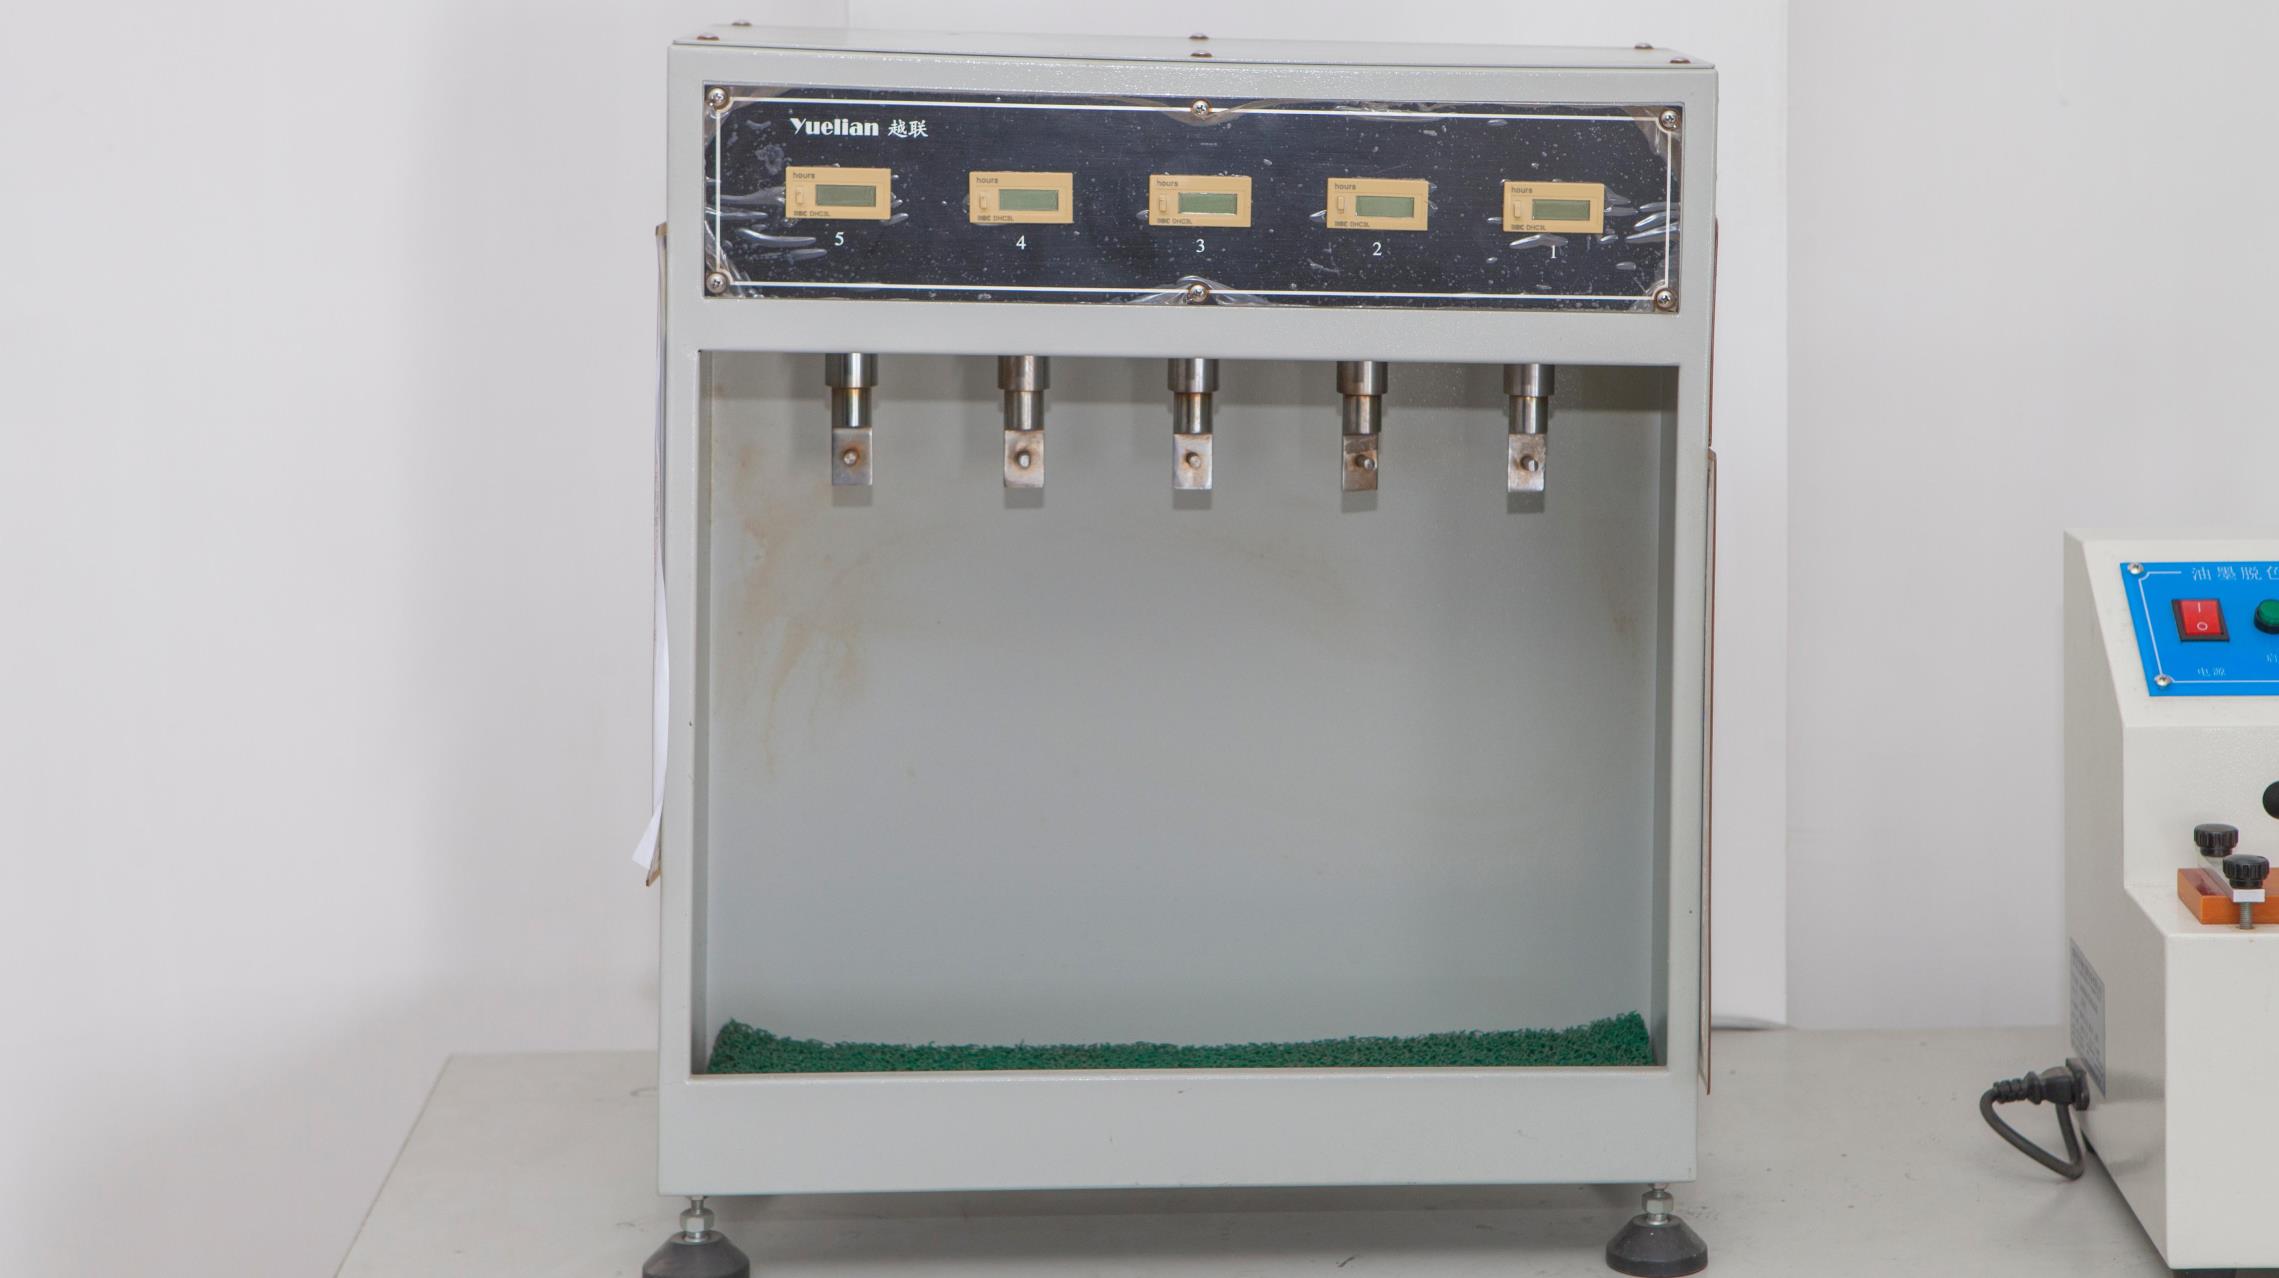
Measures 180° peel adhesion forces of 3M, Nitto, and Crown adhesive laminates, tail retention pull forces, and multi-layer structural bond durability.
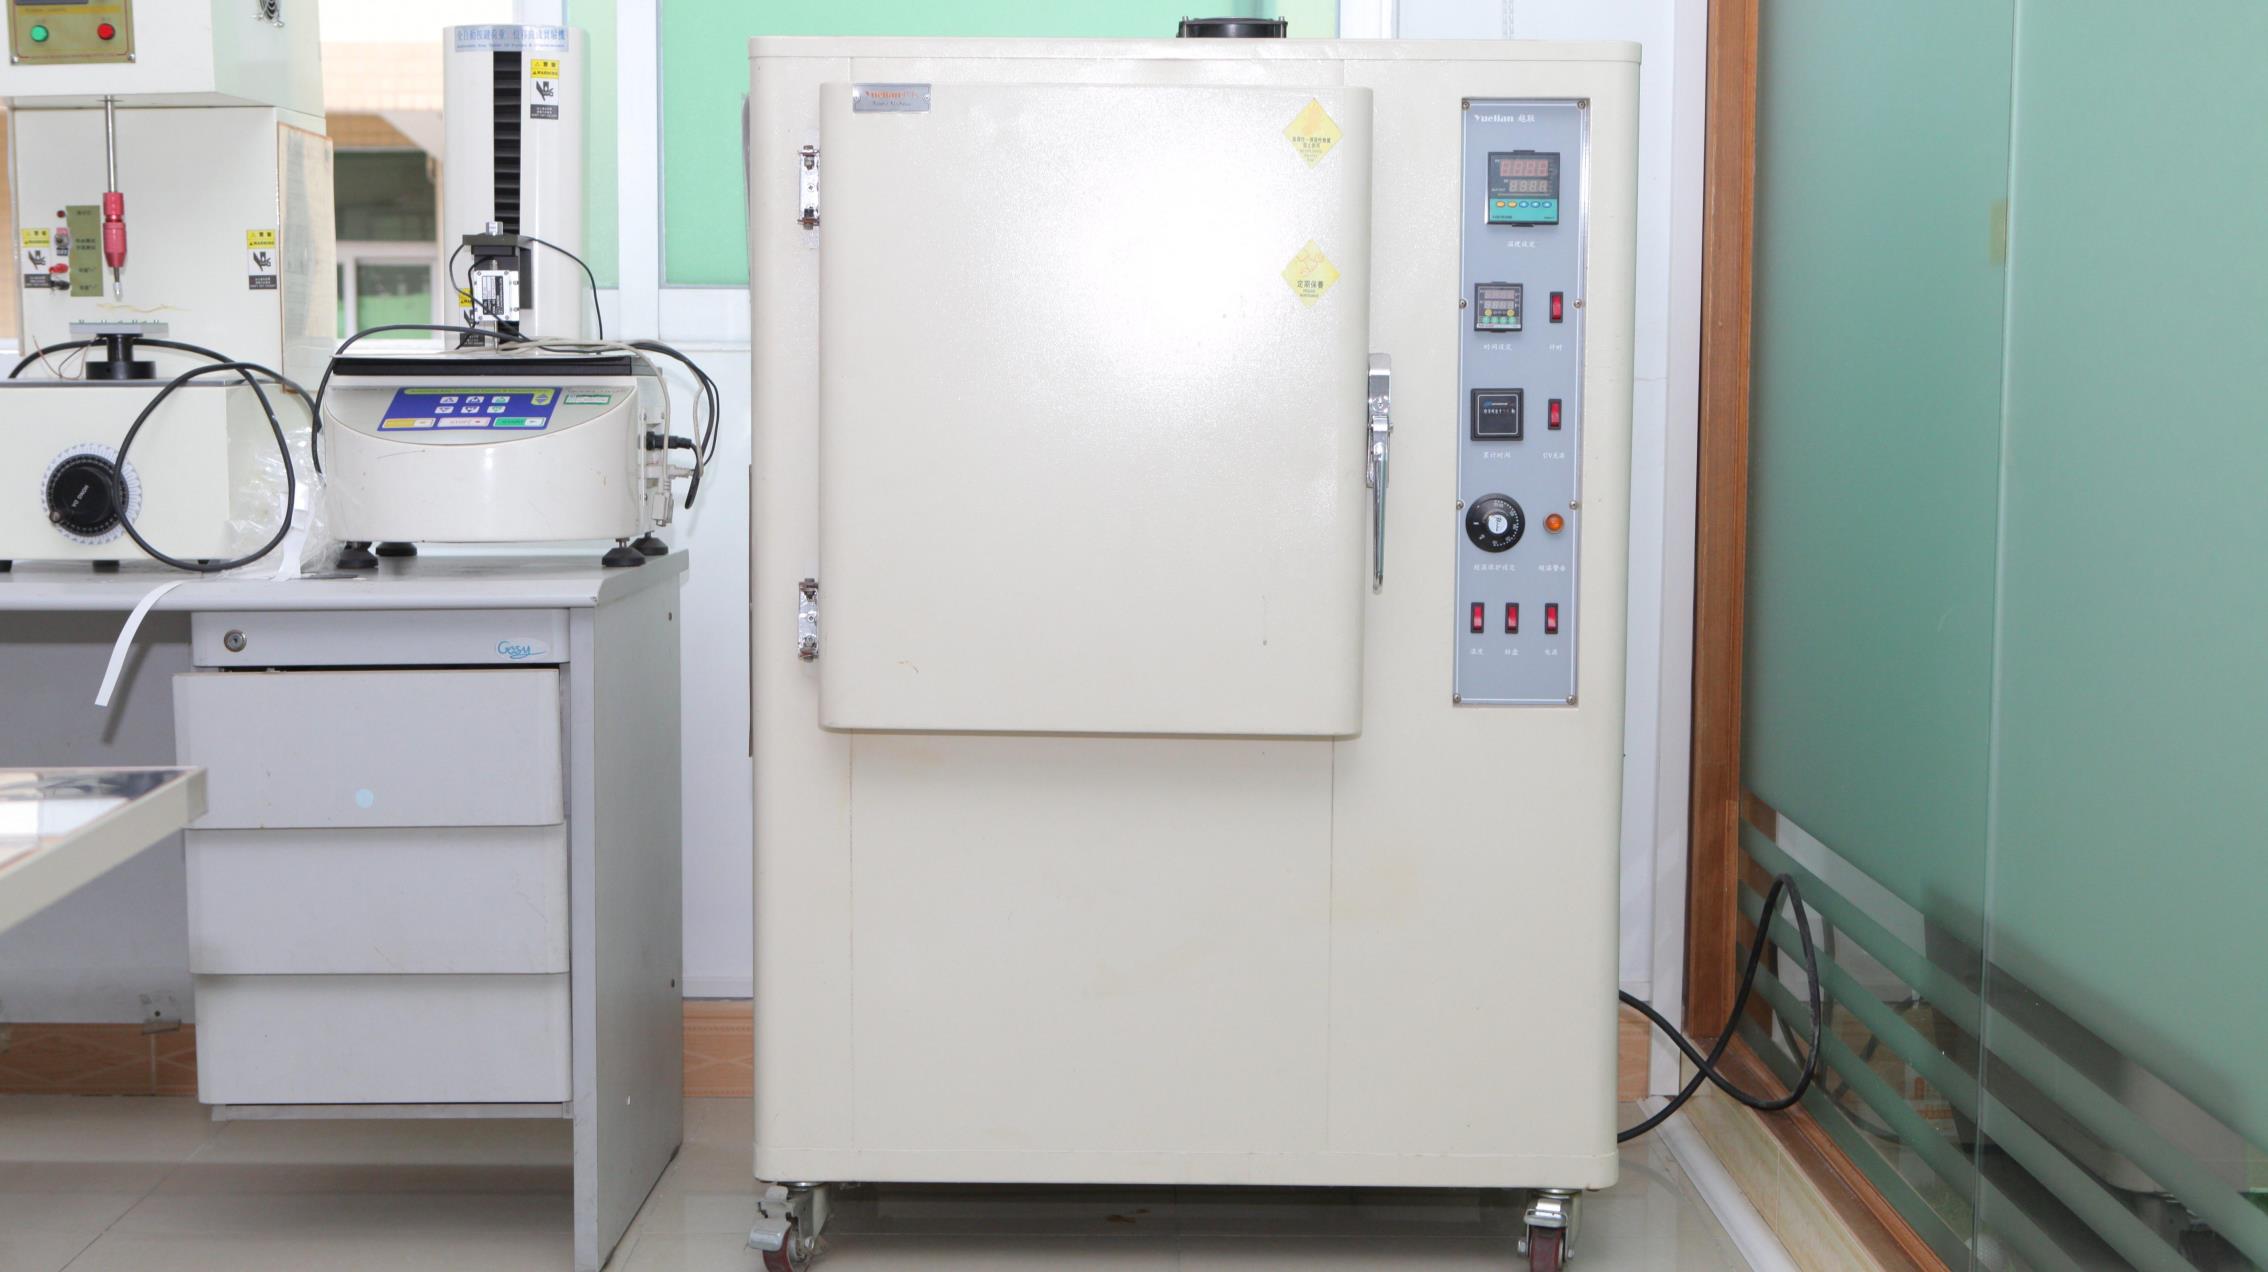
High-intensity UV exposure chambers validate the spectral color stability of graphic inks and clear window coatings against discoloration from intense sunlight.
Critical engineering considerations, shipping lead times, customs documentation, and prototyping protocols for hardware startups and established OEMs in Moldova.
For custom membrane switches and graphic overlays, engineering samples typically dispatch within 5–7 working days via air express (DHL/FedEx/UPS), arriving at Chișinău International Airport (KIV) in 4–6 business days. For specialized IMD tooling requiring precision thermoforming and injection molds, hard-tool fabrication takes 20–25 days, followed by T1 trial samples submitted with a full First Article Inspection (FAI) dimensional report.
AXRU provides comprehensive international commercial documentation, including verified Commercial Invoices, Packing Lists with HS codes (e.g., 8537.10 for electrical control panels), Certificates of Origin, and complete chemical compliance files for RoHS, REACH, and SVHC. Our products satisfy all CE marking mandates, simplifying import clearance with the Customs Service of the Republic of Moldova (Serviciul Vamal).
Recognizing the needs of high-mix, low-to-medium-volume industrial manufacturers in Eastern Europe, our standard custom membrane switch and graphic overlay MOQ starts at just 100 pieces. For complex In-Mold Decoration (IMD) assemblies requiring dedicated tooling setups, we offer pilot-batch support from 500–1,000 units to support product launches before scaling to high-volume containerized production runs.
To deliver a rapid Design for Manufacturability (DFM) assessment within 24 hours, our engineering department accepts 2D mechanical vector layouts in DXF, DWG, Adobe Illustrator (.AI), or vector PDF, accompanied by 3D CAD step files (.STEP, .IGES) for contoured IMD plastic enclosures. Graphic artwork should define PMS Pantone or RAL color references and designate clear or tinted window locations.
Yes. If you are retrofitting legacy agricultural controllers, vintage factory machinery, or discontinued medical interfaces in Moldova, you can courier a physical sample to our Dongguan engineering center. We perform non-destructive optical scanning, CMM coordinate measuring, layer stack-up peeling, and silver circuit schematic reverse-engineering to recreate complete production drawings for your approval.
We achieve IP65, IP67, and up to IP68 environmental protection through perimeter adhesive gaskets using closed-cell acrylic foams (e.g., 3M 300LSE, VHB, or Nitto 5000NS) combined with hermetically sealed tail exits. In our reliability lab, prototypes undergo continuous 24-hour water submersion and salt spray testing (ASTM B117) to confirm zero circuit corrosion or switch failure.