Featured Interface Technologies for London Hardware Teams
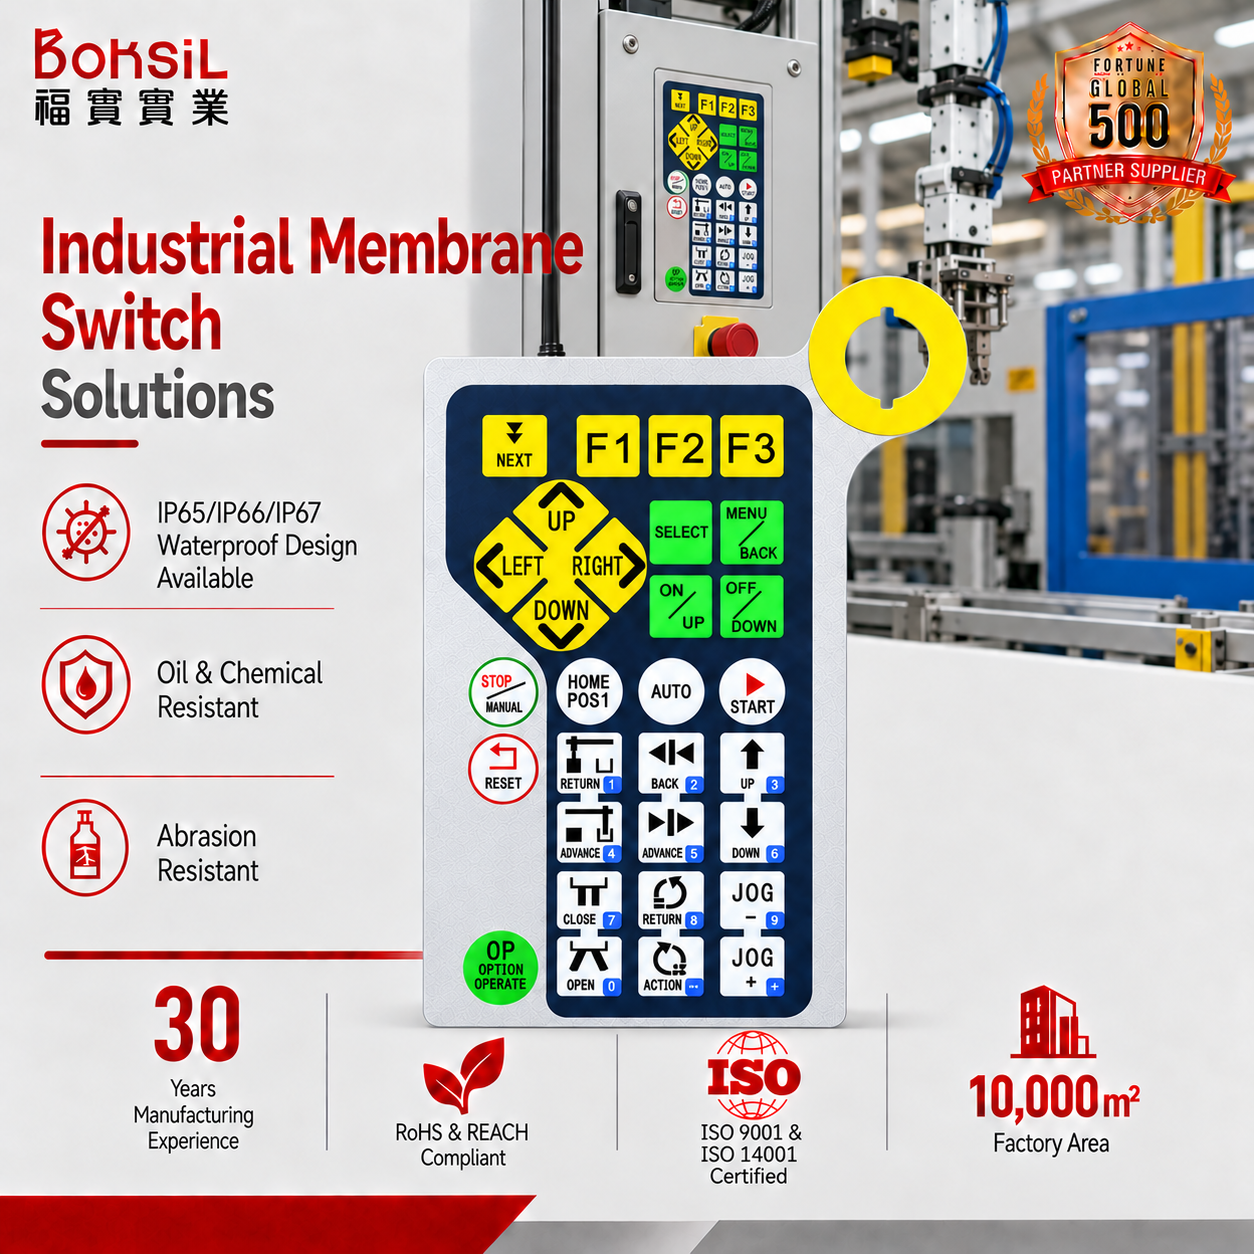
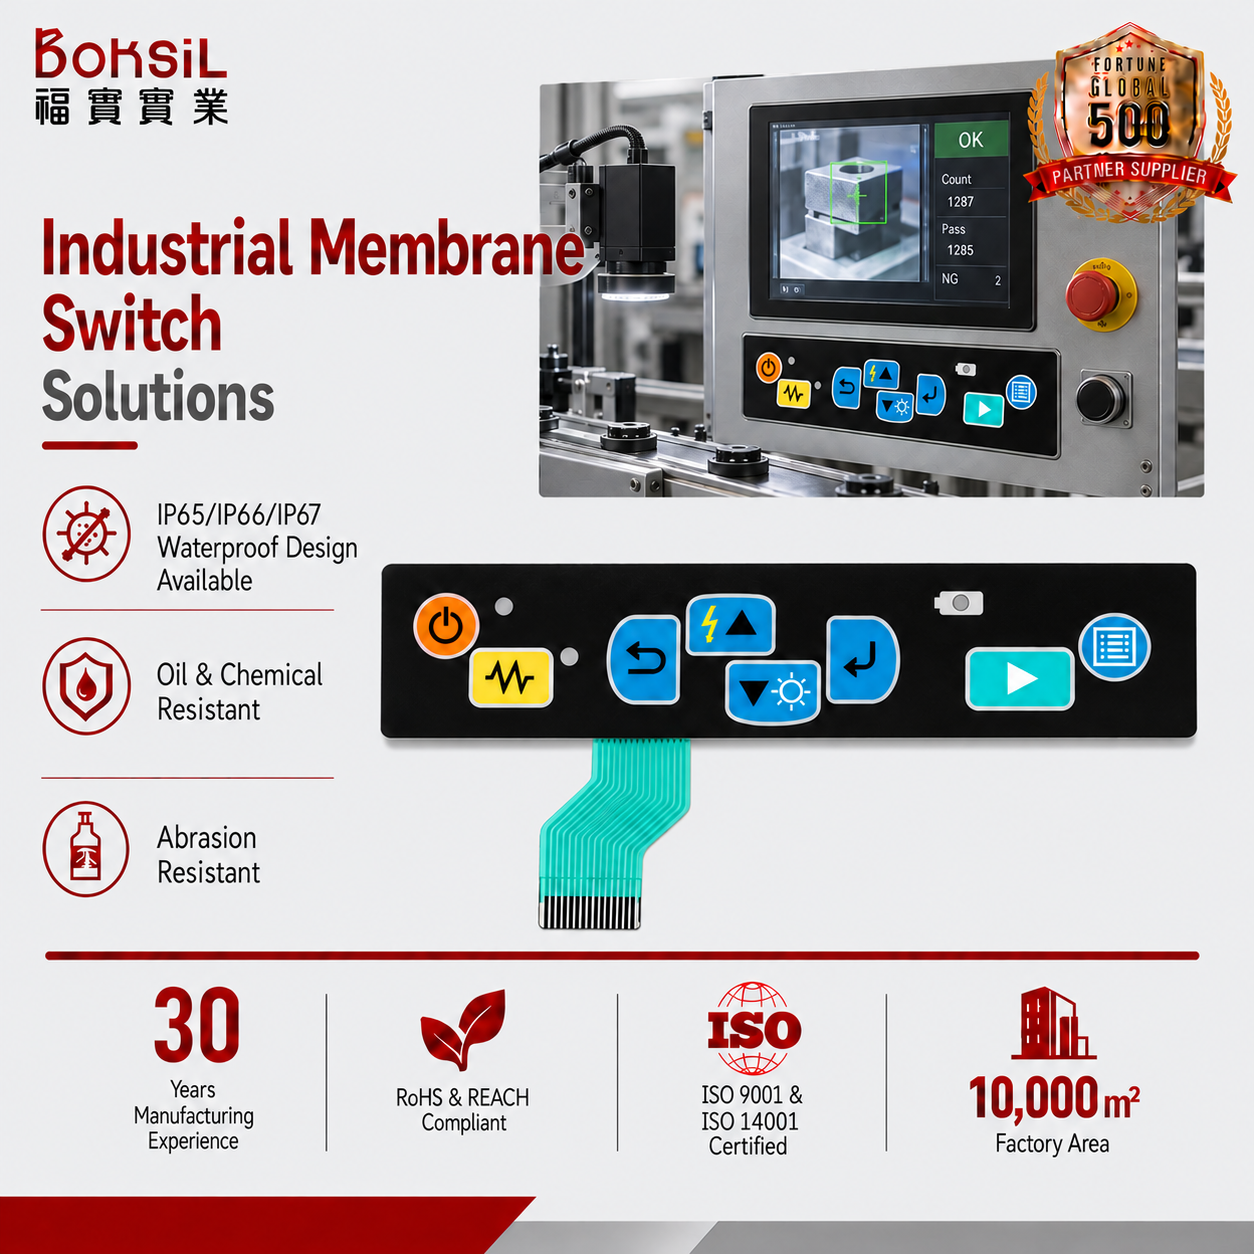
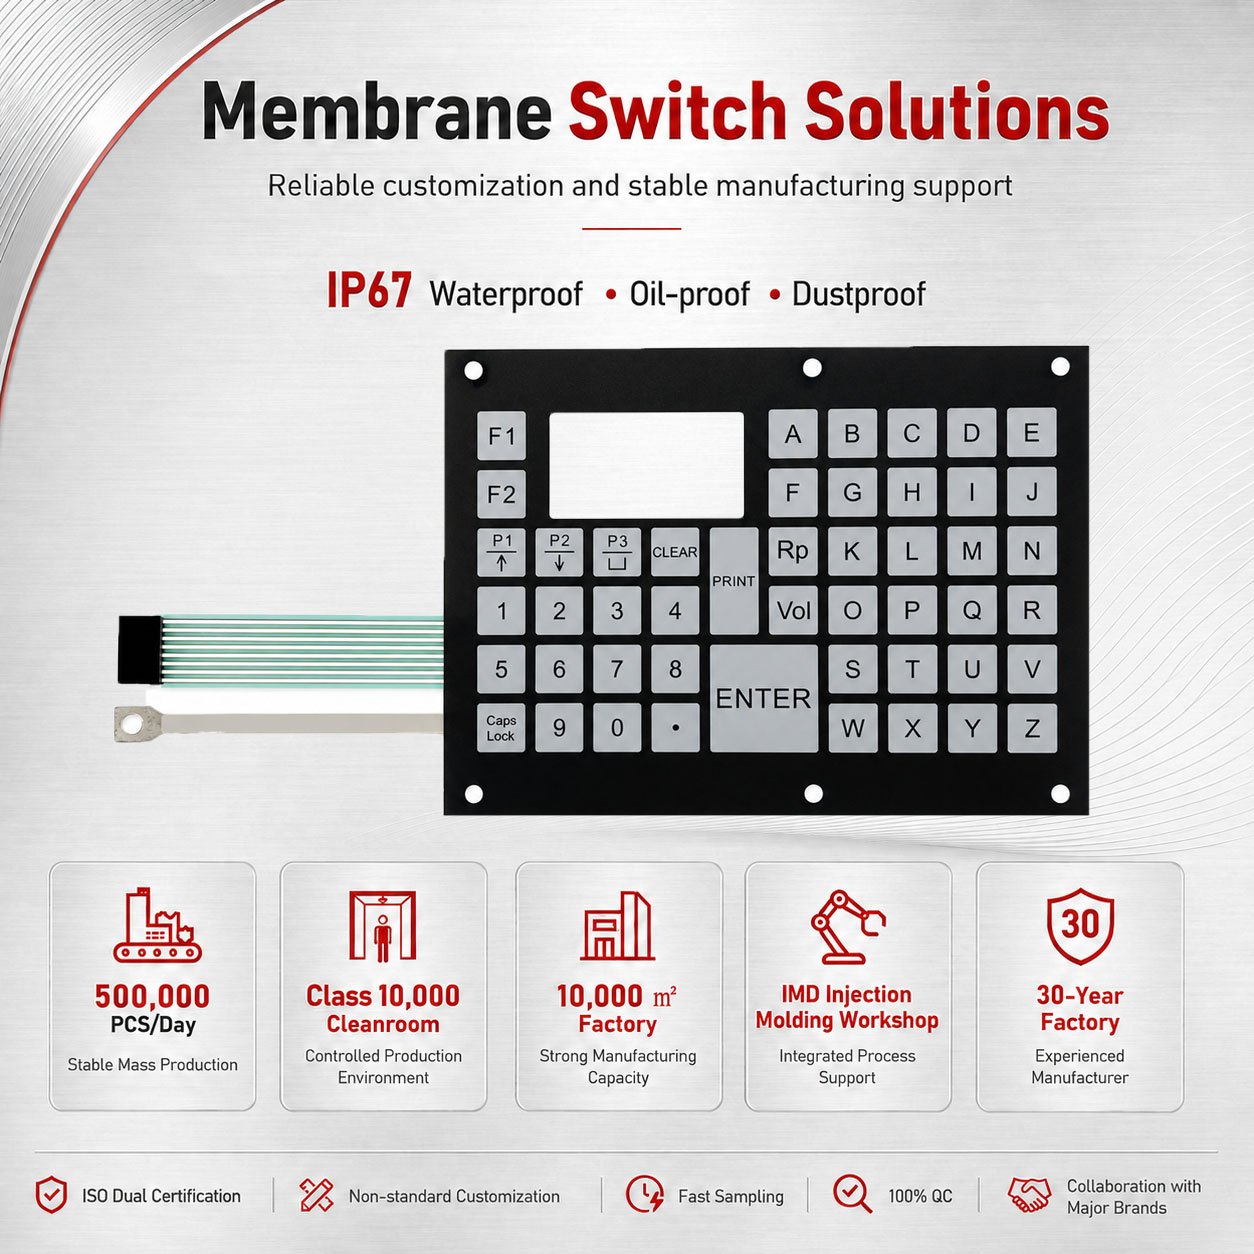
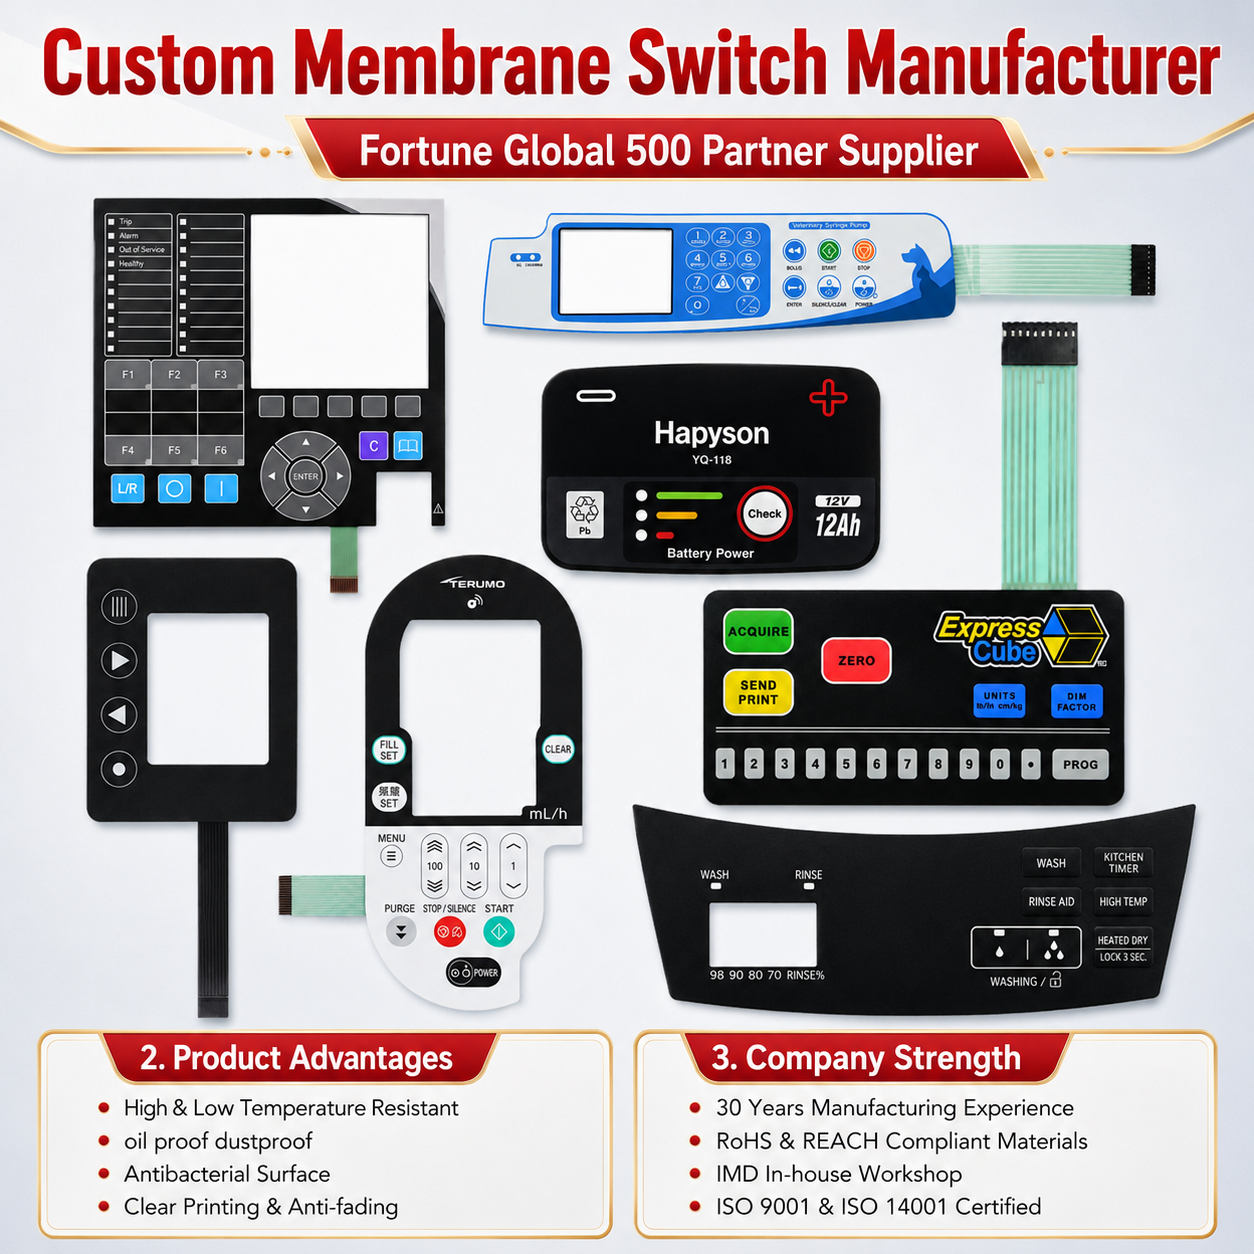
Custom fabricated to customer IPC and ISO specifications. Full architectural compatibility with UK enclosure profiles, NEMA/IP ingress requirements, and European EMC shielding mandates.
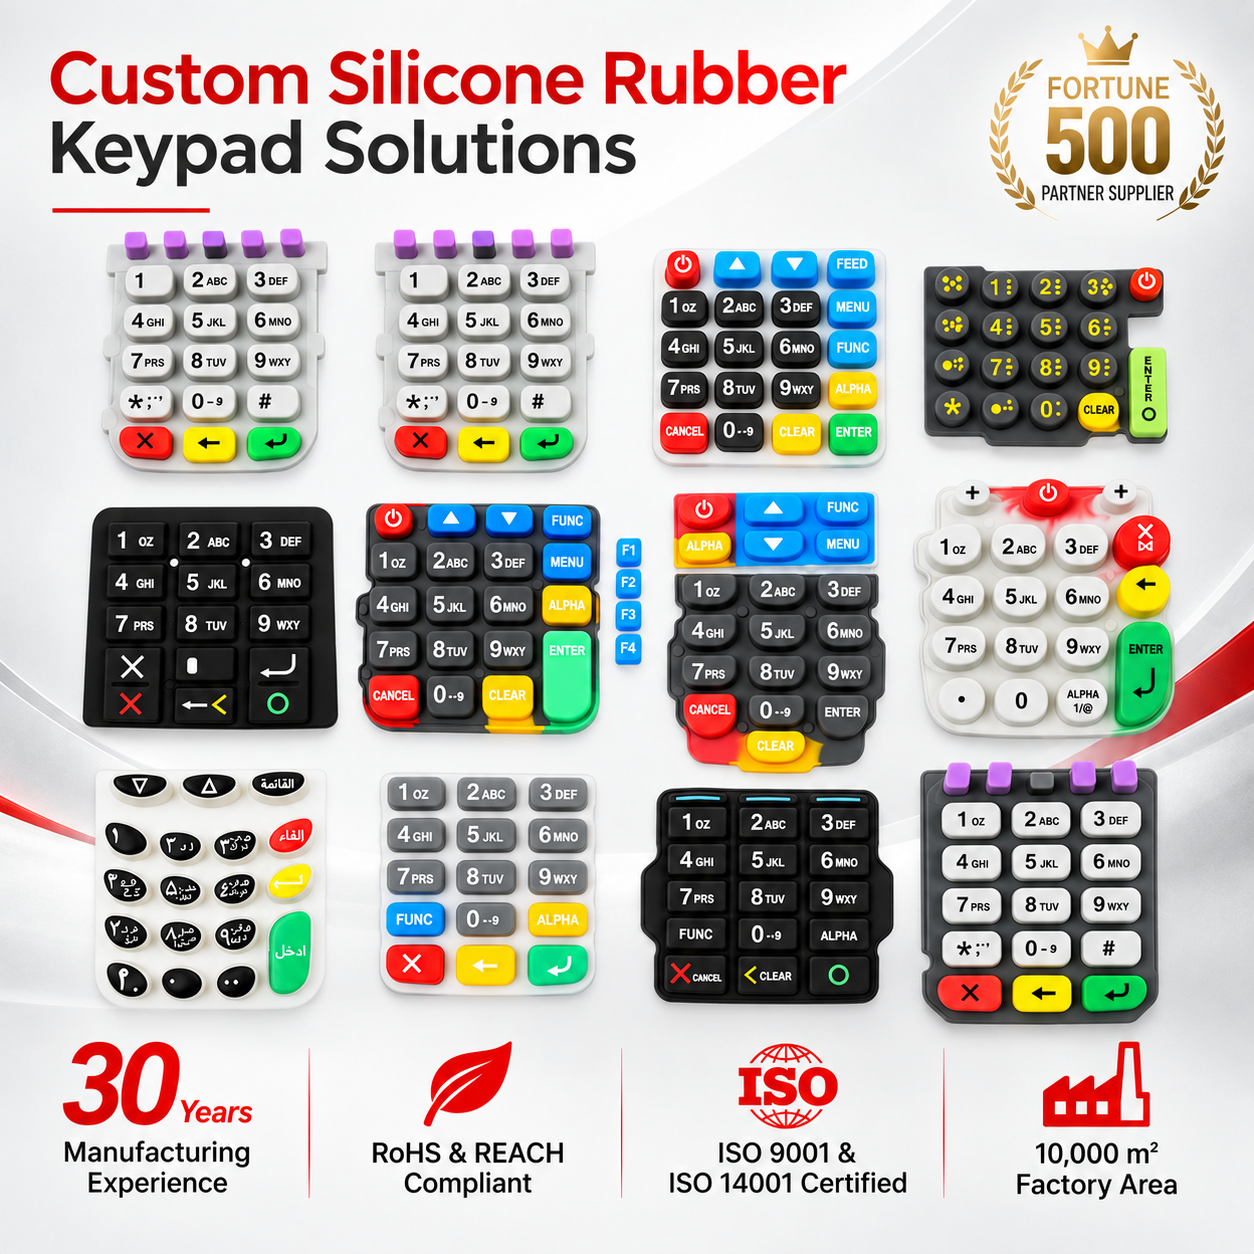
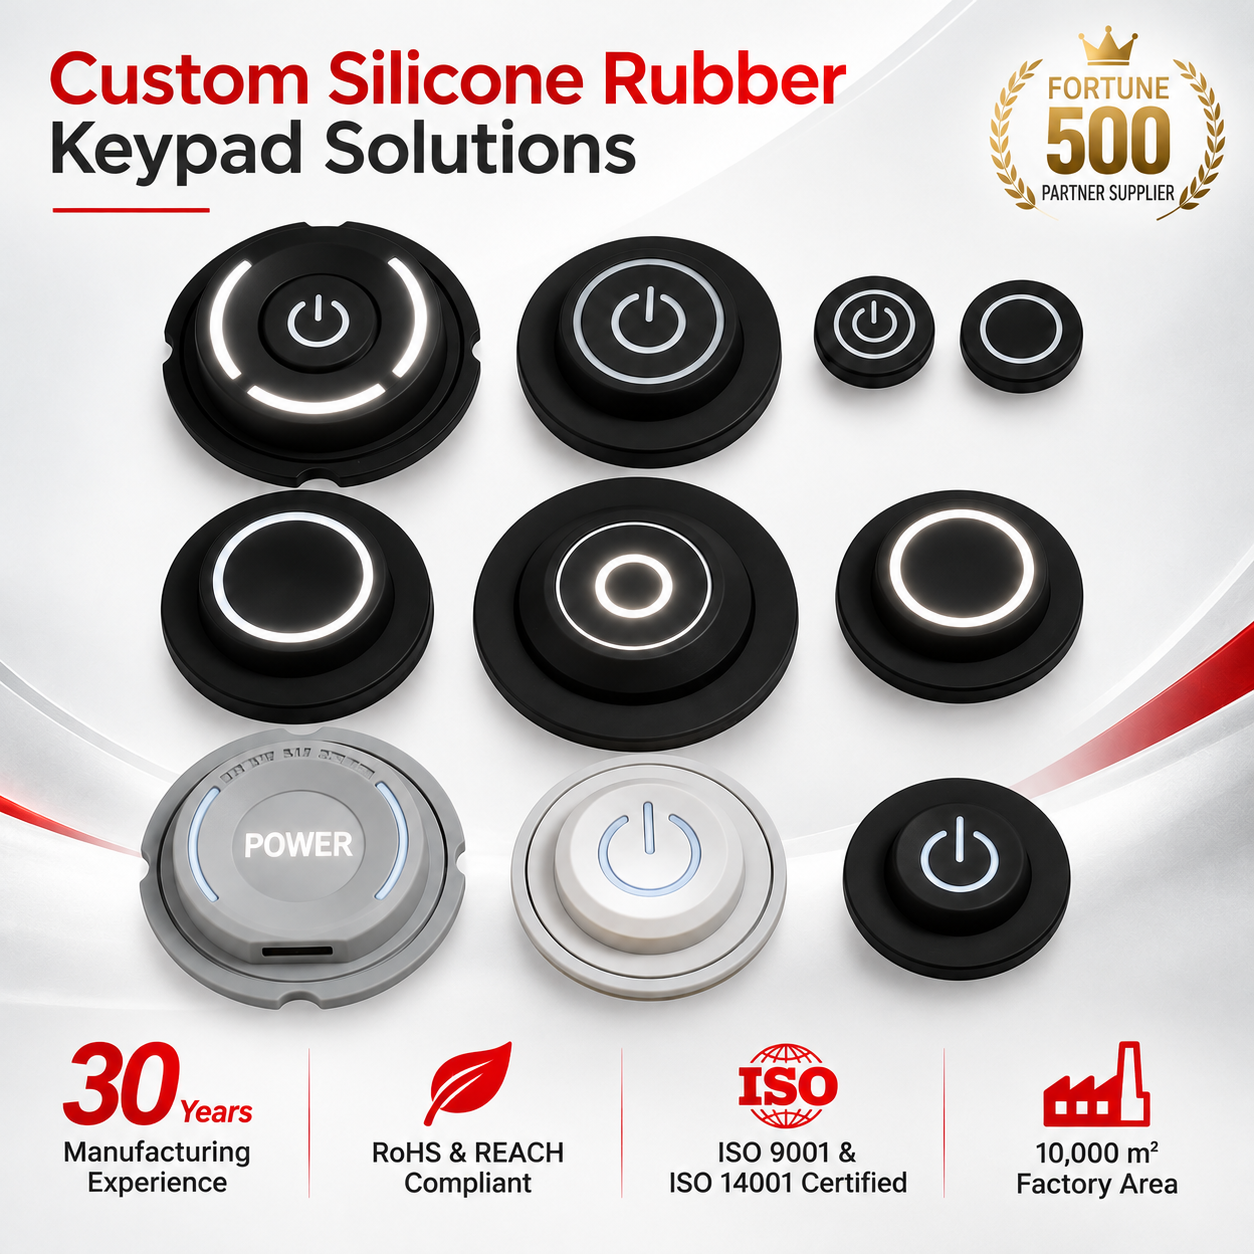
OEM/ODM medical-grade silicone keypads incorporating carbon pill contacts or integrated metal snap-domes for ergonomic feedback in diagnostic instruments.
IP67 sealed resistive pad circuit architecture with perimeter silicone sealing barriers engineered for outdoor charging nodes and London public transport points.
Integrated Light Guide Film (LGF) and surface-mount micro-LED matrix designed for low-light critical cockpits, marine systems, and broadcast equipment.
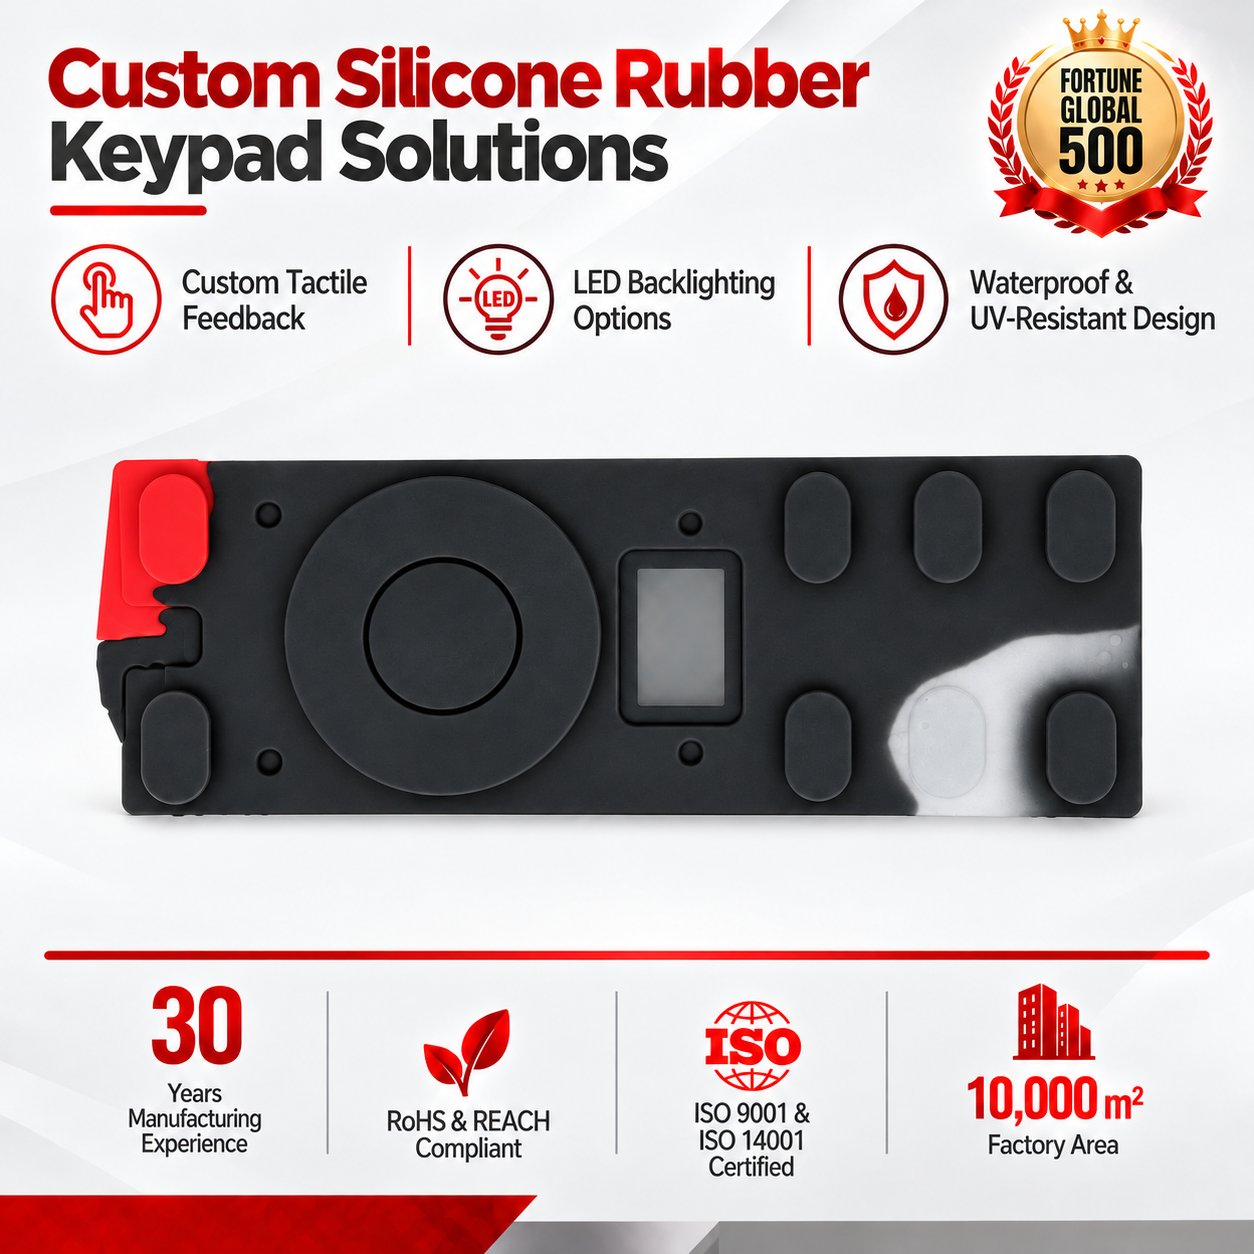
High-tactile snap ratio design with multi-colour compression molding for plant automation controllers, automation robotics, and power management units.
Reverse-printed PMMA and chemically hardened glass fascias featuring anti-fingerprint, anti-glare, and anti-scratch coats for London fintech and media gear.
In-Mold Decoration (IMD) & Advanced Keypads for London Engineering Ecosystems
The Greater London engineering cluster—spanning tech hardware startups in Shoreditch and Old Street Roundabout, advanced MedTech developers across White City Innovation District, and high-spec industrial instrumentation manufacturers in Hertfordshire and Surrey—demands an evolution in Human-Machine Interfaces (HMI). Traditional mechanical assemblies with detached bezels, secondary adhesive labels, and unsealed crevices fail to meet modern aesthetic, durability, and sanitary thresholds.
In-Mold Decoration (IMD), also referenced as In-Mold Labelling (IML) or In-Mold Insert Molding (IMD-IMF), consolidates graphic screen-printing, thermodynamic high-pressure forming, 3D die-trimming, and injection molding into an inseparable, monolithic composite. For London's design-led hardware firms, IMD keypad panels eradicate graphics abrasion, resist volatile chemical exposure, and achieve ingress protection ratings up to IP67 and IP68 within ultra-thin structural form factors.
Direct Manufacturing Advantage: By bridging custom high-precision mold engineering in our Dongguan Intertek-verified facility with technical alignment for UK engineering standards (BS EN 60601-1, RoHS, REACH, and CE/UKCA regulations), Dongguan AXRU Electronics provides turnkey prototype-to-mass-production continuity without middleman supply friction.
Architectural Breakdown: IMD vs Traditional Film Assemblies
Unlike standard surface-printed graphic overlays where secondary adhesives secure printed films over plastic housings, IMD encapsulates reverse-printed optical films within injected structural resin (typically optical polycarbonate, ABS, or PMMA blends). The printed imagery sits sandwiched beneath a durable resin top surface, shielded completely against atmospheric UV, saline air, aggressive biocidal cleansers, and abrasive wear.
Evaluation Parameter
Conventional Membrane Overlay
Silicone Elastomer Pad
IMD / IMF Integrated Keypad
Graphics Protection
Reverse-printed under film (subject to border delamination)
Top pad-printed or laser etched with PU coating
Hermetically fused inside resin core (Indelible)
3D Contour Capability
Planar with mechanical embossing (0.3 - 0.8mm)
Deep compression profiles (3.0 - 15.0mm)
Complex 3D organic geometry + deep draw curvature
Surface Hardness
2H to 3H (Hard-coated PET)
Flexible elastomer (Shore A 40-70)
4H to 6H (Automotive grade hard-coated films)
Ingress Resilience
Dependent on PSA adhesive perimeter gasket
Requires compression bezel or mechanical clamp
Unified monolithic housing; IP67/IP68 native seal
Tactile Feedback Integration
Stainless steel snap domes or polydomes
Internal silicone dome collapse structure
Hybrid support: Capacitive touch, dome matrix, or lightguides
Material Selection Science for Harsh Climate and High-Duty Cycles
London's ambient operating conditions—ranging from high condensation cycles on rapid-transit rail interfaces along the Elizabeth line and TfL networks to rigorous autoclaving regimes in NHS medical incubators—require exacting material science:
Specialist Substrates
Biaxially oriented PET (Autotype MacDermid Autotex / Autoflex) and optical-grade Polycarbonate films ensuring minimum yield stresses, extreme elongation tolerance during hot-forming, and high transparency over LCD/OLED optical cavities.
Resin Engineering
High-flow polycarbonates and UV-stabilised ABS-PC polymers calibrated for shrinkage compensation, low internal stress, and superior chemical bonding against inks to eliminate thermal delamination in industrial environments.
Conductive Traces
Micro-crack-resistant polymer thick-film (PTF) silver paste, copper-clad polyimide FPC circuits, and PEDOT:PSS transparent conductive layers designed to maintain continuity across dynamic actuation angles.
Localised Deployment
IMD & HMI Application Scenarios across Greater London
Direct manufacturing alignment for high-density smart infrastructure, enterprise medical instruments, and industrial IoT developments within the UK.
Medical Instruments & NHS Clinical Environments
Deployment in diagnostic blood-gas analysers, infusion pump controllers, and surgical theatre suites across central London hospital trusts. IMD panels eliminate seams, supporting relentless cleaning protocols with chlorine-releasing agents, isopropyl alcohol, and hydrogen peroxide vapor without clouding or legend degradation.
Smart City Kiosks & EV Charging Infrastructure
London's rapid rollout of public EV charging hubs, kerbside ticketing terminals, and ULEZ monitoring terminals requires IK09/IK10 mechanical impact tolerance and IP67 weather-sealing. Our IMD and metal-dome keypad assemblies withstand extreme UV exposure, freeze-thaw cycles, and heavy vandal strain across metropolitan environments.
Specialist Aerospace, Defence & Rail Terminals
Direct supply to communication systems and monitoring pods in transport networks (Crossrail, Underground) and regional aerospace research corridors. Assemblies offer tailored EMI/RFI shielding with full ITO deposition or printed carbon meshes, mitigating RF interference in high-density telecommunication contexts.
Industry Analysis
Emerging HMI Procurement & Engineering Trends in London
Procurement teams and principal electronics engineers across London are transitioning away from fragmented multi-vendor supply chains. Instead of sourcing bare plastic housings from one supplier, graphic foils from another, and PCBA/membrane switch tails from a third, design authorities demand unified Tier-1 manufacturing partnerships capable of supplying 100% pre-tested modular front panels.
Trend 01
Capacitive Sensing Integration
Replacing traditional push-buttons with in-mold structural electronics (IMSE), embedding capacitive copper traces directly behind curved 3D covers for uninterrupted surface flow.
Trend 02
Dead-Front & Dynamic Backlighting
Selective light guide films (LGF) and precision light-blocking inks allow warning symbols and status legends to remain hidden until backlit, aligning with modern minimalist product design.
Trend 03
Antimicrobial Surface Finishes
Permanent silver-ion antimicrobial coatings integrated into the hard-coat PET matrix, providing persistent 99.9% anti-pathogen protection for high-touch public and medical interfaces.
Trend 04
FPC Tail Consolidation
Transitioning from silver-printed flexible tails to polyimide copper FPC leads with ZIF or Amphenol FCI connectors to survive tight enclosure bend radiuses and eliminate conductive migration.
Operating a vertically integrated 10,000㎡ industrial campus in Dongguan, China, Dongguan AXRU Electronics Co., Ltd. delivers direct factory engineering governance to international OEM brands.
10,000㎡ Intertek-Verified Facility
Our production plant is physically audited and verified by Intertek. Cleanroom class 1,000 and 10,000 screen printing facilities ensure zero dust inclusion during film printing, lamination, and IMD thermal forming operations.
12+ Years Enterprise OEM Pedigree
We are a certified tier supplier to Fortune 500 corporations and global electronic equipment manufacturers. Our 121-person workforce includes dedicated bilingual HMI tooling specialists and DFM project engineers.
Complete In-House Tooling & Molding
From CAD/CAM tooling fabrication, cleanroom silkscreen and digital printing, high-pressure gas forming, to CNC laser trimming and 100-500 ton injection molding machines—zero core procedures are sub-contracted.
Flexible Prototyping (MOQ 100 Pcs)
Engineered to assist high-value product iterations. We supply dedicated rapid-sample fabrication lines to support London design firms during Alpha and Beta stage user validation trials ahead of scaled mass production runs.
Direct Engineering Communication
You liaise directly with experienced DFM engineering teams fluent in stack-up optimisation, snap-ratio adjustments, EMI shielding rules, and connector integration—avoiding sales broker misunderstandings.
Full UK & EU Logistics Compliance
Complete traceability documentation, certificates of conformity (CoC), material declarations (RoHS/REACH), and air express delivery channels via DHL/FedEx/UPS directly into London Heathrow or Thames Gateway hubs.
In-House Reliability Lab
Comprehensive Validation & Quality Control Equipment
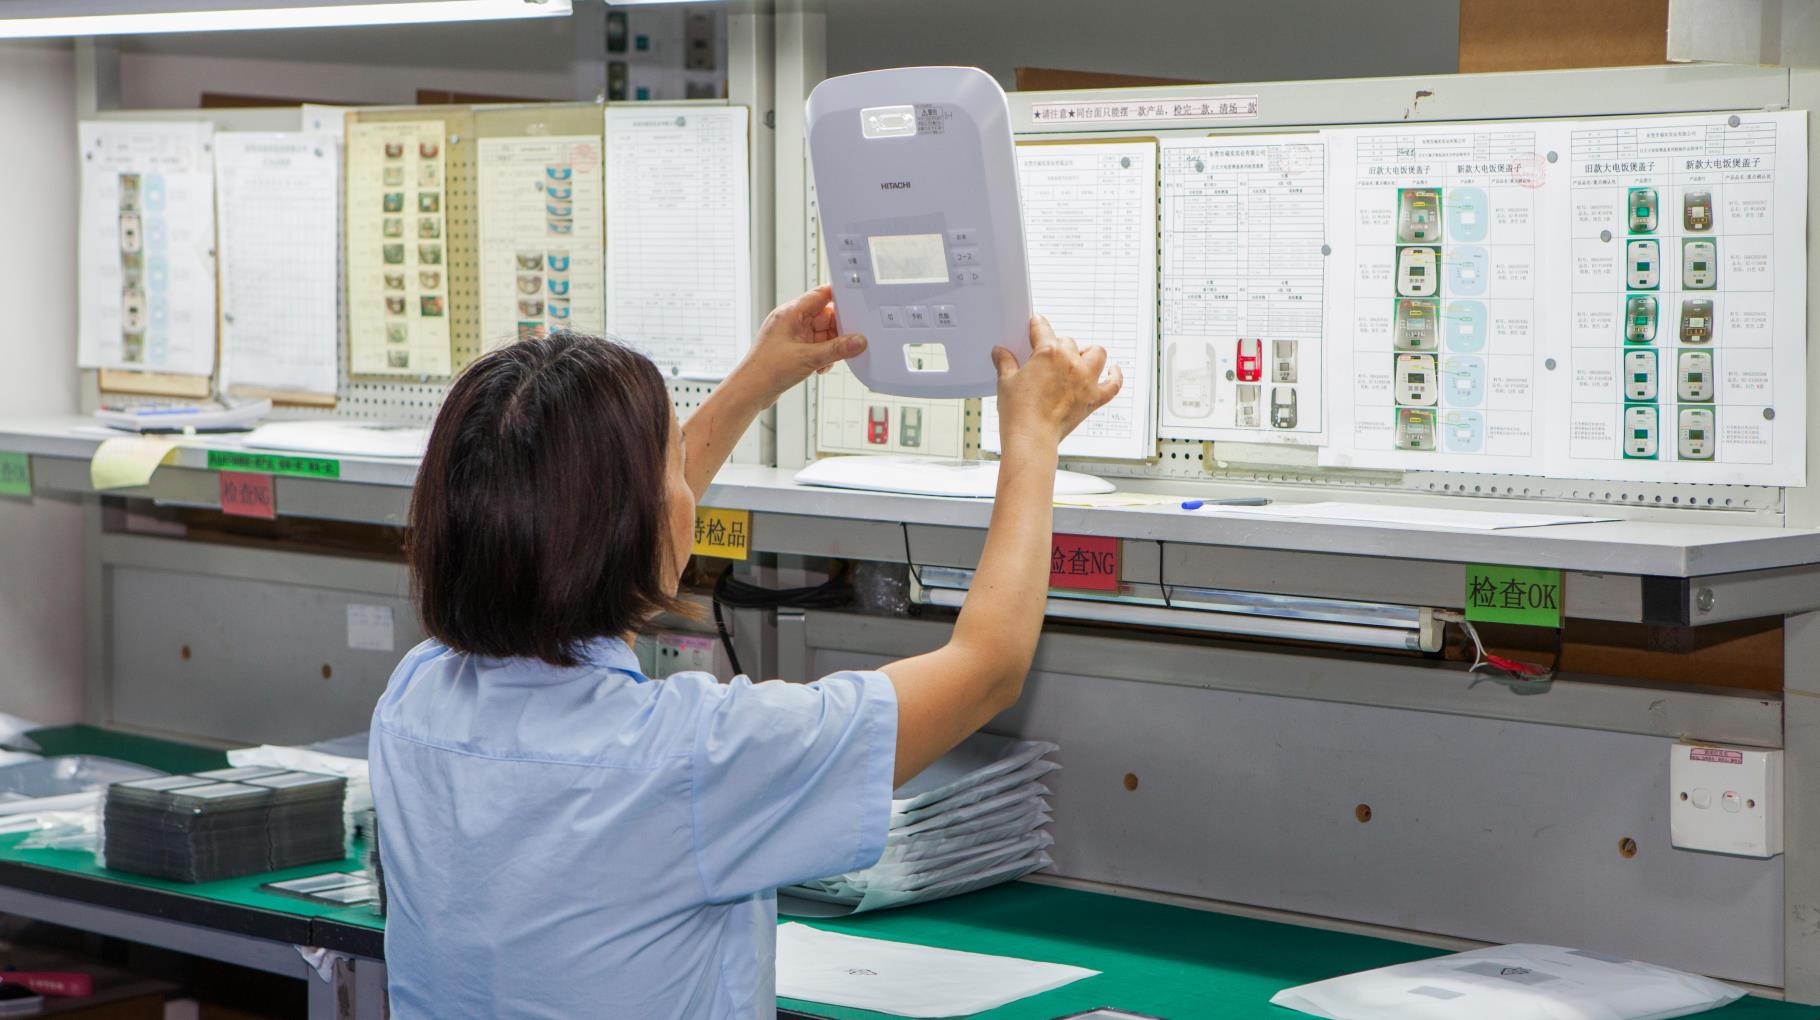
Every membrane switch, IMD fascia, and capacitive keypad undergoes 100% electrical inspection alongside multi-axis environmental stress testing before international dispatch.
100% Electrical Inspection
Automated circuit testing checking contact resistance, insulation resistance (>100MΩ @ 100V DC), LED forward voltage, and line-to-line shorts.
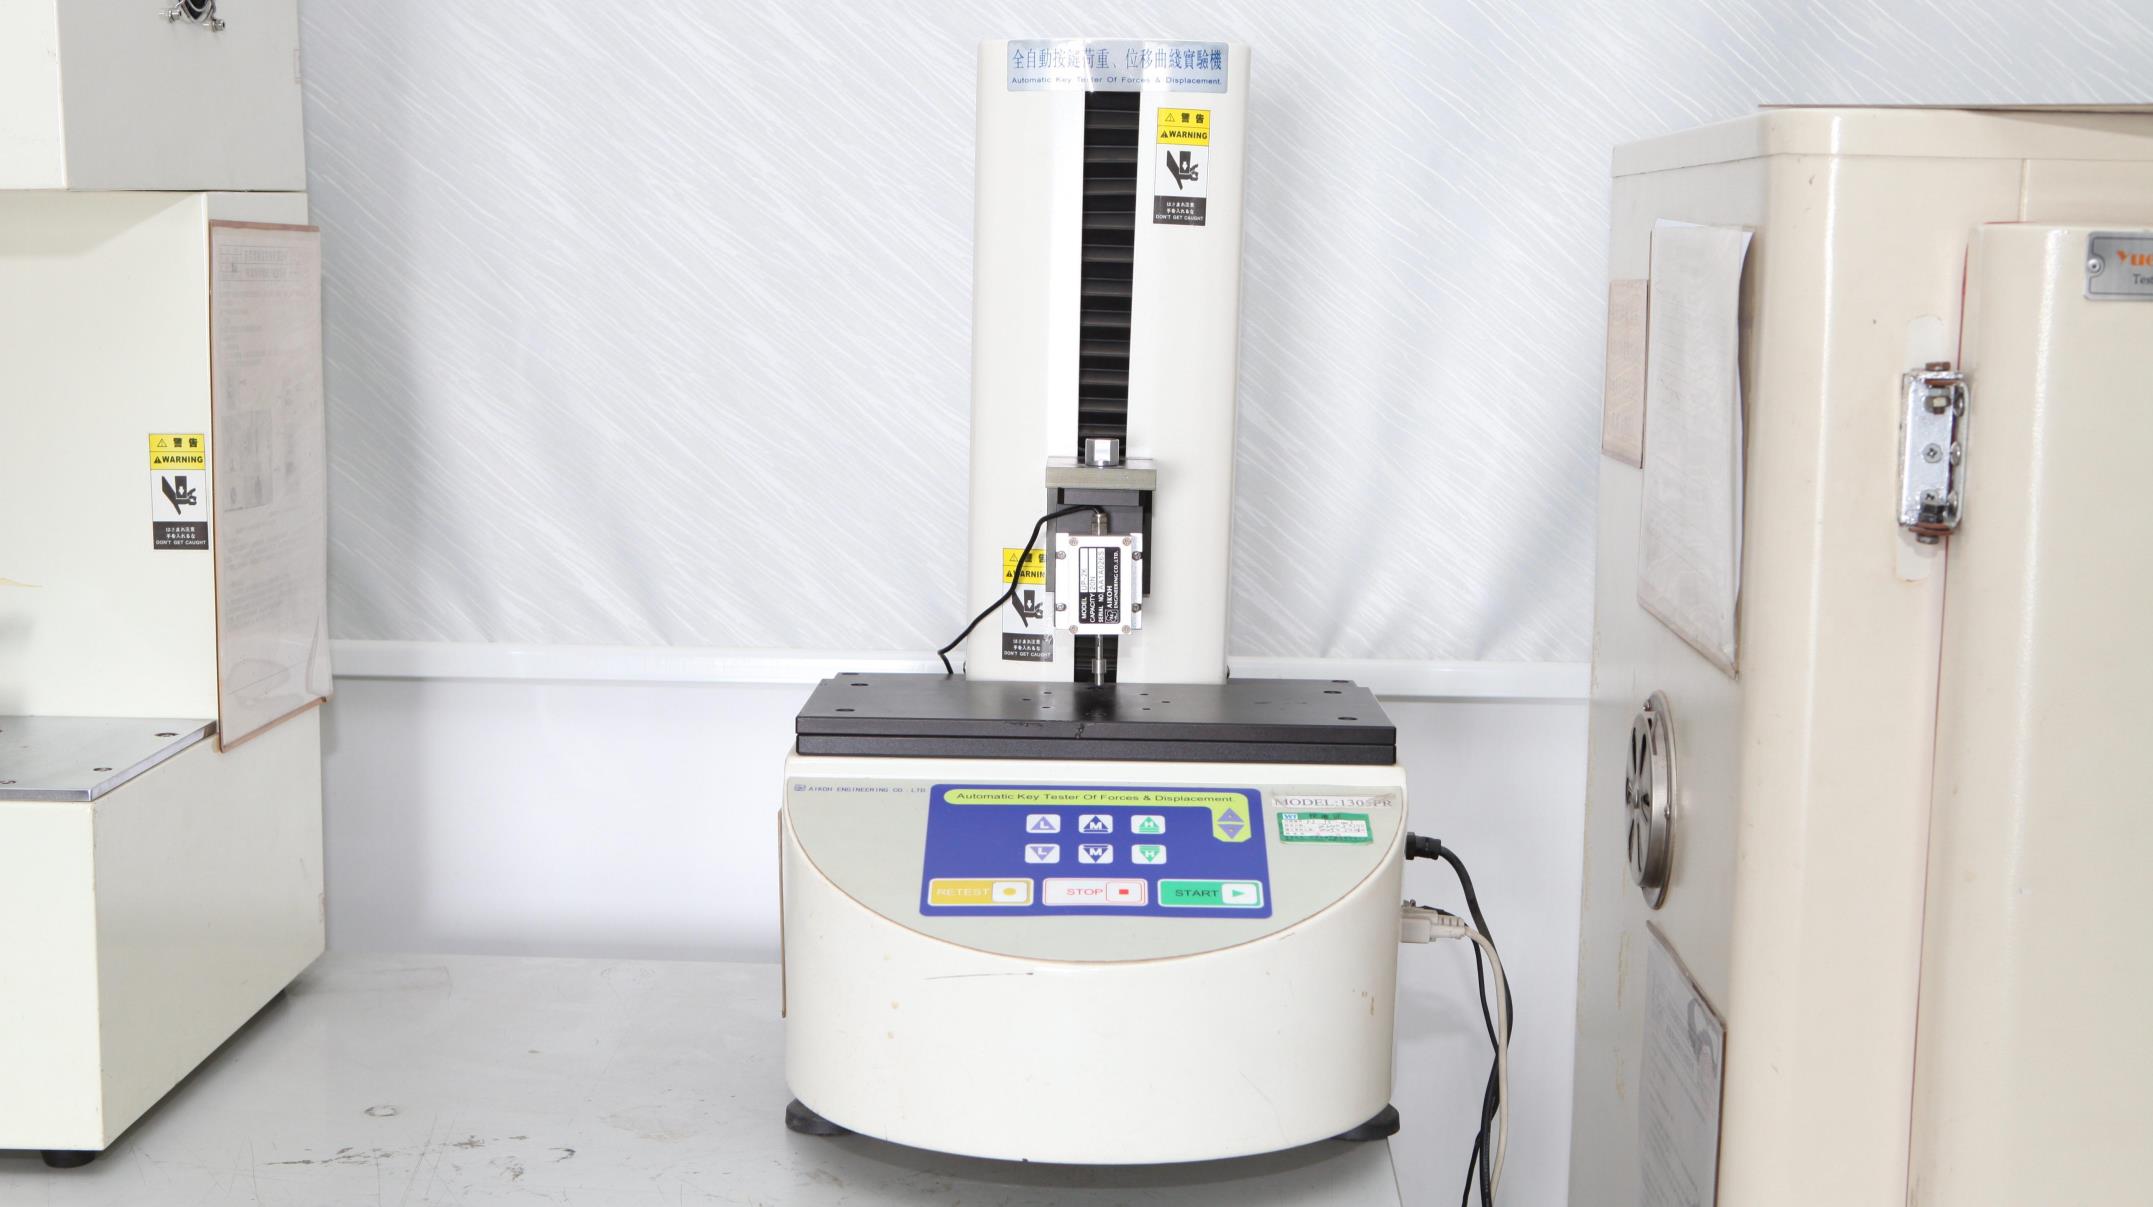
Force-Displacement Verification
Curve graphing of actuation force (typically 250g - 450g), tactile return ratio, snap click ratio, and displacement depth for identical tactile consistency.
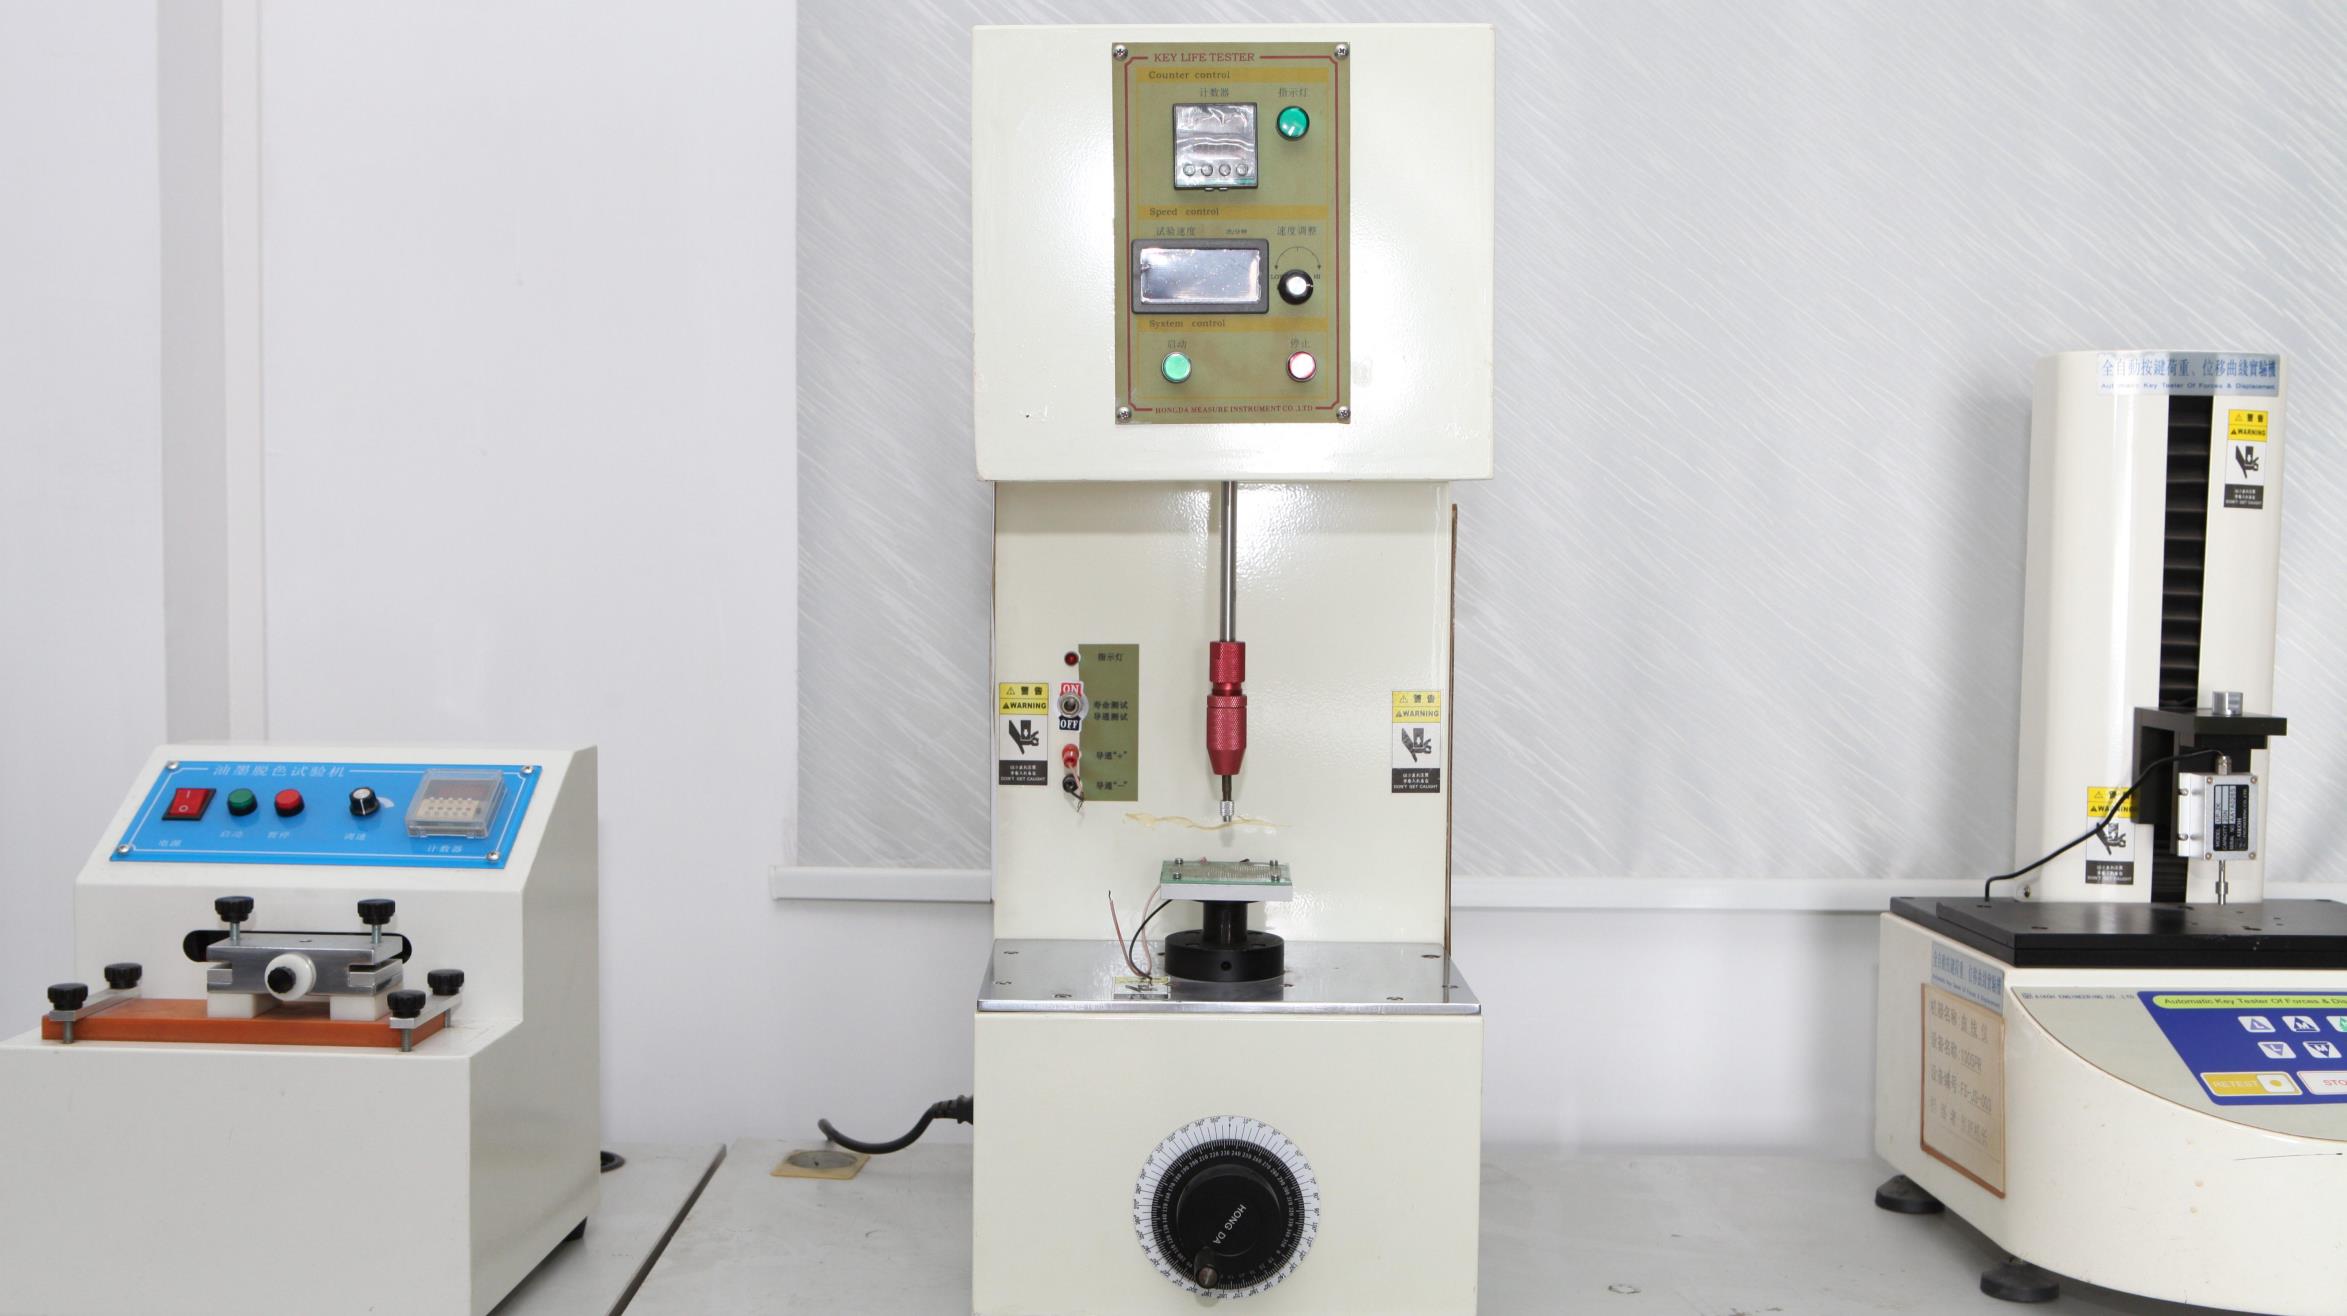
Key Actuation Life Tester
Pneumatic cycling testers stress-testing stainless metal snap-domes and silicone pills to 1,000,000 - 5,000,000 continuous actuations under load.
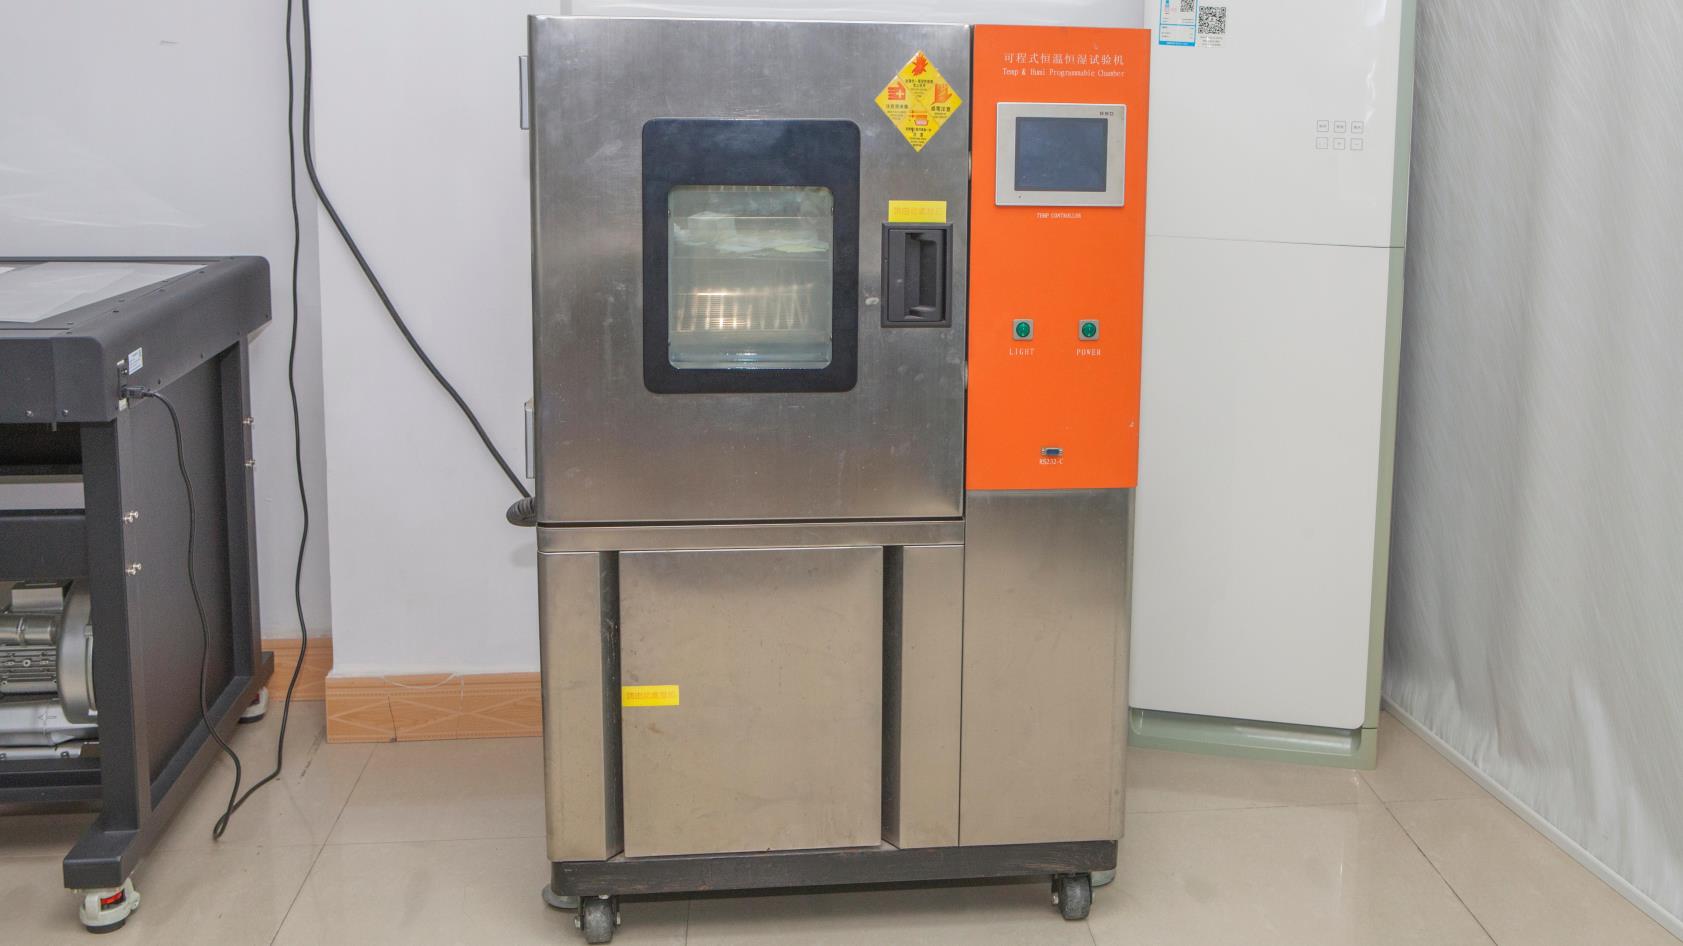
Thermal & Humidity Cycling
Stress-testing material bonding and circuit conductivity across temperature limits (-40°C to +85°C) and relative humidity up to 95% RH.
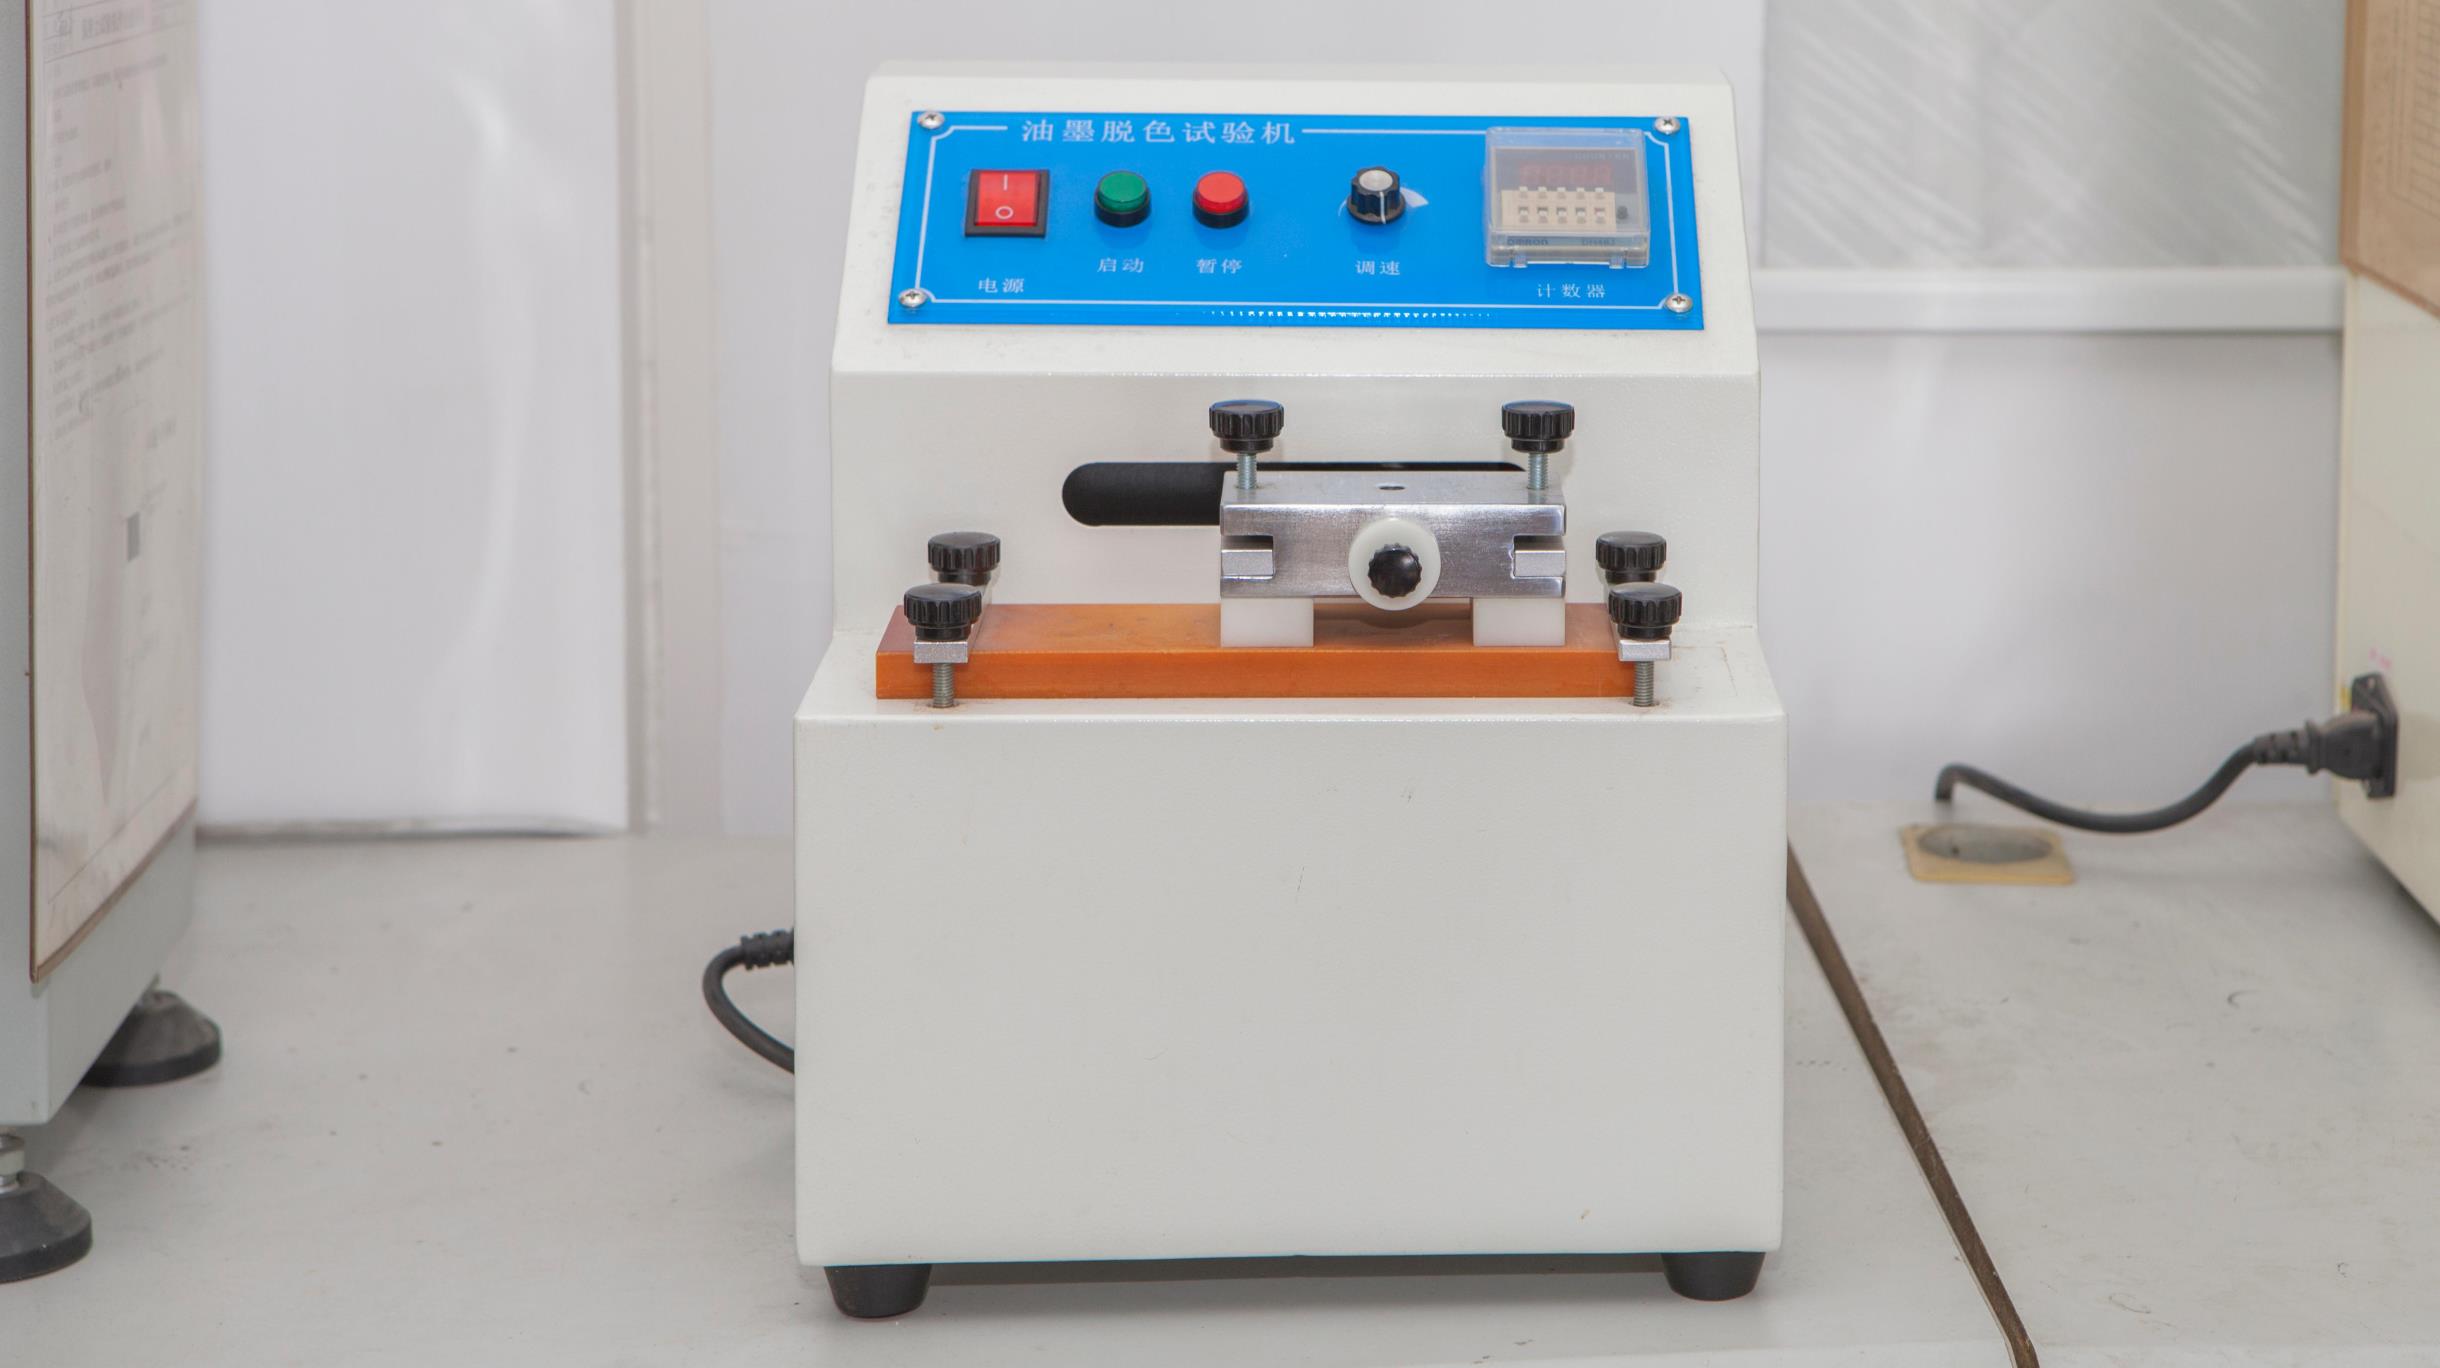
Ink Abrasion & Solvent Tester
Standardised RCA tape abrasion, linear pencil hardness tests (up to 4H-6H), and solvent resistance rub tests (MEK, alcohol, and mild acids).
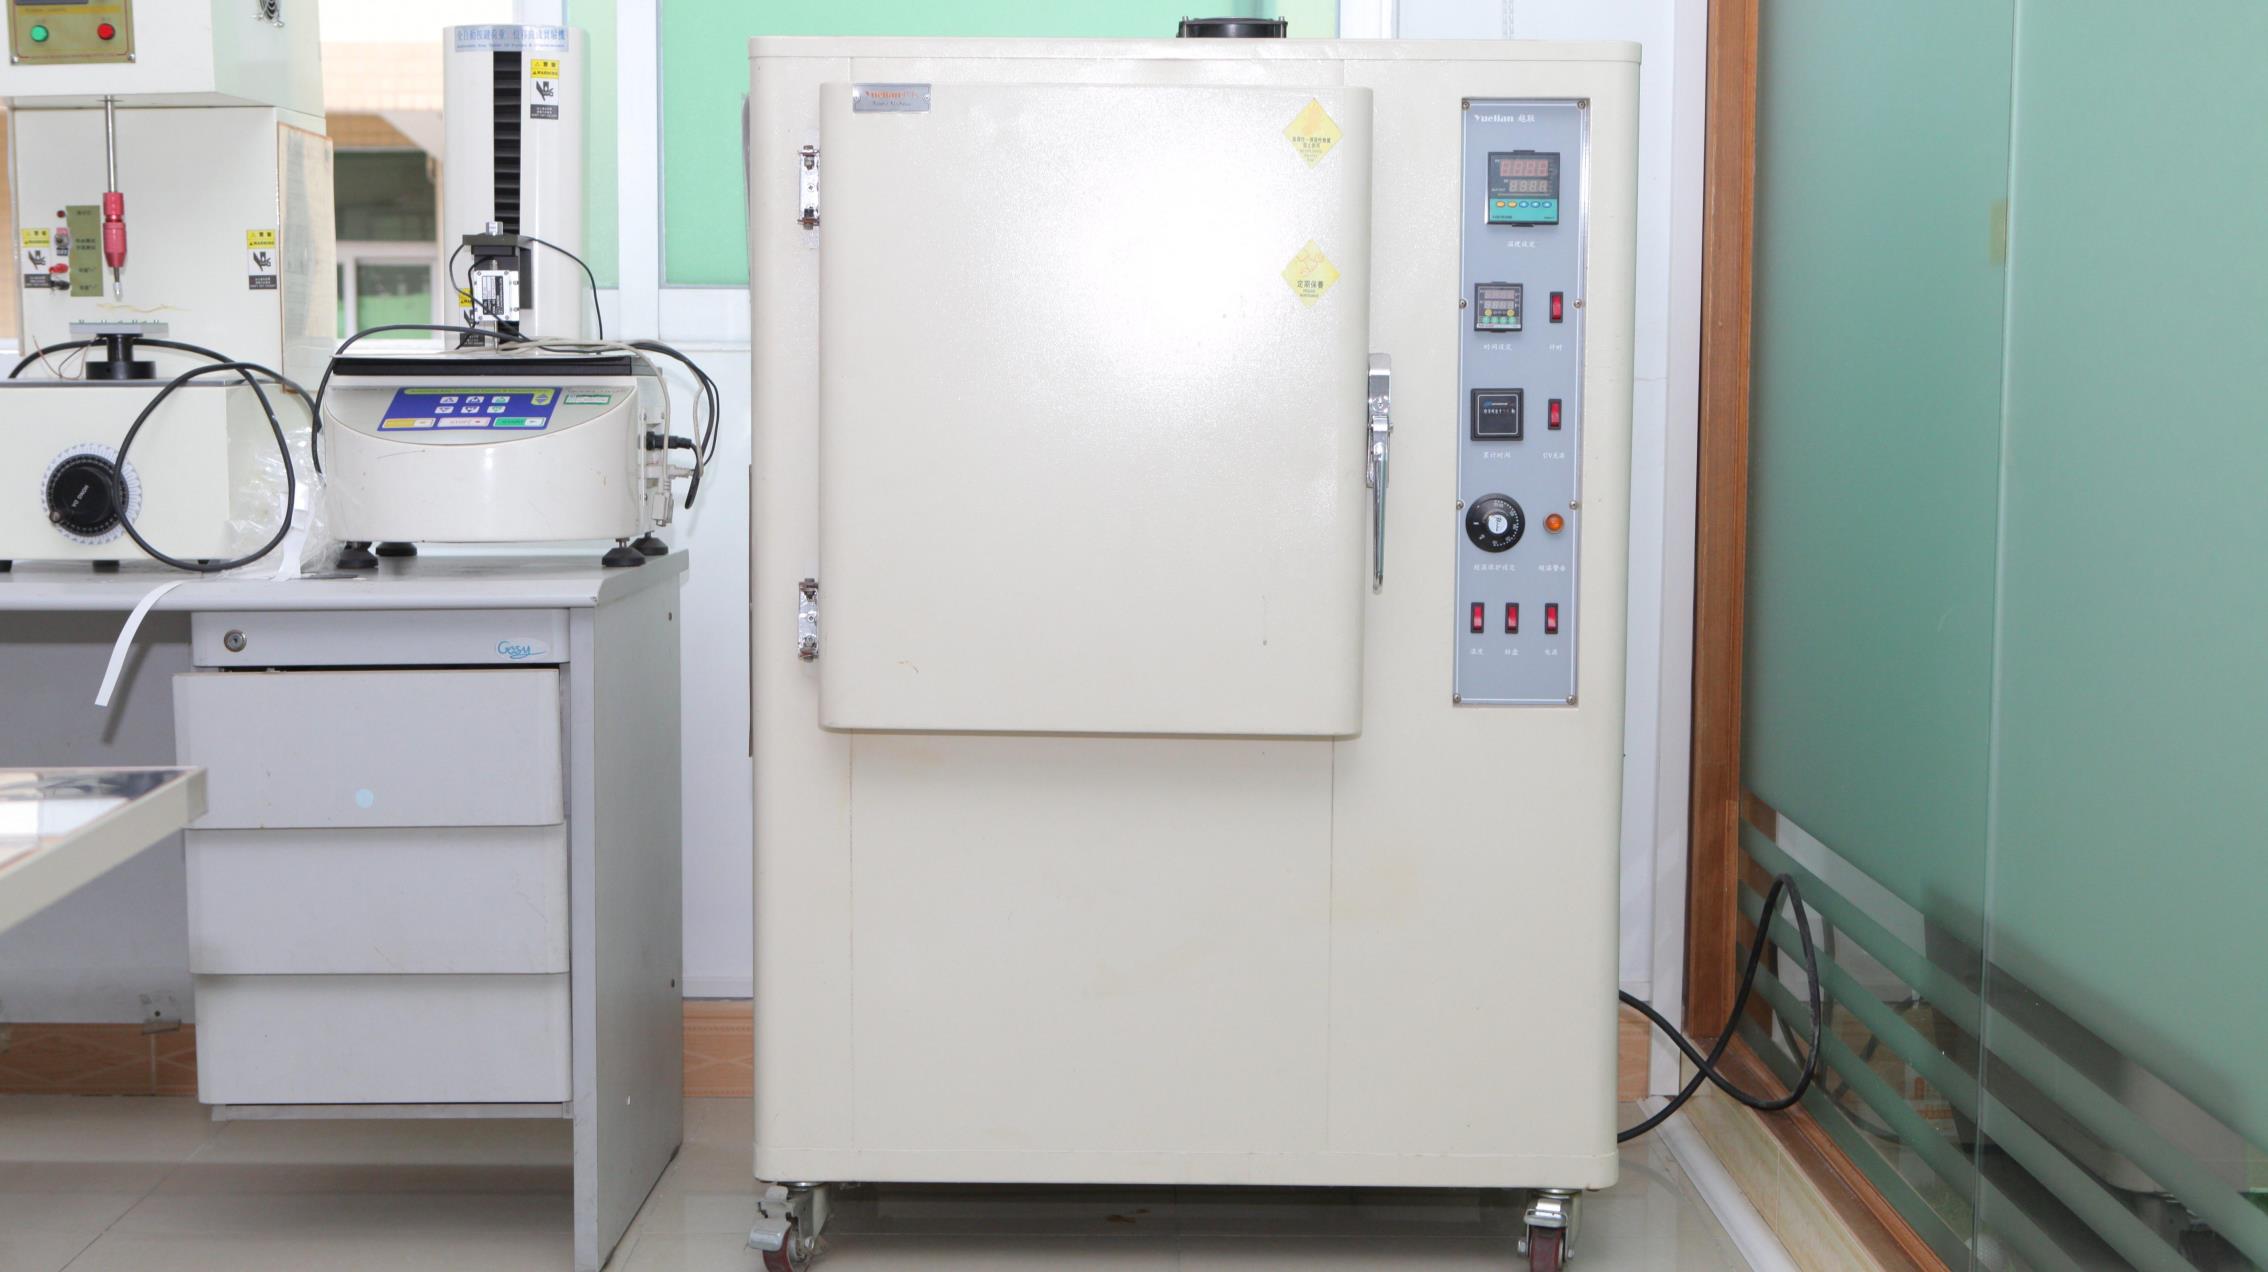
UV Weathering & Yellowing Test
Accelerated solar and UV spectral radiation checking optical transparency, clarity of LCD display windows, and colour fastness of decorative pigments.
Procurement Knowledge Base
Frequently Asked Questions by London Engineers & Buyers
Direct technical answers addressing lead times, tool investments, compliance, and design exchange protocols.
What design files and technical data are required to initiate an accurate quotation?
To provide a detailed DFM assessment and formal quotation within 24 hours, our engineering office requires:
Mechanical Geometry: 3D CAD models (STEP, IGES, or SolidWorks) detailing overall dimensions, cutouts, rib structures, and housing tolerances.
Graphic Overlay Layout: 2D vector files (Adobe Illustrator .AI, DXF, DWG, or vector PDF) specifying PMS Pantone or RAL colour designations, transparent/tinted display window coordinates, and surface texture zones (selective gloss vs matte).
Circuit & Electrical Architecture: Schematic netlist, switch matrix mapping, LED pinout configurations, tail exit orientation, connector manufacturer part number (e.g., Nicomatic, Berg, Amphenol FCI, or standard 2.54mm / 1.0mm pitch ZIF tails).
Environmental Parameters: Target IP sealing level (e.g., IP65, IP67), tactile actuation force preferences (standard 280g, 350g, or 450g), operating temperature ranges, and regulatory standards (RoHS, REACH, UL94 flammability ratings).
How does AXRU support early-stage London design prototypes with low volumes?
We recognise that product development cycles across London's tech accelerators require functional physical prototypes before unlocking volume investment capital. For traditional membrane switches, capacitive panels, and graphic overlays, we provide engineering sample runs with low minimum order quantities (MOQs starting from 100 units). For IMD/IMF assemblies involving injection molding, our tooling engineers construct rapid aluminum pilot molds or modular insert mold bases, significantly reducing upfront NRE tooling costs and lead times during Beta trials.
What is the standard tooling and manufacturing lead time for delivery to the UK?
Standard lead times follow a predictable phased schedule:
DFM & Fabrication Drawings: Completed and submitted for client sign-off within 2 business days.
Prototype Tooling & Membrane Samples: Fast-track sample delivery in 10 to 14 working days.
Hard Tooling & IMD Injection Molds: Precision steel injection tooling delivered in 25 to 35 calendar days.
Logistics Transit to Greater London: We utilise direct express air freight (DHL, FedEx, UPS) arriving at London Heathrow (LHR) within 3 to 5 business days, with all customs documentation, commodity codes, and commercial invoices prepared in strict accordance with UK Trade Tariff requirements.
How are IP67 and IP68 waterproof ratings guaranteed on membrane and IMD assemblies?
Achieving reliable hermetic sealing requires three coordinated engineering controls. First, we utilise automotive-grade double-sided acrylic foam adhesives (3M 200MP, 3M 300LSE, or 3M VHB series) cut with continuous uninterrupted perimeter sealing rings, ensuring the circuit chamber remains isolated from moisture entry. Second, the flexible connector tail exits are routed through perimeter silicone gaskets or potted with dielectric polyurethane barriers. Third, with full IMD/IMF integrated fascias, the structural polymer forms a solid resin boundary around the circuit, delivering robust and persistent IP67/IP68 ingress protection without relying solely on manual adhesive gaskets.
Can AXRU provide full material declarations for UKCA, CE, REACH, and RoHS compliance?
Yes. As an established direct exporter to European, UK, and American industrial equipment manufacturers, Dongguan AXRU Electronics ensures all raw materials—films (PET, PC), conductive silver inks, carbon tracks, copper FPC bases, adhesives, SMD LEDs, and mold resins—are fully certified compliant with EU/UK RoHS Directives (2011/65/EU and 2015/863) and REACH Regulation (EC No 1907/2006) for Substances of Very High Concern (SVHC). Full material safety datasheets (MSDS) and batch inspection reports are archived and accessible for audit.
What backlighting architectures do you recommend for low-light or outdoor control panels?
Depending on power budgets, profile thickness, and illumination uniformity requirements, we deploy three core backlighting topologies:
Light Guide Film (LGF): An optical-grade micro-etched acrylic or polycarbonate film layer that couples with side-firing ultra-thin SMD LEDs. LGF distributes light evenly across complex keypad legends with low power draw and ultra-thin profile (<0.8mm).
Discrete SMD LED Cavities: LEDs mounted directly onto the internal PET or FPC layer beneath custom-embossed light-diffusing windows. Best suited for status indicators and high-contrast night visibility.
Electroluminescent (EL) Lamps: Thin phosphorescent sheets generating uniform surface luminescence with minimal heat emission, optimal for aerospace, marine, and specialist military consoles.
Transform Your Next London HMI Project with Factory-Direct Precision
Consult directly with our Dongguan engineering team. Send your 2D graphics, 3D CAD files, or legacy component specifications today for a comprehensive DFM review, stack-up recommendation, and rapid quotation.