Core Interface Assemblies for Home & Commercial Appliances
Explore verified HMI interface modules manufactured directly at our Intertek-audited Dongguan facility. Every product line provides scalable mechanical layouts, calibrated tactile dome curves, capacitive noise shielding, and bespoke decorative finishing designed for Western European environmental compliance.
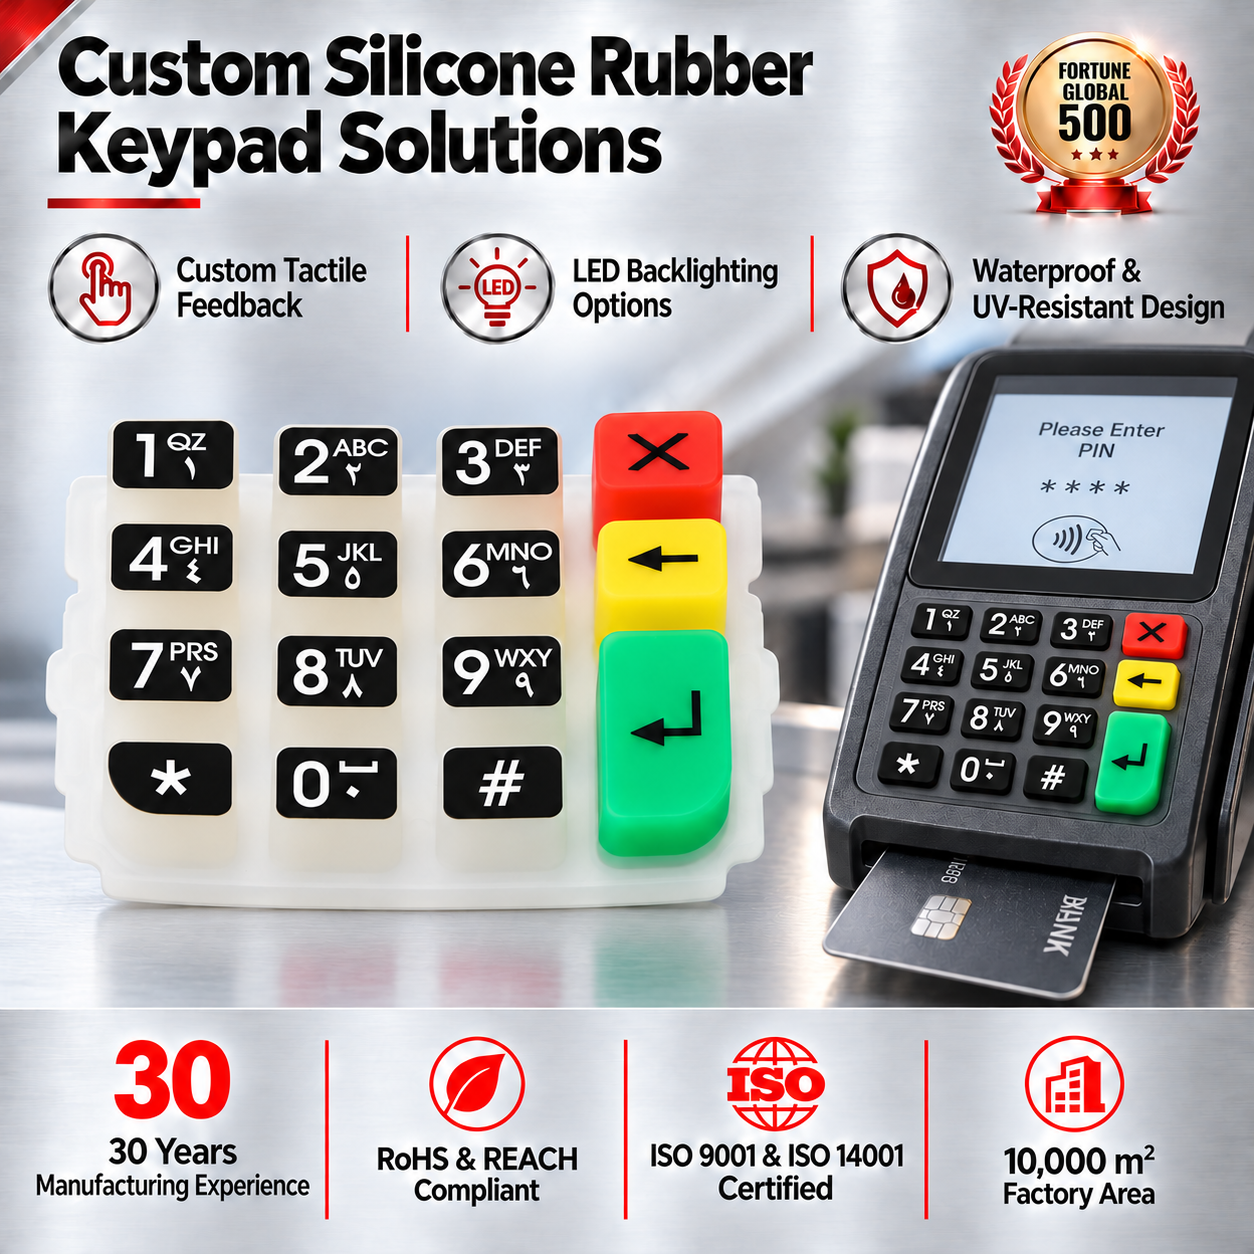
Electronic Soft Tactile Switch Plastic Silicone Button Elastomer Rubber Keypad Contact Strip for Home Appliance
- Actuation Force: 120g – 350g (±15g)
- Cycle Durability: >1,000,000 Operations
- Conductive Pill: Low-Ohm Gold/Carbon
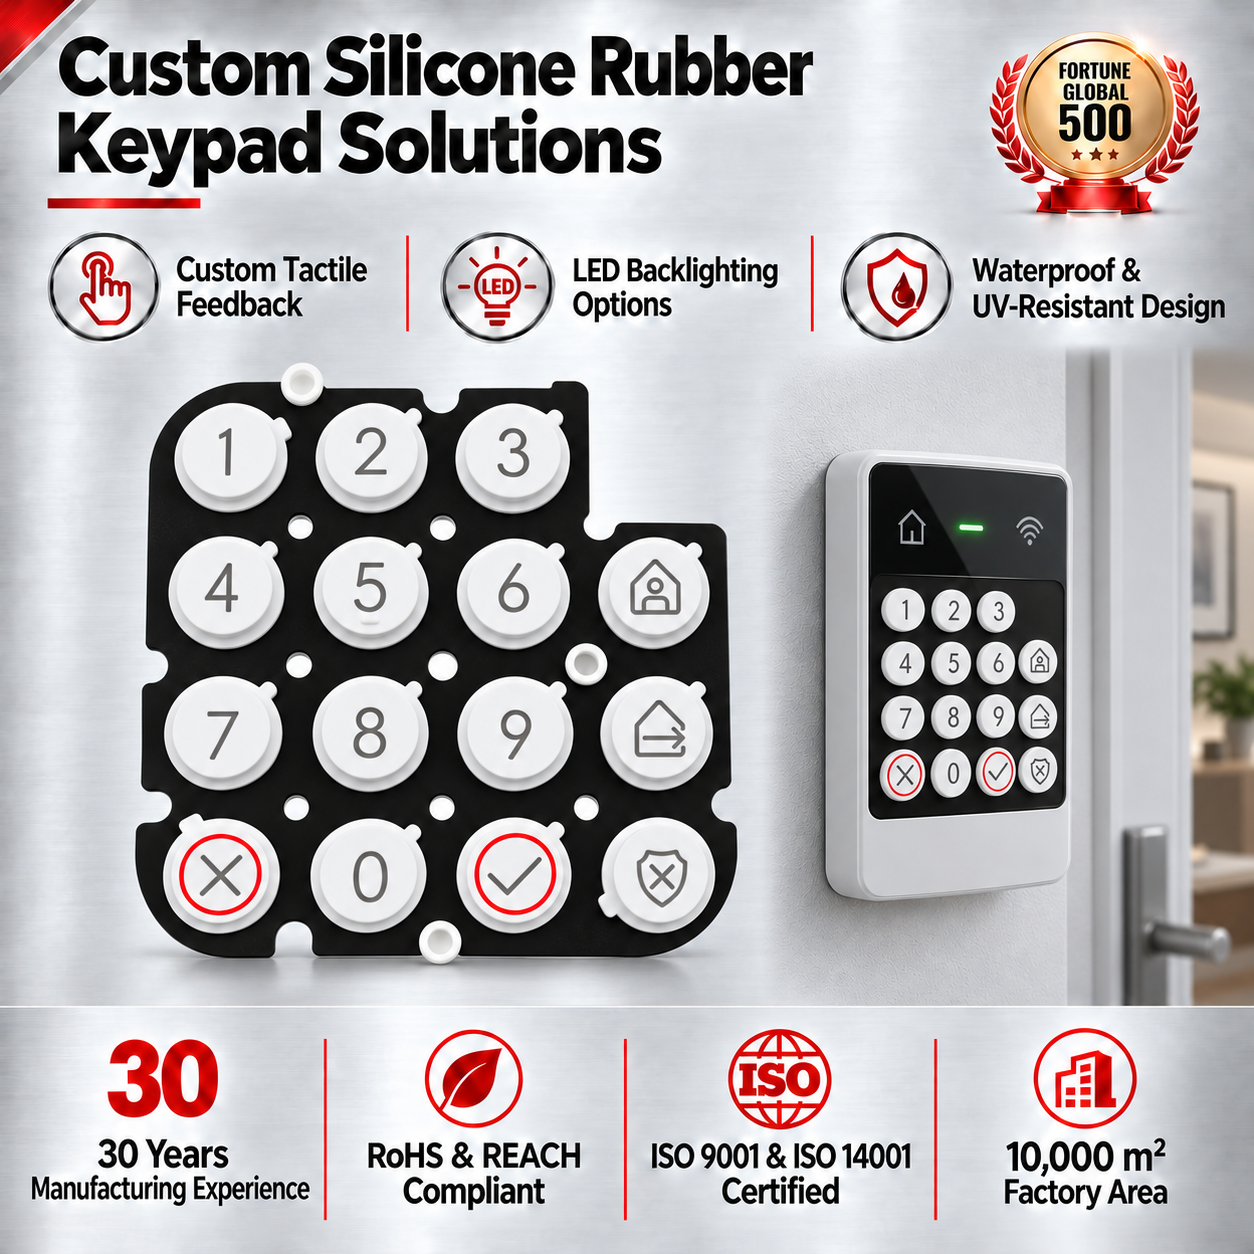
Factory Wholesale Numeric Conductive Silicone Rubber Keypad Panel Embossed Buttons for Home Appliances
- Surface Coating: Matte PU / UV-Cured
- Contact Resistance: <100 Ω Conductive Ink
- Laser Etching: Multi-Color Backlit Ready
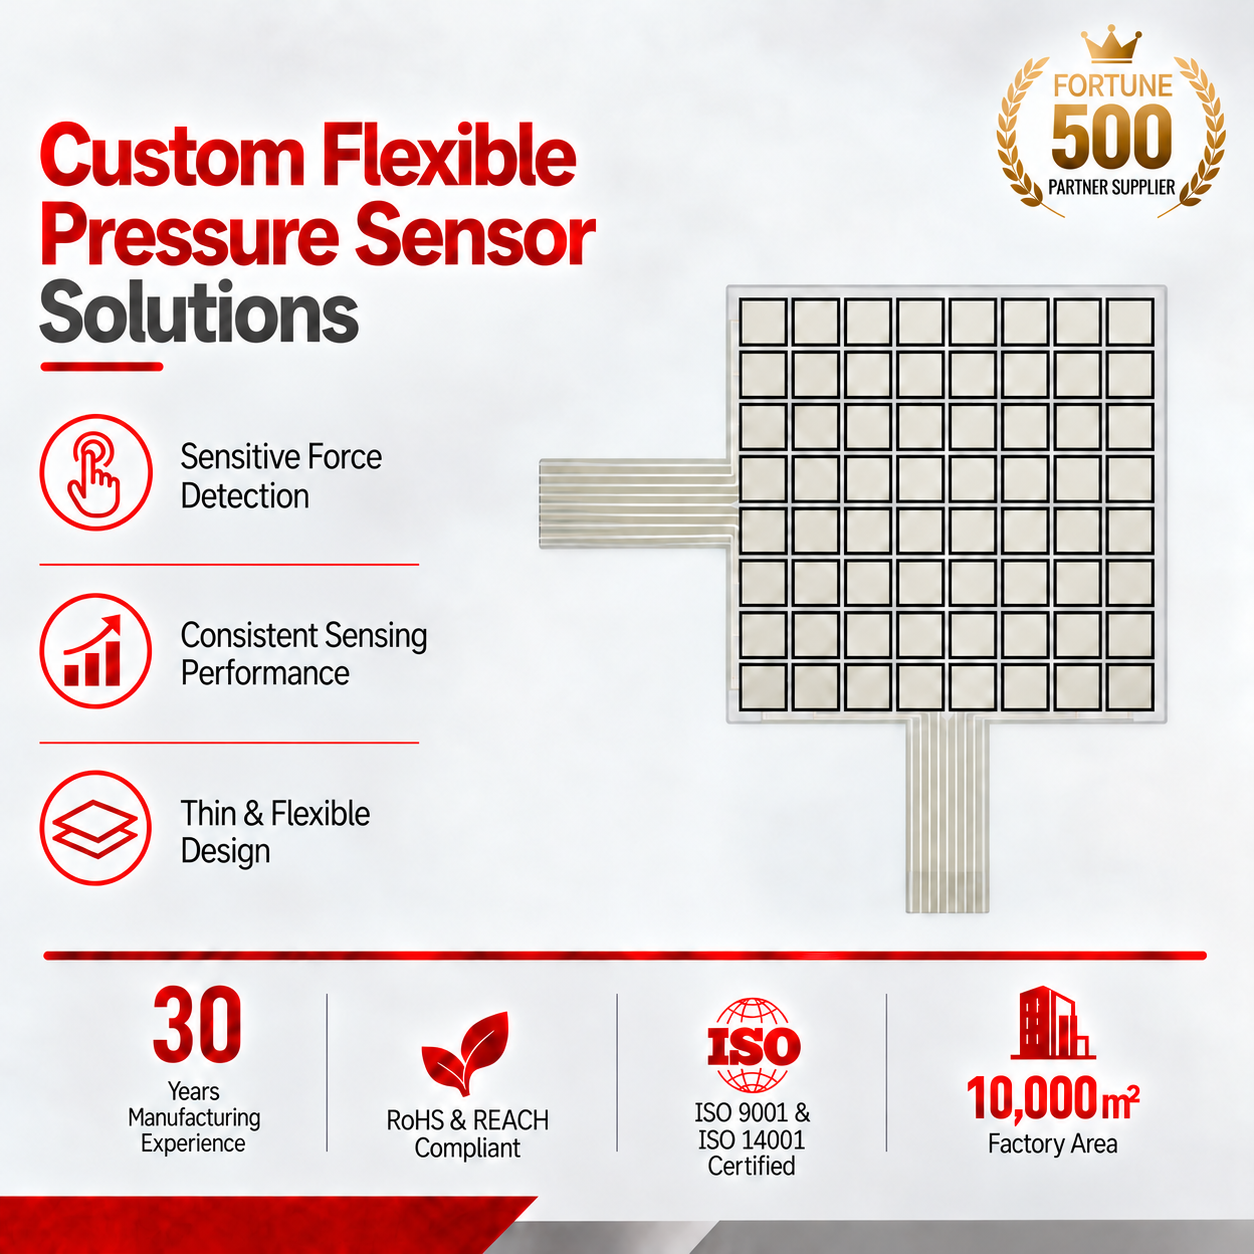
Customized Flexible Thin Film Tactile Intelligent Sensing Tactile Mirror Pressure Sensors High Sensitivity Bend Pressure Sensors
- Sensing Range: 20g – 10kg Continuous
- Substrate: Optically Clear Thin PET
- Response Latency: <5ms Ultra-Fast
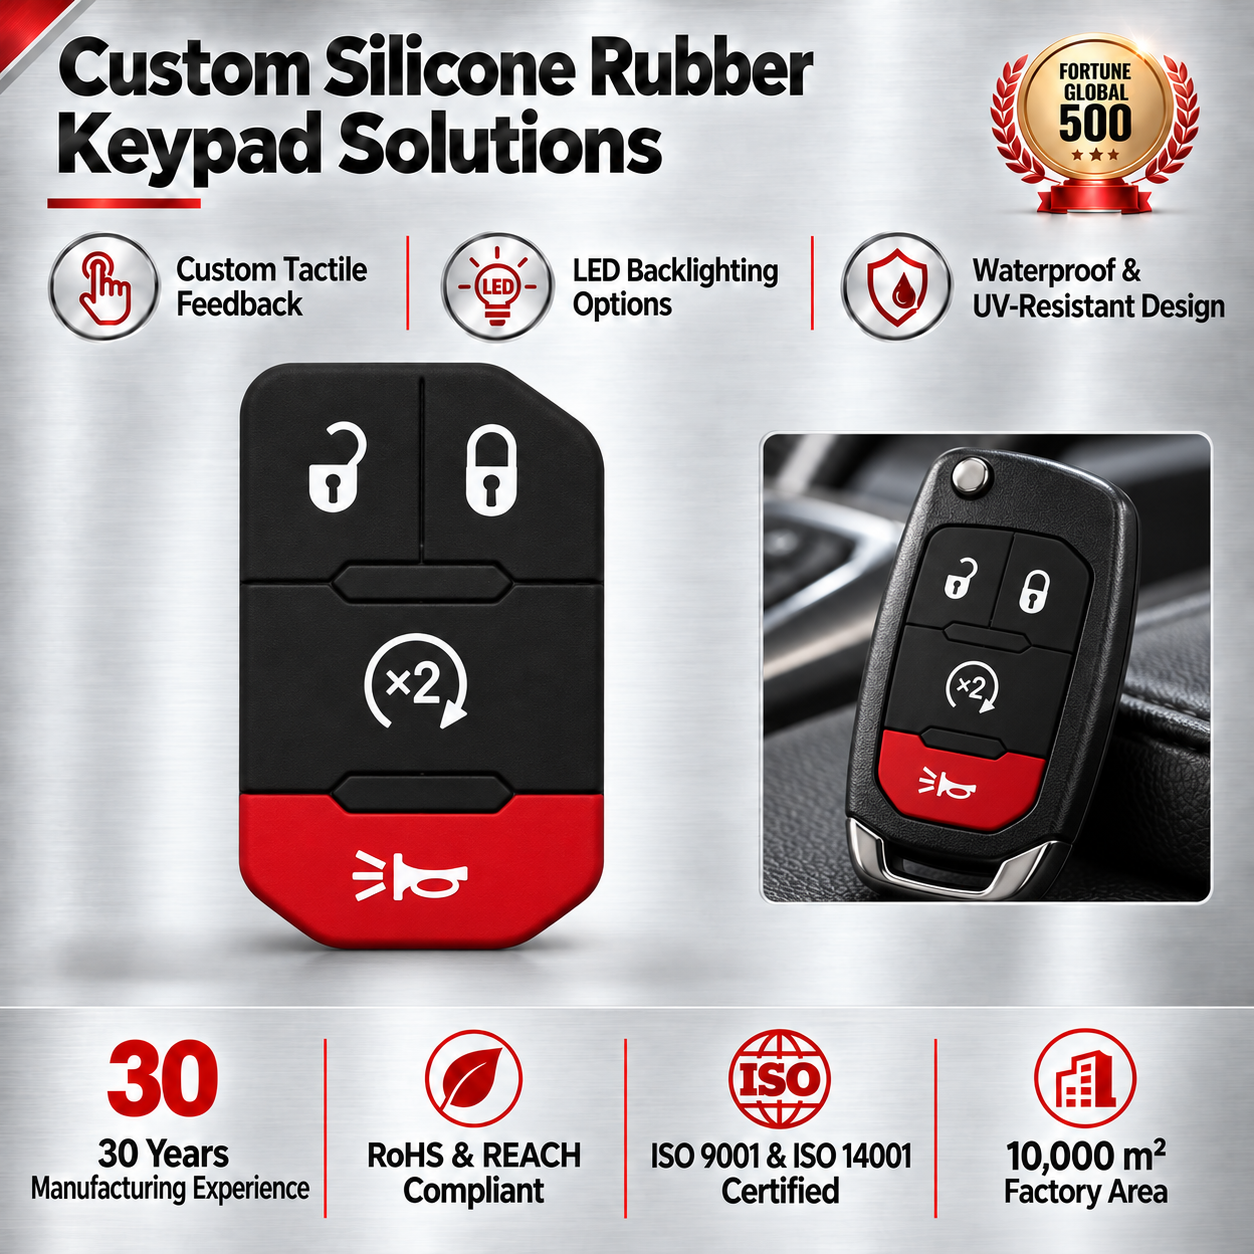
Waterproof Silicone car key Cover Press Button Rubber Keypad 4 Buttons with Printing Vehicle Wholesale Exporter
- Sealing Grade: IP67 Ingress Rated
- Shore Hardness: 50° – 70° Shore A
- Silkscreen Ink: Abrasion-Resistant Silicone
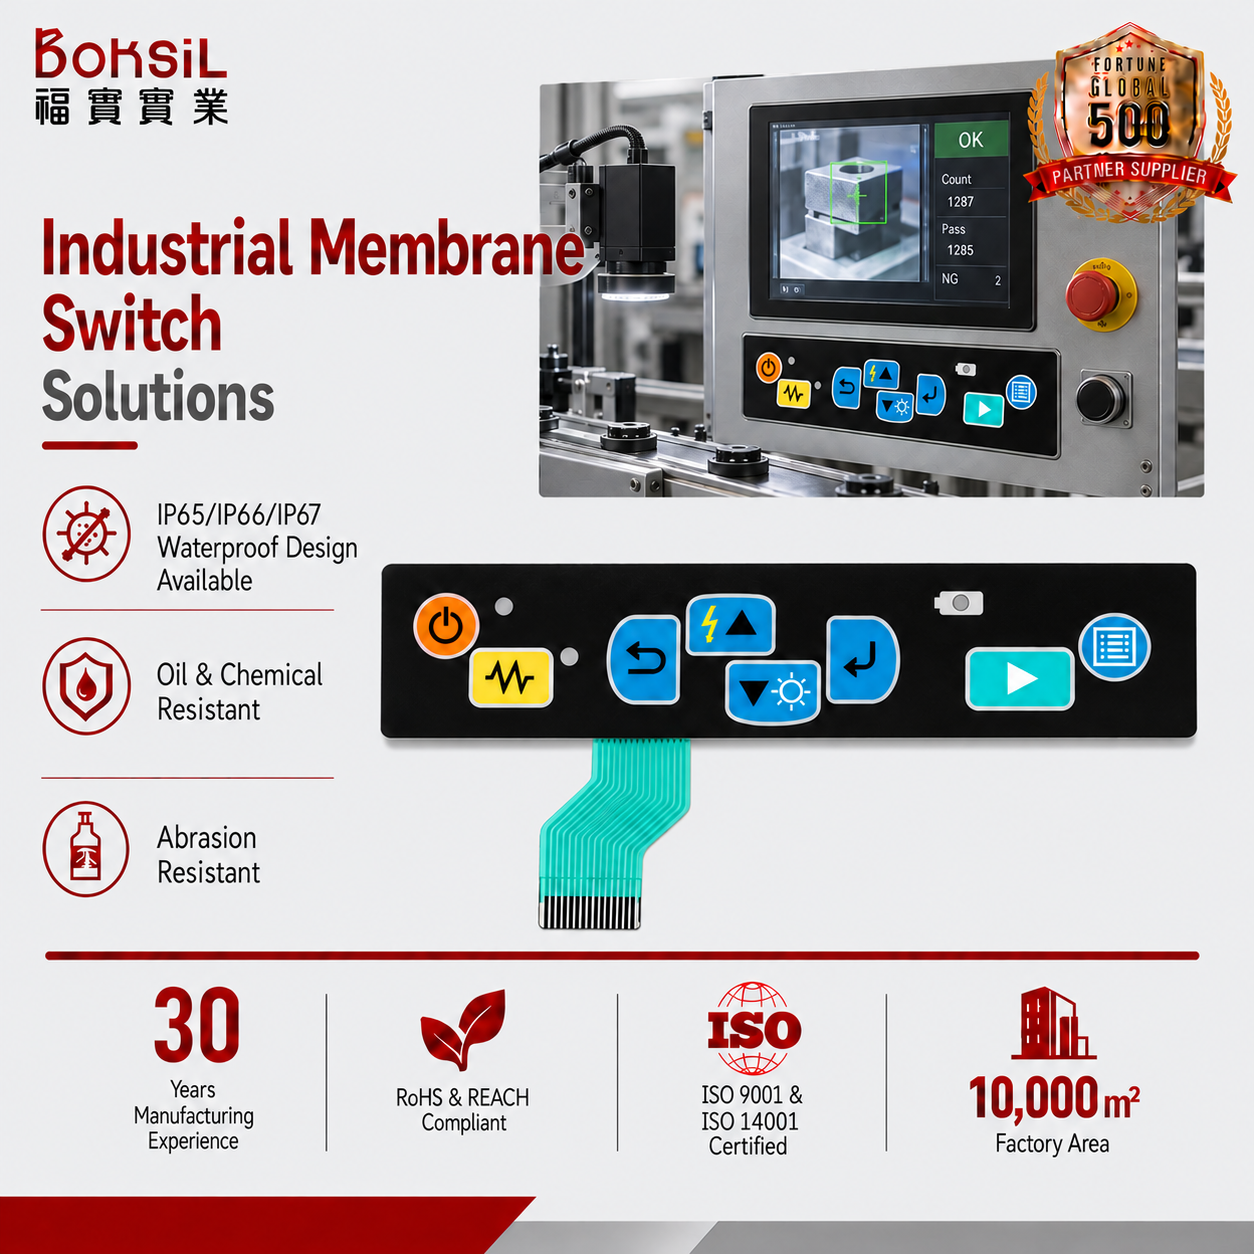
Custom Capacitive Touch Screen Panel Screen Printing Graphic Overlay Membrnae Switch for Home Appliance
- Front Substrate: Chemically Hardened Glass/PMMA
- Slide/Wheel Touch: Custom Electrode Layout
- Shielding: Rear Ground Silver Grid Layer
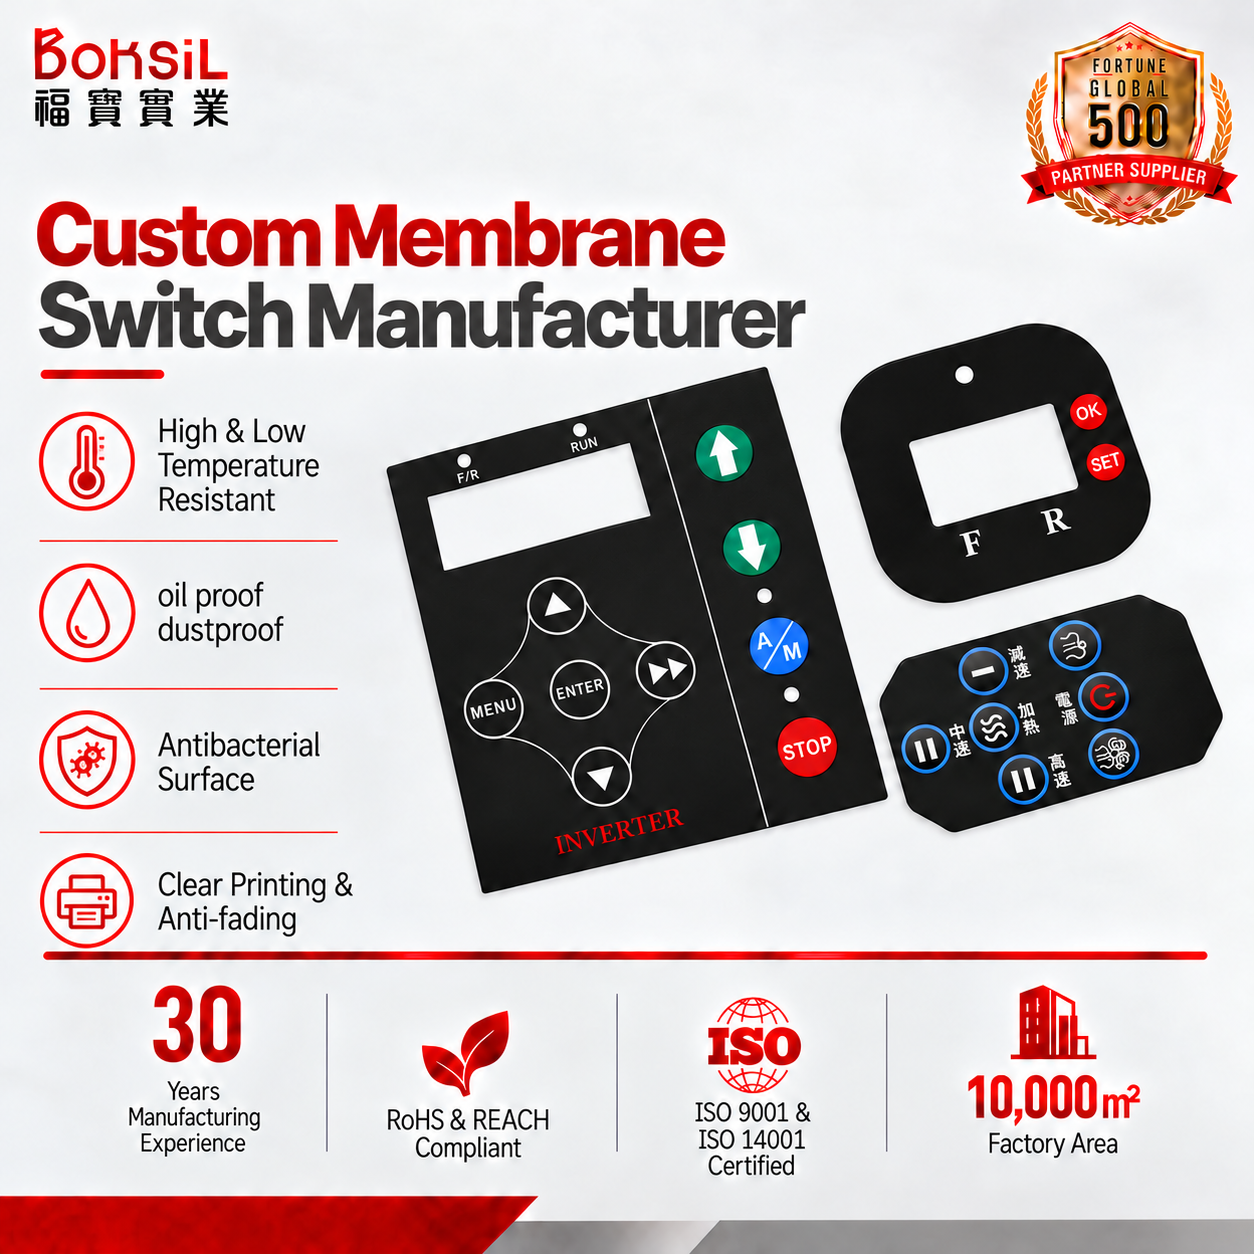
OEM/ODM Factory Front Control Electronic Panel Polycarbonate Membrane Switch Graphic Overlay
- Base Film: Lexan™ PC / Autotex™ PET
- Display Windows: High-Clarity Tinted / Dead-Front
- Backing Adhesive: 3M 467MP / 3M 468MP High Tack
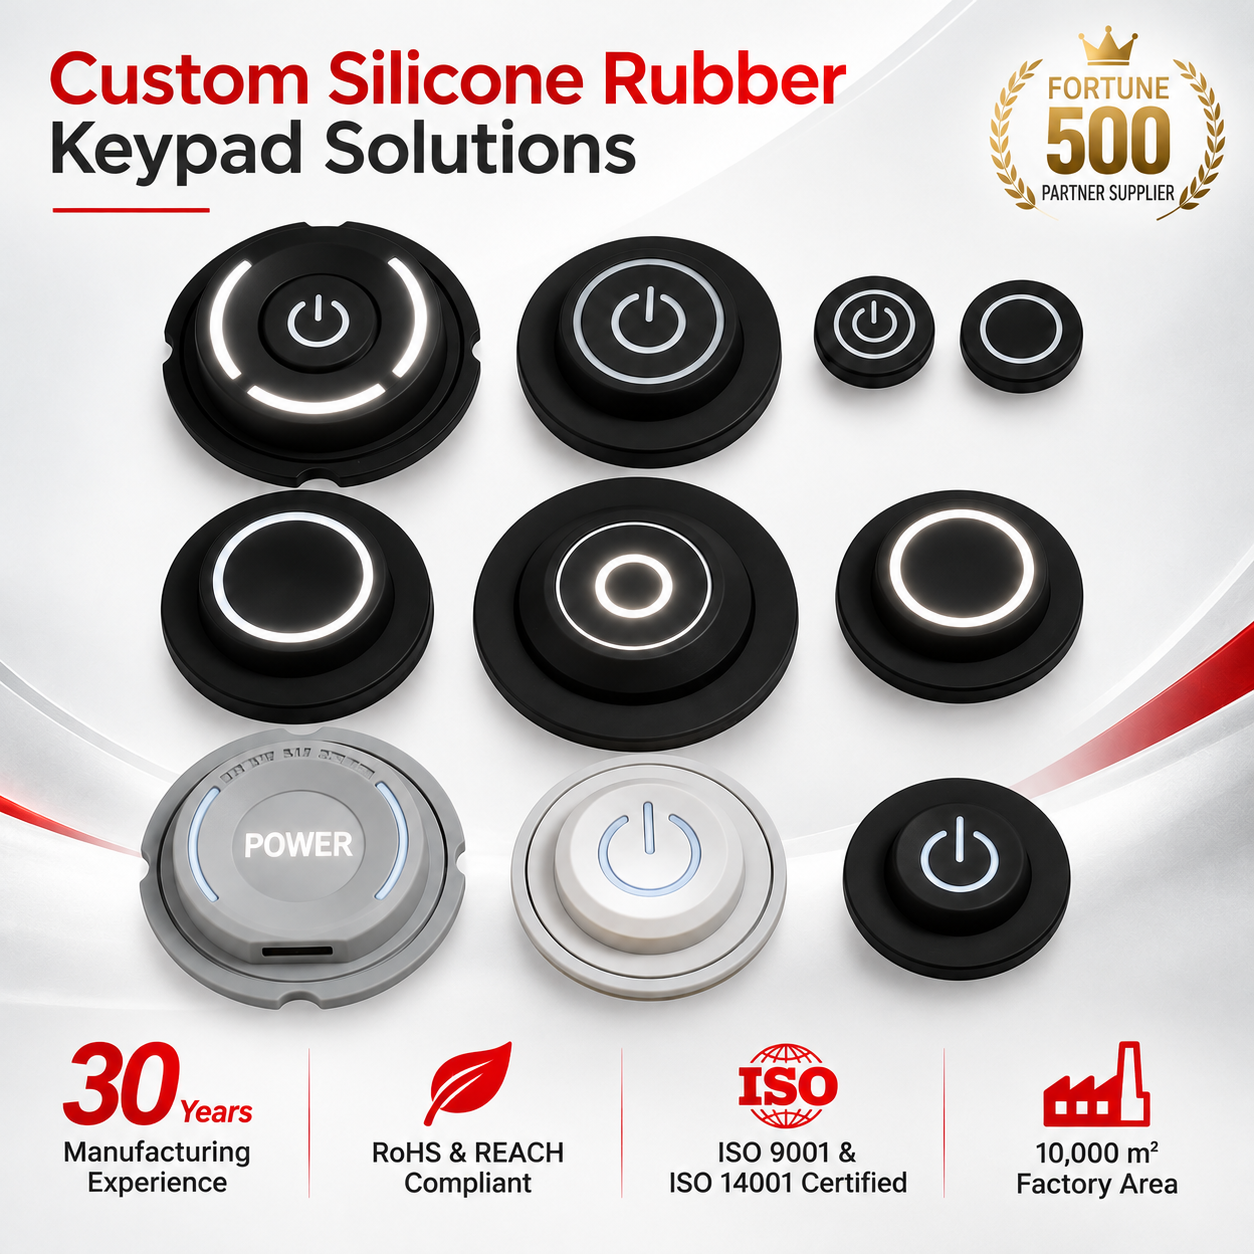
Single Tactile Cap Power Custom Silicone Rubber Button Keypad Multicolor Backlit Controller Replacement Membrnae Switch
- Illumination: Translucent Silicone Light Guide
- Switch Style: Stainless Steel Click Dome
- Tactile Feedback: Crisp Ergonomic Snap Ratio
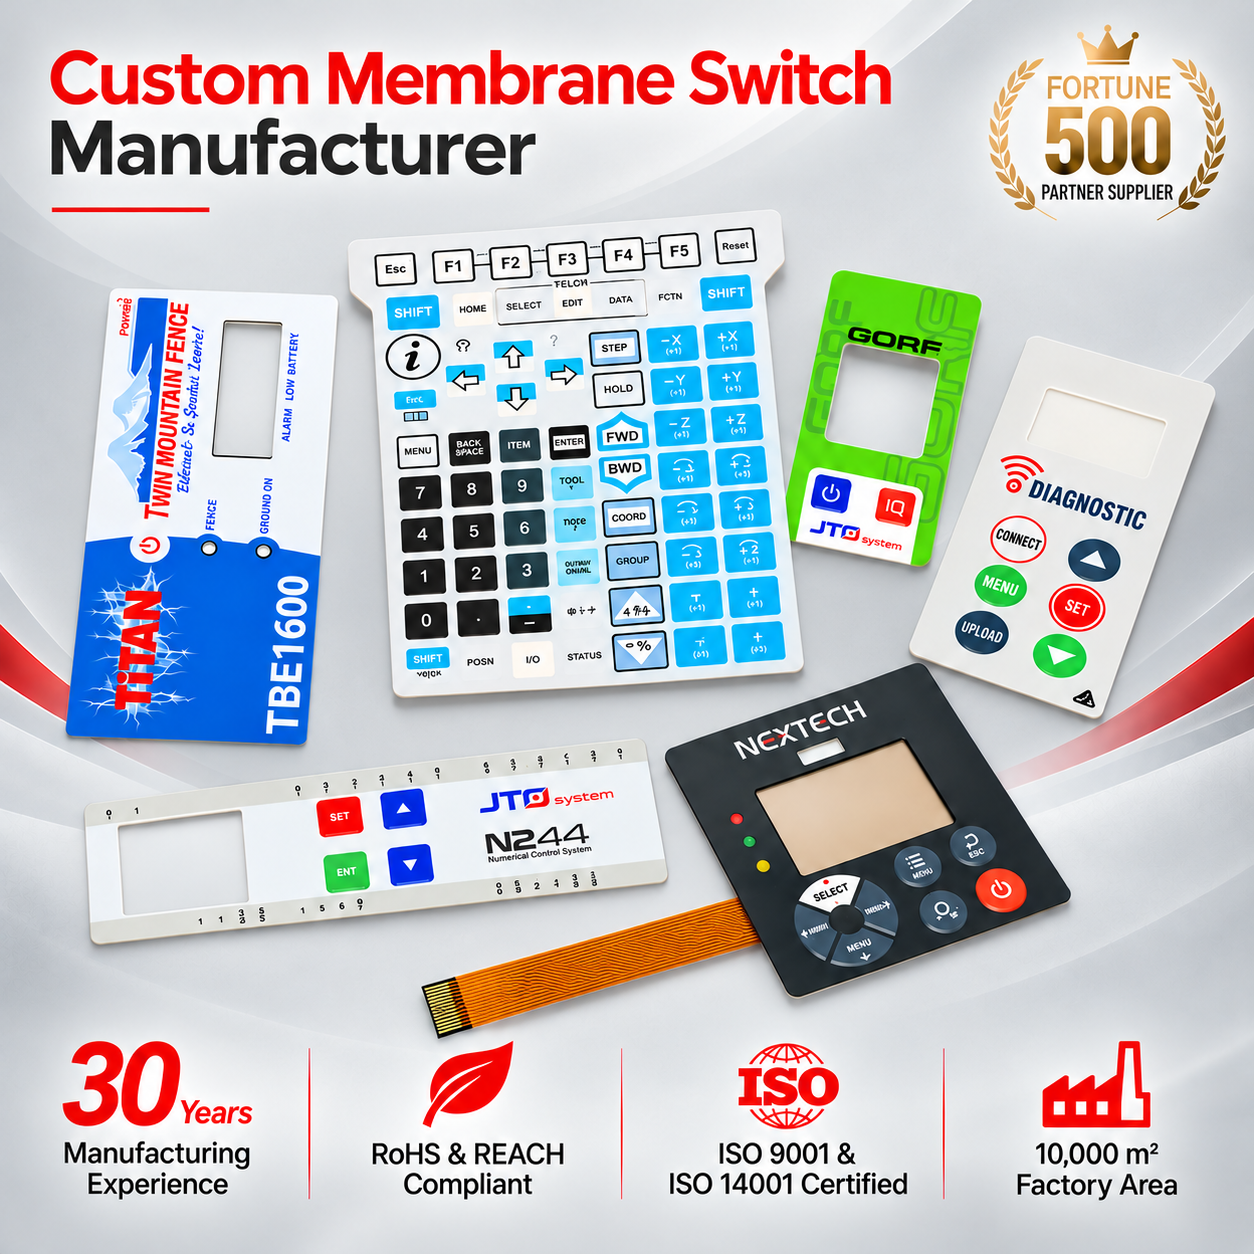
High Quality China Factory Direct Membrane Switch Graphic Overlay Embossed Button Flat Industrial Panel Product
- Embossing: Pillow / Rim Tactile Perimeter
- Circuit Layer: Printed Silver-on-Polyester
- Connector Pitch: 1.0mm / 2.54mm ZIF Standard
Equipped with Class 1,000 and 10,000 dust-free cleanrooms, dedicated automated screen printing, CNC laser die-cutting, and SMD placement cells in Dongguan, China.
In-house mechanical, chemical, and electrical engineers conducting comprehensive DFM reviews, layer stack-up optimization, and circuit schematics within 24 hours.
Every delivered batch undergoes 100% automated electrical continuity testing, dome snap inspection, environmental humidity soak, and optical alignment verification.
HMI Interface Engineering for the Strasbourg & Upper Rhine Manufacturing Corridor
Situated at the intersection of French precision engineering and the German industrial ecosystem along the Rhine Valley, Strasbourg and the broader Grand Est administrative region serve as an influential nexus for commercial catering hardware, climate management, smart building controls, and specialized home appliances. Appliance OEMs throughout this region demand human-machine interfaces (HMIs) that balance strict culinary hygiene standards, long-term tactile durability, chemical washdown survivability, and contemporary aesthetic appeal.
As an established OEM/ODM direct manufacturer, Dongguan AXRU Electronics Co., Ltd. bridges the gap between high-volume, cost-effective Asian component fabrication and Western European design stringency. By integrating in-house screen printing, cleanroom membrane lamination, precision silicone compression molding, and optical adhesive bonding into a unified quality management framework, we provide procurement directors and R&D teams across Strasbourg with fully vetted, custom-tailored interface subsystems.
Our manufacturing protocol is configured around end-to-end traceability. From initial mechanical CAD and Gerber file validation to mass manufacturing and final automated pinout verification, our engineering teams ensure that each membrane switch, capacitive sensor array, and silicone keypad assembly arrives at your assembly lines ready for seamless plug-and-play enclosure integration.
Targeted Application Scenarios Across Grand Est Appliance Manufacturing
The regional economic fabric of Alsace features world-renowned gastronomy, specialized commercial refrigeration, wine production preservation systems, and cutting-edge residential heating equipment. Designing control interfaces for these micro-climates requires tailored material choices and mechanical configurations.
Gastronomic & Professional Culinary Ranges
Strasbourg’s commercial kitchen sector demands front panels that withstand constant oil vapor, scalding water splashes, and harsh chemical sanitizers. We utilize anti-microbial, textured Autotex™ XE polyester overlays combined with perimeter gasket potting to achieve true IP65 and IP67 washdown compliance.
Alsatian Wine Cellar & Climate Cabinets
Precision climate cabinets manufactured for regional vineyards require touch interfaces functioning continuously at 10°C – 14°C with 70%+ relative humidity. Our humidity-sealed capacitive touch panels and dead-front OLED display windows eliminate internal lens fogging and avoid false condensation triggers.
Smart Thermal Management & Heat Pumps
Under France’s RE2020 environmental building standards, smart residential heat pumps and hydronic controllers need sleek, user-friendly HMIs. We provide capacitive sliders, backlight diffusion plates, and copper FPC circuitry designed for seamless surface mounting on modern architectural control panels.
Engineering Deep-Dive: Material Selection & Interface Layer Architecture
A failure in a home appliance control interface frequently traces back to suboptimal adhesive selection, inferior plasticizer migration, or lack of environmental moisture venting. AXRU engineers optimize each interface stack-up according to specific thermal and mechanical stress profiles.
| Stack-Up Layer | Standard Material Grade | High-Spec Appliance Option | Engineering Function & Protection Metric |
|---|---|---|---|
| 1. Graphic Overlay | Autotex™ Fine/Velvet PET (150μm – 200μm) | Chemically Hardened Acrylic / Anti-Glare Glass | Reverse sub-surface printing protects legends from scratching, finger oils, UV yellowing, and cleaning detergents. |
| 2. Overlay Adhesive | 3M 467MP High Performance Acrylic | 3M 9472LE / 3M 300LSE for Low Surface Energy | Creates an impervious perimeter seal preventing steam, moisture, and cooking fat ingress into internal switches. |
| 3. Tactile Switch Matrix | Nickel-plated Stainless Steel Domes (4-Leg) | Gold-plated Domes / Custom Silicone Web Dome | Delivers crisp acoustic and tactile feedback with trip forces tuned from 180g to 350g, rated up to 5,000,000 cycles. |
| 4. Spacer Layer | Double-Coated Polyester Spacer (125μm) | Laser-vented Deaeration PET Channels | Maintains consistent dome clearance while breathing channels normalize internal atmospheric pressure during actuation. |
| 5. Circuit Substrate | Conductive Silver Pastes on Stabilized PET | Polyimide Copper Flexible Printed Circuit (FPC) | Routes electrical signals with minimal line resistance (<10Ω); copper FPC supports direct micro-pitch SMT LEDs and resistors. |
| 6. Rear Mounting Layer | 3M 468MP Adhesive Carrier (130μm) | Structural Acrylic Foam (3M VHB Series) | Bonds completed assembly securely to powder-coated steel, ABS, cast aluminum, or polypropylene appliance chassis. |
For appliances requiring illuminated nighttime usability, such as induction ranges or premium laundry consoles, we incorporate light guide film (LGF) or fiber-optic side-emitting LED arrays. This prevents hotspotting, creates clean uniform icon illumination, and minimizes active power draw to under 20mA.
Regulatory Compliance & Technological Trends in the French Appliance Sector
The European Union has enacted stringent circular economy policies and ecodesign mandates that directly impact the design of electronic sub-assemblies. Supplying equipment into the Strasbourg and French national market necessitates strict alignment with European standards:
French Repairability Index (Indice de Réparabilité)
Appliances sold in France must display clear repairability ratings. Our modular interface designs use ZIF connectors, standardized pinouts, and clean-release adhesives that allow field service technicians to replace worn faceplates without scrapping entire controller sub-assemblies.
RoHS 3, REACH & Halogen-Free Materials
All conductive inks, silicone formulations, optical spacers, and adhesives are 100% compliant with EU Directive 2011/65/EU (RoHS 3) and SVHC REACH regulations. Third-party testing certifications by SGS and Intertek accompany each raw material lot.
EMC / EMI Shielding Standards (EN 55014)
Induction cookers and motor-driven kitchen equipment produce severe high-frequency electrical fields. We integrate continuous printed silver ground grids, carbon backplanes, or conductive aluminum foils into the stack-up to eliminate spurious touch events and guarantee CE EMC compliance.
AXRU Electronics: Verified In-House Reliability Testing & Quality Rig Matrix
Located in Dongguan, our 10,000m² production site eliminates the quality and schedule risks associated with broker-based component trading. Unlike distributors who outsource core processing, we own and manage screen-printing presses, SMT placement, silicone compression tooling, and an exhaustive in-house reliability testing laboratory verified on-site by Intertek.
Key Life & Actuation Endurance
Automated pneumatic actuators cycle switches from 1,000,000 to 5,000,000 continuous operations at configured speeds, recording dome fatigue and contact resistance degradation.
Force & Displacement Curve Plotting
Micro-calibrated load cells measure exact actuation force (F1), contact closure point (F2), and return snap ratio to ensure uniform tactile sensation across all interface keys.
Tensile Peel Strength Measurement
Calibrated electronic pull testers measure adhesive bonding between overlay, spacer, and tail exit joints at 90° and 180° angles to eliminate risk of field delamination.
Ink Decolorization & Rub Abrasion
Mechanical rubbing arms evaluate ink durability against 99% isopropyl alcohol, industrial degreasers, and artificial perspiration over 5,000+ abrasion cycles.
Programmable Thermal & Humidity Chambers
Assemblies undergo prolonged thermal shock (-40°C to +85°C) and 95% relative humidity testing to ensure silver traces resist dendrite electromigration.
UV Yellowing & Environmental Xenon Exposure
Accelerated solar and ultraviolet exposure chambers verify that outdoor or kitchen-facing graphic overlays retain chromatic fidelity and optical window transparency.
Frequently Asked Questions: Sourcing Interfaces for the Strasbourg & French Market
To streamline technical evaluation and procurement workflows, our senior applications engineering team has compiled direct answers to frequent questions raised by European hardware architects.
How do you handle rapid prototyping and DFM reviews for appliance teams in Strasbourg?
Upon receiving your STEP, DXF, Gerber, or vector artwork (AI/PDF), our engineering desk conducts a 24-hour Design for Manufacturability (DFM) assessment. We review layer stack-up thickness, connector pinpitch, tail exit strain relief, tactile dome venting pathways, and dielectric insulation margins.
Functional prototypes are produced using dedicated pilot flatbed digital printers and laser die-cutting machinery in our sample laboratory within 5 to 7 business days, allowing rapid ergonomic fit checks before hard steel tooling is cut.
What is your Minimum Order Quantity (MOQ) for custom-printed overlays and switches?
To support pilot production, field trial units, and specialized commercial appliance runs, our standard minimum order quantity starts at just 100 units for custom membrane switches and graphic overlays.
For compression-molded silicone rubber keypads or complex capacitive touch panels requiring dedicated injection tooling, low-volume trial lots of 300 to 500 pieces can be arranged to support your CE certification and market validation phases before transitioning to full mass production.
How do your interfaces resist moisture ingress in high-steam cooking and cleaning environments?
Moisture ingress is the primary root cause of intermittent short circuits and silver migration in kitchen appliances. We prevent this by designing a continuous perimeter ring adhesive barrier (typically 3M 468MP or 3M 300LSE) around all active switch cavities.
Additionally, our circuit flex tails feature precision hydrophobic potting or UV-curable dielectric masks at the housing exit interface. This construction easily meets IP65 and IP67 ratings according to IEC 60529, validated through our programmable humidity test chambers.
Can you provide food-contact safe and medical-grade materials for culinary equipment?
Yes. When manufacturing silicone pushbuttons or front gaskets that may contact foodstuffs or human skin during food preparation, we utilize pure synthetic platinum-cured silicone elastomers that meet FDA 21 CFR 177.2600 and European Framework Regulation (EC) No 1935/2004.
Furthermore, front polyester graphic overlays can be treated with Microban® or silver-ion antimicrobial hardcoats to inhibit bacterial colonization across high-touch commercial interfaces.
What logistics and shipping channels do you utilize for delivery into Grand Est, France?
We provide comprehensive DDP (Delivered Duty Paid), DAP, and FOB logistics options. For urgent engineering modifications and pilot lots, express air couriers (DHL, FedEx, UPS) deliver directly to your facility in Strasbourg, Colmar, or Mulhouse within 3 to 5 transit days.
For scheduled high-volume monthly releases, cost-effective consolidated air freight via Frankfurt Airport (FRA) or Paris-Charles de Gaulle (CDG), as well as maritime container shipping to Antwerp or Le Havre, is coordinated with full customs clearance and documentation.
What documentation and Quality Control reports are supplied with production shipments?
Every production lot includes a Certificate of Conformance (CoC), 100% electrical continuity and insulation resistance test logs, optical color matching records (Pantone ΔE values), and First Article Inspection (FAI) dimensional reports.
Upon request by your quality assurance team, we can provide PPAP Level 3 documentation, IMDS submissions, raw material lot certificates, and environmental test data sheets covering high/low temperature cycle testing and pull-force measurement.
Accelerate Your Next Appliance Interface Development
Partner with an Intertek-verified direct manufacturer. Send your CAD drawings, graphic artwork, or legacy sample specifications to receive a comprehensive engineering DFM analysis and quotation within 24 hours.