Silicone Elastomer
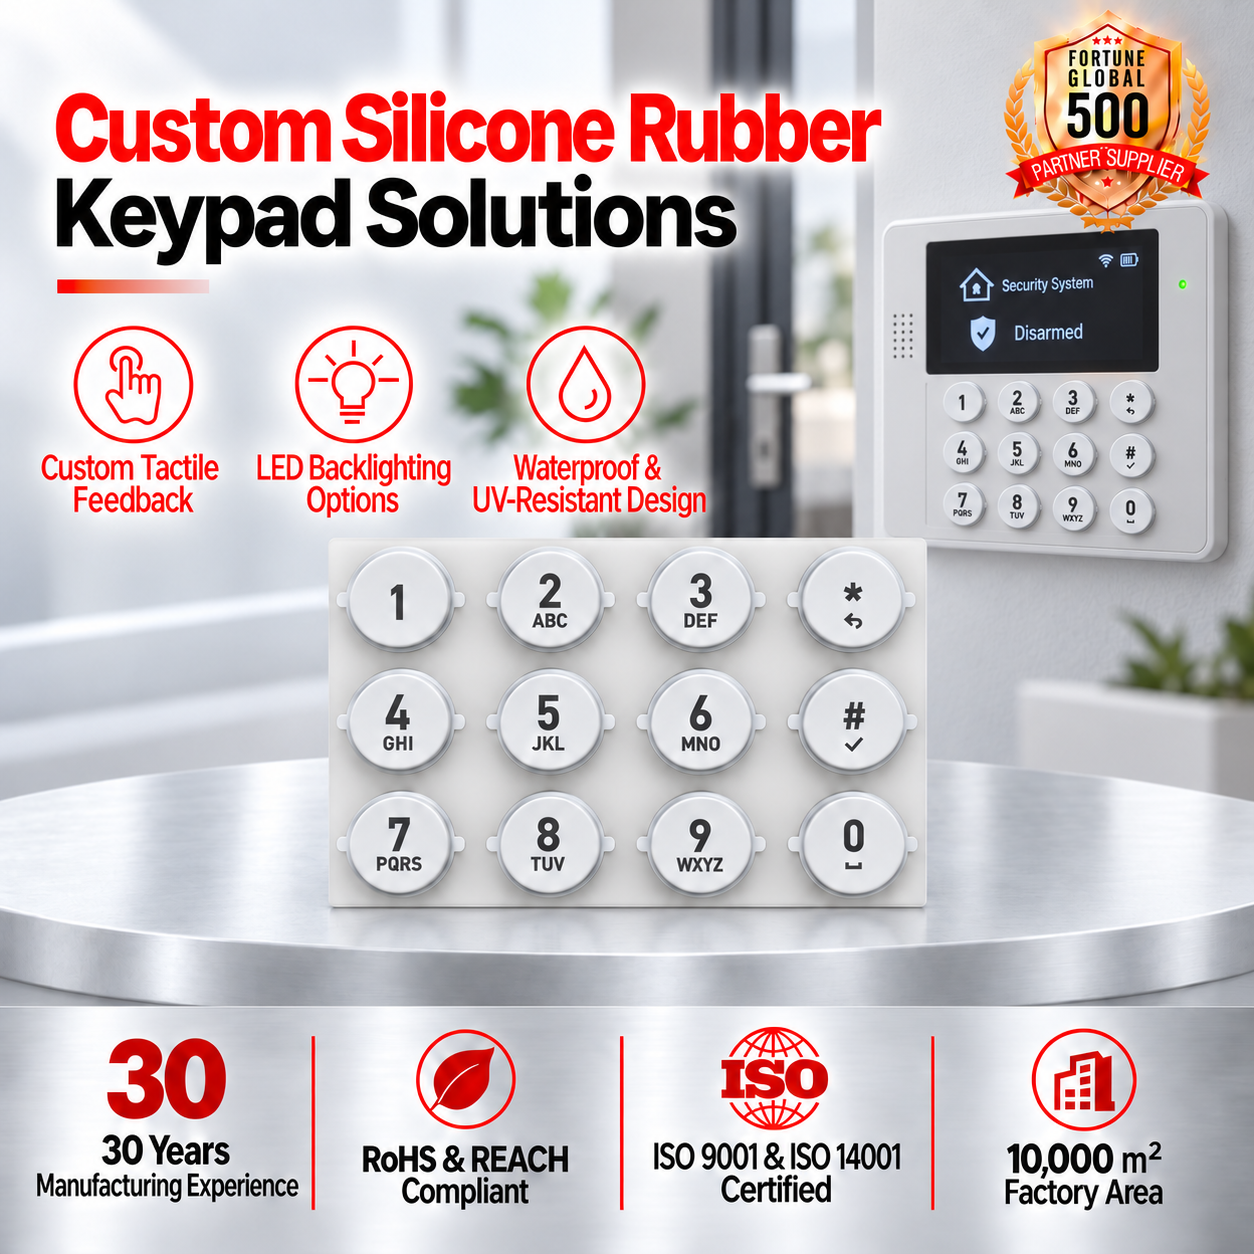
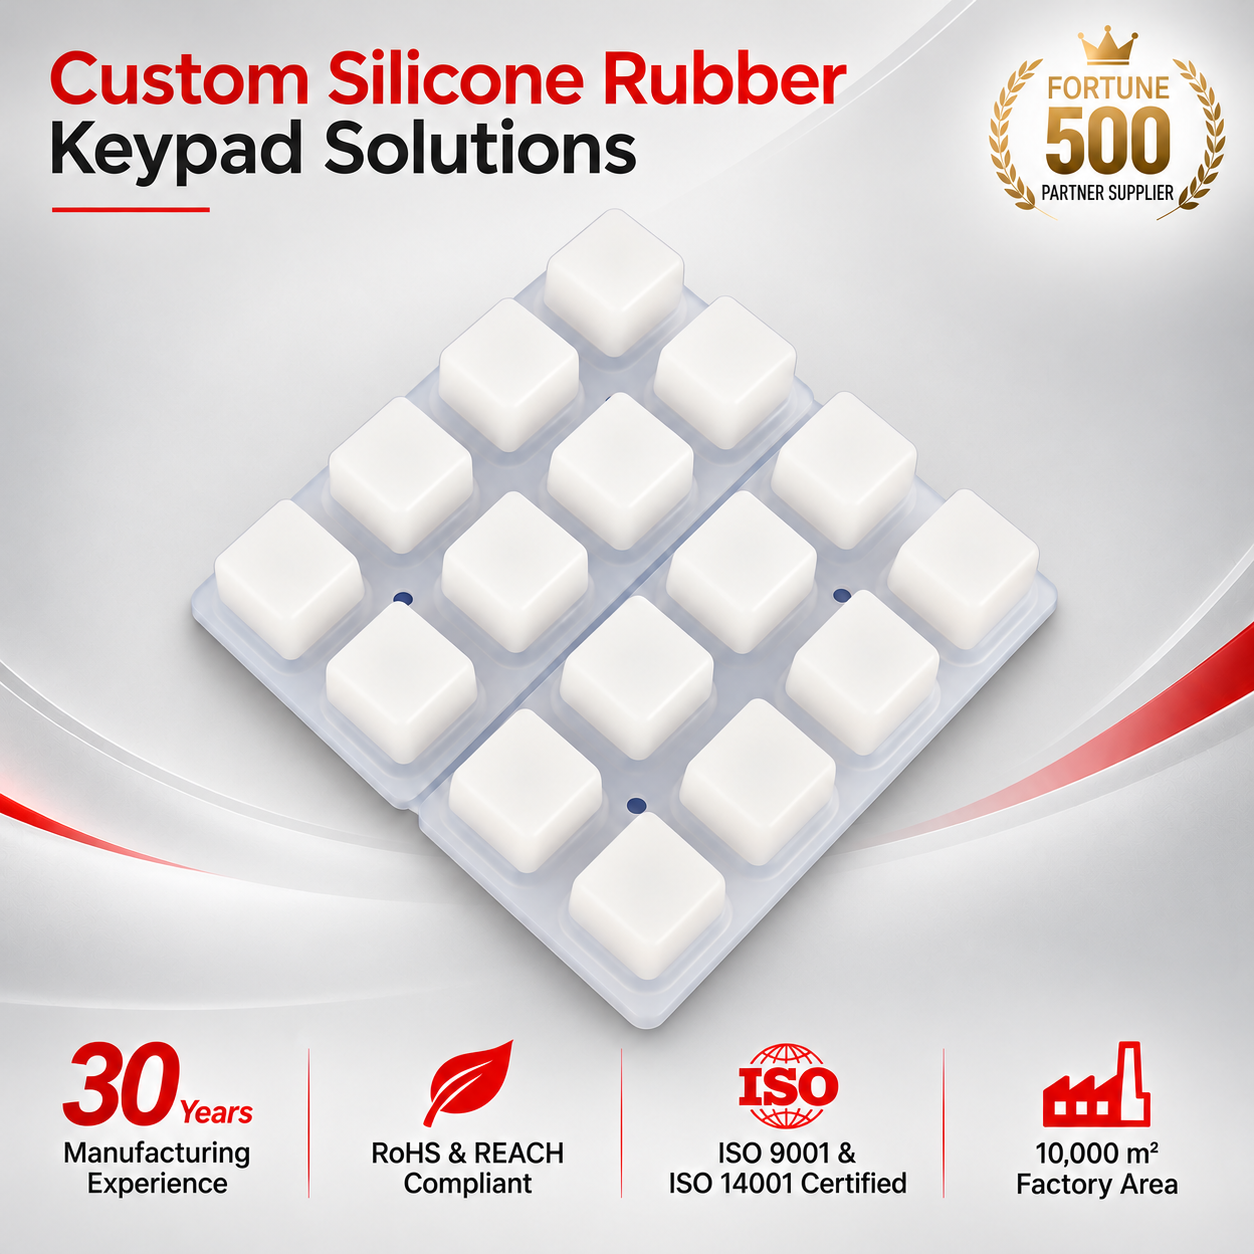
Explore our precision-fabricated industrial control keypad switches, combining durable elastomer polymers, copper FPC circuits, tactile stainless steel domes, and chemical-resistant sub-surface overlays built to survive Christchurch’s aggressive commercial cycles.
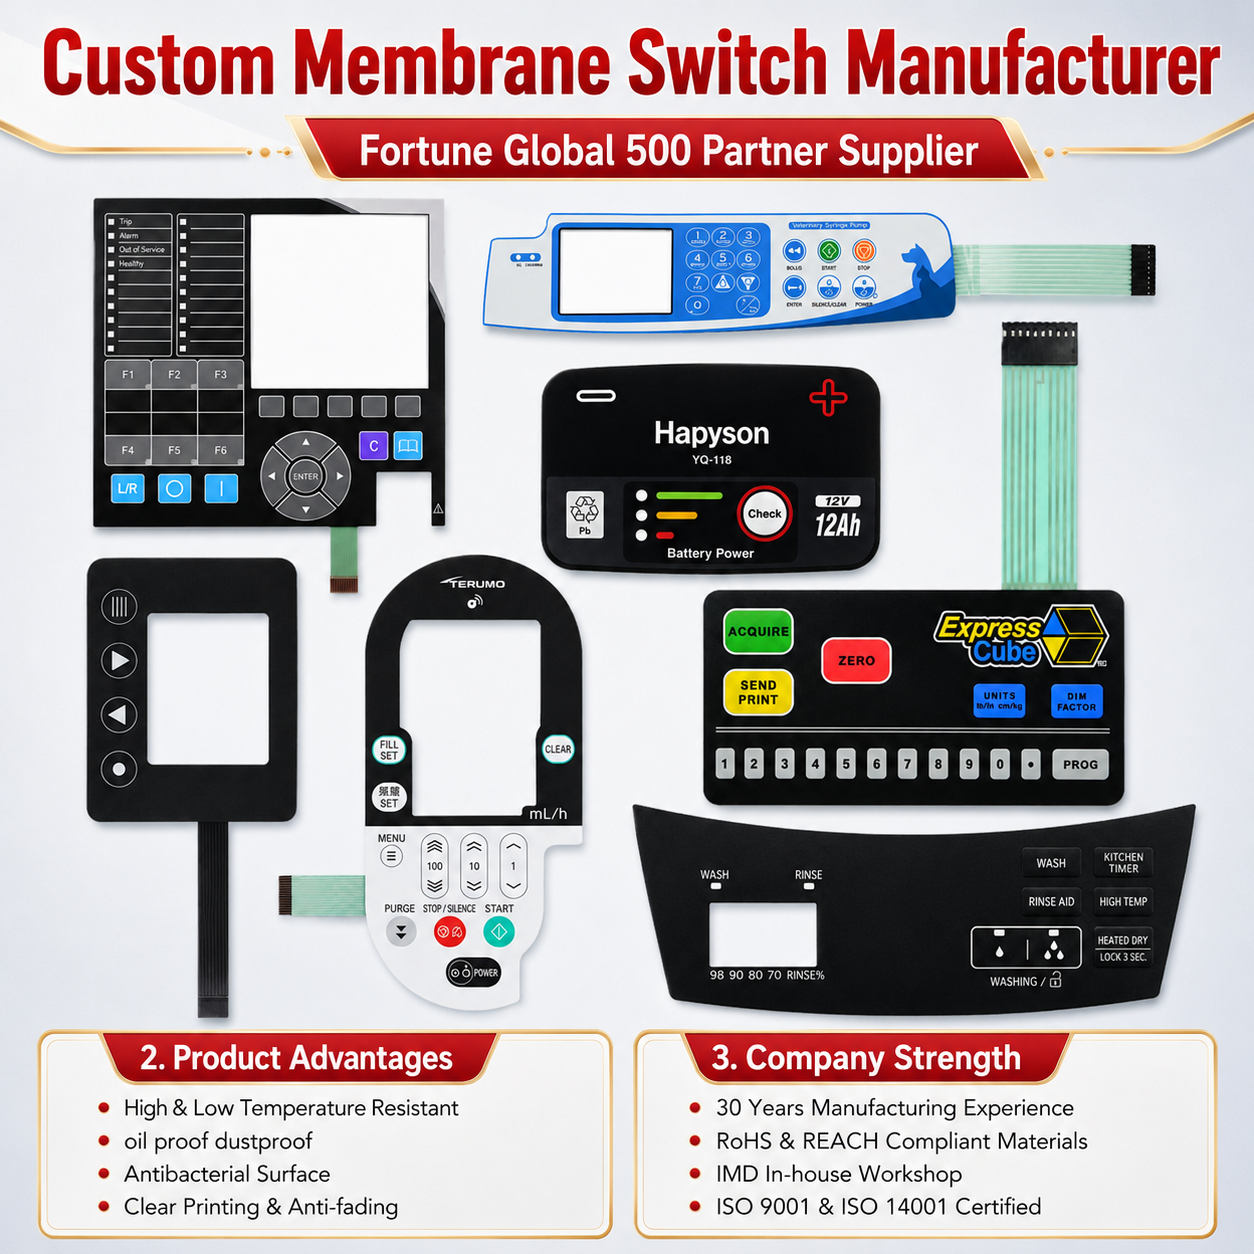
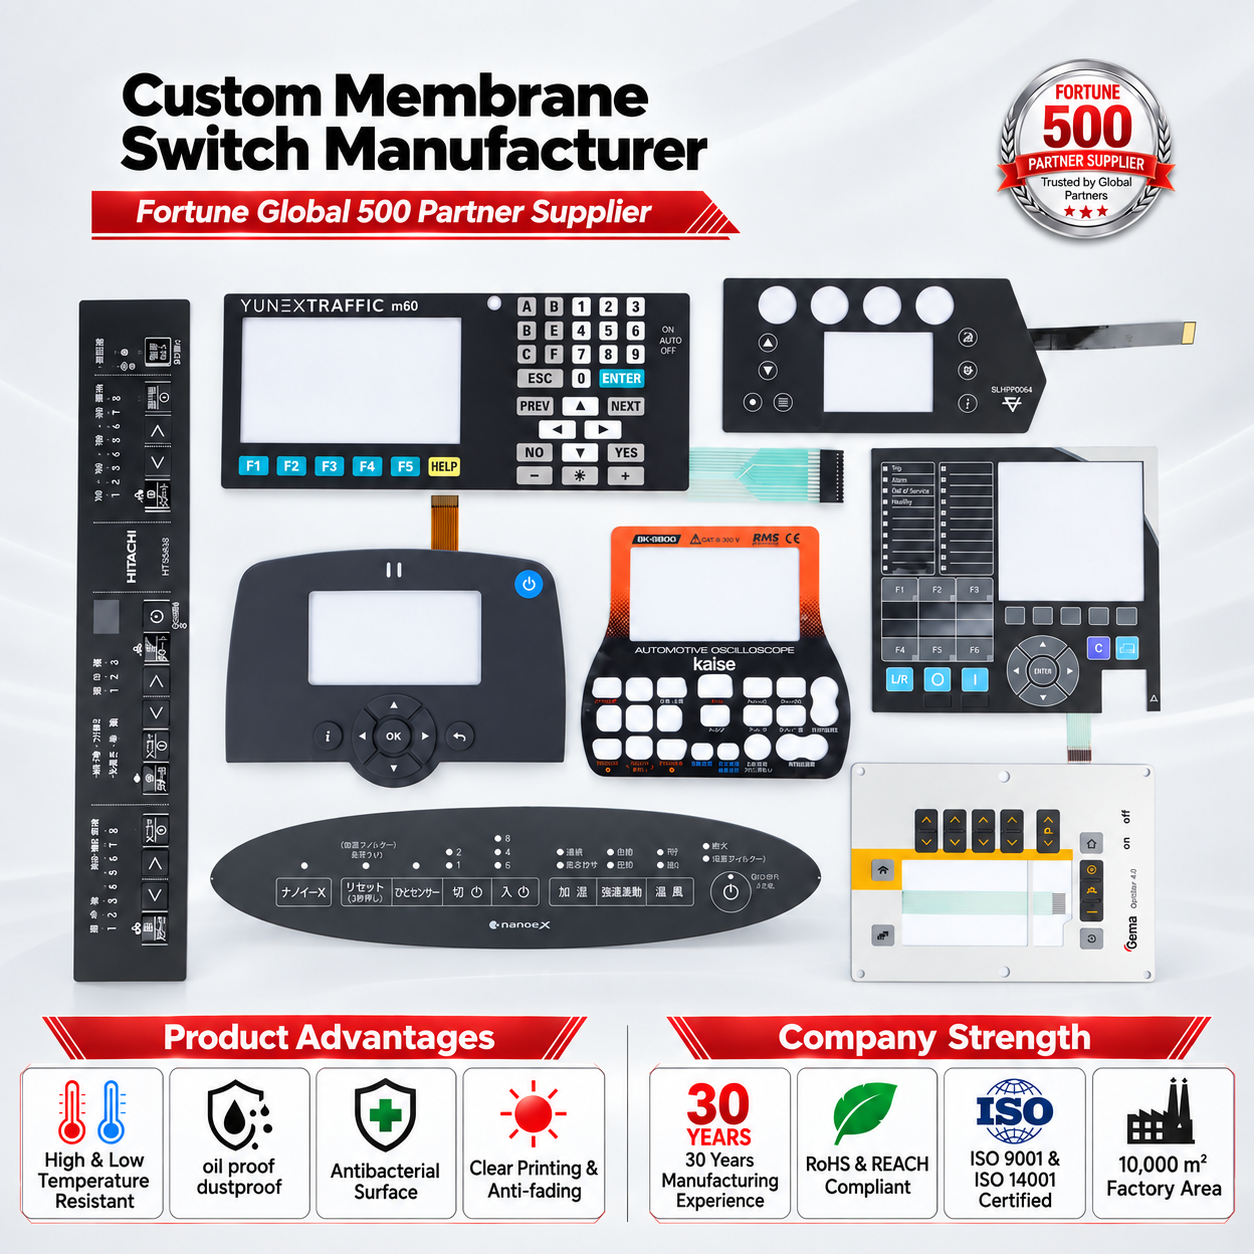
Christchurch stands as the vibrant technical hub of New Zealand’s South Island, balancing rapid precision engineering expansions in Hornby, Middleton, and Bromley with deep roots in high-efficiency agribusiness, logistics through the Port of Lyttelton, and high-altitude or Antarctic exploration hardware. Industrial Human-Machine Interfaces (HMIs) installed in Canterbury encounter severe real-world challenges: massive diurnal temperature swings across the Canterbury Plains, exposure to acidic dairy washdown sanitation chemicals, coastal marine salt atmospheres, and abrasive agricultural airborne debris. Below is how our Chinese manufacturing direct pipeline delivers tailor-engineered solutions for Christchurch OEM systems integrators.
Canterbury’s extensive dairy processing operations require HMIs capable of surviving aggressive Clean-in-Place (CIP) regimes involving boiling water, sodium hydroxide (caustic soda), and nitric acid sanitizers. Standard commercial touchscreens quickly suffer delamination or phantom actuation under direct jet streams. Our industrial control switch panels feature seamless IP67/IP69K perimeter gaskets, Autotex XE chemical-resistant polyester overlays, and zero-crevice silicone keycaps that isolate circuitry from caustic corrosion, guaranteeing uncompromised hygiene and long-term functional stability.
Across the Canterbury Plains, automated pivot irrigation, soil moisture telemetry units, and agricultural robotic harvesters operate outdoors year-round. These outdoor controllers encounter severe UV solar irradiance, winter freezes down to -10°C, and heavy dust during harvest seasons. We manufacture graphic overlays with UV-stabilized polycarbonate and PET substrates tested under accelerated xenon-arc conditions, combined with stainless steel metal domes delivering positive tactile feedback even when farm technicians operate machinery wearing heavy protective gloves.
Handling bulk coal, grain, forestry products, and ocean containers at Lyttelton Harbour demands industrial keypads proofed against relentless marine salt-fog corrosion, high mechanical vibration, and physical abrasion. We integrate pure copper flexible printed circuits (FPC) with polyimide reinforcement, nickel-gold surface finishes, and stainless steel front bezels that prevent electrochemical oxidation, ensuring zero trace degradation and high dielectric breakdown thresholds across maritime terminal cranes and marine auxiliary switchboards.
As a premier global center for earthquake research and geotechnical engineering, Christchurch-based instrument builders design critical field recorders, seismic alert stations, and structural health telemetry consoles. Our keypads incorporate embedded ESD shielding layers (conductive silver or aluminum foil grids) capable of dissipating up to 15kV static discharges, preventing circuit resets or false triggering during seismic shock vibrations and harsh subterranean deployments throughout the Alpine Fault regions.
Choosing the proper industrial keypad switch configuration is a critical engineering decision balancing thermal tolerance, cycle durability, chemical exposure, and electrical latency.
| Architecture Type | Circuit Matrix | Actuation Life | Ingress Rating | Operating Temp Range | Best Fit Canterbury Application |
|---|---|---|---|---|---|
| Metal Dome Tactile Membrane | Screen-Printed Silver on PET | 1,000,000 - 3,000,000 cycles | IP65 to IP67 | -20°C to +70°C | Medical diagnostics, laboratory analyzers, packaging plant PLCs |
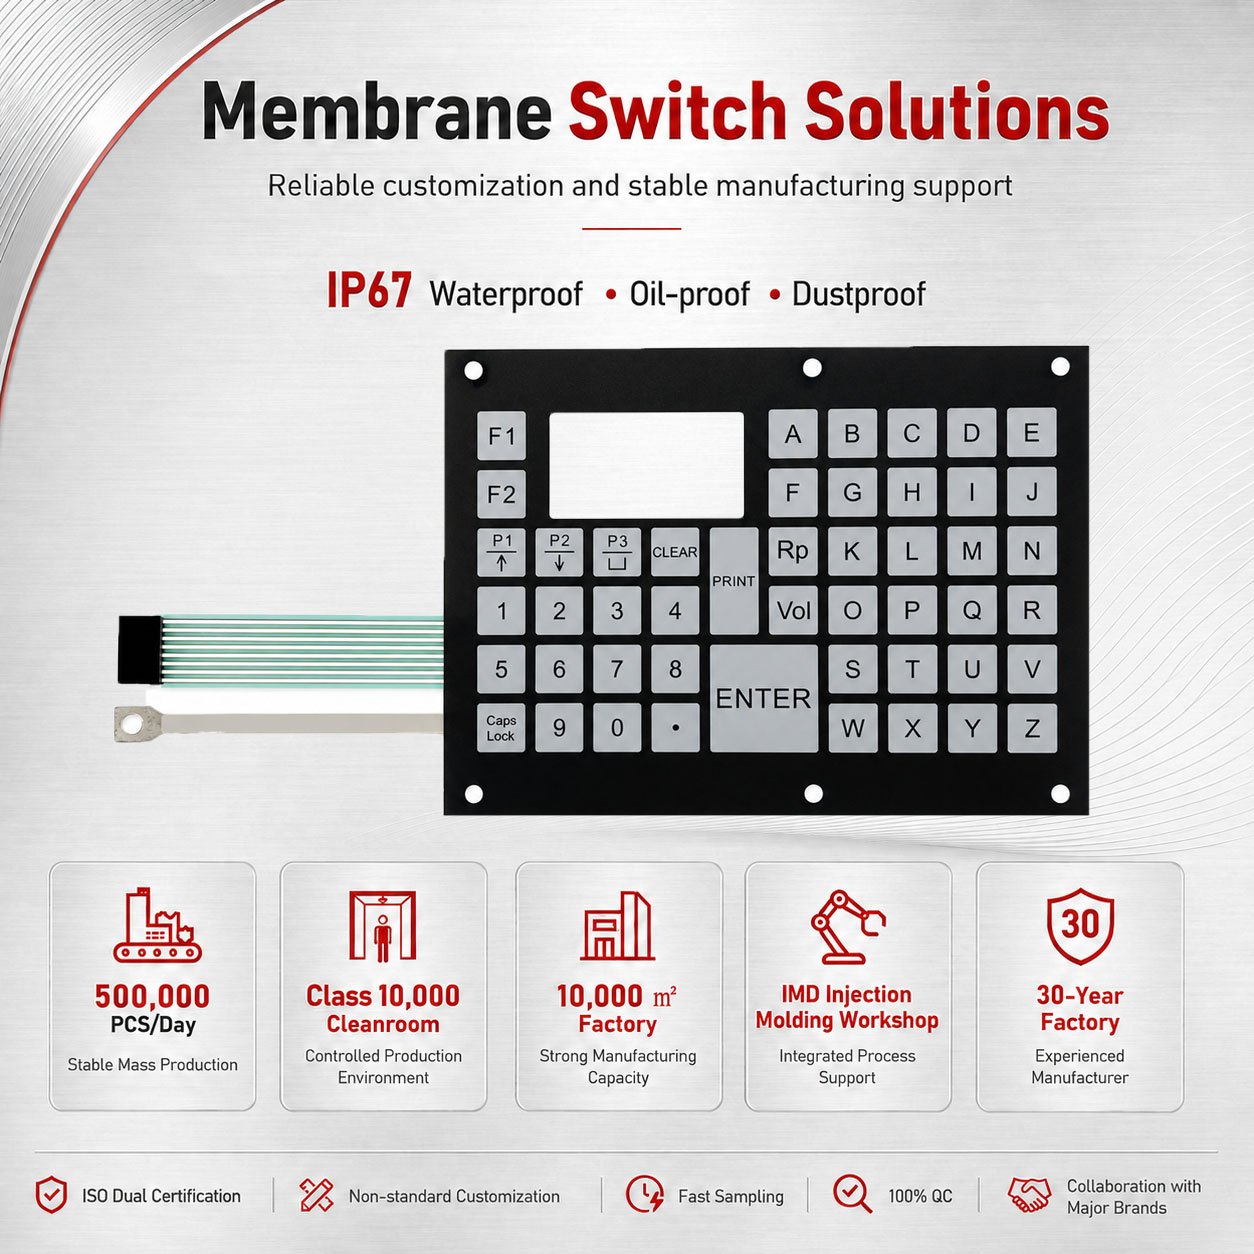
| Copper FPC Membrane Switch | Etched Polyimide Copper Layer | > 5,000,000 cycles | IP67 to IP68 | -40°C to +85°C | High-vibration mobile farming machines, Lyttelton terminal cranes |
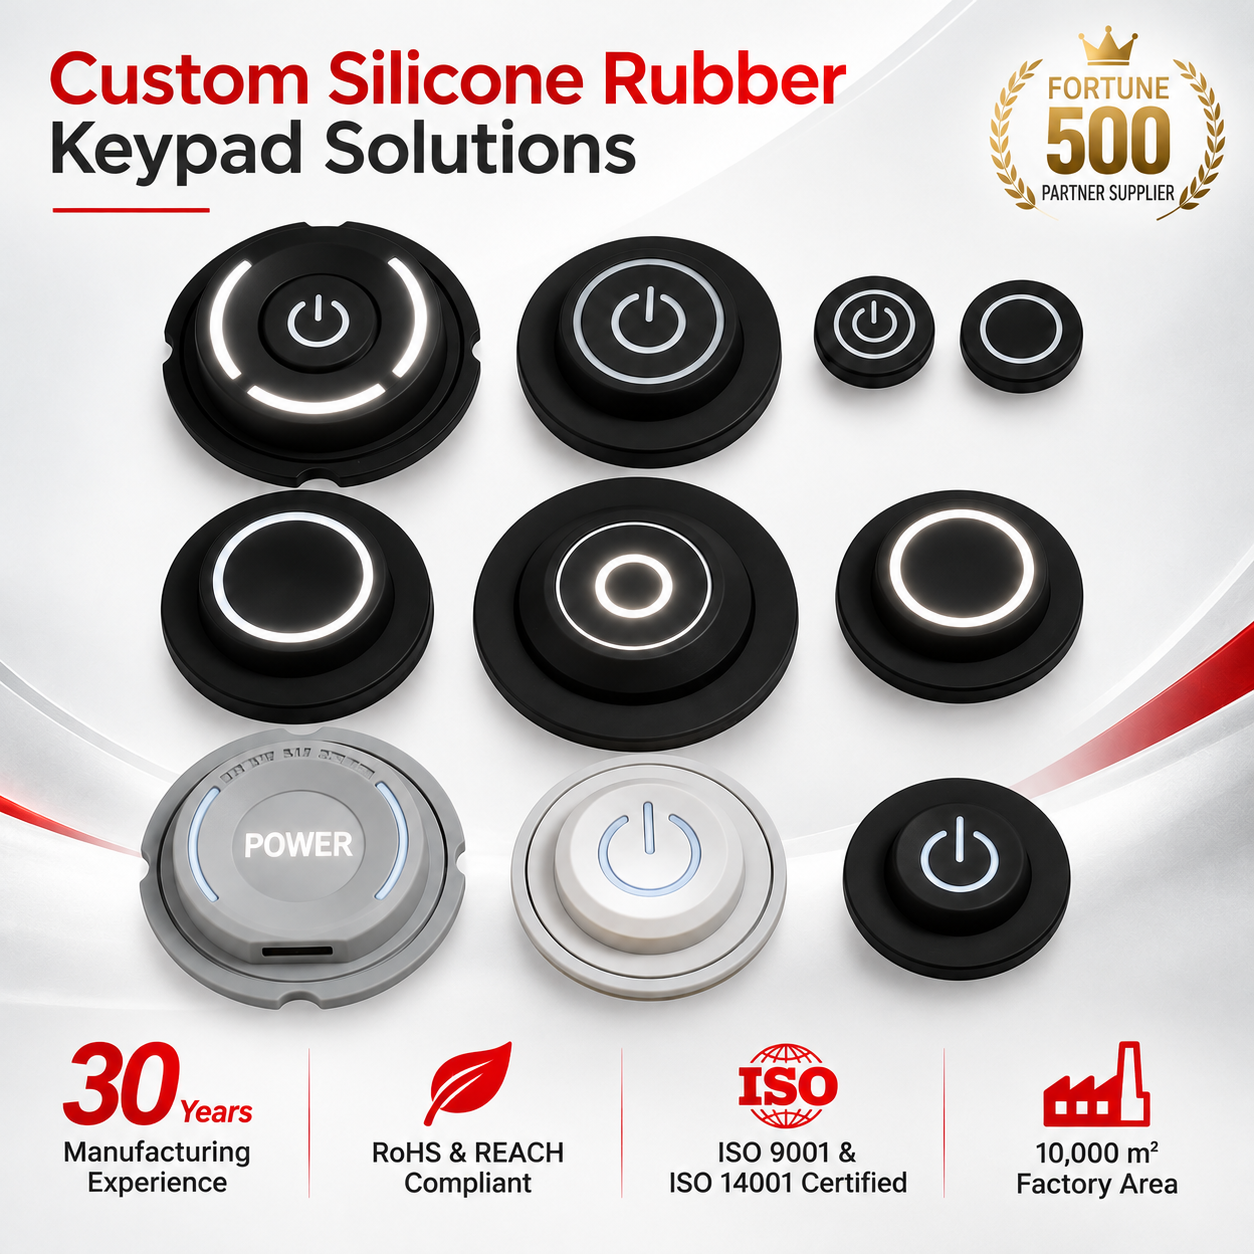
| Silicone Rubber Keypad (P+R) | Carbon Pill / Gold Plated Dome | 2,000,000 - 5,000,000 cycles | IP66 to IP68 | -40°C to +150°C | Outdoor hand-held scanners, fuel dispensing systems, cold stores |
| Capacitive Solid-State HMI | ITO / Copper Sensor Mesh | Virtually Infinite (No Wear) | IP69K Completely Sealed | -30°C to +85°C | Food processing cleanrooms, dairy CIP washdown environments |
| Vandal-Proof Stainless Steel | Rugged Microswitch / Metal Matrix | > 5,000,000 cycles | IK10 / IP67 | -30°C to +75°C | Public fuel terminals, municipal parking kiosks, mining transport |
The industrial sector across Christchurch and the wider Canterbury region is transitioning through a major wave of modernization. Rising labour costs, strict workplace health and safety compliance, and rapid adoption of Industry 4.0 IoT telemetry platforms are reshaping how local engineering directors and sourcing professionals evaluate switchgear and input peripherals.
Traditional control cabinets equipped with bulky 22mm pilot switches and mechanical push-buttons are being superseded across Christchurch workshops. OEMs are standardizing on slim-profile, customized membrane and silicone switch clusters. This shift slashes panel-wiring assembly hours by up to 70%, lowers cabinet depth requirements, and eliminates internal air volume where condensation routinely damaged older electromechanical assemblies during Christchurch winter temperature drops.
With Christchurch holding high concentration of dairy, meat processing, and biotechnology exports, regulatory demands surrounding hygiene have never been higher. Sourcing teams reject conventional perimeter adhesives that leave microscopic crevices for bacterial colonization. Our Dongguan facility implements custom CNC-cut 3M 300LSE adhesive gaskets and antimicrobial hard-coated films certified to inhibit microbial growth even under repeated hot chemical washes.
From round-the-clock dairy processing factories in Darfield to 24/7 harbor operations at Lyttelton, operators regularly handle input panels in extreme low-light environments. Modern Canterbury procurement specifications demand ultra-uniform Light Guide Film (LGF) backlighting. Unlike old electroluminescent (EL) backlights that fade rapidly, our solid-state SMD LED coupled LGF systems deliver 50,000+ hours of glare-free, uniform light across custom key icons with minimal current draw.
Christchurch engineering teams previously relied on intermediary domestic brokers who marked up component prices by 200% to 300% and added weeks of communication delays. By partnering directly with AXRU Electronics in Dongguan, local R&D teams receive direct DFM engineering reviews within 24 hours, rapid prototype iterations in 7 to 10 working days, and expedited air delivery straight to Christchurch International Airport (CHC) via DHL/FedEx Express.
Headquartered in the global electronics manufacturing heartland of Dongguan, Dongguan AXRU Electronics Co., Ltd. operates a vertically integrated 10,000㎡ production facility verified on-site by Intertek. We eliminate the vulnerabilities of outsourced production by maintaining 100% of printing, circuit fabrication, dome placement, stamping, and reliability testing in-house.
Our complete 10,000㎡ infrastructure, ISO9001 certified quality management protocols, and 121 full-time technical specialists have been thoroughly audited and certified on-site by Intertek. Canterbury procurement officers can review transparent production audit documents and quality records without travel friction.
Before shipping to New Zealand, production samples undergo thorough validation on our automated force-displacement curve testers, key life cycle testers (up to 5 million strikes), programmable temperature and humidity environmental chambers (-50°C to +150°C), ink abrasion testers, and UV yellowing chambers.
Every single industrial keypad switch manufactured undergoes automated 100% electrical continuity, loop resistance, insulation resistance (>100MΩ at 250V DC), and LED forward-voltage drop verification. You receive zero defective units upon opening your crates in Christchurch.
We recognize that New Zealand’s high-precision industrial market thrives on agile specialized production runs rather than millions of consumer units. We support Christchurch clients with initial production runs starting as low as 100 pieces, backed by full Design For Manufacturability (DFM) reviews within 24 hours.
Essential technical, logistics, and compliance answers for Canterbury procurement teams, design engineers, and systems integrators sourcing from China.
For time-critical engineering samples or urgent production batches, we ship via DHL Express, FedEx Priority, or air cargo directly into Christchurch International Airport (CHC), requiring just 4 to 6 business days from our dispatch dock to your Christchurch premises. For bulk consolidated ocean freight orders, goods ship out from Shenzhen or Guangzhou ports directly to the Port of Lyttelton, typically averaging 18 to 24 transit days.
Yes. All raw materials—from genuine Autotex polyester films, GE Sabic polycarbonates, Dow Corning silicone elastomers, to 3M acrylic adhesive matrices—are 100% compliant with RoHS 3 (EU 2015/863) and REACH regulations, matching the stringent workplace environmental safety mandates enforceable across New Zealand and Australia (AS/NZS compliance).
Absolutely. Canterbury experiences some of the highest solar UV levels in the Southern Hemisphere during summer, alongside sub-zero winter temperatures. We utilize Autotex XE (Extreme Environment) polyester films with specialized UV-inhibiting coatings that prevent surface yellowing, embrittlement, or graphic chalking for over 7 to 10 years of outdoor operation, tested under ISO 4892-2 conditions.
To deliver an accurate DFM analysis and firm pricing within 24 hours, our engineering team requires: (1) Vector artwork in Adobe Illustrator (.AI), PDF, or DXF showing dimensions and graphics; (2) Mechanical layer stack-up specifying substrate preferences; (3) Schematic or pinout matrix for tail connector pitch (e.g., 2.54mm or 1.0mm); (4) Required actuation force (e.g., 250g or 350g) and tactile response preferences.
Yes. We utilize precision spectrophotometers and automated ink dispensing units to match international Pantone Matching System (PMS) and RAL color standards. All graphics are screen-printed on the reverse (sub-surface) side of transparent PET or PC films, ensuring solvents, wash chemicals, grease, and operator thumb friction never wear away the legibility of legends.
Unlike mechanical switchgear with loose springs, solder contacts, and moving rocker arms that rattle or disconnect under vibration, our membrane and silicone switches feature zero internal momentum. Contact domes are securely sandwiched under multi-layer laminated 3M adhesive bonds, passing rigorous MIL-STD-202G vibration and shock tests without momentary circuit interruption or contact bounce.