Silicone / PTT
Industrial-grade illuminated human-machine interfaces, Light Guide Film (LGF) arrays, capacitive front panels, and rugged environmental sealing engineered for Herzegovina's manufacturing corridor.
Engineered for extreme operating environments, long actuation duty cycles, and clear tactile-optical feedback. Fully customizable layer stack-ups built to OEM industrial standards.
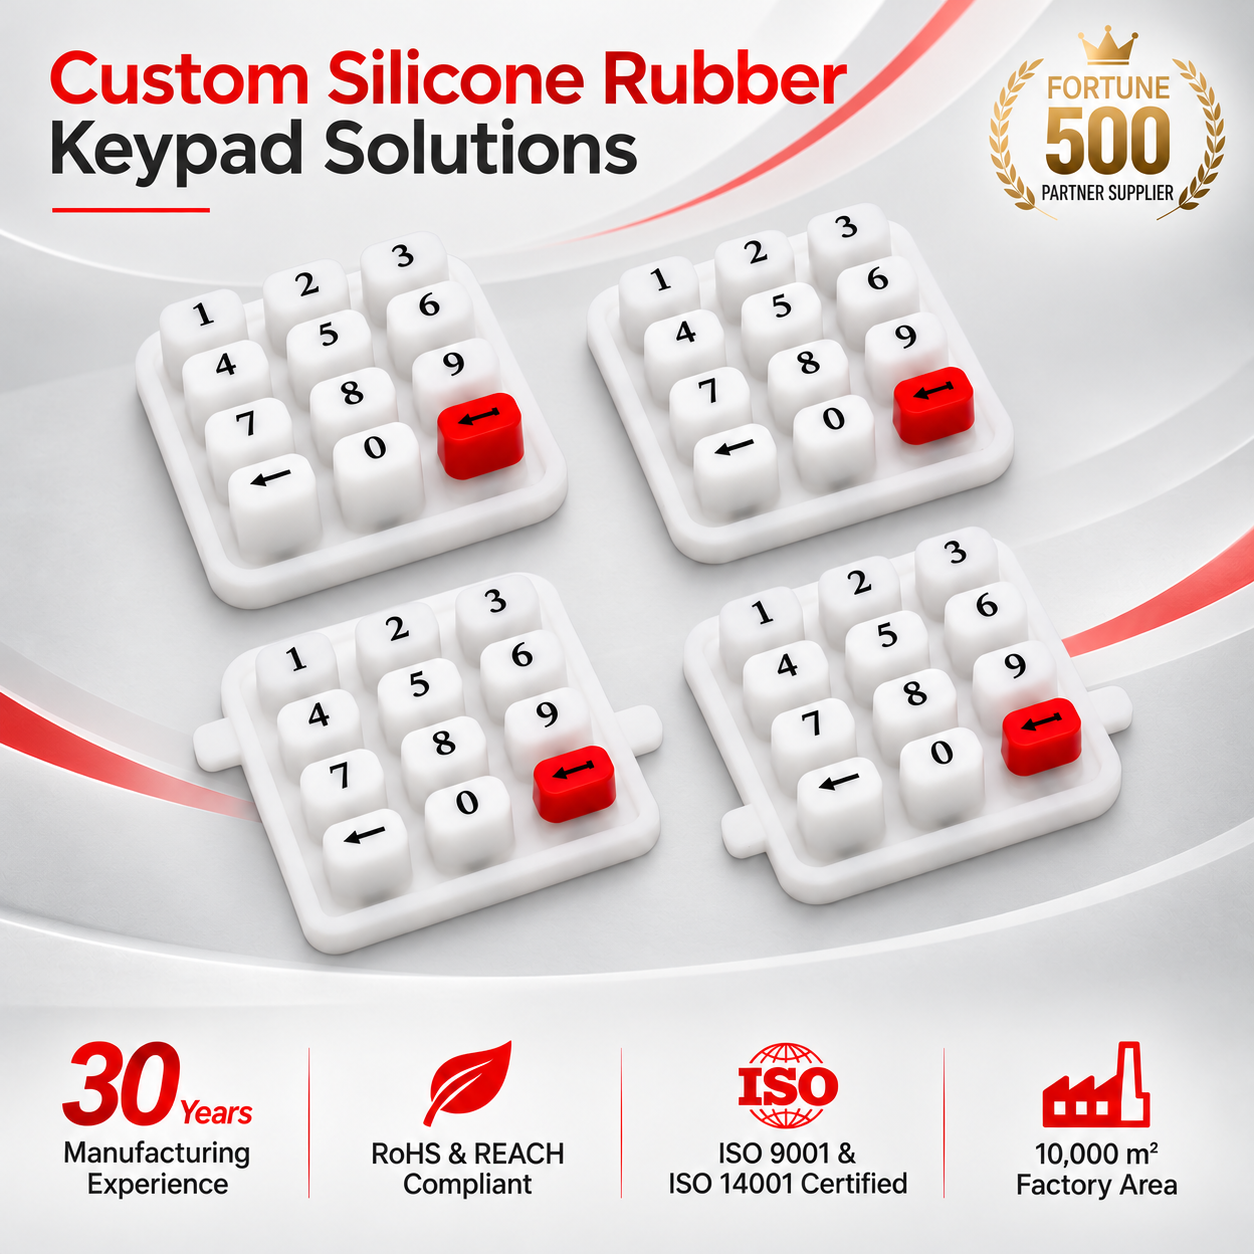
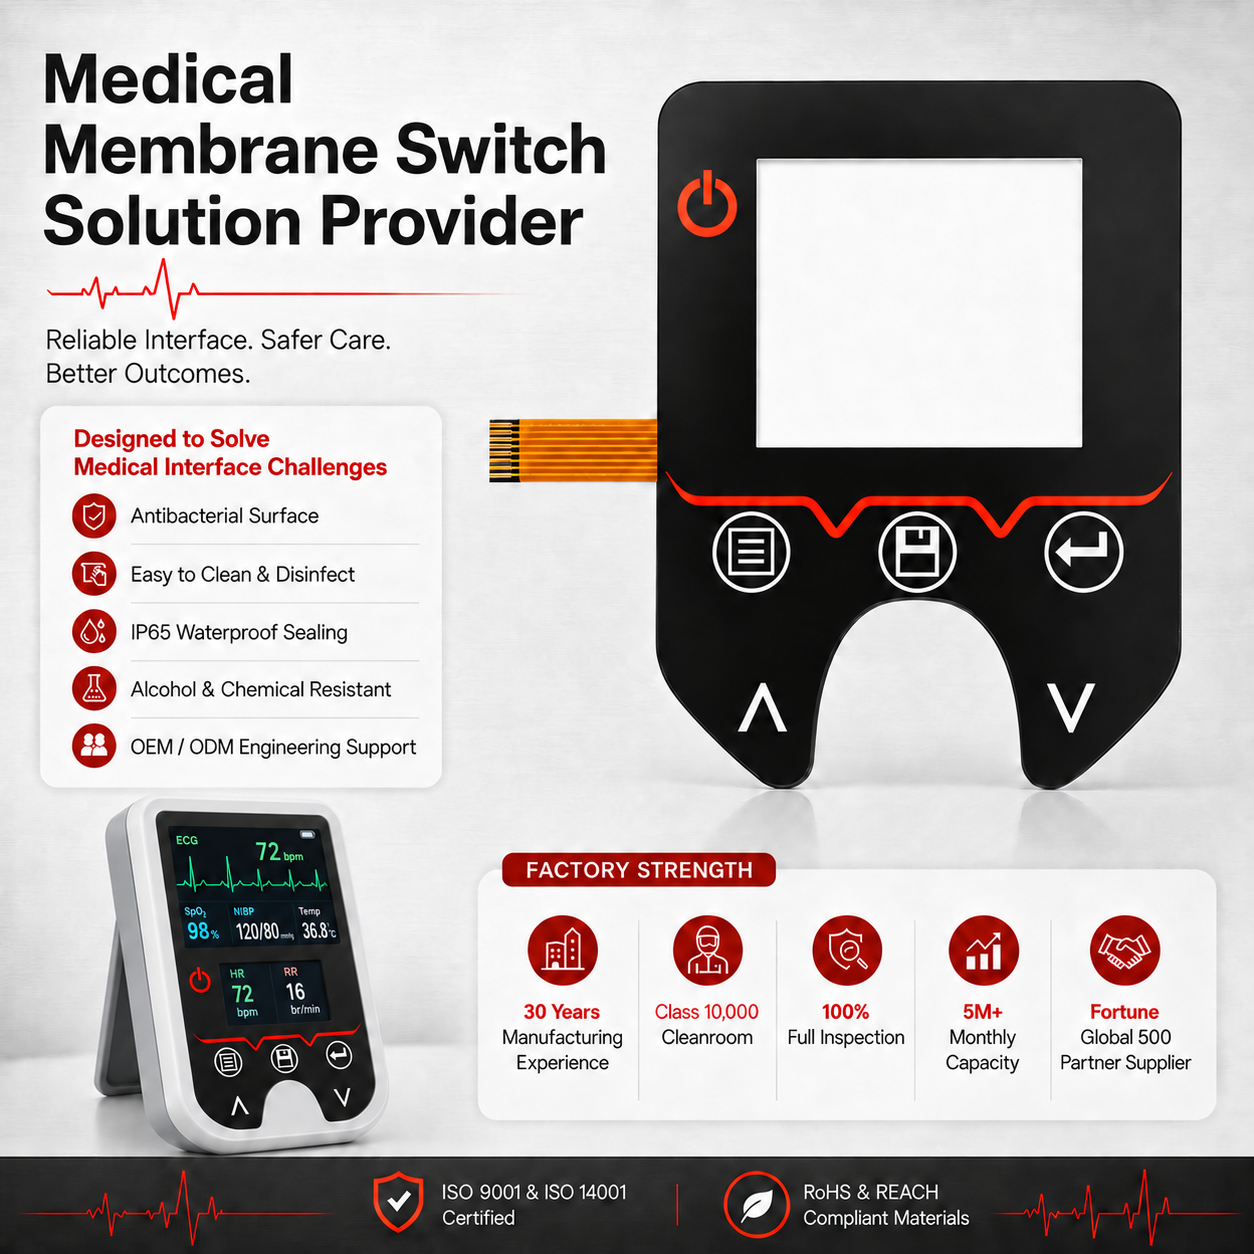
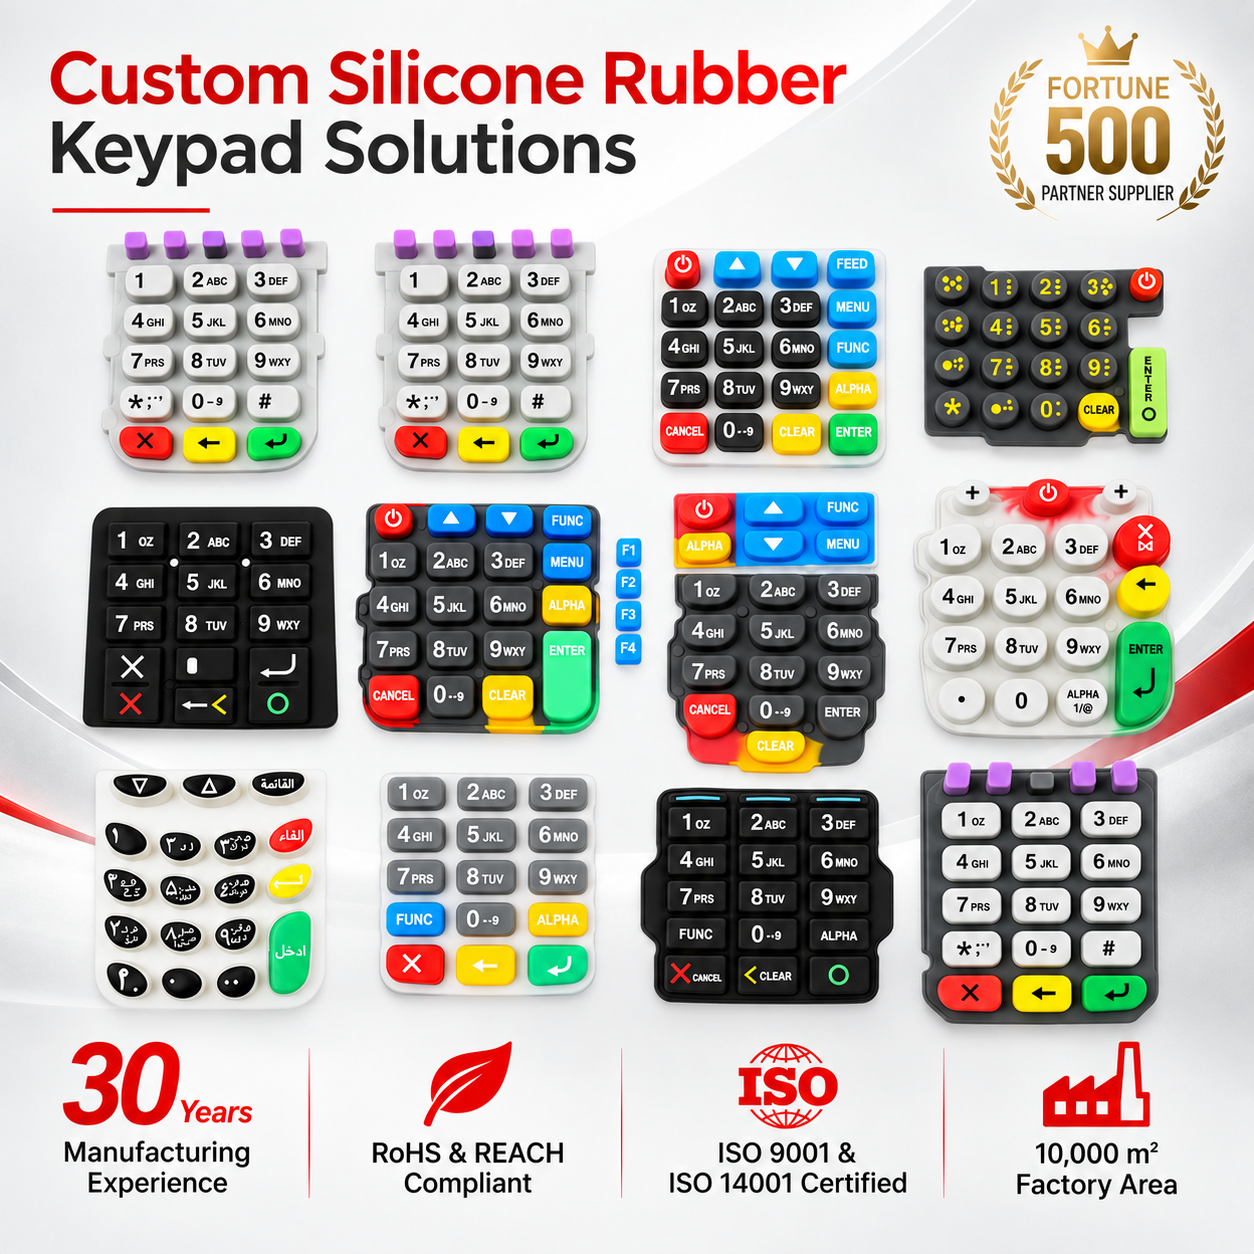
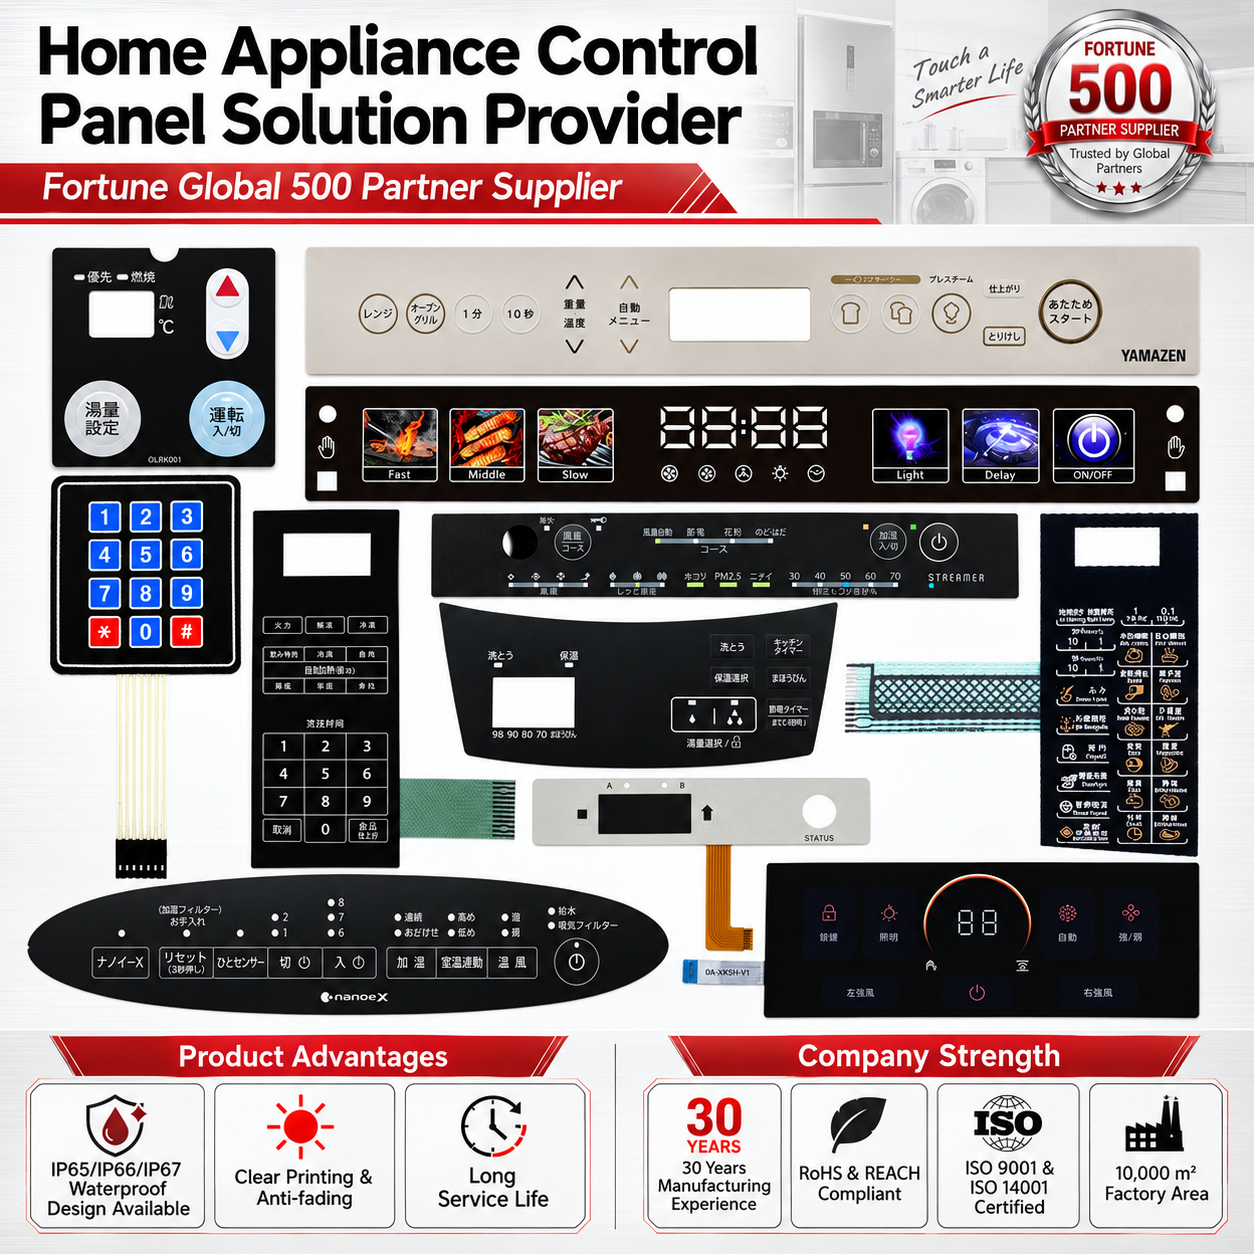
Bridging modern illuminated human-machine interface (HMI) engineering with the specific mechanical, thermal, and electrical requirements of Mostar’s growing manufacturing sector.
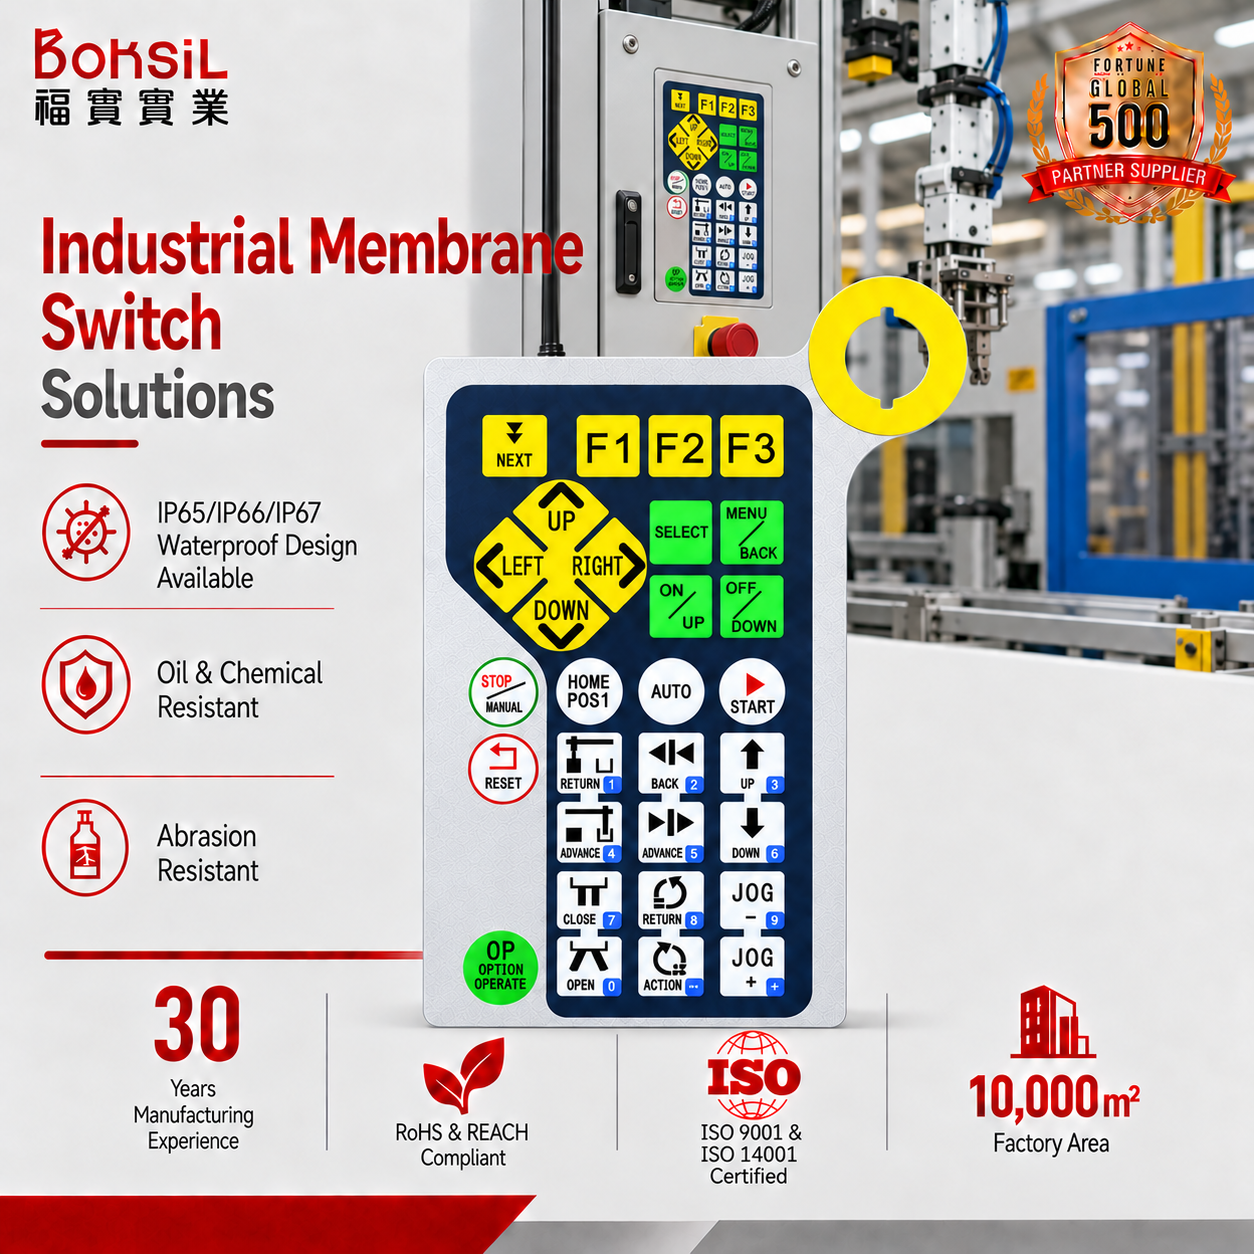
Mostar is historically known for heavy primary aluminum smelting, secondary extrusion processing, and precision aeronautical machining sub-clusters. In these workshops, backlit membrane switches face fine airborne metal particulates, lubricating oil mist, and hydraulic splashing. Our construction utilizes Autotex textured polyester overlays backed with full perimeter IP67 barrier adhesive channels and copper-based FPC (Flexible Printed Circuit) tracks that resist electromagnetic interference (EMI) originating from high-tonnage smelting furnaces and multi-axis CNC spindle drives.
The Neretva river cascading system demands rigorous 24/7 reliability for substation switchgears, turbine flow regulators, and dam monitor consoles. Backlit membrane panels operating in deep generator vaults require Light Guide Film (LGF) or fiber-optic side-lit systems to ensure zero hot-spotting under variable ambient lighting. With dead-front display windows and snap-action stainless steel domes providing an actuation force of 280g–400g, operators wearing heavy dielectric safety gloves receive sharp, positive tactile feedback without false-trigger risks.
Herzegovina's expanding viticulture and agro-industrial plants rely on automated bottling, labeling, and climate-controlled cold storage. These interfaces are exposed to acidic washdown detergents, fluctuating condensate, and thermal shocks from steam cleaning. We engineer our graphic layers with reverse screen-printed sub-surface inks and anti-fogging polycarbonate or chemically treated PET. Sealed tail connectors prevent capillary moisture migration into underlying motherboards, guaranteeing total ingress protection under high-pressure cleaning routines.
System architects in Bosnia and Herzegovina can optimize cost-to-performance tradeoffs using our comparative stack-up architecture guide.
| Backlighting Technology | Typical Stack Thickness | Uniformity Rating | Power Draw | Actuation Travel & Tactile Feel | Recommended Mostar Use Case |
|---|---|---|---|---|---|
| Light Guide Film (LGF) + Surface Mount LEDs | 0.8 mm – 1.4 mm | Excellent (>90% surface uniformity) | Low (20mA – 60mA depending on key zones) | Crisp tactile click via 0.3mm–0.5mm stainless steel metal domes | Medical diagnostic terminals, CNC console panels, and precision testing instruments. |
| Direct Surface Mount (SMD) Point LEDs | 1.0 mm – 1.8 mm (embossed) | Localized indicator only (non-diffuse) | Minimal (<15mA per node) | Embossed pillow or rim keys with tactile feedback | Hydroelectric gate monitors, substation alarm indicators, and pump automation boxes. |
| Electroluminescent (EL) Lamps | 0.5 mm – 0.8 mm | Superior soft glow (100% flat surface) | High AC excitation (Inverter required, 80-110VAC) | Ultra-thin non-tactile or flat tactile response | Aviation cockpit accessories, night-vision control panels, and darkroom monitoring consoles. |
| Fiber Optic Weave Sub-layer | 0.7 mm – 1.1 mm | Very High, zero thermal dissipation | Low-to-Moderate (driven by remote RGB LEDs) | Retains tactile sensitivity of base domes without rubber pill damping | Hazardous explosive environments (ATEX), chemical processing lines, and solvent dispensing kiosks. |
Analyzing structural shifts toward modern user experiences, environmental durability, and rapid prototyping across Southeastern Europe.
Original Equipment Manufacturers in Mostar are moving past plain mechanical pushbuttons. Modern factory floors prefer a combination of seamless capacitive touch surfaces for multi-level parameter adjustment and high-tactile snap-dome switches for mission-critical functions like Machine Start, Fault Reset, and Emergency Braking. This hybrid configuration prevents unintentional electrostatic triggers from coolant spray while maintaining an easy-to-sanitize flat exterior surface.
While screen-printed conductive silver flakes on PET remain economical for consumer devices, Mostar’s heavy-machinery and electrical infrastructure sectors are adopting flexible printed copper circuits (FPC). Etched polyimide copper circuits handle higher current traces, permit tight SMD LED component soldering without conductive-epoxy flaking, and provide low closed-circuit loop resistance (<1.0 Ohm) across long harness tails connected to programmable logic controllers (PLCs).
Mostar experiences over 2,300 hours of direct annual Mediterranean sunshine, generating elevated surface temperatures and UV radiation levels for outdoor utility stations and construction machinery. Local procurement managers require graphic films that resist chalking, yellowing, and thermal embrittlement. Utilizing UV-resistant Autotex XE polyester films coupled with weatherable acrylic adhesives ensures over five years of exterior service life without graphic delamination.
Backed by Intertek on-site facility verification and 12 years of specialized human-machine interface fabrication, our Dongguan plant operates as an extension of your mechanical engineering department.
Our operational systems, documented quality gates, and environmental compliance frameworks meet the demanding audit standards of Tier-1 multinational OEMs and defense-grade contractors.
We eliminate assembly line failures through 100% testing of trace resistance, contact bounce, short circuits, insulating dielectric resistance, and forward LED voltage drops on automatic test fixtures.
Screen printing, digital color matching, laser plotter cutting, metal dome array positioning, cleanroom lamination, and precision die cutting are executed under a single roof without third-party contracting.
We actively support pilot line testing, specialty niche machinery builds, and replacement aftermarket orders starting from just 100 pieces, backed by full PPAP and First Article Inspection (FAI) dossiers.
Clarifying lead times, international freight options, reverse engineering capabilities, and layer adhesion integrity.