Engineered Switch & Sensing Technologies
Custom-fabricated in our 10,000㎡ ISO-audited facility with full mechanical, environmental, and optoelectronic customization for industrial hardware teams in Escaldes-Engordany.
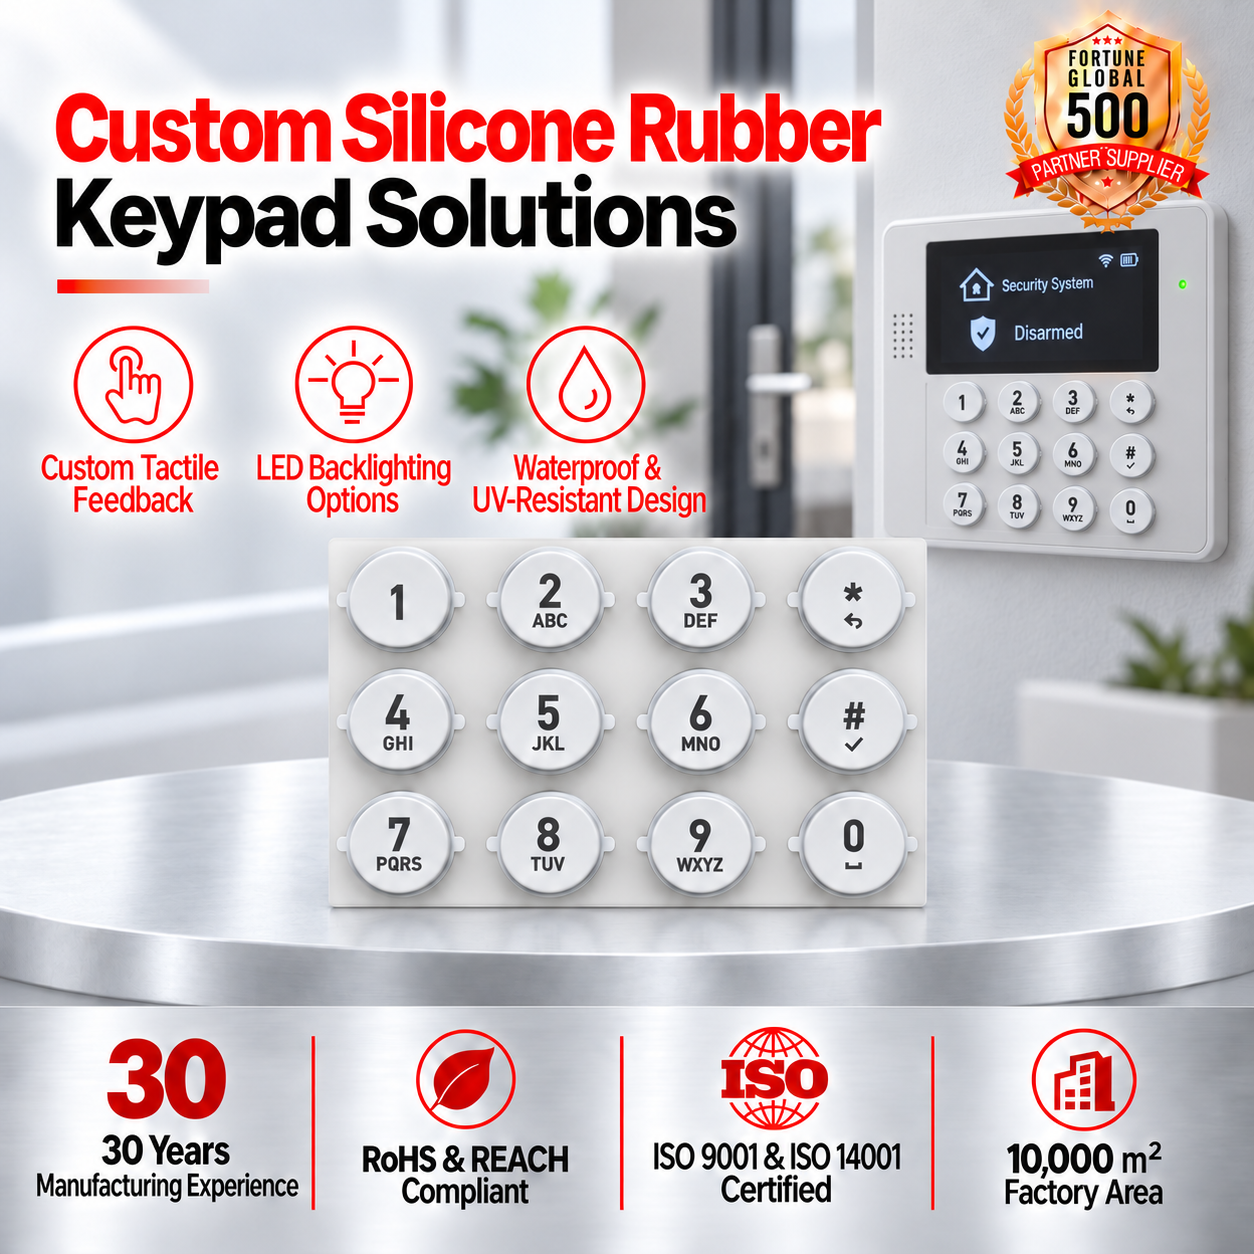
Custom OEM Silicone Rubber Keypad 3x4 Numeric 12 Keys Round Plastic Button P+R
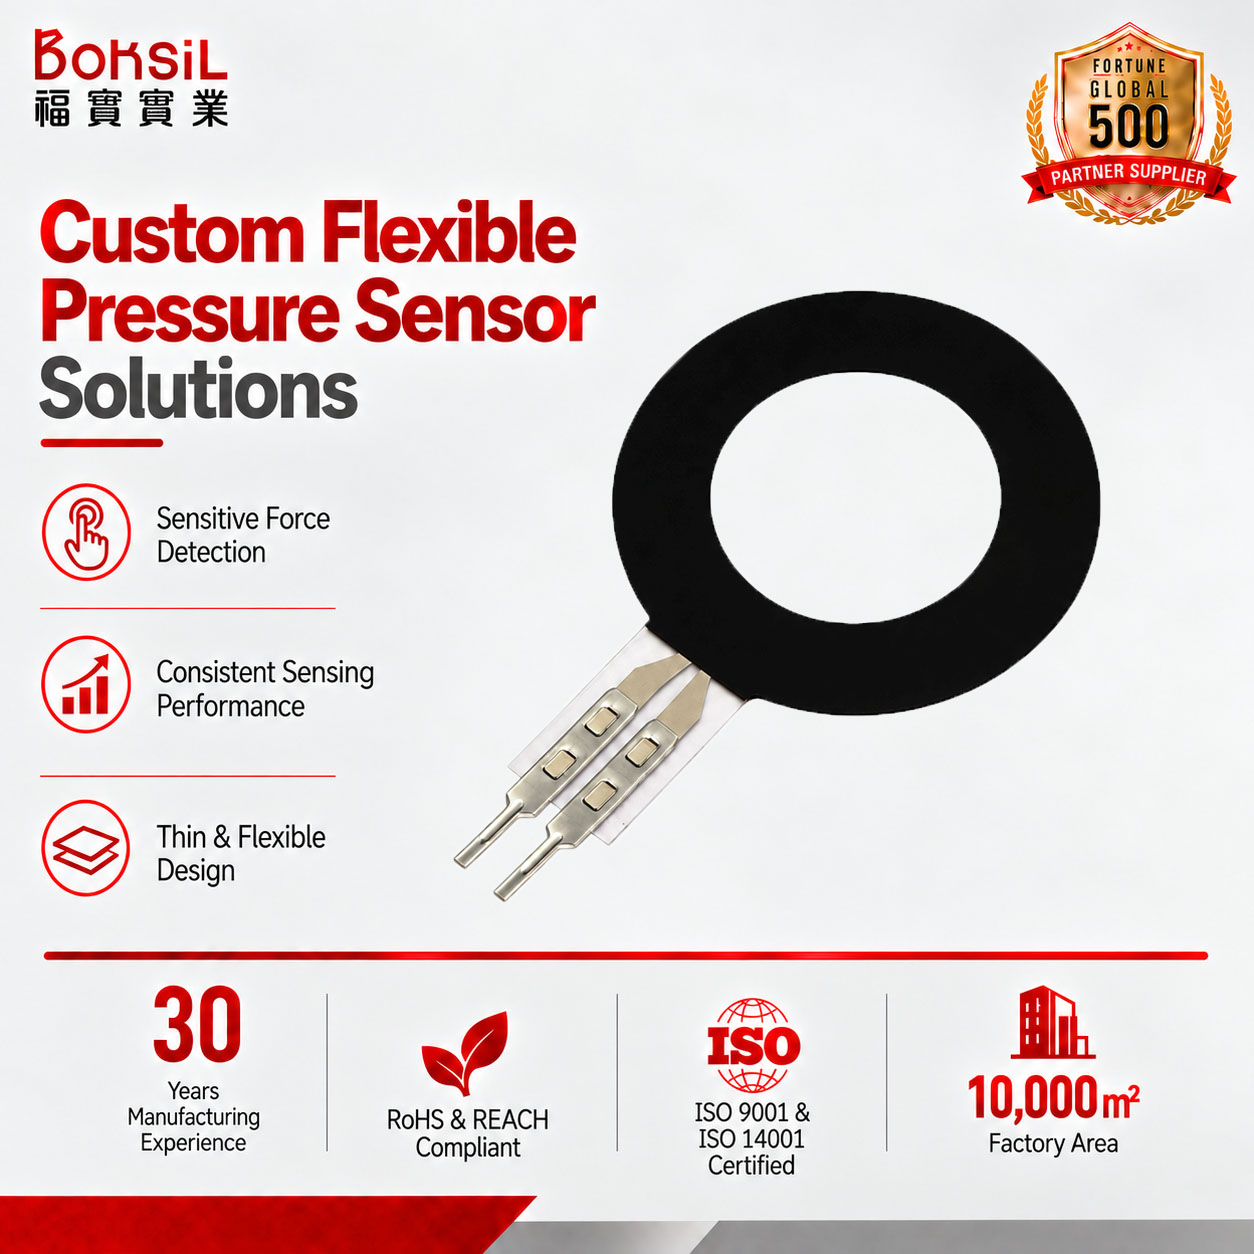
Universal FSR Flexibility Force Sensitive Capacitive Touch Thin Film Resistor
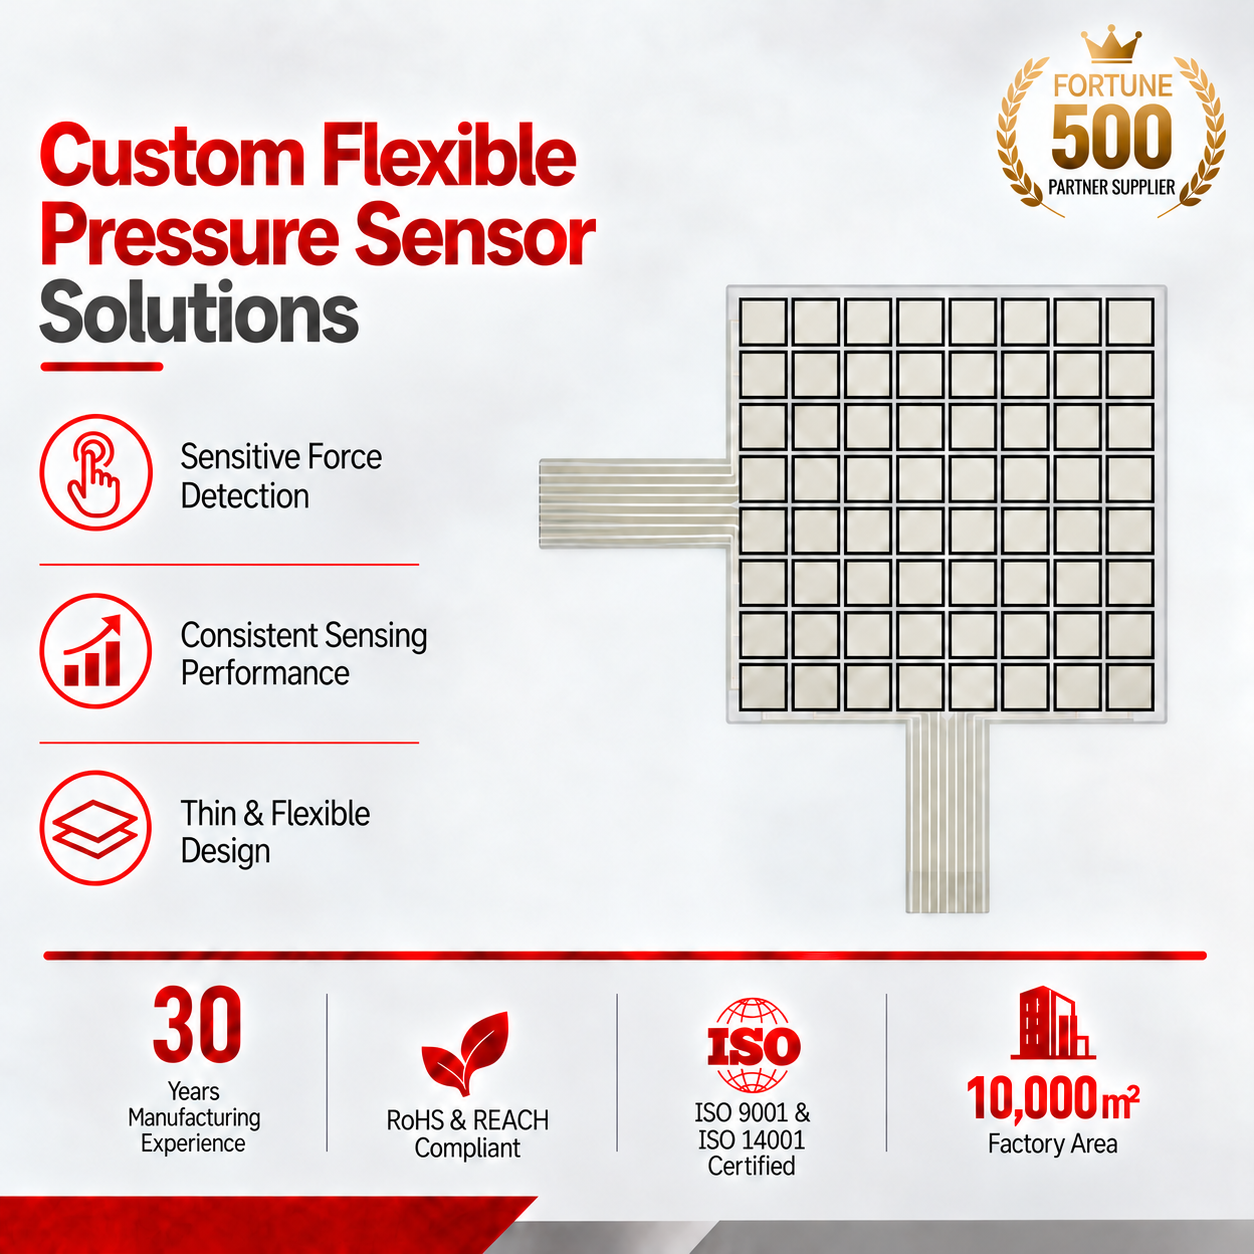
Customized Flexible Thin Film Intelligent Sensing Tactile Bend Pressure Sensors
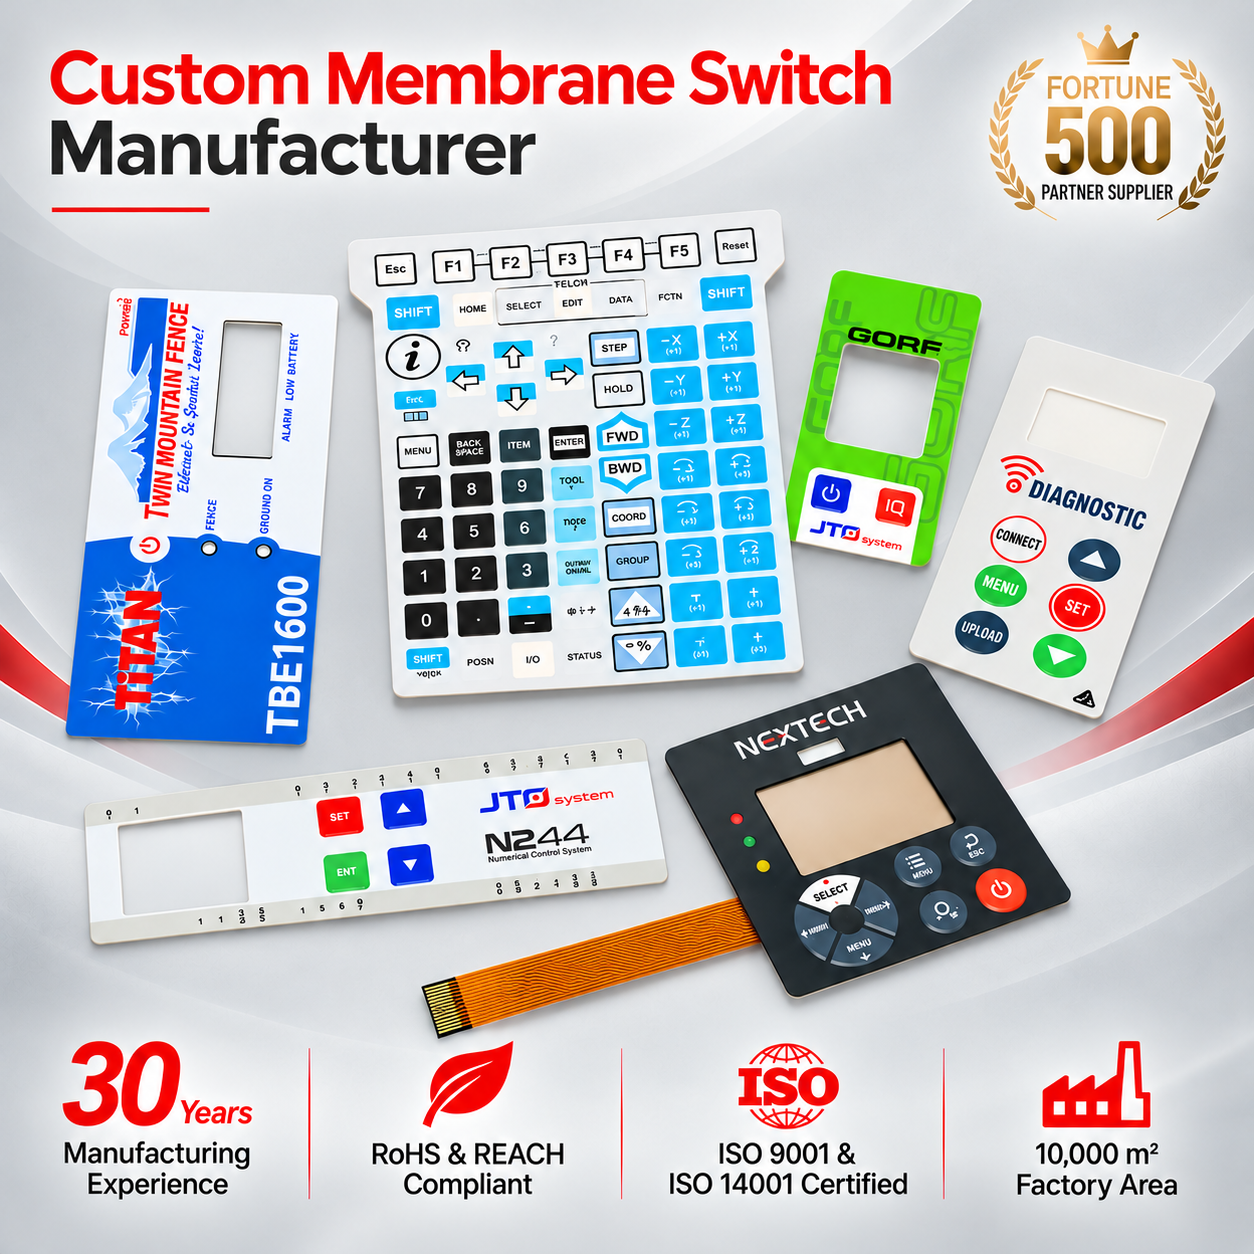
Factory Direct Membrane Switch Graphic Overlay Embossed Flat Industrial Panel
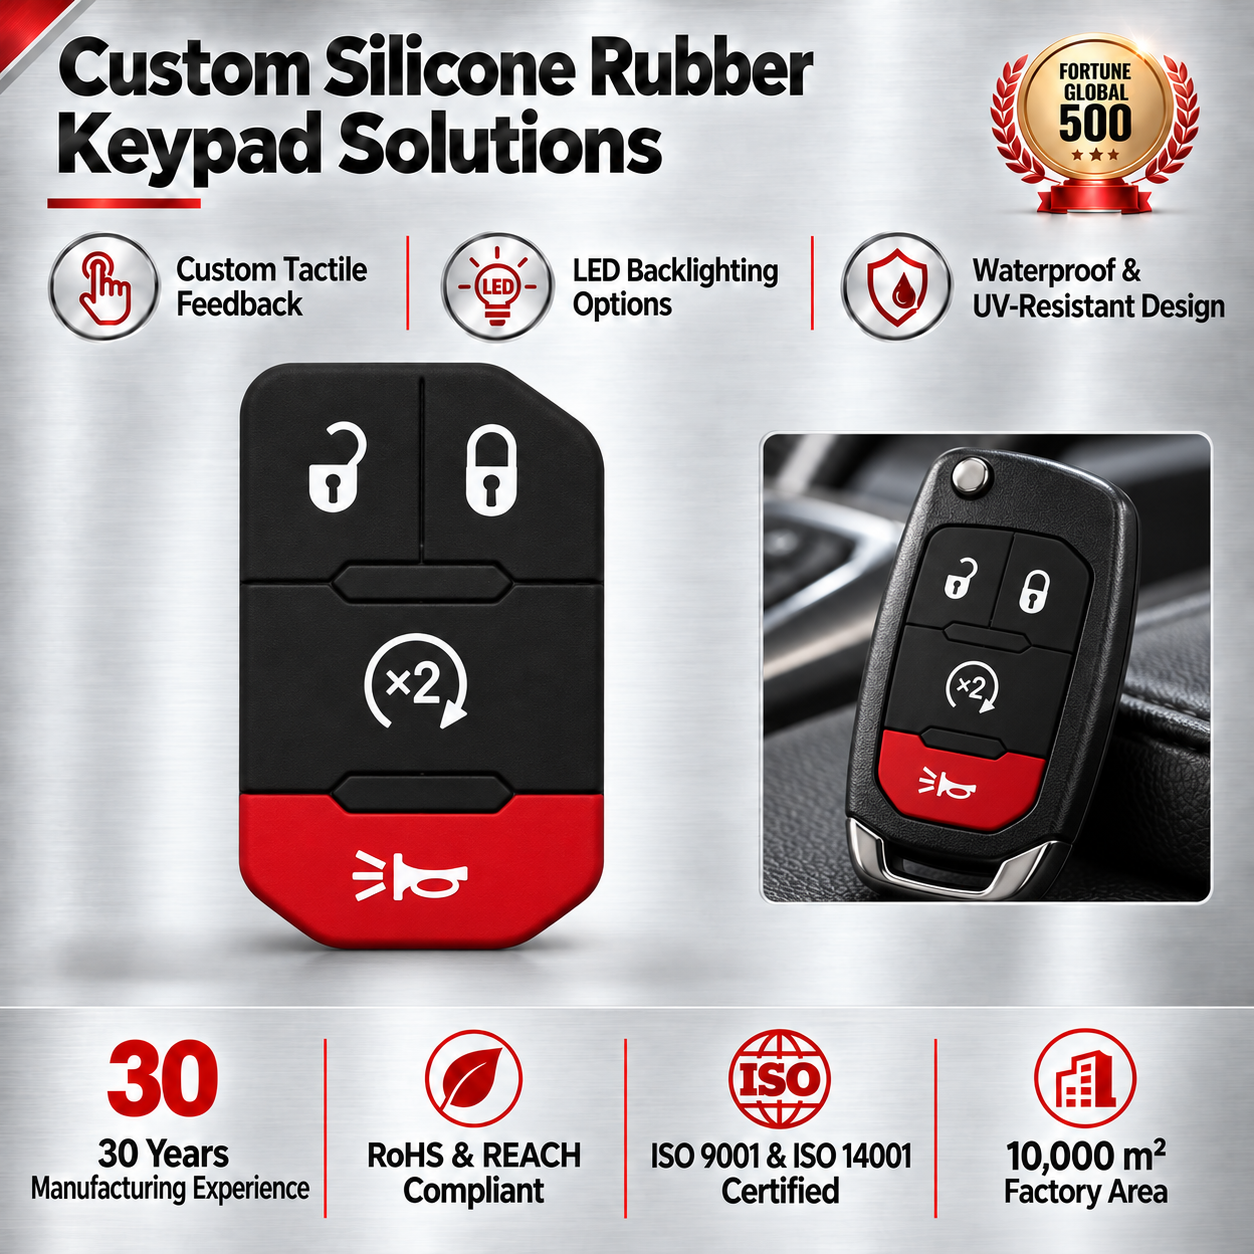
Waterproof Silicone Rubber Keypad Press Button 4 Buttons Vehicle Wholesale Unit
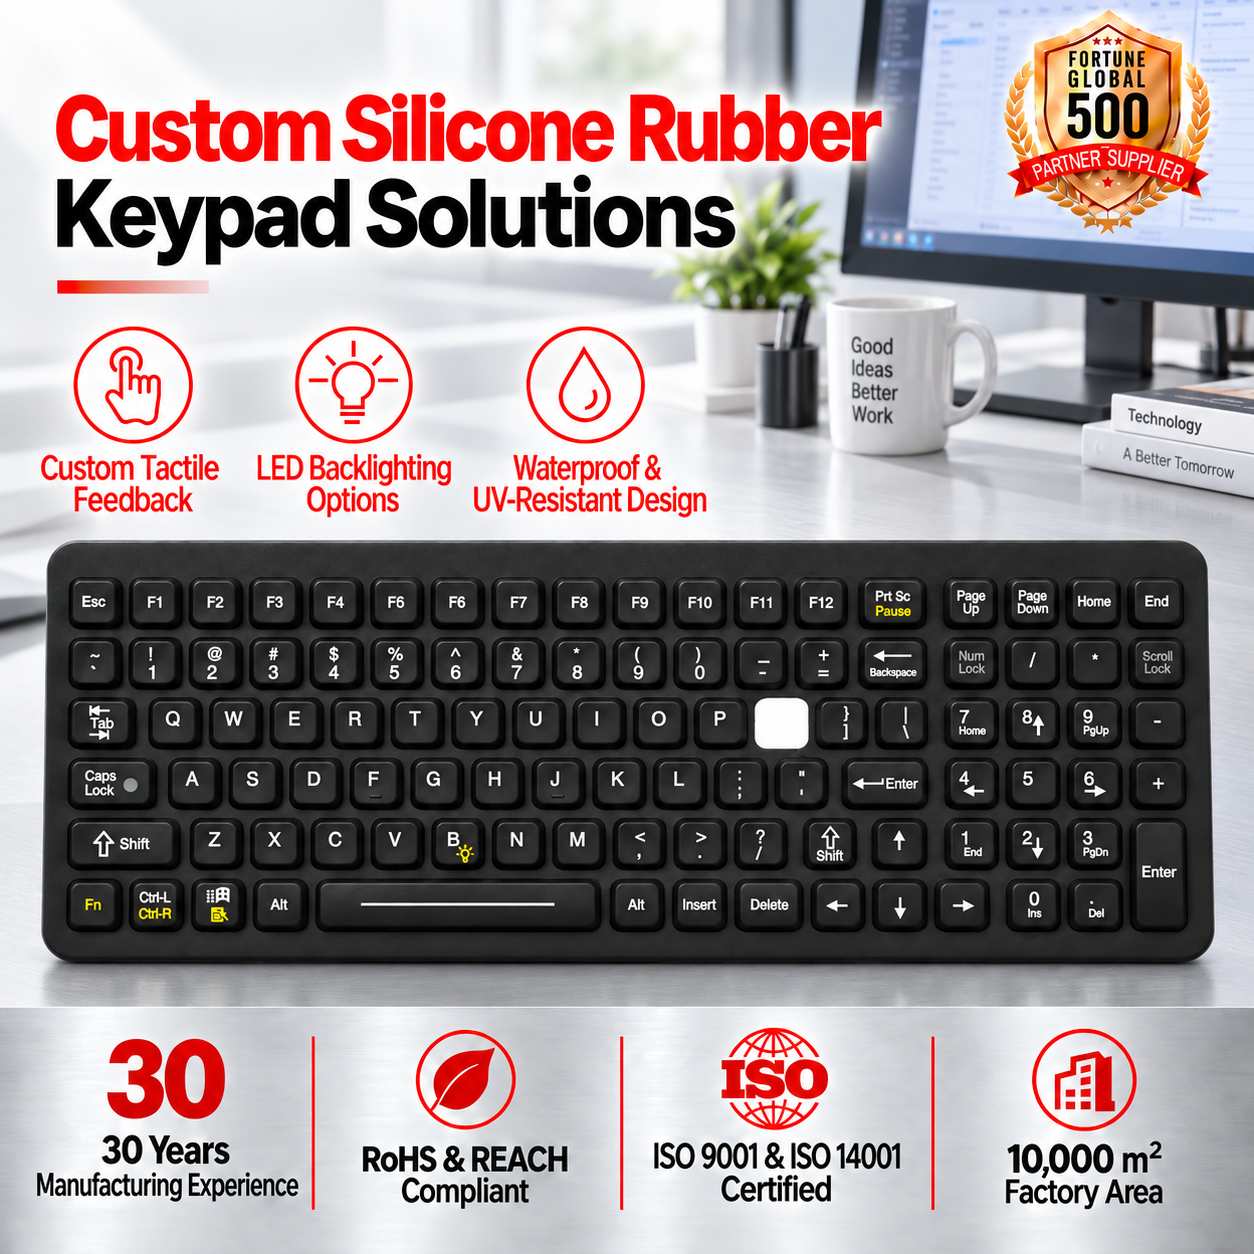
Industrial Silicone Keypad Rubber Button Conductive Non-Toxic Terminal Switch
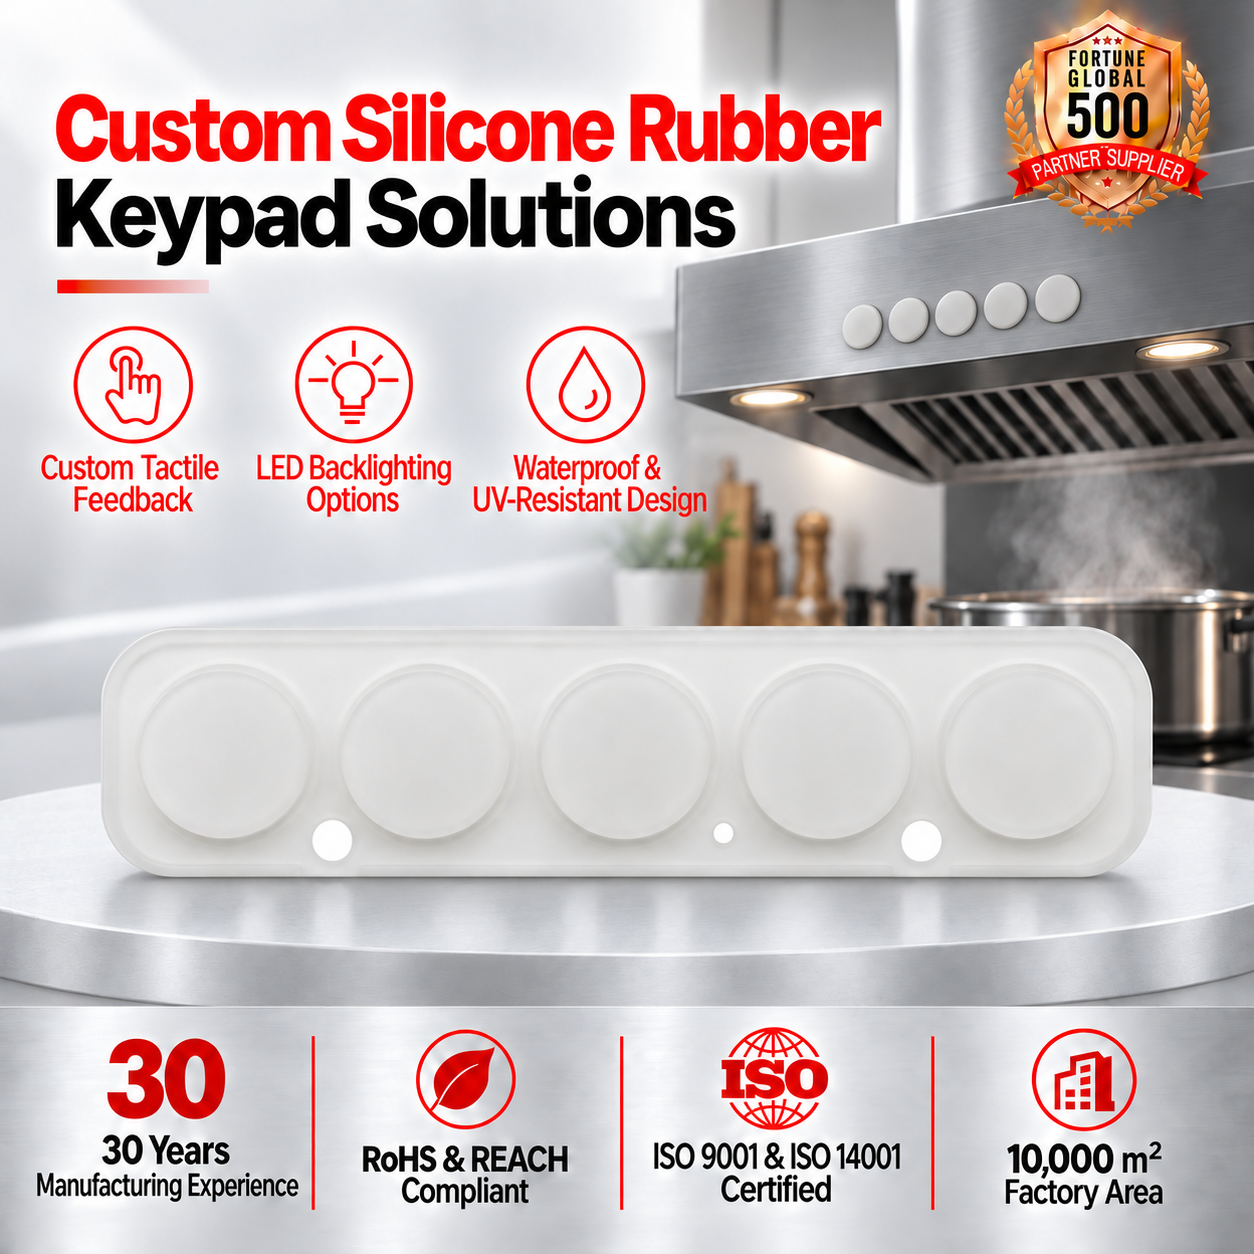
Home Appliance 5 Circular Soft Silicone Rubber Keypad Front Panel Momentary Unit
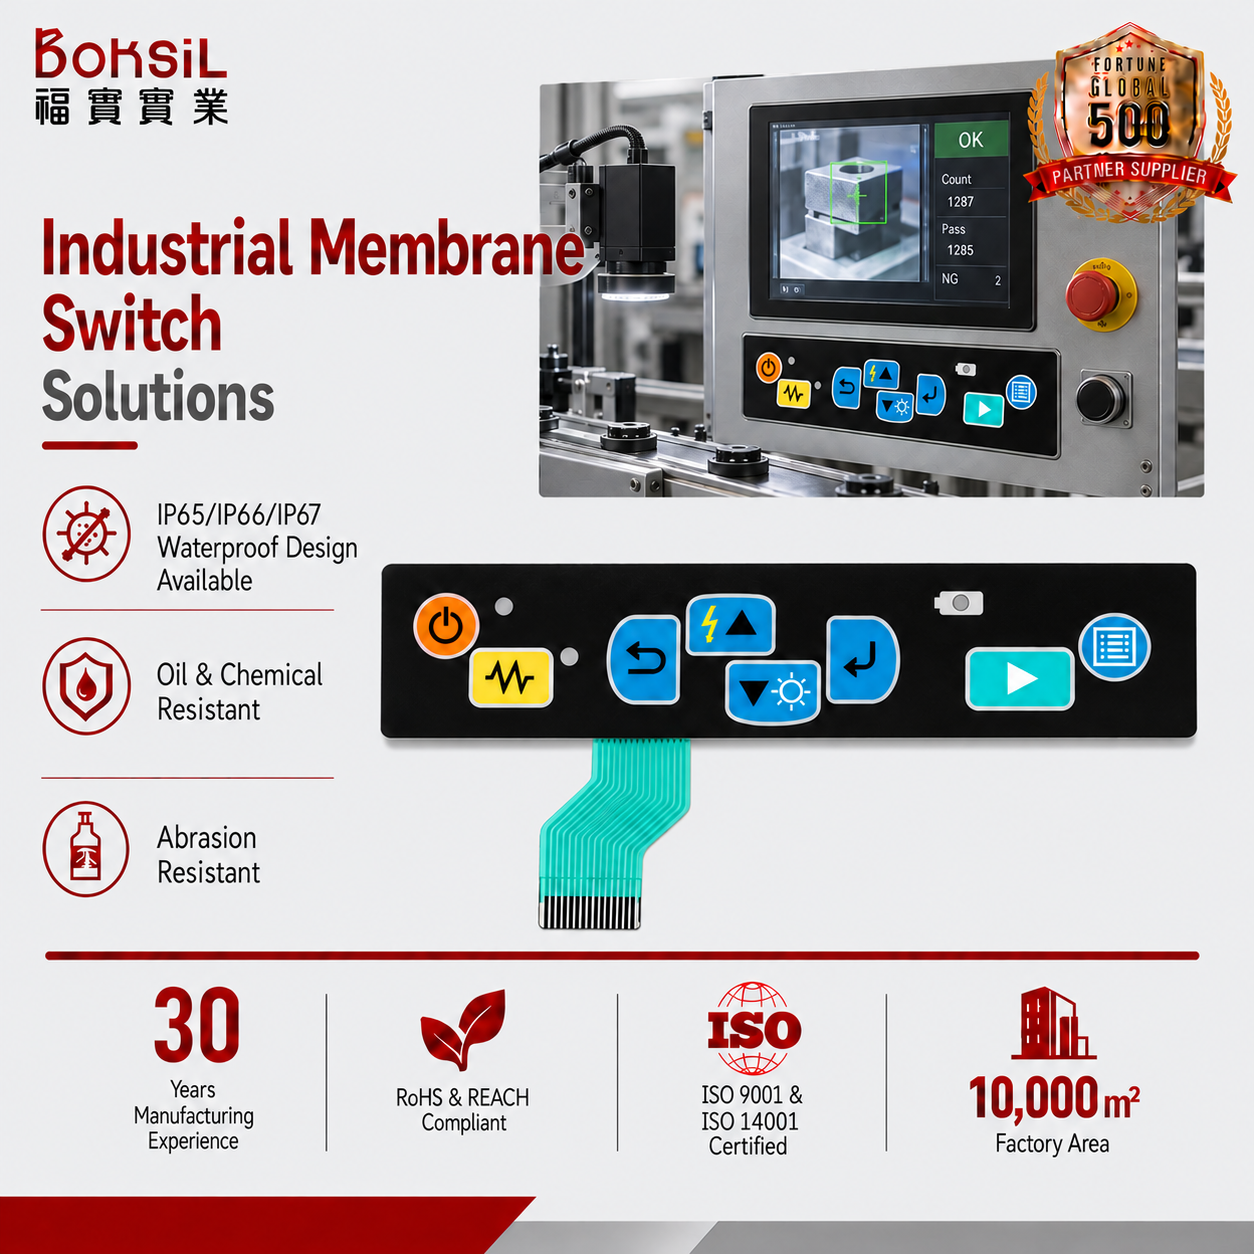
Capacitive Touch Screen Panel Screen Printing Graphic Overlay Membrane Switch
Optoelectronic Backlighting Topologies for Demanding HMIs
Achieving uniform luminance across complex graphic interfaces requires tailored illumination dynamics. We engineer optical light paths directly into the membrane stack-up to overcome environmental and spatial constraints.
Light Guide Film (LGF) Systems
Utilizing micro-etched optical-grade polycarbonate or PMMA layers (0.125mm to 0.250mm), LGF redirect light horizontally from perimeter side-firing SMD LEDs across target graphic zones. This topology delivers exceptional photometric homogeneity with minimal z-axis thickness, critical for slimline industrial interfaces.
Discrete SMD Embedded Arrays
Chip-on-flex (COF) surface-mount technology places miniature LEDs directly onto polyester (PET) or polyimide (FPC) circuitry. When matched with precision-machined light-blocking spacers and embossed dead-front windows, discrete arrays achieve zero light-bleed between adjacent control buttons with multi-color status reporting.
Electroluminescent (EL) Lamps
Ideal for ambient, low-light operational environments requiring cool phosphorescent glow. EL backlighting generates absolute surface uniformity without generating hot spots or thermal dissipation challenges, consuming low current while functioning reliably across severe sub-zero thermal extremes.
| Illumination Method | Z-Axis Profile (Thickness) | Luminance Uniformity | Power Consumption | Best Fit Scenario |
|---|---|---|---|---|
| Light Guide Film (LGF) | 0.2mm – 0.5mm | High (90%+ with micro-dots) | Low (Driven by 2-6 LEDs) | Handheld diagnostics, ultra-thin control consoles |
| Discrete SMT LEDs | 0.8mm – 1.6mm (requires dome clearance) | Targeted (Key-specific) | Scalable by active node | Status indicators, multi-color tactile keyboards |
| Electroluminescent (EL) | 0.15mm – 0.3mm | Very High (Continuous plane) | AC Inverter dependent (Medium) | Night-vision equipment, thermal spa control units |
| Fiber Optic Weave | 0.3mm – 0.6mm | Moderate to High | Extremely Low (1-2 central sources) | Explosive atmospheres (ATEX), high-EMI zones |
Contextual HMI Implementations in Escaldes-Engordany
Positioned in the Madriu-Perafita-Claror valley at the intersection of alpine tourism, balneotherapy, and modern commercial infrastructure, Escaldes-Engordany requires interface hardware that resists harsh environmental variables.
Thermal Spa & Hydrotherapy Controls
Escaldes-Engordany is world-renowned for natural thermal mineral waters. HMIs deployed in balneotherapy environments face relentless humidity, chlorine exposure, and sulfur-rich steam. We supply perimeter-sealed IP67 and IP68 membrane interfaces built with medical-grade silicone keypads, preventing trace gas corrosion and contact oxidation.
Ski Infrastructure & Sub-Alpine Telemetry
Lift access controls, piste grooming telemetry, and snowmaking terminal switches in the surrounding parish mountains endure wide thermal cycles from -25°C to +40°C. Our specialized polyester graphic overlays and cold-temperature conductive silver circuits resist brittle fracture, delamination, and tactile dome fatigue.
Commercial Building Automation & Retail
From luxury retail boutiques along Avinguda Carlemany to modern banking institutions and data infrastructure, our backlit capacitive touch panels and dead-front graphic overlays provide seamless, architectural-grade interfaces with anti-fingerprint and antimicrobial surface treatments.
Emerging Technology Trends for Pyrenean Smart Hardware
System designers in Andorra are transforming user interaction paradigms through material science, sensor fusion, and circular product design.
Transition from Discrete Switchgear to Unified In-Mold Interfaces
The convergence of decorative industrial styling and reliable switching has accelerated the adoption of In-Mold Decoration (IMD) and In-Mold Electronics (IME). By encapsulating structural electronics directly within molded polymer resin, devices achieve total ingress immunity, sleek aesthetics, and reduced assembly labour overhead for European electronics manufacturers.
Adaptive Haptic Capacitive & Force Sensing (FSR) Arrays
Standard capacitive switches can register false activations when wet—a frequent challenge in thermal wellness or snowy environments. By pairing thin-film Force Sensitive Resistors (FSR) with capacitive sensing matrices, our hybrid panels demand intentional actuation pressure before triggering a state change, delivering tactile certainty without mechanical wear components.
Factory-Direct Capabilities: Intertek-Verified Engineering
We eliminate quality variance by conducting 100% of printing, component integration, assembly, and reliability characterization in our Dongguan production headquarters.
Comprehensive DFM Verification
Before metal dies or silk screens are cut, our senior engineers complete an exhaustive Design For Manufacturability audit covering switch travel, snap ratio (40%–60%), tail routing, ESD shield dissipation, and adhesive stack shear properties.
Rigorous Laboratory Validation
Batch integrity is validated using automated force-displacement testers, key life cycle testers (guaranteed up to 5,000,000 cycles for stainless steel snap domes), ink decolorization abrasion rigs, and UV-accelerated yellowing resistance chambers.
Streamlined Global Logistics
With an export record spanning more than a decade to Fortune 500 equipment builders and European OEMs, we provide certified anti-static export packaging, rapid sample prototyping (5–7 days), and low batch MOQ thresholds (100 pieces).
Frequently Asked Questions for Escaldes-Engordany Importers
Answers to technical, regulatory, and shipping inquiries when sourcing custom human-machine interfaces from our factory.
How do you ensure membrane switch longevity in sub-zero Pyrenean alpine environments?
Low-temperature failure typically results from adhesive crystallization, micro-cracking of PET substrates, or loss of spring temper in actuation domes. For installations throughout Escaldes-Engordany and surrounding elevated regions, we specify premium 3M 200MP or 300LSE acrylic adhesives with working limits down to -40°C, employ biaxially-oriented, heat-stabilized polyester film (such as Autotex or Melinex), and install nickel-plated or gold-plated stainless steel metal domes with tested flex memory.
Can AXRU build interfaces resistant to mineralized thermal water and aggressive sanitation?
Yes. For hydrotherapy, balneotherapy, and clinical hygiene devices, we engineer perimeter ring gasket seals using closed-cell structural acrylic foams that achieve IP67 immersion ratings. Overlay surfaces are printed using chemically hard-coated PET materials resilient to alcohol, chloramines, mild acids, and detergent wipe-down cycles.
What engineering files and specifications are needed to initiate a tooling quotation?
To provide a detailed DFM appraisal and tooling quote, please provide your 2D CAD profile (DXF, DWG, or PDF) illustrating key boundaries, tail exit position, and cutouts; vector artwork (AI or vector PDF) with specified Pantone solid coated references; your electrical matrix or pinout assignment; and required environmental constraints (target IP rating, illumination preferences, and operating voltage).
What customs documentation and compliance standards accompany shipments into Andorra?
Shipments directed to Escaldes-Engordany (Principat d'Andorra) are supplied with commercial invoices, itemized packing lists, HS code designations, Certificate of Origin (COO), and RoHS/REACH compliance documentation. We regularly coordinate with DHL, FedEx, and freight forwarders via Barcelona-El Prat or Toulouse-Blagnac logistical hubs to ensure prompt clearance through Andorran Customs (Duana d'Andorra).
Can you support low-volume pilot runs prior to committing to mass production?
Yes. Our minimum order quantity starts at just 100 units for custom membrane switches and graphic overlays. For engineering prototypes, our dedicated sample-making department utilizes flatbed CNC cutting and digital proofing systems, delivering fully functioning physical evaluation units within 5 to 7 working days before cutting hard production tooling.
Ready to Build Your Custom HMI Interface?
Send your drawings, CAD files, or technical performance criteria to our senior engineering team. We deliver complete DFM feedback and competitive production quotes within 24 hours.